


ASTM B905-00(2016)
(Test Method)Standard Test Methods for Assessing the Adhesion of Metallic and Inorganic Coatings by the Mechanized Tape Test
Standard Test Methods for Assessing the Adhesion of Metallic and Inorganic Coatings by the Mechanized Tape Test
SIGNIFICANCE AND USE
4.1 If a coating is to fulfill its function of protecting or imparting unique properties to the surface of a substrate, it must adhere to the substrate for the expected service life. Because surface preparation (or lack of it) has a drastic effect on adhesion of coatings, a test method for evaluating adhesion to different surface treatments or of different coatings to the same treatment is of considerable use to the industry.
4.2 The limitations of all adhesion methods, and the specific limitation of this test method to lower levels of adhesion (see 1.3) should be recognized before using it. These test methods are mechanized adaptations of Test Methods D3359; therefore, the intra- and interlaboratory precision of these test methods are similar to Test Methods D3359 and to other widely-accepted tests for coated substrates, for example, Test Method D2370, but this is partly the result of it being insensitive to all but large differences in adhesion. The pass-fail scale of 0 to 5 for Method B1 and B2 was selected deliberately to avoid a false impression of being sensitive.
SCOPE
1.1 These test methods describe procedures for assessing the adhesion of metallic and inorganic coatings and other thin films to metallic and nonmetallic substrates. Assessment is made by applying pressure-sensitive tape to a coated surface and then utilizing a mechanical device to remove the tape at a regulated, uniform rate and constant angle while simultaneously recording the removal force.
1.2 Four methods are described. Methods A1 and A2 are intended primarily for use on parts. Methods B1 and B2 are intended primarily for use in laboratory evaluations. Methods B1 and B2 are not recommended for testing coatings and films on polymer substrates.
1.3 These test methods may be used to establish whether the adhesion of a coating to a substrate is within a required range (between a quantified low and a quantified high level). Determination of actual adhesive forces requires more sophisticated methods of measurement. In multilayer systems adhesion failure may occur between intermediate coating layers so that the adhesion of the total coating system to the substrate may not necessarily be determined.
1.4 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.5 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: B905 − 00 (Reapproved 2016)
Standard Test Methods for
Assessing the Adhesion of Metallic and Inorganic Coatings
by the Mechanized Tape Test
This standard is issued under the fixed designation B905; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope 2. Referenced Documents
2.1 ASTM Standards:
1.1 These test methods describe procedures for assessing
B183 Practice for Preparation of Low-Carbon Steel for
the adhesion of metallic and inorganic coatings and other thin
Electroplating
films to metallic and nonmetallic substrates. Assessment is
B242 Guide for Preparation of High-Carbon Steel for Elec-
made by applying pressure-sensitive tape to a coated surface
troplating
and then utilizing a mechanical device to remove the tape at a
B252 Guide for Preparation of Zinc Alloy Die Castings for
regulated, uniform rate and constant angle while simultane-
Electroplating and Conversion Coatings
ously recording the removal force.
B253 Guide for Preparation of Aluminum Alloys for Elec-
1.2 Four methods are described. Methods A1 and A2 are troplating
intended primarily for use on parts. Methods B1 and B2 are B254 Practice for Preparation of and Electroplating on
Stainless Steel
intended primarily for use in laboratory evaluations. Methods
B281 Practice for Preparation of Copper and Copper-Base
B1 and B2 are not recommended for testing coatings and films
Alloys for Electroplating and Conversion Coatings
on polymer substrates.
B320 Practice for Preparation of Iron Castings for Electro-
1.3 Thesetestmethodsmaybeusedtoestablishwhetherthe
plating
adhesion of a coating to a substrate is within a required range
B343 Practice for Preparation of Nickel for Electroplating
(between a quantified low and a quantified high level). Deter-
with Nickel
mination of actual adhesive forces requires more sophisticated
B480 Guide for Preparation of Magnesium and Magnesium
methods of measurement. In multilayer systems adhesion
Alloys for Electroplating
failure may occur between intermediate coating layers so that
B481 Practice for Preparation of Titanium and Titanium
the adhesion of the total coating system to the substrate may
Alloys for Electroplating
not necessarily be determined. B482 Practice for Preparation of Tungsten and Tungsten
Alloys for Electroplating
1.4 The values stated in SI units are to be regarded as
B537 Practice for Rating of Electroplated Panels Subjected
standard. No other units of measurement are included in this
to Atmospheric Exposure
standard.
B538 Method of FACT (Ford Anodized Aluminum Corro-
1.5 This standard does not purport to address all of the sion Test) (Withdrawn 1986)
B629 Practice for Preparation of Molybdenum and Molyb-
safety concerns, if any, associated with its use. It is the
denum Alloys for Electroplating
responsibility of the user of this standard to establish appro-
B630 Practice for Preparation of Chromium for Electroplat-
priate safety and health practices and determine the applica-
ing with Chromium
bility of regulatory limitations prior to use.
B727 Practice for Preparation of Plastics Materials for Elec-
troplating
D1730 Practices for Preparation of Aluminum and
Aluminum-Alloy Surfaces for Painting
1 2
These test methods are under the jurisdiction of ASTM Committee B08 on For referenced ASTM standards, visit the ASTM website, www.astm.org, or
Metallic and Inorganic Coatings and are the direct responsibility of Subcommittee contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
B08.10 onTest Methods. Standards volume information, refer to the standard’s Document Summary page on
Current edition approved Nov. 1, 2016. Published November 2016. Originally the ASTM website.
approved in 2000. Last previous edition approved in 2010 as B905 – 00 (2010). The last approved version of this historical standard is referenced on
DOI: 10.1520/B0905-00R16. www.astm.org.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B905 − 00 (2016)
D1731 Practices for Preparation of Hot-DipAluminum Sur- 5. Apparatus and Materials
faces for Painting
5.1 PeelTestFixture—Thefixtureshallconsistofaframeto
D1732 Practices for Preparation of Magnesium Alloy Sur-
which the specimen is rigidly clamped, and a moveable beam
faces for Painting
by which the tape is pulled off under a constant peel angle of
D2370 Test Method for Tensile Properties of Organic Coat-
90 (MethodA1 and B1) or 180° (MethodA2 and B2).The peel
ings
rate should be controllable between 20 mm/s and 200 mm/s for
D3330/D3330M TestMethodforPeelAdhesionofPressure-
Method A1 and B1 and between 14 mm/s and 140 mm/s for
Sensitive Tape
Methods A2 and B2. A recording force gage is fitted between
D3359 Test Methods for Measuring Adhesion by Tape Test
the tape grip and the movable beam (see Fig. 1).
5.2 Pressure-Sensitive Tape—Unless otherwise specified in
3. Summary of Test Method
the document referencing this test, the tape shall be 25 mm
3.1 Pressure-sensitive tape is adhered to the surface of the
wide,semitransparent,pressure-sensitivetapewithanadhesion
coating and then removed utilizing a motorized mechanical
strength of 43 6 5.6 g/mm or N/100 mm width when tested in
device that peels the tape at a constantly maintained angle and
accordance with D3330/D3330M. The adhesion shall not
controlled rate of peel.Adigital recording force gage is used to
change by more than + 6.5 % of its mean value within 12
record the maximum peel force.
months.Thebackingofthetapemayconsistoffiber-reinforced
cellulose acetate, unplasticized poly (vinyl chloride), or poly-
NOTE 1—All due care must be taken to ensure that test specimens are
ester film. When results obtained in different laboratories do
handled and stored such that they are not subjected to conditions that will
notagreeitisrecommendedthatthetestberepeatedusingtape
cause deleterious effects. These conditions include but are not limited to
handling without the use of gloves, storing in areas that accumulate dust,
from the same batch.
areas of high humidity or where the sample may be subjected to fumes or
5.3 Roller—The roller, which is hand operated, consists of
vapors that might condense on the sample.
a steel roller 85 6 2.5 mm in diameter and 45 6 1.5 mm in
3.2 Methods A1 and A2:
width, covered with rubber approximately 6 mm in thickness,
3.2.1 In these methods, which are nondestructive, the mea-
having a Shore scale A durometer hardness of 80 6 5. The
surement area used is the unbroken coating surface with peel
surfaceoftherollershallbeatruecylindervoidofanyconcave
angles of 90 and 180° respectively.
orconvexdeviations.Themassoftherollershallbe2040 645
3.2.2 Adhesion is assessed in terms of “passed,” if the
g.
coating does not detach, or “failed,” if the coating detaches
NOTE 2—A standardized roller is used in place of the pencil eraser of
within the specified range of peel forces as recorded during the
Test Methods D3359 because of the variety of rubber and abrasives
test.
formulations used to make pencil erasers.Afurther consideration was the
extended range of localized pressures that could be exerted by the pencil
3.3 Methods B1 and B2:
and eraser.
3.3.1 In these methods, which are destructive, the measure-
ment area used is a broken coating surface created by scoring
TEST METHOD A
alatticepatternthroughthecoatingtothesubstrateandpeeling
NONDESTRUCTIVE, PARTS TAPE TEST
at angles of 90 and 180°, respectively.
3.3.2 Adhesion is assessed qualitatively on the 0 to 5 scale.
6. Test Specimen
6.1 Parts—This test normally is performed on parts. Any
4. Significance and Use
requirements for test specimens will be found in the document
4.1 If a coating is to fulfill its function of protecting or specifying their use.
imparting unique properties to the surface of a substrate, it
NOTE 3—When specified by the document referencing this test, the
must adhere to the substrate for the expected service life.
coated parts shall be subjected to a preliminary exposure, such as water
Because surface preparation (or lack of it) has a drastic effect immersion, salt spray, or humidity, before conducting the tape test.
on adhesion of coatings, a test method for evaluating adhesion
7. Procedure
to different surface treatments or of different coatings to the
7.1 Test Area—Select a flat area, on a significant surface,
same treatment is of considerable use to the industry.
free of blemishes and minor surface imperfections. Ensure that
4.2 The limitations of all adhesion methods, and the specific
the surface is clean and dry. Extremes in temperature or
limitation of this test method to lower levels of adhesion (see
relative humidity may affect the adhesion of the tape or the
1.3) should be recognized before using it. These test methods
coating.
are mechanized adaptations of Test Methods D3359; therefore,
7.2 Tape Section—Remove two complete laps of the
the intra- and interlaboratory precision of these test methods
pressure-sensitive tape from the roll and discard. Remove an
are similar to Test Methods D3359 and to other widely-
accepted tests for coated substrates, for example, Test Method
The sole source of supply of the apparatus known to the committee at this time
D2370, but this is partly the result of it being insensitive to all
is Pressure-Sensitive Tape Council (PSTC), 104 Wilmot Rd., Suite 201, Deerfield,
but large differences in adhesion. The pass-fail scale of 0 to 5
IL 60015. If you are aware of alternative suppliers, please provide this information
for Method B1 and B2 was selected deliberately to avoid a
to ASTM International Headquarters. Your comments will receive careful consid-
false impression of being sensitive. eration at a meeting of the responsible technical committee, which you may attend.
B905 − 00 (2016)
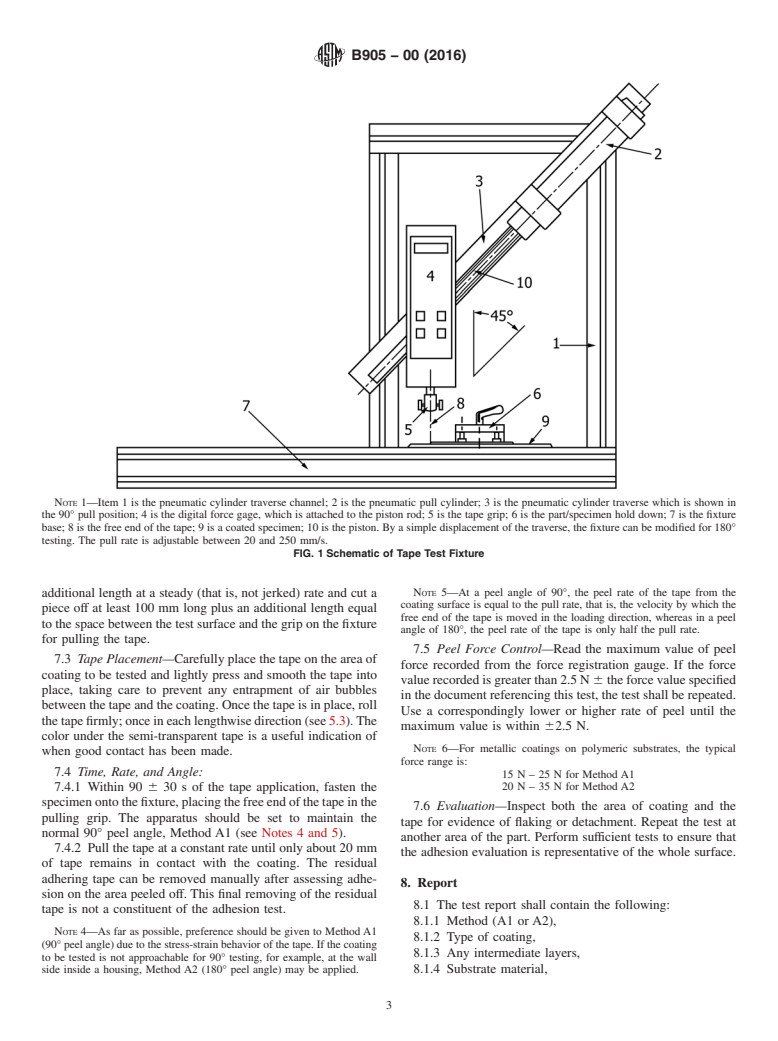
NOTE 1—Item 1 is the pneumatic cylinder traverse channel; 2 is the pneumatic pull cylinder; 3 is the pneumatic cylinder traverse which is shown in
the 90° pull position; 4 is the digital force gage, which is attached to the piston rod; 5 is the tape grip; 6 is the part/specimen hold down; 7 is the fixture
base; 8 is the free end of the tape; 9 is a coated specimen; 10 is the piston. By a simple displacement of the traverse, the fixture can be modified for 180°
testing. The pull rate is adjustable between 20 and 250 mm/s.
FIG. 1 Schematic of Tape Test Fixture
NOTE 5—At a peel angle of 90°, the peel rate of the tape from the
additional length at a steady (that is, not jerked) rate and cut a
coating surface is equal to the pull rate, that is, the velocity by which the
piece off at least 100 mm long plus an additional length equal
free end of the tape is moved in the loading direction, whereas in a
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B905 − 00 (Reapproved 2010) B905 − 00 (Reapproved 2016)
Standard Test Methods for
Assessing the Adhesion of Metallic and Inorganic Coatings
by the Mechanized Tape Test
This standard is issued under the fixed designation B905; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 These test methods describe procedures for assessing the adhesion of metallic and inorganic coatings and other thin films
to metallic and nonmetallic substrates. Assessment is made by applying pressure-sensitive tape to a coated surface and then
utilizing a mechanical device to remove the tape at a regulated, uniform rate and constant angle while simultaneously recording
the removal force.
1.2 Four methods are described. Methods A1 and A2 are intended primarily for use on parts. Methods B1 and B2 are intended
primarily for use in laboratory evaluations. Methods B1 and B2 are not recommended for testing coatings and films on polymer
substrates.
1.3 These test methods may be used to establish whether the adhesion of a coating to a substrate is within a required range
(between a quantified low and a quantified high level). Determination of actual adhesive forces requires more sophisticated
methods of measurement. In multilayer systems adhesion failure may occur between intermediate coating layers so that the
adhesion of the total coating system to the substrate may not necessarily be determined.
1.4 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.5 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use.
2. Referenced Documents
2.1 ASTM Standards:
B183 Practice for Preparation of Low-Carbon Steel for Electroplating
B242 Guide for Preparation of High-Carbon Steel for Electroplating
B252 Guide for Preparation of Zinc Alloy Die Castings for Electroplating and Conversion Coatings
B253 Guide for Preparation of Aluminum Alloys for Electroplating
B254 Practice for Preparation of and Electroplating on Stainless Steel
B281 Practice for Preparation of Copper and Copper-Base Alloys for Electroplating and Conversion Coatings
B320 Practice for Preparation of Iron Castings for Electroplating
B343 Practice for Preparation of Nickel for Electroplating with Nickel
B480 Guide for Preparation of Magnesium and Magnesium Alloys for Electroplating
B481 Practice for Preparation of Titanium and Titanium Alloys for Electroplating
B482 Practice for Preparation of Tungsten and Tungsten Alloys for Electroplating
B537 Practice for Rating of Electroplated Panels Subjected to Atmospheric Exposure
B538 Method of FACT (Ford Anodized Aluminum Corrosion Test) (Withdrawn 1986)
B629 Practice for Preparation of Molybdenum and Molybdenum Alloys for Electroplating
B630 Practice for Preparation of Chromium for Electroplating with Chromium
B727 Practice for Preparation of Plastics Materials for Electroplating
These test methods are under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and are the direct responsibility of Subcommittee B08.10
onTest Methods.
Current edition approved April 1, 2010Nov. 1, 2016. Published June 2010November 2016. Originally approved in 2000. Last previous edition approved in 20052010 as
B905 – 00 (2005).(2010). DOI: 10.1520/B0905-00R10.10.1520/B0905-00R16.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
The last approved version of this historical standard is referenced on www.astm.org.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B905 − 00 (2016)
D1730 Practices for Preparation of Aluminum and Aluminum-Alloy Surfaces for Painting
D1731 Practices for Preparation of Hot-Dip Aluminum Surfaces for Painting
D1732 Practices for Preparation of Magnesium Alloy Surfaces for Painting
D2370 Test Method for Tensile Properties of Organic Coatings
D3330/D3330M Test Method for Peel Adhesion of Pressure-Sensitive Tape
D3359 Test Methods for Measuring Adhesion by Tape Test
3. Summary of Test Method
3.1 Pressure-sensitive tape is adhered to the surface of the coating and then removed utilizing a motorized mechanical device
that peels the tape at a constantly maintained angle and controlled rate of peel. A digital recording force gage is used to record the
maximum peel force.
NOTE 1—All due care must be taken to ensure that test specimens are handled and stored such that they are not subjected to conditions that will cause
deleterious effects. These conditions include but are not limited to handling without the use of gloves, storing in areas that accumulate dust, areas of high
humidity or where the sample may be subjected to fumes or vapors that might condense on the sample.
3.2 Methods A1 and A2:
3.2.1 In these methods, which are nondestructive, the measurement area used is the unbroken coating surface with peel angles
of 90 and 180° respectively.
3.2.2 Adhesion is assessed in terms of “passed,” if the coating does not detach, or “failed,” if the coating detaches within the
specified range of peel forces as recorded during the test.
3.3 Methods B1 and B2:
3.3.1 In these methods, which are destructive, the measurement area used is a broken coating surface created by scoring a lattice
pattern through the coating to the substrate and peeling at angles of 90 and 180°, respectively.
3.3.2 Adhesion is assessed qualitatively on the 0 to 5 scale.
4. Significance and Use
4.1 If a coating is to fulfill its function of protecting or imparting unique properties to the surface of a substrate, it must adhere
to the substrate for the expected service life. Because surface preparation (or lack of it) has a drastic effect on adhesion of coatings,
a test method for evaluating adhesion to different surface treatments or of different coatings to the same treatment is of considerable
use to the industry.
4.2 The limitations of all adhesion methods, and the specific limitation of this test method to lower levels of adhesion (see 1.3)
should be recognized before using it. These test methods are mechanized adaptations of Test Methods D3359; therefore, the intra-
and interlaboratory precision of these test methods are similar to Test Methods D3359 and to other widely-accepted tests for coated
substrates, for example, Test Method D2370, but this is partly the result of it being insensitive to all but large differences in
adhesion. The pass-fail scale of 0 to 5 for Method B1 and B2 was selected deliberately to avoid a false impression of being
sensitive.
5. Apparatus and Materials
5.1 Peel Test Fixture—The fixture shall consist of a frame to which the specimen is rigidly clamped, and a moveable beam by
which the tape is pulled off under a constant peel angle of 90 (Method A1 and B1) or 180° (Method A2 and B2). The peel rate
should be controllable between 20 mm/s and 200 mm/s for Method A1 and B1 and between 14 mm/s and 140 mm/s for Methods
A2 and B2. A recording force gage is fitted between the tape grip and the movable beam (see Fig. 1).
5.2 Pressure-Sensitive Tape—Unless otherwise specified in the document referencing this test, the tape shall be 25 mm wide,
semitransparent, pressure-sensitive tape with an adhesion strength of 43 6 5.6 g/mm or N/100 mm width when tested in
accordance with D3330/D3330M. The adhesion shall not change by more than + 6.5 % of its mean value within 12 months. The
backing of the tape may consist of fiber-reinforced cellulose acetate, unplasticized poly (vinyl chloride), or polyester film. When
results obtained in different laboratories do not agree it is recommended that the test be repeated using tape from the same batch.
5.3 Roller—The roller, which is hand operated, consists of a steel roller 85 6 2.5 mm in diameter and 45 6 1.5 mm in width,
covered with rubber approximately 6 mm in thickness, having a Shore scale A durometer hardness of 80 6 5. The surface of the
roller shall be a true cylinder void of any concave or convex deviations. The mass of the roller shall be 2040 6 45 g.
NOTE 2—A standardized roller is used in place of the pencil eraser of Test Methods D3359 because of the variety of rubber and abrasives formulations
used to make pencil erasers. A further consideration was the extended range of localized pressures that could be exerted by the pencil and eraser.
The sole source of supply of the apparatus known to the committee at this time is Pressure-Sensitive Tape Council (PSTC), 104 Wilmot Rd., Suite 201, Deerfield, IL
60015. If you are aware of alternative suppliers, please provide this information to ASTM International Headquarters. Your comments will receive careful consideration at
a meeting of the responsible technical committee, which you may attend.
B905 − 00 (2016)
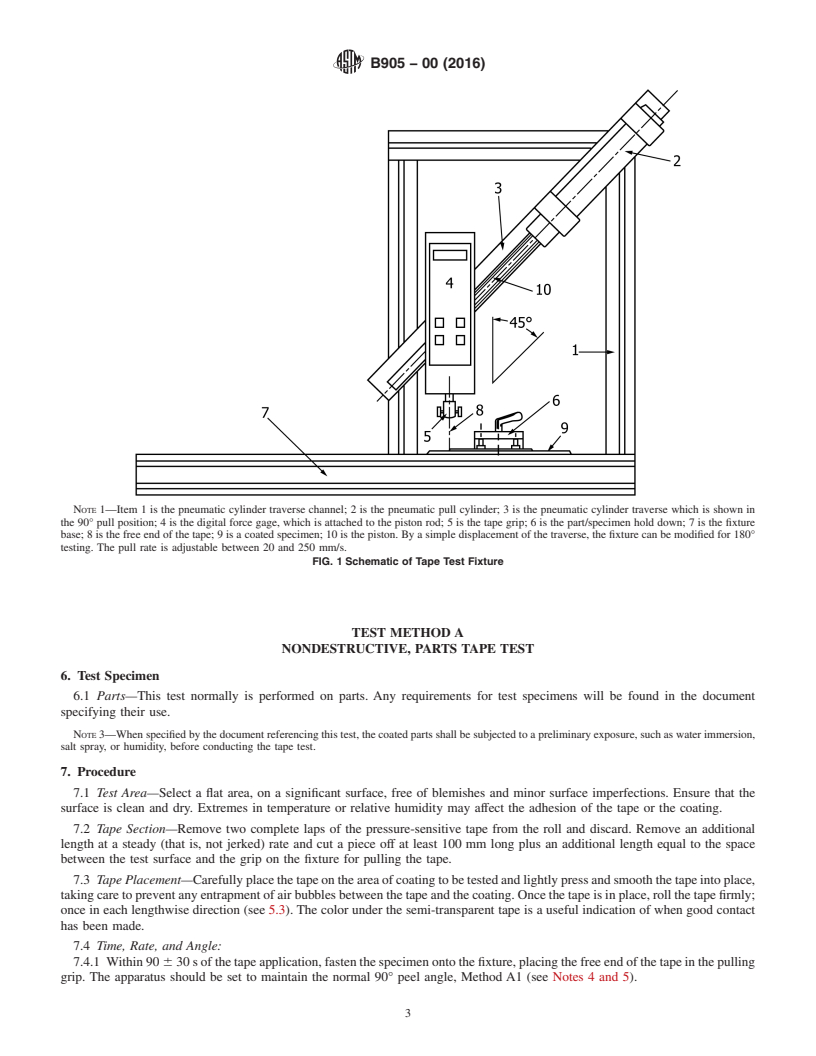
NOTE 1—Item 1 is the pneumatic cylinder traverse channel; 2 is the pneumatic pull cylinder; 3 is the pneumatic cylinder traverse which is shown in
the 90° pull position; 4 is the digital force gage, which is attached to the piston rod; 5 is the tape grip; 6 is the part/specimen hold down; 7 is the fixture
base; 8 is the free end of the tape; 9 is a coated specimen; 10 is the piston. By a simple displacement of the traverse, the fixture can be modified for 180°
testing. The pull rate is adjustable between 20 and 250 mm/s.
FIG. 1 Schematic of Tape Test Fixture
TEST METHOD A
NONDESTRUCTIVE, PARTS TAPE TEST
6. Test Specimen
6.1 Parts—This test normally is performed on parts. Any requirements for test specimens will be found in the document
specifying their use.
NOTE 3—When specified by the document referencing this test, the coated parts shall be subjected to a preliminary exposure, such as water immersion,
salt spray, or humidity, before conducting the tape test.
7. Procedure
7.1 Test Area—Select a flat area, on a significant surface, free of blemishes and minor surface imperfections. Ensure that the
surface is clean and dry. Extremes in temperature or relative humidity may affect the adhesion of the tape or the coating.
7.2 Tape Section—Remove two complete laps of the pressure-sensitive tape from the roll and discard. Remove an additional
length at a steady (that is, not jerked) rate and cut a piece off at least 100 mm long plus an additional length equal to the space
between the test surface and the grip on the fixture for pulling the tape.
7.3 Tape Placement—Carefully place the tape on the area of coating to be tested and lightly press and smooth the tape into place,
taking care to prevent any entrapment of air bubbles between the tape and the coating. Once the tape is in place, roll the tape firmly;
once in each lengthwise direction (see 5.3). The color under the semi-transparent tape is a useful indication of when good contact
has been made.
7.4 Time, Rate, and Angle:
7.4.1 Within 90 6 30 s of the tape application, fasten the specimen onto the fixture, placing the free end of the tape in the pulling
grip. The apparatus should be set to maintain the normal 90° peel angle, Method A1 (see Notes 4 and 5).
B905 − 00 (2016)
7.4.2 Pull the tape at a constant rate until only about 20 mm of tape remains in contact with the coating. The residual adhering
tape can be removed manually after assessing adhesion on the area peeled off. This final removing of the residual tape is not a
constituent of the adhesion test.
NOTE 4—As far as possible, preference should be given to Method A1 (90° peel angle) due to the stress-strain behavior of the tape. If the coating to
be tested is not approachable for 90° testing, for example, at the wall side inside a housing, Method A2 (180° peel angle) may be applied.
NOTE 5—At a peel angle of 90°, the peel rate of the tape from the coating surface is equal to the pull rate, that is, the velocity by which the free end
of the tape is moved in the loading direction, whereas in a peel angle of 180°, the peel rate of the tape is only half the pull rate.
7.5 Peel Force Control—Read the maximum value of peel force recorded from the force registration gauge. If the force value
recorded is greater than 2.5 N 6 the force value specified in the document referencing this test, the test shall be repeated. Use a
correspondingly lower or higher rate of peel until the maximum value is within 62.5 N.
NOTE 6—For metallic coatings on polymeric substrates, the typical force range is:
15 N – 25 N for Method A1
20 N – 35 N for Method A2
7.6 Evaluation—Inspect both the area of coating and the tape for evidence of flaking or detachment. Repeat the test at another
area of the part. Perform sufficient tests to ensure that the adhesion evaluation is representative of the whole surface.
8. Report
8.1 The test report shall contain the following:
8.1.1 Method (A1 or A2),
8.1.2 Type of coating,
8.1.3 Any intermediate layers,
8.1.4 Substrate material,
8.1.5 Type of tape used,
8.1.6 Peel angle,
8.1.7 Rate of peel,
8.1.8 Any environmental exposure, and
8.1.9 Any failure at intermediate layers.
8.2 Report the test results as:
p/F (1)
max
or
f/F (2)
max
where:
p = passed (no coating detachment),
f = failed (coating detachment), and
F = maximum registered peel force.
max
9. Precision of Test Method A
9.1 An interlaboratory study of this test method reviewed tape peel measurements on various coatings under several peel
conditions. The results showed that maximum peel force of the tape depended significantly on the type of coating, the type of tape,
the peel rate and the peel angle. There was an insignificant relationship to the pressure used for adhering the tape to the coating.
9.2 The results of coating adhesion assessments obtained on different coatings should only be compared when the maximum
deviation recorded, does not exceed 62.5 N.
9.3 The results of coating adhesion assessments obtained with Method A1 should not be compared with the resul
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.