


ASTM B605-95a(2015)
(Specification)Standard Specification for Electrodeposited Coatings of Tin-Nickel Alloy
Standard Specification for Electrodeposited Coatings of Tin-Nickel Alloy
ABSTRACT
This specification establishes the requirements for electrodeposited tin-nickel alloy coatings from aqueous solutions intended for the corrosion protection of fabricated articles of iron, steel, zinc-base alloys, copper, and copper alloys. This specification does not apply to sheets, strips, or wires in the fabricated form. It also may not be applicable to finely threaded articles, but the decision to use the coating on such components may be made by the purchaser. Coating grades shall be designated by a service condition number, which indicates the severity of exposure for which the coating is intended, and a coating thickness notation. Iron and steel specimens shall undergo pre- and post-coating treatments for reducing the risk of hydrogen embrittlement. Coatings shall be sampled, tested, and conform to specified requirements as to appearance (visible defects), composition, thickness (assessed either by microscopical, magnetic, coulometric, beta backscatter, or X-ray spectrometry), adhesion (determined either by burnishing, or heat-quench test), and integrity (including gross defects, mechanical damage, and porosity).
SCOPE
1.1 This specification covers the requirements for electrodeposited tin-nickel alloy coatings from aqueous solutions intended for the corrosion protection of fabricated articles of iron, steel, zinc-base alloys, copper, and copper alloys. The composition of the alloy remains constant at 65/35 tin-nickel in spite of wide fluctuations in both composition and operating conditions. The composition corresponds quite closely to an equiatomic ratio, and the process favors the co-deposition of tin and nickel atoms at identical rates.
1.2 This specification does not apply to sheet, strip, or wire in the fabricated form. It also may not be applicable to threaded articles having basic major diameters up to and including 19 mm because of the nonuniformity of thickness that can be expected on fine threads. However, a decision to use the coating on such components may be made by the purchaser.
1.3 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:B605 −95a (Reapproved 2015)
Standard Specification for
Electrodeposited Coatings of Tin-Nickel Alloy
This standard is issued under the fixed designation B605; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope B252Guide for Preparation of Zinc Alloy Die Castings for
Electroplating and Conversion Coatings
1.1 Thisspecificationcoverstherequirementsforelectrode-
B281Practice for Preparation of Copper and Copper-Base
posited tin-nickel alloy coatings from aqueous solutions in-
Alloys for Electroplating and Conversion Coatings
tended for the corrosion protection of fabricated articles of
B322Guide for Cleaning Metals Prior to Electroplating
iron, steel, zinc-base alloys, copper, and copper alloys. The
B374Terminology Relating to Electroplating
compositionofthealloyremainsconstantat65/35tin-nickelin
B487Test Method for Measurement of Metal and Oxide
spite of wide fluctuations in both composition and operating
Coating Thickness by Microscopical Examination of
conditions. The composition corresponds quite closely to an
Cross Section
equiatomic ratio, and the process favors the co-deposition of
B499Test Method for Measurement of CoatingThicknesses
tin and nickel atoms at identical rates.
by the Magnetic Method: Nonmagnetic Coatings on
1.2 This specification does not apply to sheet, strip, or wire
Magnetic Basis Metals
inthefabricatedform.Italsomaynotbeapplicabletothreaded
B504Test Method for Measurement of Thickness of Metal-
articles having basic major diameters up to and including 19
lic Coatings by the Coulometric Method
mm because of the nonuniformity of thickness that can be
B507Practice for Design ofArticles to Be Electroplated on
expected on fine threads. However, a decision to use the
Racks
coating on such components may be made by the purchaser.
B567Test Method for Measurement of Coating Thickness
by the Beta Backscatter Method
1.3 The values stated in SI units are to be regarded as
standard. No other units of measurement are included in this B568Test Method for Measurement of Coating Thickness
by X-Ray Spectrometry
standard.
B571Practice for Qualitative Adhesion Testing of Metallic
1.4 This standard does not purport to address all of the
Coatings
safety concerns, if any, associated with its use. It is the
B602Test Method for Attribute Sampling of Metallic and
responsibility of the user of this standard to establish appro-
Inorganic Coatings
priate safety and health practices and determine the applica-
B634Specification for Electrodeposited Coatings of Rho-
bility of regulatory limitations prior to use.
dium for Engineering Use
B697Guide for Selection of Sampling Plans for Inspection
2. Referenced Documents
of Electrodeposited Metallic and Inorganic Coatings
2.1 ASTM Standards:
B762Test Method of Variables Sampling of Metallic and
B183Practice for Preparation of Low-Carbon Steel for
Inorganic Coatings
Electroplating
B765GuideforSelectionofPorosityandGrossDefectTests
B242Guide for Preparation of High-Carbon Steel for Elec-
for Electrodeposits and Related Metallic Coatings
troplating
B809Test Method for Porosity in Metallic Coatings by
B246Specification for Tinned Hard-Drawn and Medium-
Humid Sulfur Vapor (“Flowers-of-Sulfur”)
Hard-Drawn Copper Wire for Electrical Purposes
B849Specification for Pre-Treatments of Iron or Steel for
Reducing Risk of Hydrogen Embrittlement
B850GuideforPost-CoatingTreatmentsofSteelforReduc-
This specification is under the jurisdiction of ASTM Committee B08 on
Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee ing the Risk of Hydrogen Embrittlement
B08.06 on Soft Metals.
D3951Practice for Commercial Packaging
Current edition approved March 1, 2015. Published April 2015. Originally
approved in 1975. Last previous edition approved in 2009 as B605–95a(2009).
3. Terminology
DOI: 10.1520/B0605-95AR15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
3.1 Definitions:
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
3.1.1 Many terms used in this standard are defined in
Standards volume information, refer to the standard’s Document Summary page on
the ASTM website. Terminology B374.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B605−95a (2015)
TABLE 2 Tin-Nickel Coatings on Copper or Copper Alloys
3.1.2 significant surface—that portion of a coated article’s
surface where the coating is required to meet all the require- Service Minimum
Thickness
Condition Thickness,
ments of the coating specification for that article. Significant
Notation
Number µm
surfaces are those that are essential to the serviceability or
A B B
5 Cu/Sn-Ni as specified as specified
function of the article, or which can be a source of corrosion
(above 45) (above 45)
A
4 Cu/Sn-Ni 45 45
products or tarnish films that interfere with the function or
A
3 Cu/Sn-Ni 25 25
desirable appearance of the article. Significant surfaces are
A
2 Cu/Sn-Ni 15 15
A
those surfaces that are identified by the purchaser by, for
0 Cu/Sn-Ni 44
example, indicating them on an engineering drawing of the
A
An undercoating of copper 4.0 µm thick shall be applied on copper-zinc alloys to
product or marking a sample item of the product. serve as a zinc diffusion barrier.
B
Thickness of Sn-Ni shall be stated in a Thickness Notation. A statement of
3.1.3 undercoating—a metallic coating layer between the
Service Condition 5 is not sufficient.
basis metal or substrate and the topmost metallic coating. The
thickness of an undercoating is usually greater than 0.8 µm.
This is in contrast to strikes or flashes, whose thicknesses are TABLE 3 Tin-Nickel Coatings on Zinc Alloys
generally lower.
Service Minimum
Thickness
Condition Thickness,
Notation
Number µm
4. Classifications
A
4 Zn/Cu /Sn-Ni 45 45
4.1 Coating Grades—Six grades of coatings, designated by
A
3 Zn/Cu /Sn-Ni 25 25
A
service condition numbers, are covered by this specification.
2 Zn/Cu /Sn-Ni 15 15
A
1 Zn/Cu /Sn-Ni 8 8
For each coating grade a coating thickness grade is specified
A
An undercoating of copper 4.0 µm thick shall be applied to prevent zinc from
(see Tables 1-3).
contaminating the Sn-Ni plating bath and to serve as a diffusion barrier.
4.2 Service Condition Number—Theserviceconditionnum-
ber indicates the severity of exposure for which the grade of
coating is intended.
5.1.2 Location of significant surface(s) (see section 3.1.2),
SC5—extended severe service
5.1.3 The service number or coating thickness notation (see
SC4—very severe service
SC3—severe service 4.2 and 4.3),
SC2—moderate service
5.1.4 Undercoating, if required (see 6.2 and Tables 1-3),
SC1—mild service
5.1.5 Any requirement for submission of sample coated
SC0—mild service (copper and copper alloys only)
articles (see 7.2.1),
NOTE 1—Typical service conditions for which the service condition
5.1.6 Whether or not location of rack marks is to be defined
numbers are appropriate are given in Appendix X1.
(see 7.2.1),
4.3 Coating Thickness Notation—The coating thickness is
5.1.7 Any requirement for porosity testing and the criteria
specified for each service condition in the following manner:
for acceptance (see 7.5.2),
Basis metal/Undercoating (thickness)/Sn-Ni (thickness). For
5.1.8 Heat treatment for stress relief, whether it has been
example, Fe/Cu4/Sn-Ni25 would indicate a 25 µm tin-nickel
performed by the purchaser, or is required (see 7.6),
coating over an iron or steel article with a 4-µm thick copper
5.1.9 Heat treatment after electroplating, if required (see
undercoating. All thickness notations are minimum thick-
7.7),
nesses.
5.1.10 Any packaging requirement (see section 7.8),
5.1.11 Inspection procedure to be used (see Section 9),
5. Ordering Information
5.1.12 Any requirement for certification (see Section 11),
5.1 To make the application of this standard complete, the
and
purchaser needs to supply the following information to the
5.1.13 Any requirement for test specimens (see 8.1.1).
seller in the purchase order or other government documents.
5.1.1 The name, designation, and date of issue of this
6. Material and Process
standard,
6.1 Composition of Coating—Electrolytes that have been
investigated for producing Sn-Ni alloy deposits include
TABLE 1 Tin-Nickel Coatings on Steel
cyanide, fluoborate, pyrophosphate, and acetate, but the only
Service Minimum
one in general commercial use is the fluoride-chloride formu-
Thickness
Condition Thickness,
Notation
lation. Thedepositcontains35 65%nickelwiththeremain-
Number µm
A B B der tin (see Note 2).
5 Fe/Cu /Sn-Ni as specified as specified
(above 45) (above 45)
NOTE 2—The electrodeposited tin-nickel coating is a single-phase,
A
4 Fe/Cu /Sn-Ni 45 45
A metastable compound, corresponding approximately to the formula SnNi.
3 Fe/Cu /Sn-Ni 25 25
It is stable at ordinary temperatures but starts to recrystallize at elevated
2 Fe/Sn-Ni 15 15
temperatures. The safe working temperature of the coating is 300°C,
1 Fe/Sn-Ni 8 8
although actual melting does not commence below 800°C. The coating is
A
Copper undercoat shall be at least 4.0 µm.
B
Thickness of Sn-Ni shall be stated in a Thickness Notation. A statement of
Service Condition 5 is not sufficient.
Lowenheim, F. A., Electroplating, McGraw-Hill Inc., 1978.
B605−95a (2015)
hard (700HV100). Like many such compounds, it is inherently somewhat
7.3.1 The thickness of the coating everywhere on the
brittle, but if it is free of internal stresses, the brittleness is not sufficient
significantsurfacesshallconformtotherequirementsinTables
to impair its serviceability or to cause the coating to flake under impact.
1-3 as to minimum thickness.
Because of the brittleness of the tin-nickel, however, it is not possible to
fabricate parts by bending coated sheet material, because the compressive
NOTE 6—The thickness of electrodeposited coatings varies from point
stresses in the coating on the inside of the bend usually cause some of the
to point on the surface of the product. (See Practice B507.)The thickness
coating to flake off. To provide serviceability, the coating must be
is less in interior corners and holes. Such surfaces are often exempt from
depositedinastress-freecondition.Inaddition,itisgenerallyinadvisable
thickness requirements. If the full thickness is required in those locations,
to specify tin-nickel finish for parts subject to deformation in service.
the electroplater will have to use special techniques that will probably
raise the cost of the process.
6.2 Basis Metal—Tin-nickel can be deposited directly on
NOTE 7—The coating thickness requirement of this specification is a
steel, copper, and copper-base alloys. However, an undercoat-
minimum. Variation in the thickness from point to point on an article and
ing of copper can improve performance in some systems and
from article to article in a production lot is inherent in electroplating.
shall be used under the following conditions: Therefore, if all of the articles in a production are to meet the thickness
requirement, the average coating thickness for the production lot as a
6.2.1 On steel, a copper undercoating with a minimum
whole will be greater than the specified minimum.
thickness of 4 µm, shall be used for Service Conditions 3, 4,
7.4 Adhesion—The coatings shall be adherent to the basis
and 5.
metal when subject to either test, in accordance with 8.5.2 and
6.2.2 On copper-zinc alloys, a copper undercoating with a
8.5.3. There shall be no separation of the coating from the
minimum thickness of 4 µm shall be used for all service
substrate.
conditions to prevent diffusion of the zinc.
6.2.3 Zinc-base alloys shall have an undercoating of a 7.5 Integrity of the Coating:
minimum of 4 µm of copper to prevent diffusion of the zinc 7.5.1 Gross Defects/Mechanical Damage—The coatings
intothedepositandtopreventcontaminationoftheelectrolyte shall be free of mechanical damage, large pores, and similar
with zinc. gross defects. For some applications this requirement may be
relaxed to allow for a small number of such defects (per unit
NOTE 3—Tin-nickel-coated zinc-alloy diecastings shall never be re-
area), especially if they are outside the significant surfaces.
turned for remelting to prevent contamination of the zinc alloy with tin.
7.5.2 Porosity—Almostallas-platedelectrodepositscontain
some porosity. The amount of porosity that may be tolerable
7. Coating Requirements
depends on the severity of the environment that the article is
7.1 Composition of Coating—The deposit shall contain
likely to encounter during service or storage. If the pores are
65 65% tin, the balance nickel.
few in number or away from significant surfaces, their pres-
ence can often be tolerated. Such acceptance (or pass-fail)
7.2 Appearance:
criteria shall be part of the product specification for the
7.2.1 The coating on all readily visible surfaces shall be
particular article or coating requiring the porosity test (see 8.6
smooth, fine grained, continuous, adherent, free of visible
for porosity test methods).
blisters, pits, nodules, indications of burning, excessive
buildup, staining, and other defects. All tin-nickel coated
7.6 Pre-Treatments of Iron and Steel for Reducing the Risk
articles shall be clean and undamaged. When necessary,
of Hydrogen Embrittlement—Parts that are made of steels with
preliminary samples showing the finish shall be supplied for
ultimate tensile strengths of 1000 MPa (hardness of 31 HRC)
approval. Where a rack contact mark is unavoidable, its
or greater that have been machined, ground, cold formed, or
location shall be indicated on the article or its drawing.
cold straightened subsequent to heat treatment shall be heat
7.2.2 Defects and variations in appearance in the coating treated prior to processing according to Specification B849.
that arise from surface conditions of the substrate (scratches, The tensile strength shall be supplied by the purchaser.
pores, roll marks, inclusions, and the like) and that persist in
7.7 Post-Coating Treatments of Iron and Steel for Reducing
the coating despite the observance of good metal finishing
the Risk of Hydrogen Embrittlement—Partsthataremadefrom
practices shall not be cause for rejection.
steels with ultimate tensile strengths equal to or greater than
1000 MPa (hardness of 31 HRC) and surface hardened parts
NOTE 4—Coatings generally perform better in service when the
substrate over which they are applied is smooth and free of torn metal, shall require heat treatment according to Specification B
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B605 − 95a (Reapproved 2009) B605 − 95a (Reapproved 2015)
Standard Specification for
Electrodeposited Coatings of Tin-Nickel Alloy
This standard is issued under the fixed designation B605; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 This specification covers the requirements for electrodeposited tin-nickel alloy coatings from aqueous solutions intended for
the corrosion protection of fabricated articles of iron, steel, zinc-base alloys, copper, and copper alloys. The composition of the
alloy remains constant at 65/35 tin-nickel in spite of wide fluctuations in both composition and operating conditions. The
composition corresponds quite closely to an equiatomic ratio, and the process favors the co-deposition of tin and nickel atoms at
identical rates.
1.2 This specification does not apply to sheet, strip, or wire in the fabricated form. It also may not be applicable to threaded
articles having basic major diameters up to and including 19 mm because of the nonuniformity of thickness that can be expected
on fine threads. However, a decision to use the coating on such components may be made by the purchaser.
1.3 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use.
2. Referenced Documents
2.1 ASTM Standards:
B183 Practice for Preparation of Low-Carbon Steel for Electroplating
B242 Guide for Preparation of High-Carbon Steel for Electroplating
B246 Specification for Tinned Hard-Drawn and Medium-Hard-Drawn Copper Wire for Electrical Purposes
B252 Guide for Preparation of Zinc Alloy Die Castings for Electroplating and Conversion Coatings
B281 Practice for Preparation of Copper and Copper-Base Alloys for Electroplating and Conversion Coatings
B322 Guide for Cleaning Metals Prior to Electroplating
B374 Terminology Relating to Electroplating
B487 Test Method for Measurement of Metal and Oxide Coating Thickness by Microscopical Examination of Cross Section
B499 Test Method for Measurement of Coating Thicknesses by the Magnetic Method: Nonmagnetic Coatings on Magnetic Basis
Metals
B504 Test Method for Measurement of Thickness of Metallic Coatings by the Coulometric Method
B507 Practice for Design of Articles to Be Electroplated on Racks
B567 Test Method for Measurement of Coating Thickness by the Beta Backscatter Method
B568 Test Method for Measurement of Coating Thickness by X-Ray Spectrometry
B571 Practice for Qualitative Adhesion Testing of Metallic Coatings
B602 Test Method for Attribute Sampling of Metallic and Inorganic Coatings
B634 Specification for Electrodeposited Coatings of Rhodium for Engineering Use
B697 Guide for Selection of Sampling Plans for Inspection of Electrodeposited Metallic and Inorganic Coatings
B762 Test Method of Variables Sampling of Metallic and Inorganic Coatings
B765 Guide for Selection of Porosity and Gross Defect Tests for Electrodeposits and Related Metallic Coatings
B809 Test Method for Porosity in Metallic Coatings by Humid Sulfur Vapor (“Flowers-of-Sulfur”)
This specification is under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee B08.06 on Soft
Metals.
Current edition approved Sept. 1, 2009March 1, 2015. Published November 2009April 2015. Originally approved in 1975. Last previous edition approved in 20042009
as B605 – 95a (2004).(2009). DOI: 10.1520/B0605-95AR09.10.1520/B0605-95AR15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B605 − 95a (2015)
B849 Specification for Pre-Treatments of Iron or Steel for Reducing Risk of Hydrogen Embrittlement
B850 Guide for Post-Coating Treatments of Steel for Reducing the Risk of Hydrogen Embrittlement
D3951 Practice for Commercial Packaging
3. Terminology
3.1 Definitions:
3.1.1 Many terms used in this standard are defined in Terminology B374.
3.1.2 significant surface—that portion of a coated article’s surface where the coating is required to meet all the requirements
of the coating specification for that article. Significant surfaces are those that are essential to the serviceability or function of the
article, or which can be a source of corrosion products or tarnish films that interfere with the function or desirable appearance of
the article. Significant surfaces are those surfaces that are identified by the purchaser by, for example, indicating them on an
engineering drawing of the product or marking a sample item of the product.
3.1.3 undercoating—a metallic coating layer between the basis metal or substrate and the topmost metallic coating. The
thickness of an undercoating is usually greater than 0.8 μm. This is in contrast to strikes or flashes, whose thicknesses are generally
lower.
4. Classifications
4.1 Coating Grades—Six grades of coatings, designated by service condition numbers, are covered by this specification. For
each coating grade a coating thickness grade is specified (see Tables 1-3).
4.2 Service Condition Number—The service condition number indicates the severity of exposure for which the grade of coating
is intended.
SC5—extended severe service
SC4—very severe service
SC3—severe service
SC2—moderate service
SC1—mild service
SC0—mild service (copper and copper alloys only)
NOTE 1—Typical service conditions for which the service condition numbers are appropriate are given in Appendix X1.
4.3 Coating Thickness Notation—The coating thickness is specified for each service condition in the following manner: Basis
metal/Undercoating (thickness)/Sn-Ni (thickness). For example, Fe/Cu4/Sn-Ni25 would indicate a 25 μm tin-nickel coating over
an iron or steel article with a 4-μm thick copper undercoating. All thickness notations are minimum thicknesses.
5. Ordering Information
5.1 To make the application of this standard complete, the purchaser needs to supply the following information to the seller in
the purchase order or other government documents.
5.1.1 The name, designation, and date of issue of this standard,
5.1.2 Location of significant surface(s) (see section 3.1.2),
5.1.3 The service number or coating thickness notation (see 4.2 and 4.3),
5.1.4 Undercoating, if required (see 6.2 and Tables 1-3),
5.1.5 Any requirement for submission of sample coated articles (see 7.2.1),
5.1.6 Whether or not location of rack marks is to be defined (see 7.2.1),
5.1.7 Any requirement for porosity testing and the criteria for acceptance (see 7.5.2),
5.1.8 Heat treatment for stress relief, whether it has been performed by the purchaser, or is required (see 7.6),
5.1.9 Heat treatment after electroplating, if required (see 7.7),
5.1.10 Any packaging requirement (see section 7.8),
TABLE 1 Tin-Nickel Coatings on Steel
Service Minimum
Thickness
Condition Thickness,
Notation
Number μm
A B B
5 Fe/Cu /Sn-Ni as specified as specified
(above 45) (above 45)
A
4 Fe/Cu /Sn-Ni 45 45
A
3 Fe/Cu /Sn-Ni 25 25
2 Fe/Sn-Ni 15 15
1 Fe/Sn-Ni 8 8
A
Copper undercoat shall be at least 4.0 μm.
B
Thickness of Sn-Ni shall be stated in a Thickness Notation. A statement of
Service Condition 5 is not sufficient.
B605 − 95a (2015)
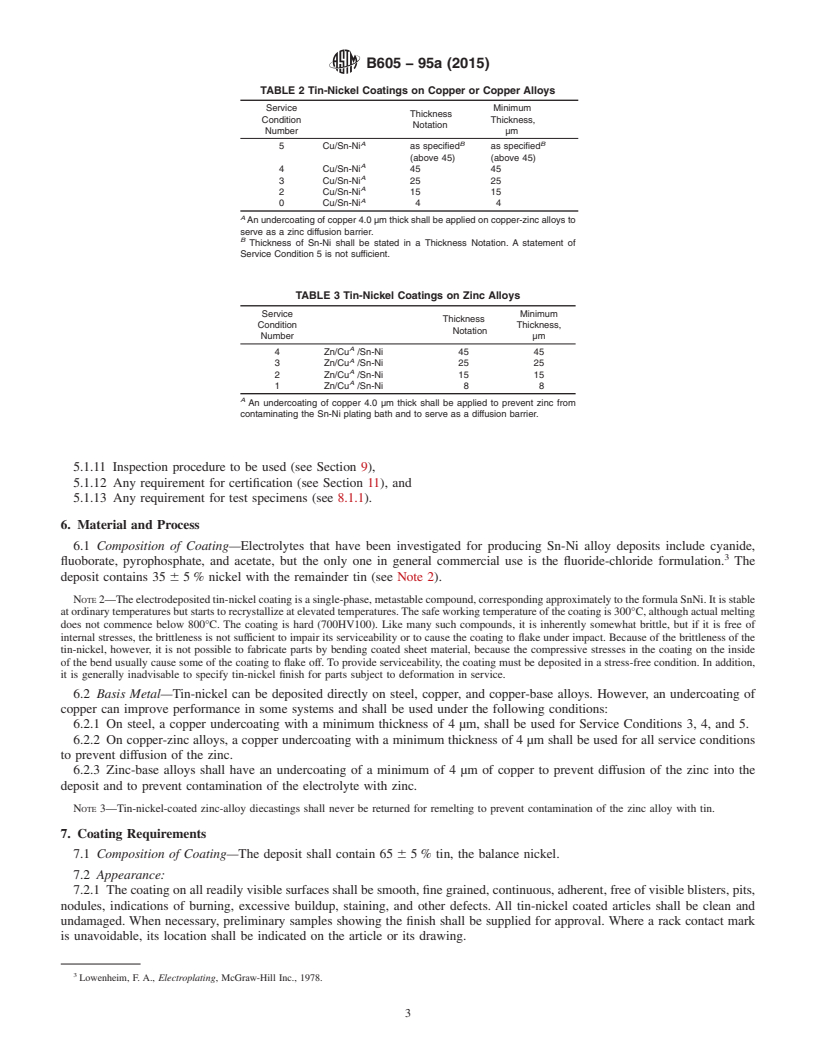
TABLE 2 Tin-Nickel Coatings on Copper or Copper Alloys
Service Minimum
Thickness
Condition Thickness,
Notation
Number μm
A B B
5 Cu/Sn-Ni as specified as specified
(above 45) (above 45)
A
4 Cu/Sn-Ni 45 45
A
3 Cu/Sn-Ni 25 25
A
2 Cu/Sn-Ni 15 15
A
0 Cu/Sn-Ni 4 4
A
An undercoating of copper 4.0 μm thick shall be applied on copper-zinc alloys to
serve as a zinc diffusion barrier.
B
Thickness of Sn-Ni shall be stated in a Thickness Notation. A statement of
Service Condition 5 is not sufficient.
TABLE 3 Tin-Nickel Coatings on Zinc Alloys
Service Minimum
Thickness
Condition Thickness,
Notation
Number μm
A
4 Zn/Cu /Sn-Ni 45 45
A
3 Zn/Cu /Sn-Ni 25 25
A
2 Zn/Cu /Sn-Ni 15 15
A
1 Zn/Cu /Sn-Ni 8 8
A
An undercoating of copper 4.0 μm thick shall be applied to prevent zinc from
contaminating the Sn-Ni plating bath and to serve as a diffusion barrier.
5.1.11 Inspection procedure to be used (see Section 9),
5.1.12 Any requirement for certification (see Section 11), and
5.1.13 Any requirement for test specimens (see 8.1.1).
6. Material and Process
6.1 Composition of Coating—Electrolytes that have been investigated for producing Sn-Ni alloy deposits include cyanide,
fluoborate, pyrophosphate, and acetate, but the only one in general commercial use is the fluoride-chloride formulation. The
deposit contains 35 6 5 % nickel with the remainder tin (see Note 2).
NOTE 2—The electrodeposited tin-nickel coating is a single-phase, metastable compound, corresponding approximately to the formula SnNi. It is stable
at ordinary temperatures but starts to recrystallize at elevated temperatures. The safe working temperature of the coating is 300°C, although actual melting
does not commence below 800°C. The coating is hard (700HV100). Like many such compounds, it is inherently somewhat brittle, but if it is free of
internal stresses, the brittleness is not sufficient to impair its serviceability or to cause the coating to flake under impact. Because of the brittleness of the
tin-nickel, however, it is not possible to fabricate parts by bending coated sheet material, because the compressive stresses in the coating on the inside
of the bend usually cause some of the coating to flake off. To provide serviceability, the coating must be deposited in a stress-free condition. In addition,
it is generally inadvisable to specify tin-nickel finish for parts subject to deformation in service.
6.2 Basis Metal—Tin-nickel can be deposited directly on steel, copper, and copper-base alloys. However, an undercoating of
copper can improve performance in some systems and shall be used under the following conditions:
6.2.1 On steel, a copper undercoating with a minimum thickness of 4 μm, shall be used for Service Conditions 3, 4, and 5.
6.2.2 On copper-zinc alloys, a copper undercoating with a minimum thickness of 4 μm shall be used for all service conditions
to prevent diffusion of the zinc.
6.2.3 Zinc-base alloys shall have an undercoating of a minimum of 4 μm of copper to prevent diffusion of the zinc into the
deposit and to prevent contamination of the electrolyte with zinc.
NOTE 3—Tin-nickel-coated zinc-alloy diecastings shall never be returned for remelting to prevent contamination of the zinc alloy with tin.
7. Coating Requirements
7.1 Composition of Coating—The deposit shall contain 65 6 5 % tin, the balance nickel.
7.2 Appearance:
7.2.1 The coating on all readily visible surfaces shall be smooth, fine grained, continuous, adherent, free of visible blisters, pits,
nodules, indications of burning, excessive buildup, staining, and other defects. All tin-nickel coated articles shall be clean and
undamaged. When necessary, preliminary samples showing the finish shall be supplied for approval. Where a rack contact mark
is unavoidable, its location shall be indicated on the article or its drawing.
Lowenheim, F. A., Electroplating, McGraw-Hill Inc., 1978.
B605 − 95a (2015)
7.2.2 Defects and variations in appearance in the coating that arise from surface conditions of the substrate (scratches, pores,
roll marks, inclusions, and the like) and that persist in the coating despite the observance of good metal finishing practices shall
not be cause for rejection.
NOTE 4—Coatings generally perform better in service when the substrate over which they are applied is smooth and free of torn metal, inclusions, pores,
and other defects. The specifications covering the unfinished product should provide limits for these defects. A metal finisher can often remove defects
through special treatments, such as grinding, polishing, abrasive blasting, chemical etches, and electropolishing. However, these are not normal in the
treatment steps preceding the application of the coating. When they are desired, they are the subject of special agreement between the purchaser and the
seller.
NOTE 5—Proper preparatory procedures and thorough cleaning are essential to ensure satisfactory adhesion and corrosion resistance performance of
the coating. Materials used for cleaning should not damage the basis metal, for example, by causing defects such as pits, intergranular attack, stress
corrosion cracking, and unwarranted hydrogen embrittlement. It is recommended that the following Practices, where appropriate for cleaning, be used:
B183, B242, B252, B281, and B322.
7.3 Thickness:
7.3.1 The thickness of the coating everywhere on the significant surfaces shall conform to the requirements in Tables 1-3 as to
minimum thickness.
NOTE 6—The thickness of electrodeposited coatings varies from point to point on the surface of the product. (See Practice B507.) The thickness is less
in interior corners and holes. Such surfaces are often exempt from thickness requirements. If the full thickness is required in those locations, the
electroplater will have to use special techniques that will probably raise the cost of the process.
NOTE 7—The coating thickness requirement of this specification is a minimum. Variation in the thickness from point to point on an article and from
article to article in a production lot is inherent in electroplating. Therefore, if all of the articles in a production are to meet the thickness requirement,
the average coating thickness for the production lot as a whole will be greater than the specified minimum.
7.4 Adhesion—The coatings shall be adherent to the basis metal when subject to either test, in accordance with 8.5.2 and 8.5.3.
There shall be no separation of the coating from the substrate.
7.5 Integrity of the Coating:
7.5.1 Gross Def
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.