


ASTM B635-00(2015)
(Specification)Standard Specification for Coatings of Cadmium-Tin Mechanically Deposited
Standard Specification for Coatings of Cadmium-Tin Mechanically Deposited
ABSTRACT
This specification covers the requirements for a coating that is a mixture of cadmium and tin mechanically deposited on metal products. The coating shall be 45 to 75 mass % cadmium, the remainder tin. All steel parts that have ultimate tensile strength of 1000 MPa and above and that contain tensile stresses caused by machining, grinding, straightening, or cold forming operation shall be given a stress relief heat treatment prior to cleaning and metal deposition. High-strength steels that have heavy oxide or scale shall be cleaned before application of the coating in accordance with guide B 242. Chromate treatment for Type II shall be done in a solution containing hexavalent chromium. The cadmium-tin coating shall be sufficiently adherent to the basis metal to pass the prescribed testing. Steel springs and other high-strength steel parts shall be free from hydrogen embrittlement. The coating shall be uniform in appearance and substantially free of blisters, pits, nodules, flaking and other defects that can adversely affect the function of the coating. Chemical composition of the cadmium-tin coating shall be determined when required on the purchase order by procedures given in methods E 87 or test methods E 396. The thickness of the coating shall be determined by the microscopical method, the magnetic method, or the beta backscatter method as applicable. Chromate conversion coatings of cadmium-tin both have an essentially silvery-white appearance. Adhesion of the cadmium-tin deposit to the basis metal shall be tested in a manner that is consistent with the service requirements of the coated article. Coated parts to be tested for the absence of embrittlement from cleaning shall be tested for brittle failure in accordance with a suitable method.
SCOPE
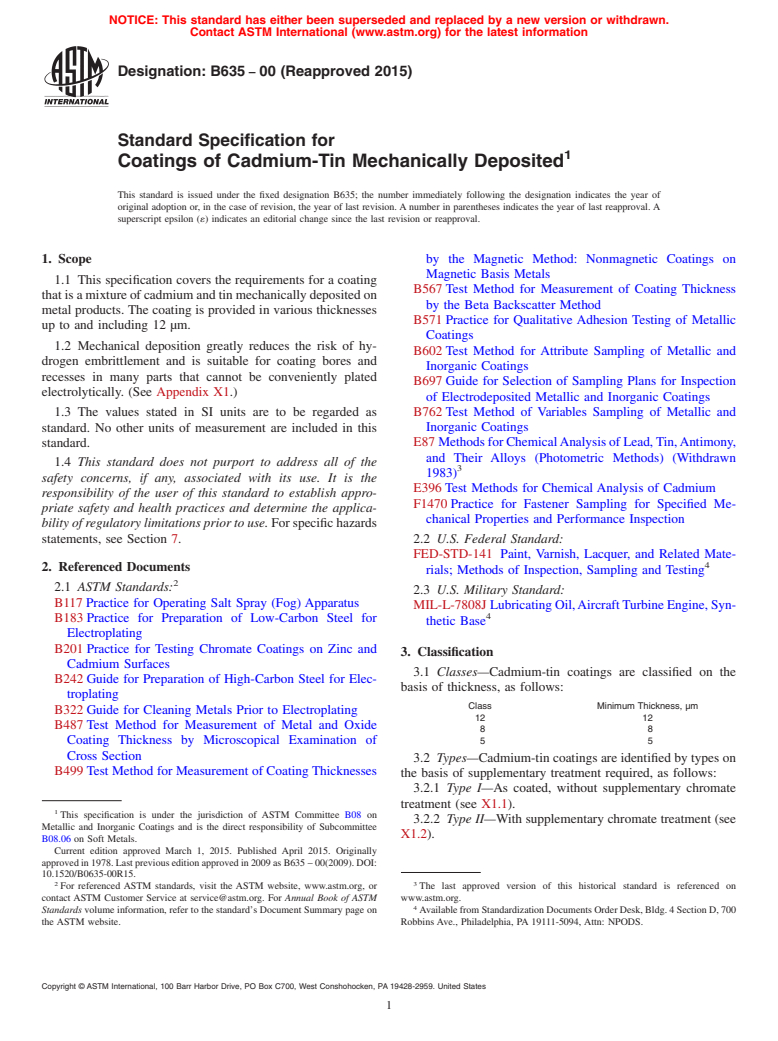
1.1 This specification covers the requirements for a coating that is a mixture of cadmium and tin mechanically deposited on metal products. The coating is provided in various thicknesses up to and including 12 μm.
1.2 Mechanical deposition greatly reduces the risk of hydrogen embrittlement and is suitable for coating bores and recesses in many parts that cannot be conveniently plated electrolytically. (See Appendix X1.)
1.3 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use. For specific hazards statements, see Section 7.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: B635 − 00 (Reapproved 2015)
Standard Specification for
Coatings of Cadmium-Tin Mechanically Deposited
This standard is issued under the fixed designation B635; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope by the Magnetic Method: Nonmagnetic Coatings on
Magnetic Basis Metals
1.1 This specification covers the requirements for a coating
B567 Test Method for Measurement of Coating Thickness
that is a mixture of cadmium and tin mechanically deposited on
by the Beta Backscatter Method
metal products. The coating is provided in various thicknesses
B571 Practice for Qualitative Adhesion Testing of Metallic
up to and including 12 µm.
Coatings
1.2 Mechanical deposition greatly reduces the risk of hy-
B602 Test Method for Attribute Sampling of Metallic and
drogen embrittlement and is suitable for coating bores and
Inorganic Coatings
recesses in many parts that cannot be conveniently plated
B697 Guide for Selection of Sampling Plans for Inspection
electrolytically. (See Appendix X1.)
of Electrodeposited Metallic and Inorganic Coatings
B762 Test Method of Variables Sampling of Metallic and
1.3 The values stated in SI units are to be regarded as
standard. No other units of measurement are included in this Inorganic Coatings
E87 Methods for Chemical Analysis of Lead, Tin, Antimony,
standard.
and Their Alloys (Photometric Methods) (Withdrawn
1.4 This standard does not purport to address all of the
1983)
safety concerns, if any, associated with its use. It is the
E396 Test Methods for Chemical Analysis of Cadmium
responsibility of the user of this standard to establish appro-
F1470 Practice for Fastener Sampling for Specified Me-
priate safety and health practices and determine the applica-
chanical Properties and Performance Inspection
bility of regulatory limitations prior to use. For specific hazards
statements, see Section 7. 2.2 U.S. Federal Standard:
FED-STD-141 Paint, Varnish, Lacquer, and Related Mate-
2. Referenced Documents
rials; Methods of Inspection, Sampling and Testing
2.1 ASTM Standards:
2.3 U.S. Military Standard:
B117 Practice for Operating Salt Spray (Fog) Apparatus
MIL-L-7808J Lubricating Oil, Aircraft Turbine Engine, Syn-
B183 Practice for Preparation of Low-Carbon Steel for
thetic Base
Electroplating
B201 Practice for Testing Chromate Coatings on Zinc and
3. Classification
Cadmium Surfaces
3.1 Classes—Cadmium-tin coatings are classified on the
B242 Guide for Preparation of High-Carbon Steel for Elec-
basis of thickness, as follows:
troplating
Class Minimum Thickness, µm
B322 Guide for Cleaning Metals Prior to Electroplating
12 12
B487 Test Method for Measurement of Metal and Oxide
8 8
5 5
Coating Thickness by Microscopical Examination of
Cross Section
3.2 Types—Cadmium-tin coatings are identified by types on
B499 Test Method for Measurement of Coating Thicknesses
the basis of supplementary treatment required, as follows:
3.2.1 Type I—As coated, without supplementary chromate
treatment (see X1.1).
This specification is under the jurisdiction of ASTM Committee B08 on
3.2.2 Type II—With supplementary chromate treatment (see
Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee
X1.2).
B08.06 on Soft Metals.
Current edition approved March 1, 2015. Published April 2015. Originally
approved in 1978. Last previous edition approved in 2009 as B635 – 00(2009). DOI:
10.1520/B0635-00R15.
2 3
For referenced ASTM standards, visit the ASTM website, www.astm.org, or The last approved version of this historical standard is referenced on
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM www.astm.org.
Standards volume information, refer to the standard’s Document Summary page on Available from Standardization Documents Order Desk, Bldg. 4 Section D, 700
the ASTM website. Robbins Ave., Philadelphia, PA 19111-5094, Attn: NPODS.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B635 − 00 (2015)
4. Ordering Information used to ensure conformance to the salt spray corrosion resistant
requirements or to enhance the test results of the lead acetate
4.1 To make the application of this specification complete,
spot test (8.5.2).
the purchaser needs to supply the following information to the
supplier in the purchase order or other governing document:
5.3 Thickness:
4.1.1 Class, including a maximum thickness, if appropriate,
5.3.1 The thickness of the coating everywhere on the
type, and need for supplemental lubricant (3.1, 3.2, and
significant surfaces shall be at least that of the specified class
5.2.4.2).
as defined in 3.1.
4.1.2 Nature of substrate, for example, high-strength steel,
5.3.2 Significant surfaces are defined as those normally
need for stress-relief, and cleaning precautions to be followed
visible (directly or by reflection) that are essential to the
(5.2.2).
appearance or serviceability of the article when assembled in
4.1.3 Significant surfaces (5.3).
normal position; or which can be the source of corrosion
4.1.4 Requirements and methods of testing for one or more
products that deface visible surfaces on the assembled article.
of the following requirements: need for and type of test
When necessary, the significant surfaces shall be indicated on
specimens (8.1), composition (8.2), thickness (8.4), adhesion
the drawing of the article, or by the provision of suitably
(8.6), and absence of hydrogen embrittlement and the waiting
marked samples.
period prior to testing and testing loads (8.8) and lubricating
resistance (S2).
NOTE 1—The thickness of mechanically-deposited coatings varies from
point-to-point on the surface of a product, characteristically tending to be
4.1.5 Sampling plan for each inspection criterion and re-
thicker on flat surfaces and thinner at exposed edges, sharp projections,
sponsibility for inspection, if necessary (Section 6 and Supple-
shielded or recessed areas, interior corners and holes, with such thinner
mentary Requirement S1).
areas often being exempted from thickness requirement.
4.1.6 Requirements for certified report of test results (Sec-
5.3.3 When significant surfaces are involved on which the
tion 10).
specified thickness of deposit cannot readily be controlled, the
5. Requirements purchaser and manufacturer should recognize the necessity for
either thicker or thinner deposits. For example, to reduce
5.1 Nature of Finish—The coating shall be 45 to 75 mass %
buildup in thread roots, holes, deep recesses, bases of angles,
cadmium, the remainder tin.
and similar areas, the deposit thickness on the more accessible
5.2 Process:
surfaces will have to be reduced proportionately.
5.2.1 Stress Relief Treatment—All steel parts that have
NOTE 2—The coating thickness requirement of this specification is a
ultimate tensile strength of 1000 MPa and above and that
minimum requirement; that is, the coating thickness is required to equal or
contain tensile stresses caused by machining, grinding,
exceed the specified thickness everywhere on the significant surfaces.
straightening, or cold forming operation shall be given a stress
Variation in the coating thickness from point to point on a coated article
relief heat treatment prior to cleaning and metal deposition.
is an inherent characteristic of mechanical deposition processes.
Therefore, the coating thickness will have to exceed the specified value at
The temperature and time at temperature shall be 190 6 15°C
some points on the significant surfaces to ensure that the thickness equals
for a minimum of 3 h so that maximum stress relief is obtained
or exceeds the specified value at all points. Thus, in most cases, the
without reducing the hardness below the specified minimum.
average coating thickness on an article will be greater than the specified
5.2.2 High-strength steels that have heavy oxide or scale
value; how much greater is largely determined by the shape of the article
shall be cleaned before application of the coating in accordance
and the characteristics of the deposition process. In addition, the average
coating thickness on articles will vary from article to article within a
with Guide B242. In general, non-electrolytic alkaline, anodic-
production lot. Therefore, if all of the articles in a production lot are to
alkaline, and some inhibited acid cleaners are preferred to
meet the thickness requirement, the average coating thickness for the
avoid the risk of producing hydrogen embrittlement from the
production lot as a whole will be greater than the average necessary to
cleaning procedure.
ensure that a single article meets the requirement.
5.2.3 For preparation of low-carbon steels, see Practice
5.4 Adhesion—The cadmium-tin coating shall be suffi-
B183. For cleaning, useful guidelines are also given in Guide
ciently adherent to the basis metal to pass the tests specified in
B322.
8.6.
5.2.4 Supplementary Treatments:
5.2.4.1 Chromate treatment for Type II shall be done in a
5.5 Corrosion Resistance:
solution containing hexavalent chromium. This solution shall
5.5.1 The presence of corrosion products visible to the
produce a bright or semi-bright continuous, smooth, protective
unaided eye at normal reading distance at the end of the
film. This film may have a slight yellowish or iridescent color.
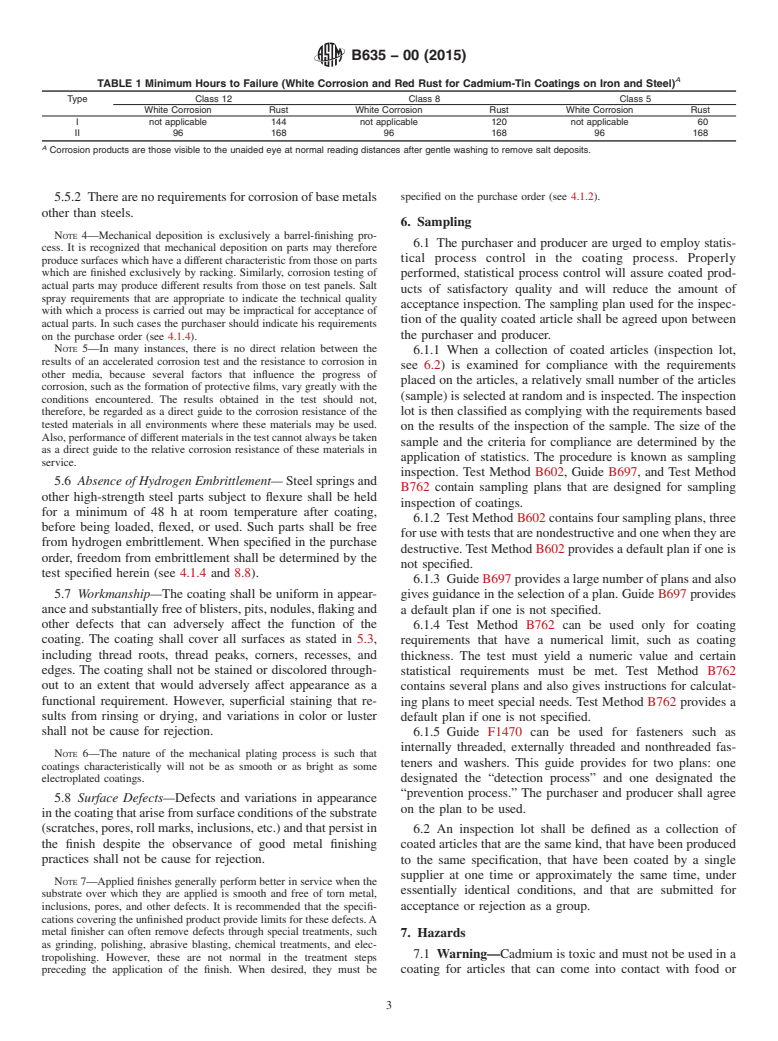
specified test period as stated in Table 1 shall constitute failure,
The absence of color shall not be considered evidence of the
except that corrosion products at the edges of specimens shall
absence of a Type II film or as a basis for rejection of the parts.
not constitute failure. Slight “wisps” of white corrosion, as
Only post treatments that contain salts that yield films contain-
opposed to obvious accumulations, shall be acceptable.
ing hexavalent chromium are permitted as treatments for
NOTE 3—The hours given in Table 1 are the minimums required to
producing Type II coatings.
guarantee satisfactory performance. Longer periods before the appearance
5.2.4.2 Waxes, lacquers, or other organic coatings may be
of white corrosion products and rust are possible, but salt spray resistance
used to improve lubricity, and the need for them should be
does not vary in exact proportion with increased plating thickness. The
supplied in the purchase order or other governing document
hours given for Type II reflect the added protection of chromate treatments
(4.1.1). Such supplemental lubrication treatments shall not be without requiring impractical testing periods.
B635 − 00 (2015)
A
TABLE 1 Minimum Hours to Failure (White Corrosion and Red Rust for Cadmium-Tin Coatings on Iron and Steel)
Type Class 12 Class 8 Class 5
White Corrosion Rust White Corrosion Rust White Corrosion Rust
I not applicable 144 not applicable 120 not applicable 60
II 96 168 96 168 96 168
A
Corrosion products are those visible to the unaided eye at normal reading distances after gentle washing to remove salt deposits.
specified on the purchase order (see 4.1.2).
5.5.2 There are no requirements for corrosion of base metals
other than steels.
6. Sampling
NOTE 4—Mechanical deposition is exclusively a barrel-finishing pro-
6.1 The purchaser and producer are urged to employ statis-
cess. It is recognized that mechanical deposition on parts may therefore
tical process control in the coating process. Properly
produce surfaces which have a different characteristic from those on parts
which are finished exclusively by racking. Similarly, corrosion testing of performed, statistical process control will assure coated prod-
actual parts may produce different results from those on test panels. Salt
ucts of satisfactory quality and will reduce the amount of
spray requirements that are appropriate to indicate the technical quality
acceptance inspection. The sampling plan used for the inspec-
with which a process is carried out may be impractical for acceptance of
tion of the quality coated article shall be agreed upon between
actual parts. In such cases the purchaser should indicate his requirements
the purchaser and producer.
on the purchase order (see 4.1.4).
NOTE 5—In many instances, there is no direct relation between the
6.1.1 When a collection of coated articles (inspection lot,
results of an accelerated corrosion test and the resistance to corrosion in
see 6.2) is examined for compliance with the requirements
other media, because several factors that influence the progress of
placed on the articles, a relatively small number of the articles
corrosion, such as the formation of protective films, vary greatly with the
(sample) is selected at random and is inspected. The inspection
conditions encountered. The results obtained in the test should not,
therefore, be regarded as a direct guide to the corrosion resistance of the lot is then classified as complying with the requirements based
tested materials in all environments where these materials may be used.
on the results of the inspection of the sample. The size of the
Also, performance of different materials in the test cannot always be taken
sample and the criteria for compliance are determined by the
as a direct guide to the relative corrosion resistance of these materials in
application of statistics. The procedure is known as sampling
service.
inspection. Test Method B602, Guide B697, and Test Method
5.6 Absence of Hydrogen Embrittlement— Steel springs and
B762 contain sampling plans that are designed for sampling
other high-strength steel parts subject to flexure shall be held
inspection of coatings.
for a minimum of 48 h at room temperature after coating,
6.1.2 Test Method B602 contains four sampling plans, three
before being loaded, flexed, or used. Such parts shall be free
for use with tests that are nondestructive and one when they are
from hydrogen embrittlement. When specified in the purchase
destructive. Test Method B602 provides a default plan if one is
order, freedom from embrittlement shall be determined by the
not specified.
test specified herein (see 4.1.4 and 8.8).
6.1.3 Guide B697 provides a large number of plans and also
5.7 Workmanship—The coating shall be uniform in appear- gives guidance in the selection of a plan. Guide B697 provides
ance and substantially free of blisters, pits, nodules, flaking and
a default plan if one is not specified.
other defects that can adversely affect the function of the 6.1.4 Test Method B762 can be used only for coating
coating. The coating shall cover all surfaces as stated in 5.3,
requirements that have a numeri
...
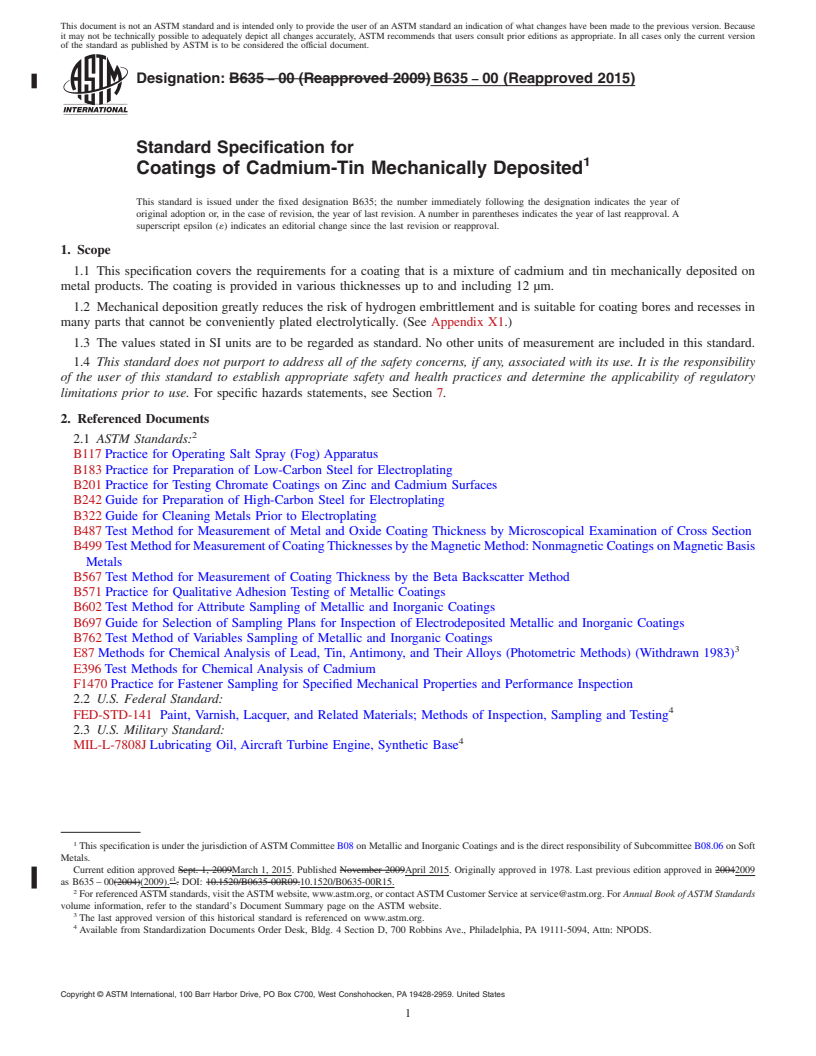
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B635 − 00 (Reapproved 2009) B635 − 00 (Reapproved 2015)
Standard Specification for
Coatings of Cadmium-Tin Mechanically Deposited
This standard is issued under the fixed designation B635; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 This specification covers the requirements for a coating that is a mixture of cadmium and tin mechanically deposited on
metal products. The coating is provided in various thicknesses up to and including 12 μm.
1.2 Mechanical deposition greatly reduces the risk of hydrogen embrittlement and is suitable for coating bores and recesses in
many parts that cannot be conveniently plated electrolytically. (See Appendix X1.)
1.3 The values stated in SI units are to be regarded as standard. No other units of measurement are included in this standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use. For specific hazards statements, see Section 7.
2. Referenced Documents
2.1 ASTM Standards:
B117 Practice for Operating Salt Spray (Fog) Apparatus
B183 Practice for Preparation of Low-Carbon Steel for Electroplating
B201 Practice for Testing Chromate Coatings on Zinc and Cadmium Surfaces
B242 Guide for Preparation of High-Carbon Steel for Electroplating
B322 Guide for Cleaning Metals Prior to Electroplating
B487 Test Method for Measurement of Metal and Oxide Coating Thickness by Microscopical Examination of Cross Section
B499 Test Method for Measurement of Coating Thicknesses by the Magnetic Method: Nonmagnetic Coatings on Magnetic Basis
Metals
B567 Test Method for Measurement of Coating Thickness by the Beta Backscatter Method
B571 Practice for Qualitative Adhesion Testing of Metallic Coatings
B602 Test Method for Attribute Sampling of Metallic and Inorganic Coatings
B697 Guide for Selection of Sampling Plans for Inspection of Electrodeposited Metallic and Inorganic Coatings
B762 Test Method of Variables Sampling of Metallic and Inorganic Coatings
E87 Methods for Chemical Analysis of Lead, Tin, Antimony, and Their Alloys (Photometric Methods) (Withdrawn 1983)
E396 Test Methods for Chemical Analysis of Cadmium
F1470 Practice for Fastener Sampling for Specified Mechanical Properties and Performance Inspection
2.2 U.S. Federal Standard:
FED-STD-141 Paint, Varnish, Lacquer, and Related Materials; Methods of Inspection, Sampling and Testing
2.3 U.S. Military Standard:
MIL-L-7808J Lubricating Oil, Aircraft Turbine Engine, Synthetic Base
This specification is under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee B08.06 on Soft
Metals.
Current edition approved Sept. 1, 2009March 1, 2015. Published November 2009April 2015. Originally approved in 1978. Last previous edition approved in 20042009
ε1
as B635 – 00(2004)(2009). . DOI: 10.1520/B0635-00R09.10.1520/B0635-00R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
The last approved version of this historical standard is referenced on www.astm.org.
Available from Standardization Documents Order Desk, Bldg. 4 Section D, 700 Robbins Ave., Philadelphia, PA 19111-5094, Attn: NPODS.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B635 − 00 (2015)
3. Classification
3.1 Classes—Cadmium-tin coatings are classified on the basis of thickness, as follows:
Class Minimum Thickness, μm
12 12
8 8
5 5
3.2 Types—Cadmium-tin coatings are identified by types on the basis of supplementary treatment required, as follows:
3.2.1 Type I—As coated, without supplementary chromate treatment (see X1.1).
3.2.2 Type II—With supplementary chromate treatment (see X1.2).
4. Ordering Information
4.1 To make the application of this specification complete, the purchaser needs to supply the following information to the
supplier in the purchase order or other governing document:
4.1.1 Class, including a maximum thickness, if appropriate, type, and need for supplemental lubricant (3.1, 3.2, and 5.2.4.2).
4.1.2 Nature of substrate, for example, high-strength steel, need for stress-relief, and cleaning precautions to be followed (5.2.2).
4.1.3 Significant surfaces (5.3).
4.1.4 Requirements and methods of testing for one or more of the following requirements: need for and type of test specimens
(8.1), composition (8.2), thickness (8.4), adhesion (8.6), and absence of hydrogen embrittlement and the waiting period prior to
testing and testing loads (8.8) and lubricating resistance (S2).
4.1.5 Sampling plan for each inspection criterion and responsibility for inspection, if necessary (Section 6 and Supplementary
Requirement S1).
4.1.6 Requirements for certified report of test results (Section 10).
5. Requirements
5.1 Nature of Finish—The coating shall be 45 to 75 mass % cadmium, the remainder tin.
5.2 Process:
5.2.1 Stress Relief Treatment—All steel parts that have ultimate tensile strength of 1000 MPa and above and that contain tensile
stresses caused by machining, grinding, straightening, or cold forming operation shall be given a stress relief heat treatment prior
to cleaning and metal deposition. The temperature and time at temperature shall be 190 6 15°C for a minimum of 3 h so that
maximum stress relief is obtained without reducing the hardness below the specified minimum.
5.2.2 High-strength steels that have heavy oxide or scale shall be cleaned before application of the coating in accordance with
Guide B242. In general, non-electrolytic alkaline, anodic-alkaline, and some inhibited acid cleaners are preferred to avoid the risk
of producing hydrogen embrittlement from the cleaning procedure.
5.2.3 For preparation of low-carbon steels, see Practice B183. For cleaning, useful guidelines are also given in Guide B322.
5.2.4 Supplementary Treatments:
5.2.4.1 Chromate treatment for Type II shall be done in a solution containing hexavalent chromium. This solution shall produce
a bright or semi-bright continuous, smooth, protective film. This film may have a slight yellowish or iridescent color. The absence
of color shall not be considered evidence of the absence of a Type II film or as a basis for rejection of the parts. Only post treatments
that contain salts that yield films containing hexavalent chromium are permitted as treatments for producing Type II coatings.
5.2.4.2 Waxes, lacquers, or other organic coatings may be used to improve lubricity, and the need for them should be supplied
in the purchase order or other governing document (4.1.1). Such supplemental lubrication treatments shall not be used to ensure
conformance to the salt spray corrosion resistant requirements or to enhance the test results of the lead acetate spot test (8.5.2).
5.3 Thickness:
5.3.1 The thickness of the coating everywhere on the significant surfaces shall be at least that of the specified class as defined
in 3.1.
5.3.2 Significant surfaces are defined as those normally visible (directly or by reflection) that are essential to the appearance or
serviceability of the article when assembled in normal position; or which can be the source of corrosion products that deface visible
surfaces on the assembled article. When necessary, the significant surfaces shall be indicated on the drawing of the article, or by
the provision of suitably marked samples.
NOTE 1—The thickness of mechanically-deposited coatings varies from point-to-point on the surface of a product, characteristically tending to be
thicker on flat surfaces and thinner at exposed edges, sharp projections, shielded or recessed areas, interior corners and holes, with such thinner areas often
being exempted from thickness requirement.
5.3.3 When significant surfaces are involved on which the specified thickness of deposit cannot readily be controlled, the
purchaser and manufacturer should recognize the necessity for either thicker or thinner deposits. For example, to reduce buildup
in thread roots, holes, deep recesses, bases of angles, and similar areas, the deposit thickness on the more accessible surfaces will
have to be reduced proportionately.
NOTE 2—The coating thickness requirement of this specification is a minimum requirement; that is, the coating thickness is required to equal or exceed
B635 − 00 (2015)
the specified thickness everywhere on the significant surfaces. Variation in the coating thickness from point to point on a coated article is an inherent
characteristic of mechanical deposition processes. Therefore, the coating thickness will have to exceed the specified value at some points on the significant
surfaces to ensure that the thickness equals or exceeds the specified value at all points. Thus, in most cases, the average coating thickness on an article
will be greater than the specified value; how much greater is largely determined by the shape of the article and the characteristics of the deposition process.
In addition, the average coating thickness on articles will vary from article to article within a production lot. Therefore, if all of the articles in a production
lot are to meet the thickness requirement, the average coating thickness for the production lot as a whole will be greater than the average necessary to
ensure that a single article meets the requirement.
5.4 Adhesion—The cadmium-tin coating shall be sufficiently adherent to the basis metal to pass the tests specified in 8.6.
5.5 Corrosion Resistance:
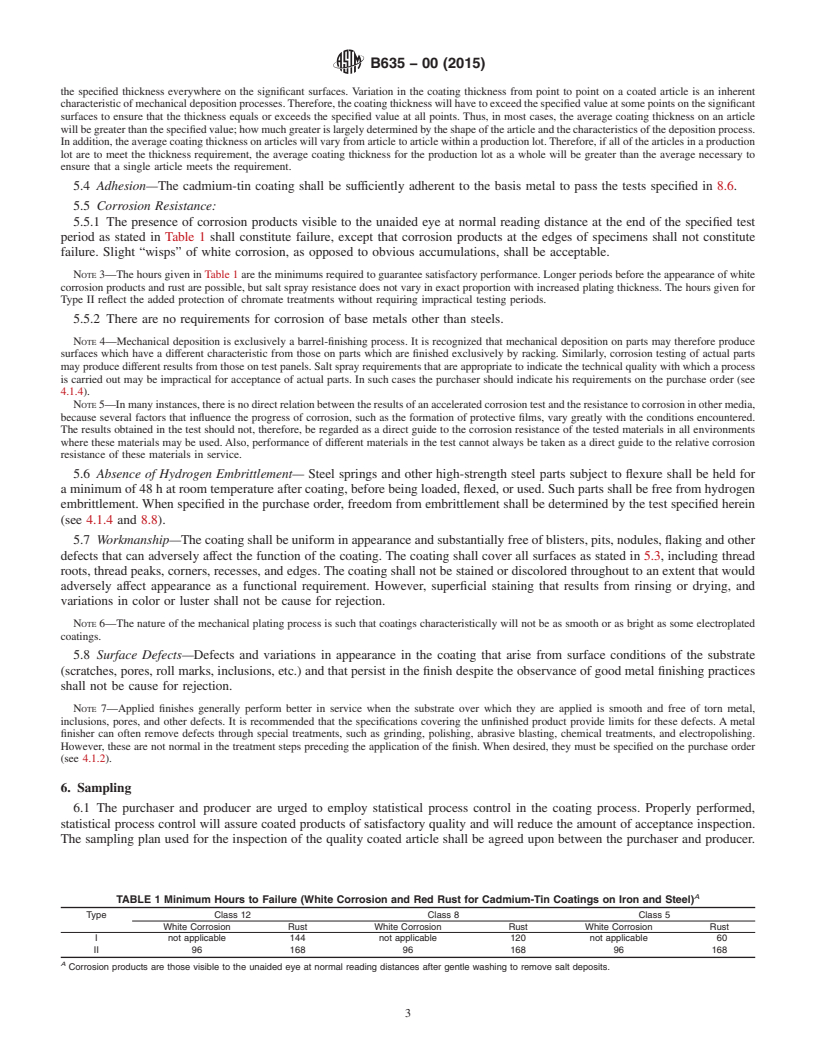
5.5.1 The presence of corrosion products visible to the unaided eye at normal reading distance at the end of the specified test
period as stated in Table 1 shall constitute failure, except that corrosion products at the edges of specimens shall not constitute
failure. Slight “wisps” of white corrosion, as opposed to obvious accumulations, shall be acceptable.
NOTE 3—The hours given in Table 1 are the minimums required to guarantee satisfactory performance. Longer periods before the appearance of white
corrosion products and rust are possible, but salt spray resistance does not vary in exact proportion with increased plating thickness. The hours given for
Type II reflect the added protection of chromate treatments without requiring impractical testing periods.
5.5.2 There are no requirements for corrosion of base metals other than steels.
NOTE 4—Mechanical deposition is exclusively a barrel-finishing process. It is recognized that mechanical deposition on parts may therefore produce
surfaces which have a different characteristic from those on parts which are finished exclusively by racking. Similarly, corrosion testing of actual parts
may produce different results from those on test panels. Salt spray requirements that are appropriate to indicate the technical quality with which a process
is carried out may be impractical for acceptance of actual parts. In such cases the purchaser should indicate his requirements on the purchase order (see
4.1.4).
NOTE 5—In many instances, there is no direct relation between the results of an accelerated corrosion test and the resistance to corrosion in other media,
because several factors that influence the progress of corrosion, such as the formation of protective films, vary greatly with the conditions encountered.
The results obtained in the test should not, therefore, be regarded as a direct guide to the corrosion resistance of the tested materials in all environments
where these materials may be used. Also, performance of different materials in the test cannot always be taken as a direct guide to the relative corrosion
resistance of these materials in service.
5.6 Absence of Hydrogen Embrittlement— Steel springs and other high-strength steel parts subject to flexure shall be held for
a minimum of 48 h at room temperature after coating, before being loaded, flexed, or used. Such parts shall be free from hydrogen
embrittlement. When specified in the purchase order, freedom from embrittlement shall be determined by the test specified herein
(see 4.1.4 and 8.8).
5.7 Workmanship—The coating shall be uniform in appearance and substantially free of blisters, pits, nodules, flaking and other
defects that can adversely affect the function of the coating. The coating shall cover all surfaces as stated in 5.3, including thread
roots, thread peaks, corners, recesses, and edges. The coating shall not be stained or discolored throughout to an extent that would
adversely affect appearance as a functional requirement. However, superficial staining that results from rinsing or drying, and
variations in color or luster shall not be cause for rejection.
NOTE 6—The nature of the mechanical plating process is such that coatings characteristically will not be as smooth or as bright as some electroplated
coatings.
5.8 Surface Defects—Defects and variations in appearance in the coating that arise from surface conditions of the substrate
(scratches, pores, roll marks, inclusions, etc.) and that persist in the finish despite the observance of good metal finishing practices
shall not be cause for rejection.
NOTE 7—Applied finishes generally perform better in service when the substrate over which they are applied is smooth and free of torn metal,
inclusions, pores, and other defects. It is recommended that the specifications covering the unfinished product provide limits for these defects. A metal
finisher can often remove defects through special treatments, such as grinding, polishing, abrasive blasting, chemical treatments, and electropolishing.
However, these are not normal in the treatment steps preceding the application of the finish. When desired, they must be specified on the purchase order
(see 4.1.2).
6. Sampling
6.1 The purchaser and producer are urged to employ statistical process control in the coating process. Properly performed,
statistical process control will assure coated products of satisfactory quality and will reduce the amount of acceptance i
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.