


ASTM B579-73(2015)
(Specification)Standard Specification for Electrodeposited Coatings of Tin-Lead Alloy (Solder Plate)
Standard Specification for Electrodeposited Coatings of Tin-Lead Alloy (Solder Plate)
ABSTRACT
This specification establishes the requirements for mat, bright, and flow-brightened electrodeposited tin-lead alloy coatings on fabricated articles of iron, steel, copper, and copper alloys to protect them against corrosion, to improve and preserve solderability over long periods of storage, and to improve anti-galling characteristics. Sheets, strips, or wires in the unfabricated form, or threaded articles having a specified diameter, are not covered here. The classification notation shall include the type of basis metal, thickness of tin-lead coating required, service condition number indicating the severity of service required, and coating composition. Coatings shall be sampled, tested, and shall conform accordingly to specified requirements as to composition, appearance, thickness, adhesion (to be examined either by burnishing test, quenching test, reflow test, or bend test), and solderability (to be assessed either by non-automated or automated dip test, spread test, globule test, or artificial aging test).
SCOPE
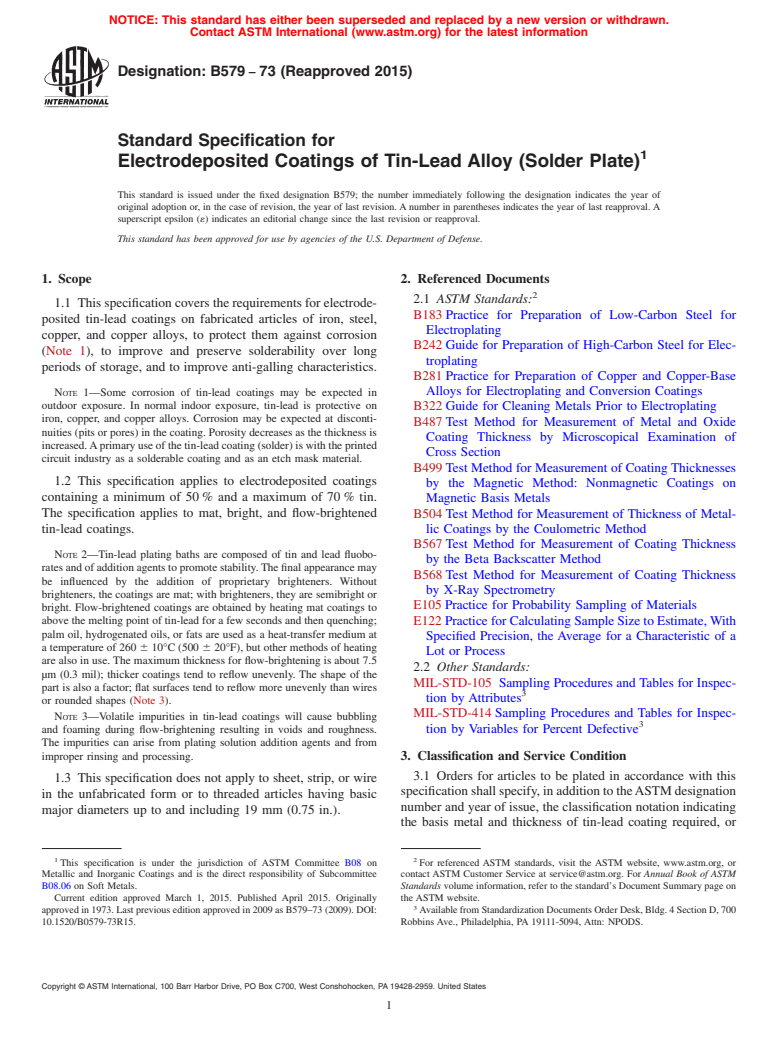
1.1 This specification covers the requirements for electrodeposited tin-lead coatings on fabricated articles of iron, steel, copper, and copper alloys, to protect them against corrosion (Note 1), to improve and preserve solderability over long periods of storage, and to improve anti-galling characteristics.
Note 1: Some corrosion of tin-lead coatings may be expected in outdoor exposure. In normal indoor exposure, tin-lead is protective on iron, copper, and copper alloys. Corrosion may be expected at discontinuities (pits or pores) in the coating. Porosity decreases as the thickness is increased. A primary use of the tin-lead coating (solder) is with the printed circuit industry as a solderable coating and as an etch mask material.
1.2 This specification applies to electrodeposited coatings containing a minimum of 50 % and a maximum of 70 % tin. The specification applies to mat, bright, and flow-brightened tin-lead coatings.
Note 2: Tin-lead plating baths are composed of tin and lead fluoborates and of addition agents to promote stability. The final appearance may be influenced by the addition of proprietary brighteners. Without brighteners, the coatings are mat; with brighteners, they are semibright or bright. Flow-brightened coatings are obtained by heating mat coatings to above the melting point of tin-lead for a few seconds and then quenching; palm oil, hydrogenated oils, or fats are used as a heat-transfer medium at a temperature of 260 ± 10°C (500 ± 20°F), but other methods of heating are also in use. The maximum thickness for flow-brightening is about 7.5 μm (0.3 mil); thicker coatings tend to reflow unevenly. The shape of the part is also a factor; flat surfaces tend to reflow more unevenly than wires or rounded shapes (Note 3).
Note 3: Volatile impurities in tin-lead coatings will cause bubbling and foaming during flow-brightening resulting in voids and roughness. The impurities can arise from plating solution addition agents and from improper rinsing and processing.
1.3 This specification does not apply to sheet, strip, or wire in the unfabricated form or to threaded articles having basic major diameters up to and including 19 mm (0.75 in.).
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: B579 −73 (Reapproved 2015)
Standard Specification for
Electrodeposited Coatings of Tin-Lead Alloy (Solder Plate)
This standard is issued under the fixed designation B579; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope 2. Referenced Documents
2.1 ASTM Standards:
1.1 Thisspecificationcoverstherequirementsforelectrode-
B183Practice for Preparation of Low-Carbon Steel for
posited tin-lead coatings on fabricated articles of iron, steel,
Electroplating
copper, and copper alloys, to protect them against corrosion
B242Guide for Preparation of High-Carbon Steel for Elec-
(Note 1), to improve and preserve solderability over long
troplating
periods of storage, and to improve anti-galling characteristics.
B281Practice for Preparation of Copper and Copper-Base
Alloys for Electroplating and Conversion Coatings
NOTE 1—Some corrosion of tin-lead coatings may be expected in
outdoor exposure. In normal indoor exposure, tin-lead is protective on
B322Guide for Cleaning Metals Prior to Electroplating
iron, copper, and copper alloys. Corrosion may be expected at disconti-
B487Test Method for Measurement of Metal and Oxide
nuities(pitsorpores)inthecoating.Porositydecreasesasthethicknessis
Coating Thickness by Microscopical Examination of
increased.Aprimaryuseofthetin-leadcoating(solder)iswiththeprinted
Cross Section
circuit industry as a solderable coating and as an etch mask material.
B499Test Method for Measurement of CoatingThicknesses
1.2 This specification applies to electrodeposited coatings
by the Magnetic Method: Nonmagnetic Coatings on
containing a minimum of 50% and a maximum of 70% tin.
Magnetic Basis Metals
The specification applies to mat, bright, and flow-brightened B504Test Method for Measurement of Thickness of Metal-
tin-lead coatings. lic Coatings by the Coulometric Method
B567Test Method for Measurement of Coating Thickness
NOTE 2—Tin-lead plating baths are composed of tin and lead fluobo-
by the Beta Backscatter Method
ratesandofadditionagentstopromotestability.Thefinalappearancemay
B568Test Method for Measurement of Coating Thickness
be influenced by the addition of proprietary brighteners. Without
by X-Ray Spectrometry
brighteners, the coatings are mat; with brighteners, they are semibright or
E105Practice for Probability Sampling of Materials
bright. Flow-brightened coatings are obtained by heating mat coatings to
abovethemeltingpointoftin-leadforafewsecondsandthenquenching; E122PracticeforCalculatingSampleSizetoEstimate,With
palm oil, hydrogenated oils, or fats are used as a heat-transfer medium at
Specified Precision, the Average for a Characteristic of a
a temperature of 260 6 10°C (500 6 20°F), but other methods of heating
Lot or Process
are also in use. The maximum thickness for flow-brightening is about 7.5
2.2 Other Standards:
µm (0.3 mil); thicker coatings tend to reflow unevenly. The shape of the
MIL-STD-105 Sampling Procedures and Tables for Inspec-
part is also a factor; flat surfaces tend to reflow more unevenly than wires
tion by Attributes
or rounded shapes (Note 3).
MIL-STD-414Sampling Procedures and Tables for Inspec-
NOTE 3—Volatile impurities in tin-lead coatings will cause bubbling
and foaming during flow-brightening resulting in voids and roughness. tion by Variables for Percent Defective
The impurities can arise from plating solution addition agents and from
improper rinsing and processing. 3. Classification and Service Condition
3.1 Orders for articles to be plated in accordance with this
1.3 This specification does not apply to sheet, strip, or wire
specificationshallspecify,inadditiontotheASTMdesignation
in the unfabricated form or to threaded articles having basic
number and year of issue, the classification notation indicating
major diameters up to and including 19 mm (0.75 in.).
the basis metal and thickness of tin-lead coating required, or
1 2
This specification is under the jurisdiction of ASTM Committee B08 on For referenced ASTM standards, visit the ASTM website, www.astm.org, or
Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
B08.06 on Soft Metals. Standards volume information, refer to the standard’s Document Summary page on
Current edition approved March 1, 2015. Published April 2015. Originally the ASTM website.
approvedin1973.Lastpreviouseditionapprovedin2009asB579–73(2009).DOI: AvailablefromStandardizationDocumentsOrderDesk,Bldg.4SectionD,700
10.1520/B0579-73R15. Robbins Ave., Philadelphia, PA 19111-5094, Attn: NPODS.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B579 − 73 (2015)
the service condition number indicating the severity of service 5.2 Whenrequiredthebasismetalshallbesubjectedtosuch
requiredforthecoating.Inaddition,whenspecifyingatin-lead polishing or buffing operations as are necessary to yield
coating composition, the first number shall refer to the tin deposits with the desired final appearance (Section 6).
content in percent.
5.3 Properpreparatoryproceduresandthoroughcleaningof
3.1.1 Classification Notation:
the basis metal surface are essential in order to assure satis-
Symbol Classification
factory adhesion and corrosion performance of the coating.
Fe/ Iron or steel basis metals
Accordingly,itissuggestedthatthefollowingPracticesforthe
Cu/ Copper or copper alloy basis metals
preparation of various basis metals for electroplating be
/Sn-Pb Tin-lead coating and its composition number, when re-
quired; for example, Sn60-Pb40
followed when appropriate: B183, B281, and B322 and Guide
Number Minimum coating thickness in micrometres
B242.
(5 to 50)
5.4 Whennecessary,preliminarysamplesshowingthefinish
Suffix Letter
shallbesuppliedtoandapprovedbythepurchaser.Whererack
f flow-brightened
b bright marks are inevitable, their location shall be the subject of
m mat
agreement between supplier and purchaser.
6. Physical Composition
An example of complete classification notation is as follows:
Cu/Sn60-Pb40/5F
6.1 Composition—Thetin-leadcoatingcompositionshallbe
3.1.2 Service Condition Number:
as follows (Note 7):
No. Service Condition Element Weight, %
Tin (Sn) 50 to 70
4 very severe exposure Lead (Pb) remainder
3 severe exposure
6.1.1 The tin percentage is calculated as follows:
2 moderate exposure
1 mild exposure
Tin,% 5134.1 3 L/A 21 (1)
~ !
NOTE 4—See Appendix X1 for additional description of exposure
where:
conditions and examples of typical end uses. The coating thicknesses
given for each service condition are guidelines and are not intended to be L = weight of lead coating, g, and
absolute values.
A = weight of alloy coating, g.
NOTE 7—Only the tin content need be determined. Lead is usually
determined by difference. A sample of the deposit can be obtained by
4. Significant Surfaces
plating on a stainless steel panel from which the coating can be peeled or
4.1 Significant surfaces are defined as those surfaces nor-
by employing any recognized stripping method.The alloy composition of
the deposit can be determined by methods such as gravimetric or
mally visible (directly or by reflection) that are essential to the
volumetric analysis, density measurements, atomic absorption
appearance or serviceability of the article when assembled in
spectrophotometry, X-ray fluorescence, and beta backscatter.
normal position; or those surfaces that can be the source of
In addition, the alloy composition produced by a plating solution may
corrosion products that will deface visible surfaces on the
be obtained by comparing the weight of a tin-lead coating deposited by a
assembled article. When necessary, the significant surfaces
given number of ampere-hours to the weight of lead coating produced in
a lead fluoborate coulometer in series with the plating bath.
shall be indicated on the drawing of the part, or by the
provision of suitably marked samples.
6.2 Appearance—The tin-lead coating shall be smooth, fine
grained, continuous, adherent, and shall be free of visible
NOTE 5—When significant surfaces include areas on which the speci-
blisters, pits, nodules, indications of burning, excessive build-
fied thickness of deposit cannot readily be controlled, such as threads,
holes, deep recesses, bases of angles, and similar areas, the purchaser and up, staining, and other defects. Flow-brightened coatings shall
themanufacturershouldrecognizethenecessityforeitherthickerdeposits
not have dewetted areas or beads, and shall be free of the oil
on the more accessible surfaces or for special racking. Special racks may
used in the fusion process.
involve the use of conforming, auxiliary bipolar electrodes, or noncon-
ducting shields.
6.3 Thickness—The thickness of the coating on significant
surfacesshallconformtotherequirementsinTable1andTable
5. Materials and Manufacture
5.1 Defects in the surface of the basis metal, such as
TABLE 1 Tin-Lead Alloy Coatings on Steel
scratches, porosity, nonconducting inclusions, roll and die
Minimum
Service Classification
marks, cold shuts, and cracks, may adversely affect the
Thickness
Condition Number
appearance and the performance of coatings applied thereto
µm mil
A
despite the observance of the best plating practices.
SC4 Fe/SnPb 30 30 1.2
A
SC3 Fe/SnPb 20 20 0.8
Accordingly, the plater’s responsibility for defects in the
SC2 Fe/SnPb 10 10 0.4
coating resulting from such conditions shall be waived, except
SC1 Fe/SnPb 5 5 0.2
B
when he is also in the position of prime contractor supplying
SC1 Fe/SnPb 5f 50.2
A
plated parts.
An undercoat of 2.5 µm (0.1 mil) copper is recommended for SC3 and SC4.
B
f = flow brightened or
NOTE 6—In order to minimize problems of this sort, the specifications
m = mat or
covering the basis material or the item to be plated should contain
b=bright
appropriate limitations on such basis metal conditions.
B579 − 73 (2015)
2. chasershouldselectasuitablesamplingplanfortheacceptance
6.3.1 Thickness Measurements—Tin-lead alloy thickness testing of lots of coated items. In order that the manufacturer
measurements shall be made on those areas of the significant (plater) may know the quality standard he is expected to meet,
surfaces where the coating would be expected to be thinnest. theplanselectedshouldbemadepartofthepurchasecontract.
The method of determining the thickness shall be agreed upon
8.2 General information on sampling procedures is given in
by the manufacturer and purchaser. Several methods are
Recommended Practices E105 and E122. Standard sampling
availabledependinguponthethicknessofcoating,theshapeof
plans are suggested in Military Standards MIL-STD-105 and
the article, and the basis metal. They include beta backscatter,
MIL-STD-414.
coulometric, magnetic, microscopical, and X-ray fluorescence
test methods. The methods are outlined in 9.1.
9. Test Methods
NOTE 8—Thicknesses determined by beta backscatter, coulometry, and
9.1 Thickness:
X-ray fluorescence are a function of the composition as well as the
9.1.1 To meet the thickness specifications of the coatings,
thickness of the coating.
the plater is advised to:
6.4 Adhesion—The adhesion of the coating shall be ad-
9.1.1.1 Maintain regular control of all solutions,
equate to pass the tests described in 9.2.
9.1.1.2 Inspect the equipment at regular intervals, and
6.5 Solderability:
9.1.1.3 Check thickness at periodic intervals.
6.5.1 When specified by the purchaser, the coating shall be
9.1.2 The following ASTM methods are acceptable for
testedbyoneofthemethodsdescribedin9.2.Theresultsshall
measuring local thickness of the coating: B487, B499, B504,
be evaluated in accordance with each procedure described in
B567, and B568.
that section.
9.2 Adhesion:
6.5.2 When specified by the purchaser, the coating on
9.2.1 Burnishing Test—Rub an area of not more than 630
copper and copper alloys shall, before solderability testing, be
2 2
mm (1 in. ) of the coated surface, selected at the discretion of
subjectedtothepreliminaryartificialagingtreatmentdescribed
the inspector, rapidly and firmly for 15 s with a smooth metal
in 9.3.6 to determine if they may be expected to retain their
implement. A suitable burnishing implement is a copper or
solderability during periods of storage.
steel disk used edgewise and broadside. Maintain a pressure
NOTE9—SeeAppendixX2fordesignconsiderationsthathaveaneffect
sufficienttoburnishthecoatingateverystroke,butnotsogreat
on the selection of thickness of the coating and, ultimately, on the
as to cut it. Poor adhesion will be shown by the appearance of
solderability of the electrodeposits.
a loose blister which grows as burnishing is continued. If the
qualityofthecoatingispooralso,theblistermaycrackandthe
7. Hydrogen Embrittlement
coating peel away from the basis metal.
7.1 High-tensile strength steels, and severely cold-worked
9.2.2 Quenching Test—Heat the coating article in an oven
steels, are susceptible to embrittlement by hydrogen in both
for a sufficient time to reach 150 6 10°C (300 6 20°F) and
cleaning and plating operations. The embrittling hydrogen
quenchinroom-temperaturewater.Theadhesionisinadequate
shall be removed by heat treatment. Procedures for baking to
if the coating blisters, cracks, or peels.
minimizeembrittlementbeforeandafterplatingarecoveredin
9.2.3 Reflow Test—Parts may be evaluated by immersion in
Sections 2 and 7 of Guide B242.
a bath of palm oil at a temperature of 205 – 260°C (400 –
500°F) until the deposit melts. A bright coating completely
8. Sampling
covering the significant surfaces indicates adequate adhesion.
8.1 Test methods are time consuming and often destructive;
9.2.4 Bend Test—Bend a sample, with the coated surface
therefore 100% inspection is usually impractical. The pur-
away, over a mandrel until its two legs are parallel. The
mandrel shall have a diameter equal to the thickness of the
sample. Examination at 4× magnification should show no
A
TABLE 2 Tin-Lead Alloy Coatings on Copper, Copper Alloys ,
B
and Nonmetals evidence of peeling or cracking.
Minimum
9.3 Solderability:
Service Classification
Thickness
Condition Number
9.3.1 General:
µm mil
9.3.1.1 Methods for testing the solderability of tin-lead
SC4 Cu/SnPb 30 30 1.2
coated articles are based on the measurement of the extent of
SC3 Cu/SnPb 15 15 0.6
SC2 Cu/SnPb 8 8 0.3
wetting by molten solder or the determination of the minimum
SC1 Cu/SnPb 5 5 0.2
time required to produce full or perfect wetting by
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B579 − 73 (Reapproved 2009) B579 − 73 (Reapproved 2015)
Standard Specification for
Electrodeposited Coatings of Tin-Lead Alloy (Solder Plate)
This standard is issued under the fixed designation B579; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope
1.1 This specification covers the requirements for electrodeposited tin-lead coatings on fabricated articles of iron, steel, copper,
and copper alloys, to protect them against corrosion (Note 1), to improve and preserve solderability over long periods of storage,
and to improve anti-galling characteristics.
NOTE 1—Some corrosion of tin-lead coatings may be expected in outdoor exposure. In normal indoor exposure, tin-lead is protective on iron, copper,
and copper alloys. Corrosion may be expected at discontinuities (pits or pores) in the coating. Porosity decreases as the thickness is increased. A primary
use of the tin-lead coating (solder) is with the printed circuit industry as a solderable coating and as an etch mask material.
1.2 This specification applies to electrodeposited coatings containing a minimum of 50 % and a maximum of 70 % tin. The
specification applies to mat, bright, and flow-brightened tin-lead coatings.
NOTE 2—Tin-lead plating baths are composed of tin and lead fluoborates and of addition agents to promote stability. The final appearance may be
influenced by the addition of proprietary brighteners. Without brighteners, the coatings are mat; with brighteners, they are semibright or bright.
Flow-brightened coatings are obtained by heating mat coatings to above the melting point of tin-lead for a few seconds and then quenching; palm oil,
hydrogenated oils, or fats are used as a heat-transfer medium at a temperature of 260 6 10°C (500 6 20°F), but other methods of heating are also in
use. The maximum thickness for flow-brightening is about 7.5 μm (0.3 mil); thicker coatings tend to reflow unevenly. The shape of the part is also a factor;
flat surfaces tend to reflow more unevenly than wires or rounded shapes (Note 3).
NOTE 3—Volatile impurities in tin-lead coatings will cause bubbling and foaming during flow-brightening resulting in voids and roughness. The
impurities can arise from plating solution addition agents and from improper rinsing and processing.
1.3 This specification does not apply to sheet, strip, or wire in the unfabricated form or to threaded articles having basic major
diameters up to and including 19 mm (0.75 in.).
2. Referenced Documents
2.1 ASTM Standards:
B183 Practice for Preparation of Low-Carbon Steel for Electroplating
B242 Guide for Preparation of High-Carbon Steel for Electroplating
B281 Practice for Preparation of Copper and Copper-Base Alloys for Electroplating and Conversion Coatings
B322 Guide for Cleaning Metals Prior to Electroplating
B487 Test Method for Measurement of Metal and Oxide Coating Thickness by Microscopical Examination of Cross Section
B499 Test Method for Measurement of Coating Thicknesses by the Magnetic Method: Nonmagnetic Coatings on Magnetic Basis
Metals
B504 Test Method for Measurement of Thickness of Metallic Coatings by the Coulometric Method
B567 Test Method for Measurement of Coating Thickness by the Beta Backscatter Method
B568 Test Method for Measurement of Coating Thickness by X-Ray Spectrometry
E105 Practice for Probability Sampling of Materials
E122 Practice for Calculating Sample Size to Estimate, With Specified Precision, the Average for a Characteristic of a Lot or
Process
This specification is under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee B08.06 on Soft
Metals.
Current edition approved Sept. 1, 2009March 1, 2015. Published November 2009April 2015. Originally approved in 1973. Last previous edition approved in 20042009
as B579–73 (2004).–73 (2009). DOI: 10.1520/B0579-73R09.10.1520/B0579-73R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B579 − 73 (2015)
2.2 Other Standards:
MIL-STD-105 Sampling Procedures and Tables for Inspection by Attributes
MIL-STD-414 Sampling Procedures and Tables for Inspection by Variables for Percent Defective
3. Classification and Service Condition
3.1 Orders for articles to be plated in accordance with this specification shall specify, in addition to the ASTM designation
number and year of issue, the classification notation indicating the basis metal and thickness of tin-lead coating required, or the
service condition number indicating the severity of service required for the coating. In addition, when specifying a tin-lead coating
composition, the first number shall refer to the tin content in percent.
3.1.1 Classification Notation:
Symbol Classification
Fe/ Iron or steel basis metals
Cu/ Copper or copper alloy basis metals
/Sn-Pb Tin-lead coating and its composition number, when re-
quired; for example, Sn60-Pb40
Number Minimum coating thickness in micrometres
(5 to 50)
Suffix Letter
f flow-brightened
b bright
m mat
An example of complete classification notation is as follows: Cu/Sn60-Pb40/5F
3.1.2 Service Condition Number:
No. Service Condition
4 very severe exposure
3 severe exposure
2 moderate exposure
1 mild exposure
NOTE 4—See Appendix X1 for additional description of exposure conditions and examples of typical end uses. The coating thicknesses given for each
service condition are guidelines and are not intended to be absolute values.
4. Significant Surfaces
4.1 Significant surfaces are defined as those surfaces normally visible (directly or by reflection) that are essential to the
appearance or serviceability of the article when assembled in normal position; or those surfaces that can be the source of corrosion
products that will deface visible surfaces on the assembled article. When necessary, the significant surfaces shall be indicated on
the drawing of the part, or by the provision of suitably marked samples.
NOTE 5—When significant surfaces include areas on which the specified thickness of deposit cannot readily be controlled, such as threads, holes, deep
recesses, bases of angles, and similar areas, the purchaser and the manufacturer should recognize the necessity for either thicker deposits on the more
accessible surfaces or for special racking. Special racks may involve the use of conforming, auxiliary bipolar electrodes, or nonconducting shields.
5. Materials and Manufacture
5.1 Defects in the surface of the basis metal, such as scratches, porosity, nonconducting inclusions, roll and die marks, cold
shuts, and cracks, may adversely affect the appearance and the performance of coatings applied thereto despite the observance of
the best plating practices. Accordingly, the plater’s responsibility for defects in the coating resulting from such conditions shall be
waived, except when he is also in the position of prime contractor supplying plated parts.
NOTE 6—In order to minimize problems of this sort, the specifications covering the basis material or the item to be plated should contain appropriate
limitations on such basis metal conditions.
5.2 When required the basis metal shall be subjected to such polishing or buffing operations as are necessary to yield deposits
with the desired final appearance (Section 6).
5.3 Proper preparatory procedures and thorough cleaning of the basis metal surface are essential in order to assure satisfactory
adhesion and corrosion performance of the coating. Accordingly, it is suggested that the following Practices for the preparation of
various basis metals for electroplating be followed when appropriate: B183, B281, and B322 and Guide B242.
5.4 When necessary, preliminary samples showing the finish shall be supplied to and approved by the purchaser. Where rack
marks are inevitable, their location shall be the subject of agreement between supplier and purchaser.
Available from Standardization Documents Order Desk, Bldg. 4 Section D, 700 Robbins Ave., Philadelphia, PA 19111-5094, Attn: NPODS.
B579 − 73 (2015)
6. Physical Composition
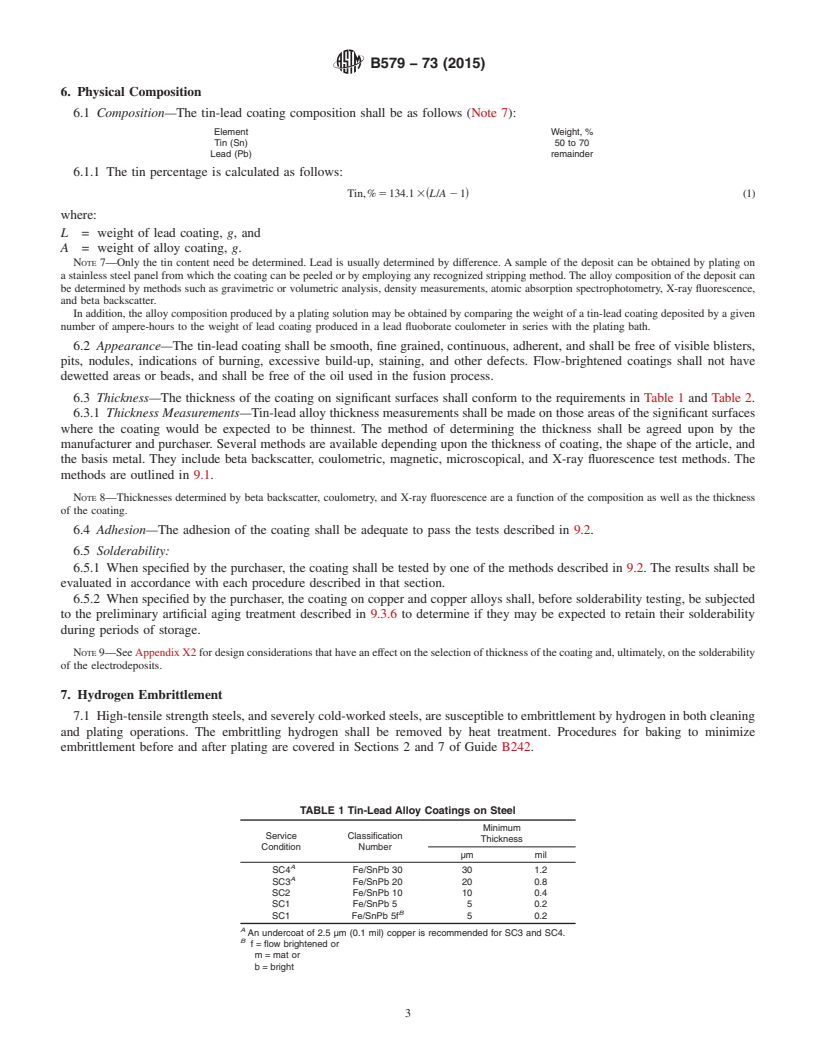
6.1 Composition—The tin-lead coating composition shall be as follows (Note 7):
Element Weight, %
Tin (Sn) 50 to 70
Lead (Pb) remainder
6.1.1 The tin percentage is calculated as follows:
Tin,%5 134.1 3~L/A 2 1! (1)
where:
L = weight of lead coating, g, and
A = weight of alloy coating, g.
NOTE 7—Only the tin content need be determined. Lead is usually determined by difference. A sample of the deposit can be obtained by plating on
a stainless steel panel from which the coating can be peeled or by employing any recognized stripping method. The alloy composition of the deposit can
be determined by methods such as gravimetric or volumetric analysis, density measurements, atomic absorption spectrophotometry, X-ray fluorescence,
and beta backscatter.
In addition, the alloy composition produced by a plating solution may be obtained by comparing the weight of a tin-lead coating deposited by a given
number of ampere-hours to the weight of lead coating produced in a lead fluoborate coulometer in series with the plating bath.
6.2 Appearance—The tin-lead coating shall be smooth, fine grained, continuous, adherent, and shall be free of visible blisters,
pits, nodules, indications of burning, excessive build-up, staining, and other defects. Flow-brightened coatings shall not have
dewetted areas or beads, and shall be free of the oil used in the fusion process.
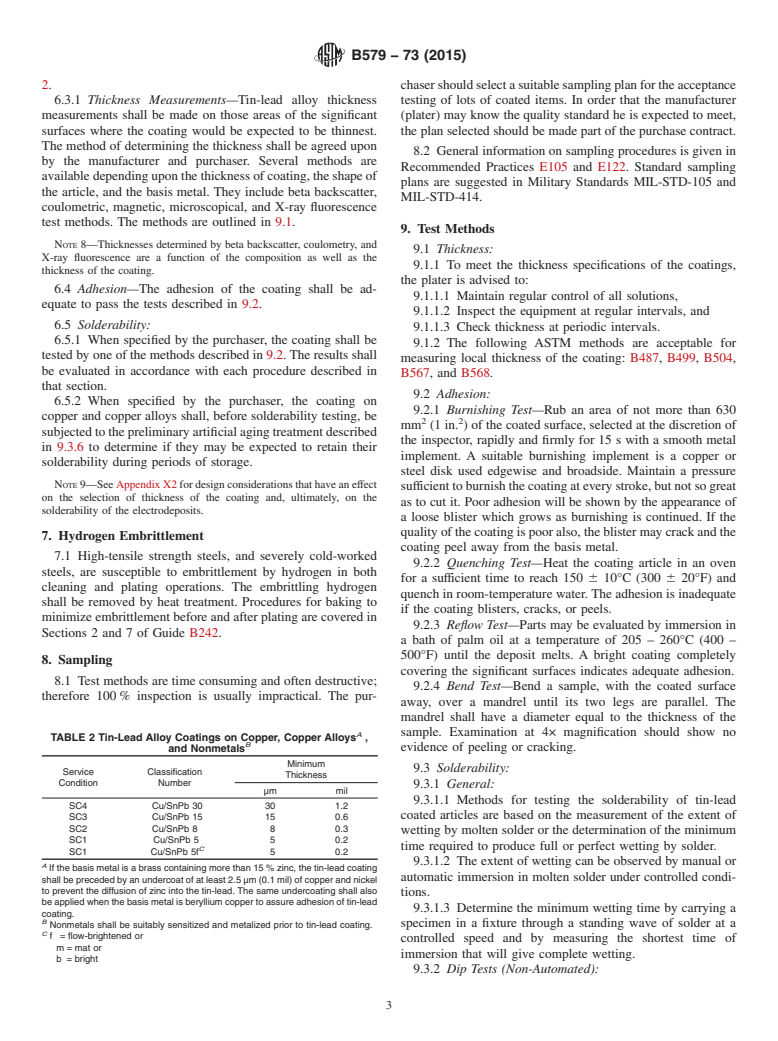
6.3 Thickness—The thickness of the coating on significant surfaces shall conform to the requirements in Table 1 and Table 2.
6.3.1 Thickness Measurements—Tin-lead alloy thickness measurements shall be made on those areas of the significant surfaces
where the coating would be expected to be thinnest. The method of determining the thickness shall be agreed upon by the
manufacturer and purchaser. Several methods are available depending upon the thickness of coating, the shape of the article, and
the basis metal. They include beta backscatter, coulometric, magnetic, microscopical, and X-ray fluorescence test methods. The
methods are outlined in 9.1.
NOTE 8—Thicknesses determined by beta backscatter, coulometry, and X-ray fluorescence are a function of the composition as well as the thickness
of the coating.
6.4 Adhesion—The adhesion of the coating shall be adequate to pass the tests described in 9.2.
6.5 Solderability:
6.5.1 When specified by the purchaser, the coating shall be tested by one of the methods described in 9.2. The results shall be
evaluated in accordance with each procedure described in that section.
6.5.2 When specified by the purchaser, the coating on copper and copper alloys shall, before solderability testing, be subjected
to the preliminary artificial aging treatment described in 9.3.6 to determine if they may be expected to retain their solderability
during periods of storage.
NOTE 9—See Appendix X2 for design considerations that have an effect on the selection of thickness of the coating and, ultimately, on the solderability
of the electrodeposits.
7. Hydrogen Embrittlement
7.1 High-tensile strength steels, and severely cold-worked steels, are susceptible to embrittlement by hydrogen in both cleaning
and plating operations. The embrittling hydrogen shall be removed by heat treatment. Procedures for baking to minimize
embrittlement before and after plating are covered in Sections 2 and 7 of Guide B242.
TABLE 1 Tin-Lead Alloy Coatings on Steel
Minimum
Service Classification
Thickness
Condition Number
μm mil
A
SC4 Fe/SnPb 30 30 1.2
A
SC3 Fe/SnPb 20 20 0.8
SC2 Fe/SnPb 10 10 0.4
SC1 Fe/SnPb 5 5 0.2
B
SC1 Fe/SnPb 5f 5 0.2
A
An undercoat of 2.5 μm (0.1 mil) copper is recommended for SC3 and SC4.
B
f = flow brightened or
m = mat or
b = bright
B579 − 73 (2015)
A
TABLE 2 Tin-Lead Alloy Coatings on Copper, Copper Alloys ,
B
and Nonmetals
Minimum
Service Classification
Thickness
Condition Number
μm mil
SC4 Cu/SnPb 30 30 1.2
SC3 Cu/SnPb 15 15 0.6
SC2 Cu/SnPb 8 8 0.3
SC1 Cu/SnPb 5 5 0.2
C
SC1 Cu/SnPb 5f 5 0.2
A
If the basis metal is a brass containing more than 15 % zinc, the tin-lead coating
shall be preceded by an undercoat of at least 2.5 μm (0.1 mil) of copper and nickel
to prevent the diffusion of zinc into the tin-lead. The same undercoating shall also
be applied when the basis metal is beryllium copper to assure adhesion of tin-lead
coating.
B
Nonmetals shall be suitably sensitized and metalized prior to tin-lead coating.
C
f = flow-brightened or
m = mat or
b = bright
8. Sampling
8.1 Test methods are time consuming and often destructive; therefore 100 % inspection is usually impractical. The purchaser
should select a suitable sampling plan for the acceptance testing of lots of coated items. In order that the manufacturer (plater) may
know the quality standard he is expected to meet, the plan selected should be made part of the purchase contract.
8.2 General information on sampling procedures is given in Recommended Practices E105 and E122. Standard sampling plans
are suggested in Military Standards MIL-STD-105 and MIL-STD-414.
9. Test Methods
9.1 Thickness:
9.1.1 To meet the thickness specifications of the coatings, the plater is advised to:
9.1.1.1 Maintain regular control of all solutions,
9.1.1.2 Inspect the equipment at regular intervals, and
9.1.1.3 Check thickness at periodic intervals.
9.1.2 The following ASTM methods are acceptable for measuring local thickness of the coating: B487, B499, B504, B567, and
B568.
9.2 Adhesion:
2 2
9.2.1 Burnishing Test—Rub an area of not more than 630 mm (1 in. ) of the coated surface, selected at the discretion of the
inspector, rapidly and firmly for 15 s with a smooth metal implement. A suitable burnishing implement is a copper or steel disk
used edgewise and broadside. Maintain a pressure sufficient to burnish the coating at every stroke, but not so great as to cut it. Poor
ad
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.