


ASTM B537-70(2019)
(Practice)Standard Practice for Rating of Electroplated Panels Subjected to Atmospheric Exposure
Standard Practice for Rating of Electroplated Panels Subjected to<brk/> Atmospheric Exposure
ABSTRACT
This practice covers the recommended method for rating the condition of electroplated test panels subjected to corrosive environments for test purposes. This method is used with standard-sized panels exposed on standard ASTM racks at outdoor test sites in both natural atmospheres and accelerated test conditions. This practice refers only to decorative-protective coatings that are cathodic to the substrate such as nickel/chromium or copper/nickel/chromium on steel or zinc die castings, and is not intended for use with anodic sacrificial coatings such as zinc and cadmium on steel. Any modifications needed to adapt the method to rating actual production parts are not considered here. Panels shall be assigned separate rating numbers based on the ability of the coating to protect the substrate from corrosion (protection rating), and the overall appearance of panels as affected by deterioration of the coating itself (appearance rating). Accordingly, rating numbers shall be derived from the type of defect that exists, that is: (1) protection defects, which include crater rusting, pinhole rusting, rust stains, blisters, and other defects that involve basis metal corrosion; and (2) appearance defects, which include surface pits, "crow's feet," crack patterns, surface stains, tarnishes, and other defects that detract from commercial acceptability as to appearance. Inspection should be made in the as-is condition, and defects to be taken into account are only those that can be seen with the unaided eye at normal reading distance.
SCOPE
1.1 This practice covers a preferred method for evaluating the condition of electroplated test panels that have been exposed to corrosive environments for test purposes. It is based on experience in use of the method with standard 10- by 15-cm (4- by 6-in.) panels exposed on standard ASTM racks at outdoor test sites in natural atmospheres. It has been used also for rating similar panels that have been subjected to accelerated tests such as those covered by Practice B117, Method B287, Test Method B368, and Test Method B380. Any modifications needed to adapt the method to rating actual production parts are not considered in this practice.
1.2 This practice refers only to decorative-protective coatings that are cathodic to the substrate, typified by nickel/chromium or copper/nickel/chromium on steel or zinc die castings. It is not intended for use with anodic sacrificial coatings such as zinc and cadmium on steel.
1.3 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: B537 − 70 (Reapproved 2019)
Standard Practice for
Rating of Electroplated Panels Subjected to
Atmospheric Exposure
This standard is issued under the fixed designation B537; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope Spray (Fog) Testing (CASS Test)
B380Test Method for Corrosion Testing of Decorative
1.1 This practice covers a preferred method for evaluating
Electrodeposited Coatings by the Corrodkote Procedure
the condition of electroplated test panels that have been
2.2 ASTM Adjunct:
exposedtocorrosiveenvironmentsfortestpurposes.Itisbased
Dot charts (9 charts, 8 ⁄2 by 11 in.) (9 color photos, 3 by 5
onexperienceinuseofthemethodwithstandard10-by15-cm
in.)
(4- by 6-in.) panels exposed on standard ASTM racks at
outdoor test sites in natural atmospheres. It has been used also
3. Basis of Procedure
forratingsimilarpanelsthathavebeensubjectedtoaccelerated
3.1 The rating method described in this recommended
tests such as those covered by Practice B117, Method B287,
practice is based on the recognition that typical decorative-
Test Method B368, and Test Method B380.Any modifications
protective deposits such as nickel/chromium, with or without a
neededtoadaptthemethodtoratingactualproductionpartsare
copper undercoat, have two functions: (1) to protect the
not considered in this practice.
substrate from corrosion and thus prevent degradation of
1.2 This practice refers only to decorative-protective coat-
appearance caused by basis metal corrosion products (for
ings that are cathodic to the substrate, typified by nickel/
example, rust and rust stain); and (2) to itself maintain a
chromium or copper/nickel/chromium on steel or zinc die
satisfactoryappearance.Althoughthesefunctionsoverlap,they
castings. It is not intended for use with anodic sacrificial
can be evaluated separately, and it is frequently desirable to do
coatings such as zinc and cadmium on steel.
so. Accordingly, this practice assigns separate ratings to (1)
1.3 This international standard was developed in accor-
appearance as affected by corrosion of the substrate and (2)
dance with internationally recognized principles on standard-
appearance as affected by deterioration of the coating itself.
ization established in the Decision on Principles for the
3.2 The rating number assigned to the ability of the coating
Development of International Standards, Guides and Recom-
to protect the substrate from corrosion is called the “protec-
mendations issued by the World Trade Organization Technical
tion” number or rating.
Barriers to Trade (TBT) Committee.
3.3 The rating number assigned to the inspector’s judgment
2. Referenced Documents of the overall appearance of the panel, including all defects
2 caused by the exposure (Note 1), is called the “appearance”
2.1 ASTM Standards:
number or rating.
B117Practice for Operating Salt Spray (Fog) Apparatus
B287Method of Acetic Acid-Salt Spray (Fog) Testing
NOTE 1—Panels that are not “perfect” even before being exposed
should normally be rejected (see Note 4).
(Withdrawn 1987)
B368Test Method for Copper-AcceleratedAceticAcid-Salt
3.4 The result of inspecting a panel is recorded as two
numbers separated by a slash (/), the protection number being
given first.
This practice is under the jurisdiction of ASTM Committee B08 on Metallic
3.5 In addition to recording the numerical rating of a panel,
and Inorganic Coatings and is the direct responsibility of Subcommittee B08.05 on
the inspector should note the type(s) and severity of defect(s)
Decorative Coatings.
Current edition approved Oct. 1, 2019. Published October 2019. Originally
contributing to the rating. This may be done by the use of
approvedin1970.Lastpreviouseditionapprovedin2013asB537–70(2013).DOI:
agreed symbols for the most common defects (Appendix X1)
10.1520/B0537-70R19.
and abbreviations for degree or severity of these defects.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
Standards volume information, refer to the standard’s Document Summary page on
the ASTM website. Color reproductions of these photographs are available from ASTM Interna-
The last approved version of this historical standard is referenced on tional Headquarters. Order Adjunct No. ADJB0537. Original adjunct produced in
www.astm.org. 1987.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B537 − 70 (2019)
4. Types of Defects 6. Assignment of Protection Rating
4.1 “Protection” defects include crater rusting (Note 2), 6.1 The numerical rating system is based on the area
pinhole rusting, rust stain, blisters (Note 3), and any other covered by protection defects, by the following equation:
defects that involve basis metal corrosion.
R 5 3 2 2 logA (1)
~ !
NOTE 2—“Rusting” or “rust” as used in this document includes
where R=rating and A=percentage of the total area cov-
corrosion products of the substrate and is not confined to iron or steel: the
ered by defects. R is rounded off to the nearest whole number,
white corrosion products of zinc die castings and aluminum, for example,
leading to the tabulation given in Table 1.
are included in this term.
NOTE3—Blistersonplatedzincdiecastingusuallyconnotebasismetal
6.1.1 Strict application of the equation given in 6.1 would
corrosion;buttheinspector’sjudgmentmayberequiredtodecidewhether
lead to ratings greater than 10 for panels with extremely small
a blister does or does not arise at the substrate-coating interface.
defective areas. Rating 10, accordingly, is arbitrarily assigned
4.2 “Appearance” defects include, the addition to those
to a panel with no defects, and the equation operates at ratings
caused by basis metal corrosion, all defects that detract from
9 and below.
the appearance (that is, the commercial acceptability) of the
6.1.2 If desired, fractional ratings between 9 and 10 may be
panel. Typical are: surface pits, “crow’s feet,” crack patterns,
assigned to panels judged better than 9 but not perfect.
surface stain, and tarnish.
Fractional ratings below 9, although normally not especially
useful, may be assigned if desired.
4.3 Defects developing on exposure that reflect improper
preparationorplatingshouldbenotedbutnoattemptshouldbe
6.2 As an aid in judging the defective area, standards of
made to rate panels showing major amounts of such defects.
comparison, consisting of photographs of panels or of dot
Peeling of the coating from the substrate, or of one coat from
charts are made part of this practice. See Appendix X2. These
another, is the principal such defect.
photographs and charts are 10 by 15 cm (4 by 6 in.) to
facilitate comparison with the panel being inspected. The
5. Preparation for and Manner of Inspection
standardsrepresentasnearlyaspossiblethemaximumamount
NOTE4—Itmaybedesirabletoexposepanelsfortesteventhoughthey
of corrosion permissible for a given rating; there is a standard
are defective in certain respects before exposure. In that case, an
foreachrating1through9.Apanelworsethanthestandardfor
inspection should be made and recorded before the panels are exposed.
rating 1 would rate 0.
5.1 Panels may be inspected on the exposure racks or may
6.2.1 The types of corrosion defects normally encountered
be removed to a more suitable location if necessary. Lighting
differ according to the type of atmospheric exposure. Typical
during inspection should be as nearly uniform as possible;
decorative deposits exposed to marine atmospheres often tend
direct reflection from sun or clouds should be avoided, and
tofailbycraterrusting,whereasinindustrialatmospheres,they
various angles of inspection should be tried to ensure that
are more likely to exhibit pinpoint rusting; and the latter
defects show up.
atmosphere also tends to be more severe with regard to
5.2 If the condition of the panels allows, inspection should
degradation of the coating system but somewhat less severe
be made in the “as-is” condition. If dirt, salt deposits, and so
with regard to basis metal corrosion. For this reason, the same
forth, make it impractical to inspect them, panels may be
standard comparison photographs or charts are not suitable for
spongedwithamildsoapsolutionfollowedbywaterrinse;but
use at both types of locations; photographs are more helpful in
no pressure should be exerted in this procedure such as would
assessing panels exposed to marine atmospheres, whereas dot
tend to upgrade the rating by, for example, cleaning off rust or
charts can be used for industrial locations (Appendix X2).
rust stain. Panels should be allowed to dry before inspecting
6.3 In rating any given panel, it is recommended that the
them.
appropriateseriesofstandardsbeplacedbesideitandthebasis
5.3 Defects to be noted and taken into account in rating
metal corrosion defects in the panel be matched as nearly as
panelsincludeonlythosethatcanbeseenwiththeunaidedeye
possible with one of the standards. If the panel is somewhat
(Note 5) at normal reading distance.
better than standard (X) but not as good as standard (X+1)it
israted(X);ifsomewhatworsethanstandard(X)butnotasbad
NOTE 5—“Unaided eye” includes wearing of correctional glasses if the
inspector normally wears them.
5.3.1 Optical aids may be used to identify or study defects
once they are found by unaided eye inspection.
TABLE 1 Protection Rating Versus Area of Defect
5.4 Edge defects, occurring within 6.5 mm ( ⁄4 in.) of the
Area of Defect (in pe
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: B537 − 70 (Reapproved 2013) B537 − 70 (Reapproved 2019)
Standard Practice for
Rating of Electroplated Panels Subjected to
Atmospheric Exposure
This standard is issued under the fixed designation B537; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 This practice covers a preferred method for evaluating the condition of electroplated test panels that have been exposed to
corrosive environments for test purposes. It is based on experience in use of the method with standard 10- by 15-cm (4- by 6-in.)
panels exposed on standard ASTM racks at outdoor test sites in natural atmospheres. It has been used also for rating similar panels
that have been subjected to accelerated tests such as those covered by Practice B117, Method B287, Test Method B368, and Test
Method B380. Any modifications needed to adapt the method to rating actual production parts are not considered in this practice.
1.2 This practice refers only to decorative-protective coatings that are cathodic to the substrate, typified by nickel/chromium or
copper/nickel/chromium on steel or zinc die castings. It is not intended for use with anodic sacrificial coatings such as zinc and
cadmium on steel.
1.3 This international standard was developed in accordance with internationally recognized principles on standardization
established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued
by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
2. Referenced Documents
2.1 ASTM Standards:
B117 Practice for Operating Salt Spray (Fog) Apparatus
B287 Method of Acetic Acid-Salt Spray (Fog) Testing (Withdrawn 1987)
B368 Test Method for Copper-Accelerated Acetic Acid-Salt Spray (Fog) Testing (CASS Test)
B380 Test Method for Corrosion Testing of Decorative Electrodeposited Coatings by the Corrodkote Procedure
2.2 ASTM Adjunct:
Dot charts (9 charts, 8 ⁄2 by 11 in.) (9 color photos, 3 by 5 in.)
3. Basis of Procedure
3.1 The rating method described in this recommended practice is based on the recognition that typical decorative-protective
deposits such as nickel/chromium, with or without a copper undercoat, have two functions: (1) to protect the substrate from
corrosion and thus prevent degradation of appearance caused by basis metal corrosion products (for example, rust and rust stain);
and (2) to itself maintain a satisfactory appearance. Although these functions overlap, they can be evaluated separately, and it is
frequently desirable to do so. Accordingly, this practice assigns separate ratings to (1) appearance as affected by corrosion of the
substrate and (2) appearance as affected by deterioration of the coating itself.
3.2 The rating number assigned to the ability of the coating to protect the substrate from corrosion is called the “protection”
number or rating.
3.3 The rating number assigned to the inspector’s judgment of the overall appearance of the panel, including all defects caused
by the exposure (Note 1), is called the “appearance” number or rating.
This practice is under the jurisdiction of ASTM Committee B08 on Metallic and Inorganic Coatings and is the direct responsibility of Subcommittee B08.05 on Decorative
Coatings.
Current edition approved Dec. 1, 2013Oct. 1, 2019. Published December 2013October 2019. Originally approved in 1970. Last previous edition approved in 20072013
as B537 – 70 (2007).(2013). DOI: 10.1520/B0537-70R13.10.1520/B0537-70R19.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
The last approved version of this historical standard is referenced on www.astm.org.
Color reproductions of these photographs are available from ASTM International Headquarters. Order Adjunct No. ADJB0537. Original adjunct produced in 1987.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
B537 − 70 (2019)
NOTE 1—Panels that are not “perfect” even before being exposed should normally be rejected (see Note 4).
3.4 The result of inspecting a panel is recorded as two numbers separated by a slash (/), the protection number being given first.
3.5 In addition to recording the numerical rating of a panel, the inspector should note the type(s) and severity of defect(s)
contributing to the rating. This may be done by the use of agreed symbols for the most common defects (Appendix X1) and
abbreviations for degree or severity of these defects.
4. Types of Defects
4.1 “Protection” defects include crater rusting (Note 2), pinhole rusting, rust stain, blisters (Note 3), and any other defects that
involve basis metal corrosion.
NOTE 2—“Rusting” or “rust” as used in this document includes corrosion products of the substrate and is not confined to iron or steel: the white
corrosion products of zinc die castings and aluminum, for example, are included in this term.
NOTE 3—Blisters on plated zinc die casting usually connote basis metal corrosion; but the inspector’s judgment may be required to decide whether
a blister does or does not arise at the substrate-coating interface.
4.2 “Appearance” defects include, the addition to those caused by basis metal corrosion, all defects that detract from the
appearance (that is, the commercial acceptability) of the panel. Typical are: surface pits, “crow’s feet,” crack patterns, surface stain,
and tarnish.
4.3 Defects developing on exposure that reflect improper preparation or plating should be noted but no attempt should be made
to rate panels showing major amounts of such defects. Peeling of the coating from the substrate, or of one coat from another, is
the principal such defect.
5. Preparation for and Manner of Inspection
NOTE 4—It may be desirable to expose panels for test even though they are defective in certain respects before exposure. In that case, an inspection
should be made and recorded before the panels are exposed.
5.1 Panels may be inspected on the exposure racks or may be removed to a more suitable location if necessary. Lighting during
inspection should be as nearly uniform as possible; direct reflection from sun or clouds should be avoided, and various angles of
inspection should be tried to ensure that defects show up.
5.2 If the condition of the panels allows, inspection should be made in the “as-is” condition. If dirt, salt deposits, and so forth,
make it impractical to inspect them, panels may be sponged with a mild soap solution followed by water rinse; but no pressure
should be exerted in this procedure such as would tend to upgrade the rating by, for example, cleaning off rust or rust stain. Panels
should be allowed to dry before inspecting them.
5.3 Defects to be noted and taken into account in rating panels include only those that can be seen with the unaided eye (Note
5) at normal reading distance.
NOTE 5—“Unaided eye” includes wearing of correctional glasses if the inspector normally wears them.
5.3.1 Optical aids may be used to identify or study defects once they are found by unaided eye inspection.
5.4 Edge defects, occurring within 6.5 mm ( ⁄4 in.) of the edges of a panel, may be noted in the description but are not counted
in arriving at the numerical rating. Similarly contact and rack marks, mounting holes, and so forth, should be disregarded.
5.5 Rubbing, polishing, and so forth, of the surface of the panel may be desirable to study one or another aspect of its condition.
Such procedure shall be confined to the minimum area absolutely necessary for the purpose, preferably not more than 1 cm of
a 10- by 15-cm panel.
6. Assignment of Protection Rating
6.1 The numerical rating system is based on the area covered by protection defects, by the following equation:
R 5 3 22 logA (1)
~ !
where R = rating and A = percentage of the total area covered by defects. R is rounded off to the nearest whole number, leading
to the tabulation given in Table 1.
6.1.1 Strict application of the equation given in 6.1 would lead to ratings greater than 10 for panels with extremely small
defective areas. Rating 10, accordingly, is arbitrarily assigned to a panel with no defects, and the equation operates at ratings 9 and
below.
6.1.2 If desired, fractional ratings between 9 and 10 may be assigned to panels judged better than 9 but not perfect. Fractional
ratings below 9, although normally not especially useful, may be assigned if desired.
6.2 As an aid in judging the defective area, standards of comparison, consisting of photographs of panels or of dot charts are
made part of this practice. See Appendix X2. These photographs and charts are 10 by 15 cm (4 by 6 in.) to facilitate comparison
with the panel being inspected. The standards represent as nearly as possible the maximum amount of corrosion permissible for
a given rating; there is a standard for each rating 1 through 9. A panel worse than the standard for rating 1 would rate 0.
B537 − 70 (2019)
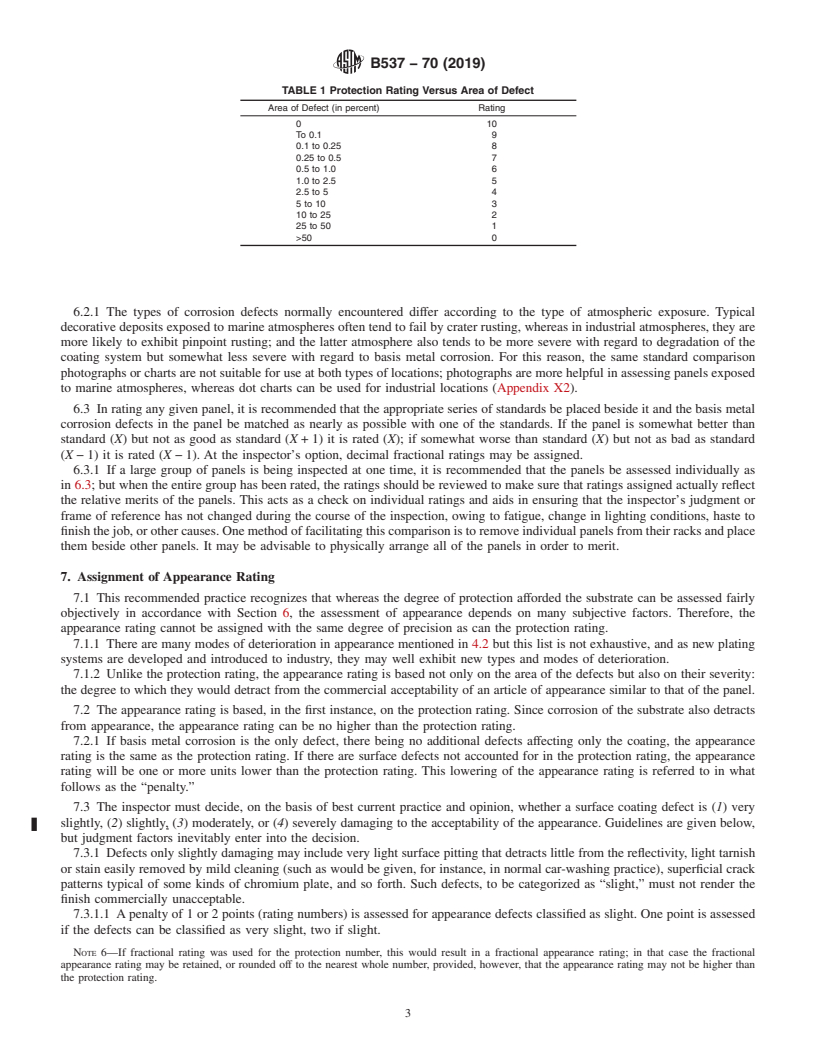
TABLE 1 Protection Rating Versus Area of Defect
Area of Defect (in percent) Rating
0 10
To 0.1 9
0.1 to 0.25 8
0.25 to 0.5 7
0.5 to 1.0 6
1.0 to 2.5 5
2.5 to 5 4
5 to 10 3
10 to 25 2
25 to 50 1
>50 0
6.2.1 The types of corrosion defects normally encountered differ according to the type of atmospheric exposure. Typical
decorative deposits exposed to marine atmospheres often tend to fail by crater rusting, whereas in industrial atmosp
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.