

ASTM F1817-17(2022)
(Test Method)Standard Test Method for Performance of Conveyor Ovens
General Information
- Abstract
SIGNIFICANCE AND USE
5.1 The energy input rate test and thermostat calibration are used to confirm that the conveyor oven is operating properly prior to further testing and to insure that all test results are determined at the same temperature.
5.2 Preheat energy and time can be useful to food service operators to manage power demands and to know how quickly the conveyor oven can be ready for operation.
5.3 Idle Energy Rate—This test provides a measure of an empty oven’s energy consumption and pilot energy during noncooking periods, at a typical cooking temperature setting. It also provides an indicator of the combined effectiveness of components of the oven’s design (for example, insulation, door seals, and combustion efficiency) that influence its energy consumption.
5.4 Cooking Energy Efficiency—A precise indicator of conveyor oven energy performance while cooking a typical food product under various loading conditions. If energy performance information is desired using a food product other than the specified test food, the test method could be adapted and applied. Energy performance information allows an end user to better understand the operating characteristics of a conveyor oven.
5.5 Production capacity information can help an end user to better understand the production capabilities of a conveyor oven as it is used to cook a typical food product and this could help in specifying the proper size and quantity of equipment. If production information is desired using a food product other than the specified test food, the test method could be adapted and applied.
SCOPE
1.1 This test method covers an evaluation of the energy consumption and cooking performance of conveyor ovens. The food service operator can use this evaluation to select a conveyor oven and understand its energy consumption.
1.2 This test method is applicable to gas and electric conveyor ovens.
1.3 The conveyor oven can be evaluated with respect to the following (where applicable):
1.3.1 Energy input rate and thermostat calibration (see 10.2),
1.3.2 Preheat energy consumption and time (see 10.3),
1.3.3 Idle energy rate (see 10.4),
1.3.4 Pilot energy rate (if applicable) (see 10.5), and
1.3.5 Cooking energy efficiency and production capacity (see 10.6).
1.4 The values stated in inch-pound units are to be regarded as standard. No other units of measurement are included in this standard.
1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use.
1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
- Status
- Published
- Publication Date
- 30-Apr-2022
- Technical Committee
- F26 - Food Service Equipment
- Drafting Committee
- F26.06 - Productivity and Energy Protocol
Overview
ASTM F1817-17(2022), "Standard Test Method for Performance of Conveyor Ovens", is a widely recognized standard developed by ASTM International. This test method specifies procedures to evaluate the energy consumption and cooking performance of gas and electric conveyor ovens, commonly used in commercial foodservice operations. By providing objective metrics for factors such as energy input, preheat energy and time, idle energy rate, cooking efficiency, and production capacity, this standard enables food service operators and equipment manufacturers to assess, compare, and optimize the performance of conveyor ovens.
Key Topics
Energy Input Rate & Thermostat Calibration
- Validates that the conveyor oven is functioning correctly before further tests.
- Ensures uniform test conditions and temperature accuracy.
Preheat Energy and Time
- Establishes how much energy and time are required to bring a cold oven to operational temperature.
- Helps operators plan for efficient kitchen startup and manage energy demand.
Idle Energy Rate
- Measures energy consumption when the oven is maintaining temperature, but not actively cooking.
- Indicates design efficiency, highlighting the effectiveness of insulation, door seals, and combustion systems.
Cooking Energy Efficiency
- Calculates the ratio of energy imparted to the food relative to the total energy consumed during cooking.
- Provides crucial data for comparing oven models and for operational cost estimations.
Production Capacity
- Determines how much food can be cooked within a given period.
- Aids in specifying the appropriate oven size and capacity for different food service requirements.
Applications
The ASTM F1817-17(2022) test method is highly beneficial across the commercial food service sector:
Equipment Selection and Specification
- Enables food service operators, kitchen designers, and consultants to choose energy-efficient conveyor ovens suited to specific production needs.
Operational Cost Management
- By revealing energy use in both cooking and idle states, operators can optimize usage patterns to reduce energy bills and improve sustainability.
Performance Benchmarking
- Manufacturers can use standard test data to benchmark new ovens, support marketing claims, and meet procurement requirements set by large chains or institutions.
Regulatory and Procurement Compliance
- Provides standardized criteria that help organizations comply with energy efficiency regulations and institutional purchasing standards.
Related Standards
For comprehensive assessment and comparison, ASTM F1817-17(2022) is often used alongside related standards and industry references, such as:
ASHRAE Handbook Chapters
- Thermal Conductivity, Diffusivity, and Enthalpy of Foods for accurate food thermal property data during testing.
AOAC Procedure 984.25
- For gravimetric moisture analysis in food products, ensuring accurate test food preparation.
ASHRAE Guideline 2
- For engineering analysis of experimental data and test result validation.
Practical Value
Using ASTM F1817-17(2022) ensures standardized, repeatable, and transparent testing of conveyor oven performance. This supports informed purchasing, operational efficiency, and sustainability goals for food service businesses, while giving manufacturers a respected benchmark for innovation and performance claims. By specifying clear measurement and reporting procedures, the standard fosters greater energy savings and performance optimization throughout the foodservice industry.
Keywords: ASTM F1817-17(2022), conveyor oven performance, energy efficiency, test method, food service equipment standards, cooking energy consumption, oven production capacity, kitchen energy management
Frequently Asked Questions
ASTM F1817-17(2022) is a standard published by ASTM International. Its full title is "Standard Test Method for Performance of Conveyor Ovens". This standard covers: SIGNIFICANCE AND USE 5.1 The energy input rate test and thermostat calibration are used to confirm that the conveyor oven is operating properly prior to further testing and to insure that all test results are determined at the same temperature. 5.2 Preheat energy and time can be useful to food service operators to manage power demands and to know how quickly the conveyor oven can be ready for operation. 5.3 Idle Energy Rate—This test provides a measure of an empty oven’s energy consumption and pilot energy during noncooking periods, at a typical cooking temperature setting. It also provides an indicator of the combined effectiveness of components of the oven’s design (for example, insulation, door seals, and combustion efficiency) that influence its energy consumption. 5.4 Cooking Energy Efficiency—A precise indicator of conveyor oven energy performance while cooking a typical food product under various loading conditions. If energy performance information is desired using a food product other than the specified test food, the test method could be adapted and applied. Energy performance information allows an end user to better understand the operating characteristics of a conveyor oven. 5.5 Production capacity information can help an end user to better understand the production capabilities of a conveyor oven as it is used to cook a typical food product and this could help in specifying the proper size and quantity of equipment. If production information is desired using a food product other than the specified test food, the test method could be adapted and applied. SCOPE 1.1 This test method covers an evaluation of the energy consumption and cooking performance of conveyor ovens. The food service operator can use this evaluation to select a conveyor oven and understand its energy consumption. 1.2 This test method is applicable to gas and electric conveyor ovens. 1.3 The conveyor oven can be evaluated with respect to the following (where applicable): 1.3.1 Energy input rate and thermostat calibration (see 10.2), 1.3.2 Preheat energy consumption and time (see 10.3), 1.3.3 Idle energy rate (see 10.4), 1.3.4 Pilot energy rate (if applicable) (see 10.5), and 1.3.5 Cooking energy efficiency and production capacity (see 10.6). 1.4 The values stated in inch-pound units are to be regarded as standard. No other units of measurement are included in this standard. 1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use. 1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
SIGNIFICANCE AND USE 5.1 The energy input rate test and thermostat calibration are used to confirm that the conveyor oven is operating properly prior to further testing and to insure that all test results are determined at the same temperature. 5.2 Preheat energy and time can be useful to food service operators to manage power demands and to know how quickly the conveyor oven can be ready for operation. 5.3 Idle Energy Rate—This test provides a measure of an empty oven’s energy consumption and pilot energy during noncooking periods, at a typical cooking temperature setting. It also provides an indicator of the combined effectiveness of components of the oven’s design (for example, insulation, door seals, and combustion efficiency) that influence its energy consumption. 5.4 Cooking Energy Efficiency—A precise indicator of conveyor oven energy performance while cooking a typical food product under various loading conditions. If energy performance information is desired using a food product other than the specified test food, the test method could be adapted and applied. Energy performance information allows an end user to better understand the operating characteristics of a conveyor oven. 5.5 Production capacity information can help an end user to better understand the production capabilities of a conveyor oven as it is used to cook a typical food product and this could help in specifying the proper size and quantity of equipment. If production information is desired using a food product other than the specified test food, the test method could be adapted and applied. SCOPE 1.1 This test method covers an evaluation of the energy consumption and cooking performance of conveyor ovens. The food service operator can use this evaluation to select a conveyor oven and understand its energy consumption. 1.2 This test method is applicable to gas and electric conveyor ovens. 1.3 The conveyor oven can be evaluated with respect to the following (where applicable): 1.3.1 Energy input rate and thermostat calibration (see 10.2), 1.3.2 Preheat energy consumption and time (see 10.3), 1.3.3 Idle energy rate (see 10.4), 1.3.4 Pilot energy rate (if applicable) (see 10.5), and 1.3.5 Cooking energy efficiency and production capacity (see 10.6). 1.4 The values stated in inch-pound units are to be regarded as standard. No other units of measurement are included in this standard. 1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use. 1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
ASTM F1817-17(2022) is classified under the following ICS (International Classification for Standards) categories: 97.040.20 - Cooking ranges, working tables, ovens and similar appliances. The ICS classification helps identify the subject area and facilitates finding related standards.
ASTM F1817-17(2022) is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the
Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
Designation: F1817 − 17 (Reapproved 2022) An American National Standard
Standard Test Method for
Performance of Conveyor Ovens
This standard is issued under the fixed designation F1817; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope 2. Referenced Documents
1.1 This test method covers an evaluation of the energy 2.1 ASHRAE Documents:
consumptionandcookingperformanceofconveyorovens.The 2013ASHRAE Handbook of FundamentalsChapter 1, Psy-
chrometrics
food service operator can use this evaluation to select a
2014ASHRAE Handbook—Refrigeration Chapter 19Ther-
conveyor oven and understand its energy consumption.
mal Conductivity of Foods, page 9 (R19.9); Diffusivity of
1.2 This test method is applicable to gas and electric
foods, R19.17, and Enthalpy of foods R19.8
conveyor ovens.
ASHRAE Guideline 2-1986 (RA90)Engineering Analysis
of Experimental Data
1.3 The conveyor oven can be evaluated with respect to the
ASHRAE Guideline 2 2010 (RA 2014)Engineering Analy-
following (where applicable):
sis of Experimental Data
1.3.1 Energy input rate and thermostat calibration (see
2.2 Other Document:
10.2),
AOAC Procedure 984.25Moisture (Loss of Mass on Dry-
1.3.2 Preheat energy consumption and time (see 10.3), 3
ing) in Frozen French Fried Potatoes
1.3.3 Idle energy rate (see 10.4),
3. Terminology
1.3.4 Pilot energy rate (if applicable) (see 10.5), and
1.3.5 Cooking energy efficiency and production capacity 3.1 Definitions of Terms Specific to This Standard:
3.1.1 chamber stabilization pizzas, n—full cooking cavity
(see 10.6).
loadofnominal12in.pizzasloadedatbeginningofproduction
1.4 The values stated in inch-pound units are to be regarded
capacity test.
asstandard.Nootherunitsofmeasurementareincludedinthis
3.1.2 conveyor oven, n—an appliance that carries the food
standard.
product on a moving conveyor into and through a heated
1.5 This test method may involve hazardous materials,
chamber.The chamber may be heated by gas or electric forced
operations, and equipment. This standard does not purport to convection, radiant, or quartz tubes. Top and bottom heat may
be independently controlled.
address all of the safety concerns, if any, associated with its
use. It is the responsibility of the user of this standard to
3.1.3 cooking energy effıciency, n—quantity of energy im-
establish appropriate safety, health, and environmental prac-
parted to the specified food product, expressed as a percentage
tices and determine the applicability of regulatory limitations of energy consumed by the conveyor oven during the cooking
event.
prior to use.
1.6 This international standard was developed in accor- 3.1.4 cooking energy rate, n—average rate of energy con-
sumption (Btu/h or kW) during the cooking energy efficiency
dance with internationally recognized principles on standard-
tests.
ization established in the Decision on Principles for the
Development of International Standards, Guides and Recom-
3.1.5 cooking stabilization pizzas, n—full cooking chamber
mendations issued by the World Trade Organization Technical
ofnominal12in.pizzascontinuouslyloadeddirectlyfollowing
Barriers to Trade (TBT) Committee.
the test pizzas. Pizzas keep the cooking chamber consistent
during the measured test pizzas.
This test method is under the jurisdiction of ASTM Committee F26 on Food
Service Equipment and is the direct responsibility of Subcommittee F26.06 on Available from American Society of Heating, Refrigerating, and Air-
Productivity and Energy Protocol. Conditioning Engineers, Inc. (ASHRAE), 1791 Tullie Circle, NE, Atlanta, GA
Current edition approved May 1, 2022. Published June 2022. Originally 30329.
approved in 1997. Last previous edition approved in 2017 as F1817–17. DOI: Available from AOAC International, 2275 Research Blvd., Suite 300,
10.1520/F1817-17R22. Rockville, MD 20850-3250, http://www.aoac.org.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
F1817 − 17 (2022)
3.1.6 energy input rate, n—peak rate at which a conveyor 4.6 Cooking Uniformity—The uniformity of heating within
oven consumes energy (Btu/h or kW). the oven’s cavity is determined and reported based on the
product cooked temperature per cooking position and visual of
3.1.7 idle energy rate, n—the conveyor oven’s rate of
product appearance top and bottom.
energy consumption (kW or Btu/h), when empty, required to
maintain its cavity temperature at the specified thermostat set
5. Significance and Use
point.
5.1 The energy input rate test and thermostat calibration are
3.1.8 oven cavity, n—that portion of the conveyor oven in
used to confirm that the conveyor oven is operating properly
which food products are heated or cooked.
prior to further testing and to insure that all test results are
determined at the same temperature.
3.1.9 pilot energy rate, n—rate of energy consumption
(Btu/h) by a conveyor oven’s continuous pilot (if applicable).
5.2 Preheat energy and time can be useful to food service
operators to manage power demands and to know how quickly
3.1.10 preheat energy, n—amount of energy consumed (Btu
the conveyor oven can be ready for operation.
or kWh), by the conveyor oven while preheating its cavity
fromambienttemperaturetothespecifiedthermostatsetpoint.
5.3 Idle Energy Rate—This test provides a measure of an
empty oven’s energy consumption and pilot energy during
3.1.11 preheat time, n—time (min.) required for the con-
noncookingperiods,atatypicalcookingtemperaturesetting.It
veyor oven cavity to preheat from ambient temperature to the
also provides an indicator of the combined effectiveness of
specified thermostat set point.
componentsoftheoven’sdesign(forexample,insulation,door
3.1.12 production capacity, n—maximum rate (lb/h) at
seals, and combustion efficiency) that influence its energy
which a conveyor oven can bring the specified food product to
consumption.
a specified “cooked” condition.
5.4 Cooking Energy Effıciency—Aprecise indicator of con-
3.1.13 production rate, n—rate (lb/h) at which a conveyor
veyor oven energy performance while cooking a typical food
oven brings the specified food product to a specified“ cooked”
product under various loading conditions. If energy perfor-
condition. Does not necessarily refer to maximum rate. Pro-
mance information is desired using a food product other than
duction rate varies with the amount of food being cooked.
the specified test food, the test method could be adapted and
3.1.14 test pizzas, n—full cooking chamber of nominal 12
applied.Energyperformanceinformationallowsanenduserto
in. pizzas continuously loaded directly following the stabiliza-
better understand the operating characteristics of a conveyor
tion load. These are the pizzas measured for production
oven.
capacity.
5.5 Production capacity information can help an end user to
3.1.15 uncertainty, n—measure of systematic and precision
better understand the production capabilities of a conveyor
errors in specified instrumentation or measure of repeatability
oven as it is used to cook a typical food product and this could
of a reported test result.
helpinspecifyingthepropersizeandquantityofequipment.If
production information is desired using a food product other
4. Summary of Test Method
than the specified test food, the test method could be adapted
and applied.
4.1 Accuracyoftheconveyoroventhermostatischeckedat
a setting of 475°F (246°C) and the thermostat is adjusted as
6. Apparatus
necessary.
6.1 Analytical Balance Scale, for measuring weights up to
4.2 Energy Input Rate—Determined to confirm that the
20 lb (9.1 kg), with a resolution of 0.01 lb (0.005 kg) and an
conveyorovenisoperatingwithin5%ofthenameplateenergy
uncertainty of 60.01 lb (60.005 kg).
inputrate.Forgasconveyoroven,thepilotenergyrateandthe
6.2 Barometer, for measuring absolute atmospheric
fanandcontrolenergyratesarealsodetermined.Theinputrate
pressure, with a range from 28 to 32 in. to be used for
of the oven is determined to check whether the oven is
adjustment of measured natural gas volume to standard condi-
operatingproperly.Ifthemeasuredinputrateisnotwithin5%
tions. Shall have a resolution of 0.2 in. Hg and an uncertainty
of the rated input, all further testing ceases until the appliance
of 60.2 in. Hg.
canbemadetooperatewithinthisspecification.Forgasovens,
6.3 Canopy Exhaust Hood, 4 ft (1.2 m) in depth, wall-
thepilotenergyrateandthefanandcontrolenergyratearealso
mounted with the lower edge of the hood 6 ft , 6 in. (1.98 m)
determined.
from the floor and with the capacity to operate at a nominal
4.3 Preheat Energy Consumption and Time—The time and
exhaust ventilation rate of 300 cfm per linear foot of active
energy required to preheat the oven from room temperature 75
hood length. This hood shall extend a minimum of 6 in. (152
6 5°F (24 6 2.8°C) to 475 6 5°F (246 6 2.8°C) determined.
mm)pastbothsidesandthefrontofthecookingapplianceand
4.4 Idle Energy Rate—The idle energy rate (kBtu/h or kW)
shall not incorporate side curtains or partitions. Makeup air
is determined with the oven set to maintain 475 6 5°F (246 6
shall be delivered through face registers or from the space, or
2.8°C).
both.
4.5 Cooking energy efficiency and production rate are 6.4 ConvectionDryingOven,withtemperaturecontrolledat
determined during heavy-load cooking tests using pizza as a 220 6 5°F (104 6 –2.8°C), to be used to determine moisture
food product. content of pizza crust, pizza sauce and pizza cheese.
F1817 − 17 (2022)
6.5 Gas Meter, for measuring the gas consumption of a 6.11 Temperature Readout Device, connected to bare junc-
conveyor oven, shall be a positive displacement type with a tionthermocoupleprobes,witharangefrom0to450°F(−17.8
resolution of at least 0.01 ft and a maximum uncertainty no
to232°C),aresolutionof0.1°F(0.06°C),andanuncertaintyof
greaterthan1%ofthemeasuredvalueforanydemandgreater
61.0°F (60.6°C), used to measure the temperature of air
than 2.2 ft /h. If the meter is used for measuring the gas
(ambient and cavity), and ice/water mixture. The device
consumed by the pilot lights, it shall have a resolution of at
readout shall be capable of displaying required average tem-
least 0.01 ft and a maximum uncertainty no greater than 2%
perature(s) during cooking energy efficiency and cooking
of the measured value.
uniformity tests (minimum of 20 thermocouples needed).
6.6 Pressure Gage, for monitoring natural gas pressure.
6.12 Watt-Hour Meter, for measuring the electrical energy
Shall have a range of 0 to 15 in. H O, a resolution of 0.2 in.
consumption of a conveyor oven, shall have a resolution of at
H O, and an uncertainty of 60.1in. H O.
2 2
least 10Wh and a maximum uncertainty no greater than 1.5%
6.7 Stop Watch, with a 1-s resolution.
of the measured value for any demand greater than 100W. For
6.8 Temperature Sensor, for measuring natural gas tempera- any demand less than 100 W, the meter shall have a resolution
ture in the range of 50 to 100°F with an uncertainty of 61°F .
of at least 10 Wh and a maximum uncertainty no greater than
10%.
6.9 Thermocouple, fiberglass insulated, 24 gage, Type K
thermocouple wire, connected at the exposed ends by tightly
6.13 Pizza Cooking Screens, for handling and cooking
twisting or soldering the two wires together.
pizzas, 12 in. diameter aluminum (3003-H14 material) ex-
6.10 Thermocouple Probe, type K, micro needle, product
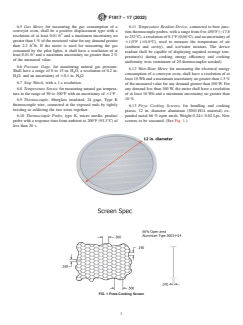
panded metal 66 % open mesh. Weight 0.246 0.02 Lps. New
probe with a response time from ambient to 200°F (93.3°C) of
screens to be seasoned. (See Fig. 1.)
less than 20 s.
FIG. 1 Pizza Cooking Screen
F1817 − 17 (2022)
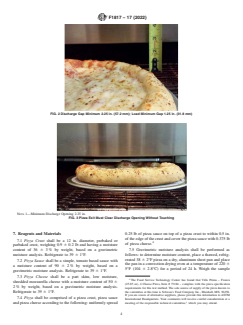
FIG. 2 Discharge Gap Minimum 2.25 in. (57.2 mm); Load Minimum Gap 1.25 in. (31.8 mm)
NOTE 1—Minimum Discharge Opening 2.25 in.
FIG. 3 Pizza Exit Must Clear Discharge Opening Without Touching
7. Reagents and Materials 0.25 lb of pizza sauce on top of a pizza crust to within 0.5 in.
oftheedgeofthecrustandcoverthepizzasaucewith0.375lb
7.1 Pizza Crust shall be a 12 in. diameter, prebaked or
of pizza cheese.
parbaked crust, weighing 0.9 6 0.2 lb and having a moisture
content of 36 6 3% by weight, based on a gravimetric 7.5 Gravimetric moisture analysis shall be performed as
moisture analysis. Refrigerate to 39 6 1°F. follows: to determine moisture content, place a thawed, refrig-
erated 38 6 2°F pizza on a dry, aluminum sheet pan and place
7.2 Pizza Sauce shall be a simple, tomato based sauce with
the pan in a convection drying oven at a temperature of 220 6
a moisture content of 90 6 2% by weight, based on a
5°F (104 6 2.8°C) for a period of 24 h. Weigh the sample
gravimetric moisture analysis. Refrigerate to 39 6 1°F.
7.3 Pizza Cheese shall be a part skim, low moisture,
The Food Service Technology Center has found that Villa Prima – Frozen
shredded mozzarella cheese with a moisture content of 50 6
(25.85 oz), 4 Cheese Pizza, Item # 73184 – complies with the pizza specification
2% by weight, based on a gravimetric moisture analysis.
requirements for this test method. The sole source of supply of the pizza known to
Refrigerate to 39 6 1°F. the committee at this time is Schwan’s Food Company Inc., Marshall, MN, 56258.
If you are aware of alternative suppliers, please provide this information toASTM
7.4 Pizza shall be comprised of a pizza crust, pizza sauce
International Headquarters. Your comments will receive careful consideration at a
and pizza cheese according to the following: uniformly spread meeting of the responsible technical committee, which you may attend.
F1817 − 17 (2022)
separate appliances in accordance with this test method.
before it is placed in the oven and after it is removed and
determine the percent moisture content based on the percent
9.4 For a gas conveyor oven, adjust (during maximum
weight loss of the sample. The sample must be thoroughly
energy input) the gas supply pressure downstream from the
chopped ( ⁄8 in. or smaller squares) and spread evenly over the
appliance’s pressure regulator to within 62.5% of the operat-
surface of the sheet pan in order for all of the moisture to
ing manifold pressure specified by the manufacturer. Make
evaporate during drying and it is permissible to spread the
adjustments to the appliance following the manufacturer’s
sample on top of baking paper in order to protect the sheet pan
recommendations for optimizing combustion.
and simplify cleanup.
10. Procedure
NOTE 1—The moisture content of pizza crust, pizza sauce, and pizza
cheese can be determined by a qualified chemistry lab using the AOAC
10.1 General:
Procedure 984.25 Moisture (Loss of Mass on Drying) in Frozen French
10.1.1 Forgasappliances,recordthefollowingforeachtest
Fried Potatoes.
run:
10.1.1.1 Higher heating value,
8. Sampling, Test Units
10.1.1.2 Standard gas pressure and temperature used to
8.1 Conveyor Oven—Select a representative production
correct measured gas volume to standard conditions,
model for performance testing.
10.1.1.3 Measured gas temperature,
10.1.1.4 Measured gas pressure,
9. Preparation of Apparatus
10.1.1.5 Barometric pressure,
10.1.1.6 Energy input rate during or immediately prior to
9.1 Install the appliance according to the manufacturer’s
test (for example, during the preheat for that days testing), and
instructions under a canopy exhaust hood. Position the con-
veyorovensothataminimumof6in.(152mm)ismaintained 10.1.1.7 Ambient temperature.
betweentheedgeofthehoodandtheverticalplaneofthefront
NOTE 4—Using a calorimeter or gas chromatograph in accordance with
and sides of the appliance. In addition, both sides of the
accepted laboratory procedures is the preferred method for determining
conveyor oven shall be a minimum of 3 ft (0.91 m) from any the higher heating value of gas supplied to the conveyor oven under test.
It is recommended that all testing be performed with gas having a higher
side wall, side partition, or other operating appliance. The
heating value of 1000 to 1075 Btu/ft .
exhaust ventilation rate shall be 300 cfm per linear foot of
10.1.2 For gas conveyor ovens, add electric energy con-
active hood length. The associated heating or cooling system
sumption to gas energy for all tests, with the exception of the
shall be capable of maintaining an ambient temperature of 75
energy input rate test (see 10.3).
6 5°F (24 6 2.8°C) within the testing environment when the
10.1.3 Forelectricconveyorovens,recordthefollowingfor
exhaust ventilation system is operating.
each test run:
9.1.1 Oven openings are to be set to minimum clearance
10.1.3.1 Voltage while elements are energized,
openingsforproductentryandcookeddischargeend.Theload
10.1.3.2 Energy input rate during or immediately prior to
opening minimum 1.25 in. (31.8 mm). Discharged cooked
test (for example, during the preheat for that days testing), and
minimum clearance of 2.25 in. (57.2 mm). See Fig. 2 and Fig.
10.1.3.3 Ambient temperature.
3.
10.1.4 For each test run, confirm that the peak input rate is
NOTE 2—The ambient temperature requirements are designed to simu-
within 65% of the rated nameplate input. If the difference is
laterealworldkitchentemperaturesandaremeanttoprovideareasonable
greater than 5%, terminate testing and contact the manufac-
guideline for the temperature requirements during testing. If a facility is
not able to maintain the required temperatures, then it is reasonable to turer. The manufacturer may make appropriate changes or
expectthattheapplicationoftheproceduremaydeviatefromthespecified
adjustments to the conveyor oven.
requirements(ifitcannotbeavoided)aslongasthosedeviationsarenoted
10.2 Energy Input Rate and Thermostat Calibration:
on the Results Reporting Sheets.
10.2.1 Install a thermocouple 2 in. above the conveyor, at
9.2 Connect the conveyor oven to a calibrated energy test
the center of the oven cavity (side to side and front to back).
meter. For gas installations, install a pressure regulator down-
10.2.2 Set the temperature control to 475°F (246°C) and
stream from the meter to maintain a constant pressure of gas
turn the conveyor oven on. Record the time and energy
for all tests. Install instrumentation to record both the pressure
consumption from the time when the unit is turned on until the
and temperature of the gas supplied to the conveyor oven and
time when any of the burners or elements first cycle off.
the barometric pressure during each test so that the measured
10.2.3 Calculate and record the conveyor oven’s energy
gas flow can be corrected to standard conditions. For electric
input rate and compare the result to the rated nameplate input.
installations,avoltageregulatormayberequiredduringtestsif
Forgasconveyorovens,onlytheburnerenergyconsumptionis
the voltage supply is not within 62.5% of the manufacturer’s
used to compare the calculated energy input rate with the rated
nameplate voltage.
gas input; any electrical energy use shall be calculated and
9.3 For an electric conveyor oven, confirm (while the
recorded separately as the fan/control energy rate.
conveyor oven elements are energized) that the supply voltage
10.2.4 Allow the conveyor oven to idle for 60 min after the
is within 62.5% of the operating voltage specified by the
burners or elements commence cycling at the thermostat set
manufacturer. Record the test voltage for each test.
point.
10.2.5 After the 60 min idle period, start monitoring the
NOTE 3—If an electric conveyor oven is rated for dual voltage (for
example, 208/240 V), the conveyor oven shall be evaluated as two conveyor oven cavity temperature and record the average
F1817 − 17 (2022)
temperature over a 30 min period. If this recorded temperature 10.4.3 At the end of 60 min, begin recording the conveyor
is 475 6 5°F (246 6 2.8°C), then the conveyor oven’s oven’s idle energy consumption, at 475°F (246°C), for a
thermostat is calibrated. minimum of 2 h. Record the length of the idle period.
10.2.6 If the average temperature is not 475 6 5°F (246 6
10.4.4 In accordance with 11.6, calculate and report the
2.8°C),adjusttheconveyoroven’stemperaturecontrolfollow-
conveyor oven’s idle energy rate.
ing the manufacturer’s instructions and repeat 10.2.5 until it is
10.5 Pilot Energy Rate:
within this range. Record the corrections made to the controls
10.5.1 Foragasconveyorovenwithastandingpilot,setthe
during calibration.
gas valve at the “pilot” position and set the conveyor oven’s
10.2.7 In accordance with 11.4, calculate and report the
temperature control to the “off” position.
conveyorovenenergyinputrate,fan/controlenergyratewhere
10.5.2 Light and adjust the pilot according to the manufac-
applicable, and rated nameplate input.
turer’s instructions.
10.3 Preheat Energy Consumption and Time:
10.5.3 Monitor gas consumption for a minimum of8hof
10.3.1 Verify that the conveyor oven cavity temperature is
pilot operation.
75 6 5°F (24 6 2.8°C). Set the calibrated temperature control
10.5.4 In accordance with 11.7, calculate and report the
to 475°F (246°C) and turn the conveyor oven on.
pilot energy rate.
10.3.2 Record the time, temperature and energy consump-
10.6 Pizza Preparation:
tionrequiredtopreheattheconveyoroven,fromthetimewhen
the unit is turned on until the time when the conveyor oven 10.6.1 Prepare enough pizzas for a minimum of three runs
each of the heavy-load pizza tests. The number of pizzas for
cavity reaches a temperature of 465°F (241°C). Recording
should occur at intervals of 5 seconds or less in order to each test is determined by the size of the oven to be tested.
Measure the width of the oven conveyor and the length of the
accurately document the temperature rise of the oven cavity.
oven cavity to determine the nominal number of pizzas that
NOTE 5—Research at PG&E’s Food Service Technology Center indi-
will fit within the oven chamber at one time. Pizzas should be
cates that a conveyor oven is sufficiently preheated and ready to cook
placed atop the approximate center of the pizza screens, to
whentheovencavitytemperatureiswithin10°F(65.6°C)oftheovenset
point(thatis,465°F(241°C)whenthethermostatissettomaintain475°F facilitate ease of handling and loading during tests.
(246°C)).
10.6.1.1 For the heavy-load tests, the number of pizzas per
10.3.3 In accordance with 11.5, calculate and report the test is determined by the number of 12-in. pizzas that can be
preheat energy consumption and time and generate a preheat accommodated within the oven cavity at one time. Each run
temperature-versus-time graph. will require an equivalent of four cavity-loads of pizzas. The
pizzas will be loaded at an angle between 0 and 45°, to
10.4 Idle Energy Rate:
maximize belt coverage (see Fig. 4). Table 1 lists how many
10.4.1 Set the calibrated temperature control to 475°F
pizzas are required for each run of a heavy load test.
(246°C) and preheat the conveyor oven.
10.4.2 Allow the conveyor oven to idle for 60 min after the
NOTE 6—Ensure enough stabilization pizzas to follow test pizzas to
burners or elements commence cycling. maintain a full cooking compartment.
FIG. 4 Pizzas Loaded to Maximize Belt Coverage
F1817 − 17 (2022)
TABLE 1 Total Number of Pizzas Required for Each Run of a
oven cavity.The cook time will be different from the conveyor
A
Heavy Load Test
speed, which is the time it takes for a single point on the
Conveyor Width (inches)
conveyor to pass through the oven cavity. The oven controls
Cavity Length
12 18 24 32 36 40 48
will most likely be based on the conveyor speed.
(inches)
12 4 8 8 12121616
10.7.2 Remove a pizza from the refrigerator and place the
16 4 8 8 12121616
pizza (centered on the pizza screen) directly on the scale and
18 4 8 8 12121616
record weight of pizza and screen.
20 4 8 8 12121616
24 8 16 1624243232
10.7.3 Load conveyor cooking feed belt so that the leading
28 8 16 1624243232
edge of the two outer edge pizza screens are adjacent to the
32 8 16 1624243232
36 12 24 24 36 36 48 48 entrance to the oven cavity. Note that the screens are to be
40 12 24 24 36 36 48 48
placed to the inter edge of belt knuckle (Fig. 5). Do not allow
55 16 32 32 48 48 64 64
more than 1 min to elapse from the time a pizza is removed
70 20 40 40 60 60 80 80
from the refrigerator until it is placed on the conveyor.
A
Includes both the stabilization pizzas and the test pizzas.
10.7.4 Allow the pizza to pass through the oven cavity and
cook.As soon as the entire pizza has passed through the oven
cavity,removethepizzafromtheconveyorandplacethepizza
on an insulated, nonmetall
...