

ASTM F2519-05(2020)
(Test Method)Standard Test Method for Grease Particle Capture Efficiency of Commercial Kitchen Filters and Extractors
General Information
- Abstract
SIGNIFICANCE AND USE
5.1 The pressure drop results can be added to the pressure drops of other components in an exhaust system to determine the total exhaust fan pressure requirement.
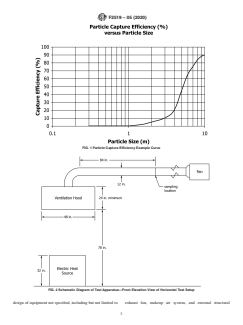
5.2 The particulate capture efficiency can be used with known particulate size emission data for a cooking appliance-food product combination to determine the total mass of grease particles captured by the filter, the total mass of grease particles that pass through the filter, and the particle size distribution of the grease particles that pass through the filter. Fig. 1 shows an example particle capture efficiency curve.
FIG. 1 Particle Capture Efficiency Example Curve
SCOPE
1.1 This test method can be used to determine the grease particle capture efficiency of components and systems used in commercial kitchens to capture grease effluent prior to entering the exhaust duct. The results can be used to select a filter system best suited to a particular application.
1.2 This test method is applicable to filter components and systems. The performance information is obtained for new or clean filters and does not include the performance of used or loaded filters.
1.3 The filter can be evaluated with respect to the following (where applicable):
1.3.1 Pressure drop as a function of airflow through the filter (10.3), and
1.3.2 Particulate capture efficiency by particle size (10.4).
1.4 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are for information only.
1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use.
1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
- Status
- Published
- Publication Date
- 30-Nov-2020
- Technical Committee
- F26 - Food Service Equipment
- Drafting Committee
- F26.07 - Commercial Kitchen Ventilation
Overview
ASTM F2519-05(2020) is the standard test method developed by ASTM for evaluating the grease particle capture efficiency of commercial kitchen filters and extractors. This method measures the ability of filtration systems used in commercial kitchen ventilation systems to capture grease particles from cooking effluent before it enters the exhaust ductwork. The standard provides reliable procedures to assess both the pressure drop and particulate capture efficiency of new or clean filters, which is essential for commercial kitchen safety, regulatory compliance, and effective exhaust system design.
Key Topics
Grease Particle Capture Efficiency
Measures the proportion of grease particles of various sizes that are captured by filters and extractors, expressed as a percentage. This data helps in selecting the most appropriate filter system for specific commercial kitchen applications.Pressure Drop Measurement
The standard outlines procedures to evaluate the resistance (pressure drop) created by different filters as airflows through them. This is a critical factor in determining the overall power requirements of an exhaust fan and the energy efficiency of the kitchen ventilation system.Applicable Filter Types
This standard applies to three primary classes of commercial kitchen filters:- Removable baffle filters
- Removable cartridge filters
- Fixed extractors
Testing involves assessing new or clean filters; the performance of used or loaded filters is not addressed.
Particle Size Distribution
Testing provides the capture efficiency by specific particle size ranges, allowing kitchen managers and engineers to understand which filters are most effective against the smallest, and potentially most hazardous, grease particles.Safety and Compliance
The standard highlights the need for users to observe proper safety, health, and environmental practices and to be aware of relevant regulations when implementing the test method.
Applications
Commercial Kitchen Ventilation Design
Filter efficiency and pressure drop data obtained using ASTM F2519-05(2020) inform the design and selection of kitchen exhaust filtration systems, ensuring that appropriate filtration devices are installed for specific cooking appliances and food products.Regulatory Compliance and Fire Safety
By following this standard, kitchen operators can meet local and national fire codes and ventilation regulations that require minimum filtration efficiencies for grease removal in commercial cooking environments.Performance Benchmarking
Manufacturers of commercial kitchen filters and extractors use this standard to test and verify the performance claims of their products. Facility managers use the results to compare different filter models and make evidence-based procurement decisions.Exhaust System Optimization
Results on pressure drop can be added to other exhaust system pressure losses to accurately determine exhaust fan requirements, leading to better energy management and reduced operating costs.
Related Standards
ANSI/ASHRAE Standard 52.2-1999:
Method of Testing General Ventilation Air-Cleaning Devices for Removal Efficiency by Particle Size. Used as a referenced method for air-cleaning device efficiency testing.ISO 3966:
Measurement of Fluid Flow in Closed Conduits - Velocity-Area Method Using Pitot Static Tubes. Referenced for accurate airflow measurement procedures used in the ASTM F2519 test method.
Summary
ASTM F2519-05(2020) provides a comprehensive, internationally recognized test method for quantifying the effectiveness of commercial kitchen filters and extractors in capturing grease particulates and for measuring the corresponding pressure drop. Applying this standard supports safer, cleaner, and more energy-efficient commercial kitchens by enabling scientifically-backed equipment selection and ensuring compliance with ventilation safety standards. Proper use of this grease capture efficiency test is essential for all stakeholders involved in commercial kitchen ventilation, including engineers, facility operators, safety officers, and equipment manufacturers.
Frequently Asked Questions
ASTM F2519-05(2020) is a standard published by ASTM International. Its full title is "Standard Test Method for Grease Particle Capture Efficiency of Commercial Kitchen Filters and Extractors". This standard covers: SIGNIFICANCE AND USE 5.1 The pressure drop results can be added to the pressure drops of other components in an exhaust system to determine the total exhaust fan pressure requirement. 5.2 The particulate capture efficiency can be used with known particulate size emission data for a cooking appliance-food product combination to determine the total mass of grease particles captured by the filter, the total mass of grease particles that pass through the filter, and the particle size distribution of the grease particles that pass through the filter. Fig. 1 shows an example particle capture efficiency curve. FIG. 1 Particle Capture Efficiency Example Curve SCOPE 1.1 This test method can be used to determine the grease particle capture efficiency of components and systems used in commercial kitchens to capture grease effluent prior to entering the exhaust duct. The results can be used to select a filter system best suited to a particular application. 1.2 This test method is applicable to filter components and systems. The performance information is obtained for new or clean filters and does not include the performance of used or loaded filters. 1.3 The filter can be evaluated with respect to the following (where applicable): 1.3.1 Pressure drop as a function of airflow through the filter (10.3), and 1.3.2 Particulate capture efficiency by particle size (10.4). 1.4 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are for information only. 1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use. 1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
SIGNIFICANCE AND USE 5.1 The pressure drop results can be added to the pressure drops of other components in an exhaust system to determine the total exhaust fan pressure requirement. 5.2 The particulate capture efficiency can be used with known particulate size emission data for a cooking appliance-food product combination to determine the total mass of grease particles captured by the filter, the total mass of grease particles that pass through the filter, and the particle size distribution of the grease particles that pass through the filter. Fig. 1 shows an example particle capture efficiency curve. FIG. 1 Particle Capture Efficiency Example Curve SCOPE 1.1 This test method can be used to determine the grease particle capture efficiency of components and systems used in commercial kitchens to capture grease effluent prior to entering the exhaust duct. The results can be used to select a filter system best suited to a particular application. 1.2 This test method is applicable to filter components and systems. The performance information is obtained for new or clean filters and does not include the performance of used or loaded filters. 1.3 The filter can be evaluated with respect to the following (where applicable): 1.3.1 Pressure drop as a function of airflow through the filter (10.3), and 1.3.2 Particulate capture efficiency by particle size (10.4). 1.4 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are for information only. 1.5 This test method may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety, health, and environmental practices and determine the applicability of regulatory limitations prior to use. 1.6 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
ASTM F2519-05(2020) is classified under the following ICS (International Classification for Standards) categories: 97.040.20 - Cooking ranges, working tables, ovens and similar appliances. The ICS classification helps identify the subject area and facilitates finding related standards.
ASTM F2519-05(2020) is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the
Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
Designation: F2519 − 05 (Reapproved 2020) An American National Standard
Standard Test Method for
Grease Particle Capture Efficiency of Commercial Kitchen
Filters and Extractors
This standard is issued under the fixed designation F2519; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope 2. Referenced Documents
1.1 This test method can be used to determine the grease
2.1 ASHRAE Standard:
particle capture efficiency of components and systems used in
ANSI/ASHRAE Standard 52.2-1999, Method of Testing
commercial kitchens to capture grease effluent prior to entering
General Ventilation Air-Cleaning Devices for Removal
the exhaust duct. The results can be used to select a filter
Efficiency by Particle Size
system best suited to a particular application.
2.2 ISO Standard:
ISO Standard 3966, Measurement of Fluid Flow in Closed
1.2 This test method is applicable to filter components and
systems. The performance information is obtained for new or Conduits—VelocityArea Method Using Pitot StaticTubes
clean filters and does not include the performance of used or
3. Terminology
loaded filters.
3.1 Definitions:
1.3 The filter can be evaluated with respect to the following
3.1.1 airflow rate, n—volumetric flow rate of air that passes
(where applicable):
through a filter or a bank of filters.
1.3.1 Pressuredropasafunctionofairflowthroughthefilter
(10.3), and 3.1.2 capture effıciency, n—proportion of aerosol particles
removed by a filter as a function of particle size, usually
1.3.2 Particulate capture efficiency by particle size (10.4).
expressed as a percentage.
1.4 The values stated in inch-pound units are to be regarded
3.1.3 cartridge filter, n—removable extractor, a removable,
as standard. The values given in parentheses are for informa-
integral component of listed exhaust hoods, which is typically
tion only.
constructed of stainless steel and containing a series of
1.5 This test method may involve hazardous materials,
horizontal baffles designed to remove grease and drain it into a
operations, and equipment. This standard does not purport to
container.
address all of the safety concerns, if any, associated with its
3.1.4 fixed extractor, n—water-wash hood or linear slot
use. It is the responsibility of the user of this standard to
hood, a fixed, integral component of listed exhaust hoods,
establish appropriate safety, health, and environmental prac-
which is typically constructed of stainless steel and containing
tices and determine the applicability of regulatory limitations
aseriesofhorizontalbafflesthatrunthefulllengthofthehood.
prior to use.
3.1.5 grease filter, n—device installed into a hood to capture
1.6 This international standard was developed in accor-
grease effluent before it enters the exhaust duct. Several
dance with internationally recognized principles on standard-
identical devices may be installed in parallel in a hood. The
ization established in the Decision on Principles for the
device may consist of more than one component or section.
Development of International Standards, Guides and Recom-
mendations issued by the World Trade Organization Technical
3.1.6 pressure drop, n—change in static pressure between
Barriers to Trade (TBT) Committee.
the front surface of the grease filter and its rear surface under
the rated airflow rate conditions.
This test method is under the jurisdiction of ASTM Committee F26 on Food
Service Equipment and is the direct responsibility of Subcommittee F26.07 on Available from American Society of Heating, Refrigerating, and Air-
Commercial Kitchen Ventilation. Conditioning Engineers, Inc. (ASHRAE), 1791 Tullie Circle, NE, Atlanta, GA
Current edition approved Dec. 1, 2020. Published December 2020. Originally 30329.
approved in 2005. Last previous edition approved in 2015 as F2519 – 05 (2015). Available from International Organization for Standardization (ISO), 1 rue de
DOI: 10.1520/F2519-05R20. Varembé, Case postale 56, CH-1211, Geneva 20, Switzerland.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
F2519 − 05 (2020)
3.1.7 reference hood, n—Type I exhaust hood used for the measured when the filters are installed. The total exhaust
“no extractors” condition when measuring the efficiency and volumetric flow rate must be equal in both pressure drop
pressure drop of fixed extractor hoods. This is typically the measurements.
same hood that is used for testing removable grease filters and 4.2.4.2 For fixed-extractor hood systems, the pressure drop
removable cartridge filters. is determined by subtracting the pressure drop of the reference
hood when the filters are removed from the pressure drop
3.2 Symbols:
measured on the fixed-extractor hood. The total exhaust
volumetric flow rate must be equal in both pressure drop
measurements.
E = capture efficiency
n = number of sample sets
4.3 The total airflow rate through the exhaust system is set
P = penetration
so that the volumetric flow rate through the filter under test is
t = t distribution variable
equivalent 250 cfm per linear foot (width) of filter (based on
T = sampling time
external filter dimensions).
W = counts of each size range (or channel) with test
4.3.1 Performancemayalsobeevaluatedatotherairflowsin
device(s) installed
accordance with manufacturer recommendations (see Appen-
WO = counts of each size range (or channel) without test
dix X1).
device(s)
δ = standard deviation of a sample
4.4 Balanced makeup air shall be provided at 75 6 5°F and
50 6 20 % RH.
4.5 Particulate capture efficiency for removable grease filter
3.3 Subscripts:
or removable cartridges is determined by comparing particle
concentration versus size in the exhaust duct with and without
b = background
the filters installed.
c = correlation
4.5.1 Particulate capture efficiency for hoods with fixed
e = estimated
extractorsisdeterminedbycomparingparticleconcentrationas
i = sample number
a function of particle size in the exhaust duct with the fixed
lcl = lower confidence limit
extractor hood and the reference hood without the filters
n = number of sample sets
installed.
o = observed
4.5.2 The test aerosol is oleic acid that covers a size range
t = testing a filter
from 0.3 to 10 µm in diameter or as specified by the
ucl = upper confidence limit
w = with test device(s) installed manufacturer. Efficiency shall be reported as zero from 0.3 µm
wo = without test device(s) installed
to the lower limit of the test conditions. Particulate concentra-
tion measurements (as a function of particle size) are taken in
4. Summary of Test Method the exhaust duct using an isokinetic sampling probe and an
optical particle counter. The particulate capture efficiency is
4.1 There are three predominant classes of filters in kitchen
determined by taking the difference between the particle
ventilation grease extraction systems: removable baffle filters,
concentration with and without the filters installed at each
removable cartridge filters, and fixed extractors.
particle size range set on the particle counter.
4.2 Removable baffle and cartridge filters to be tested are
5. Significance and Use
installed into the test system.
4.2.1 Identical filters to be tested are installed into a 5.1 The pressure drop results can be added to the pressure
standard 4-ft canopy hood connected to a nominal 12-in. round
drops of other components in an exhaust system to determine
duct exhaust system. The filters should fit tightly together and the total exhaust fan pressure requirement.
into the opening and any bypasses larger than ⁄8-in. wide on
5.2 The particulate capture efficiency can be used with
the ends are sealed.
known particulate size emission data for a cooking appliance-
4.2.2 For fixed-extractor systems, a reference hood shall be
food product combination to determine the total mass of grease
used for testing conditions that call for no filters to be installed
particlescapturedbythefilter,thetotalmassofgreaseparticles
in the hood. Testing requires switching between the reference
that pass through the filter, and the particle size distribution of
hood and the fixed extractor hood.
the grease particles that pass through the filter. Fig. 1 shows an
4.2.3 A filter system to be used in a non-standard canopy
example particle capture efficiency curve.
hood is installed at the height of actual application above the
6. Apparatus
floor and connected to a nominal 12-in. round duct exhaust
system.
6.1 Mandatory and Discretionary Requirements—Critical
4.2.4 Thestaticpressuredropacrossthefiltersisrecordedat
dimensions and arrangements of the test apparatus are shown
the test airflow.
in Figs. 2-5. Vertical ductwork may also be used with the same
4.2.4.1 For removable baffle or cartridge filters, the net filter critical dimensions (duct diameter, length, and so forth). All
pressure drop is determined by subtracting the pressure drop of dimensions shown are mandatory unless otherwise indicated.
the hood when the filters are removed from the pressure drop Units shown are in inches unless otherwise indicated. The
F2519 − 05 (2020)
FIG. 1 Particle Capture Efficiency Example Curve
FIG. 2 Schematic Diagram of Test Apparatus—Front Elevation View of Horizontal Test Setup
design of equipment not specified, including but not limited to exhaust fan, makeup air system, and external structural
F2519 − 05 (2020)
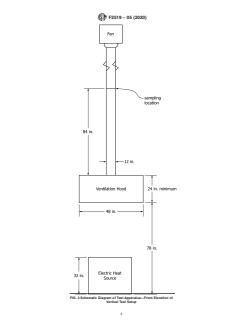
FIG. 3 Schematic Diagram of Test Apparatus—Front Elevation of
Vertical Test Setup
F2519 − 05 (2020)
in the center of the hood with the rear surface of the opening
1.0 in. from the back side of the hood. If the hood is installed
at a different height, a distance of 46 in. must be maintained
between the appliance surface and bottom of the hood. The
hood shall contain means for securing grease filters under test
in a position typical in application.
6.2.1.2 Hoods with fixed extractors should be built to match
the description given in 6.2.1.1 as closely as possible without
affecting the hood’s extraction efficiency.
6.2.1.3 The typical reference hood will be a canopy exhaust
hood matching the one described in 6.2.1.1 and shown in Fig.
6. If the hood with fixed extractors cannot be built to match
6.2.1.1,thenthereferencehoodshallbebuilttomatchthehood
with fixed extractors.
FIG. 4 Schematic Diagram of Test Apparatus—Plan View
6.2.1.4 To facilitate switching hoods, the lab may build
rolling stands for each reference hood and the current hood
being tested. These stands may be rolled in and out of the test
rig. Care should be taken to insure that both hoods are installed
in the same location at the same height (6 ⁄2 ft) each time.
6.2.1.5 The test apparatus shown in Figs. 2-5 is designed for
test filters with a nominal height of 20 in. It is permitted to test
a bank of several filters in parallel if the width of an individual
filtration device is less than 50 % of the width of the hood.
Spacers may be added symmetrically on both ends of the filter
under test if the filter does not span the entire width of the
hood.
6.2.2 Round Exhaust Duct, 12 in. (0.305 m) in diameter,
connected to the duct collar on the top of the exhaust hood and
leading to an exhaust fan.All duct connections shall be sealed.
The duct may be horizontal or vertical. If horizontal, it must
have a 90-degree elbow configured as shown in Fig. 7. The
elbow must have a centerline duct radius of 14-in.
NOTE 1—The r/D ratio is 1.167 for this configuration.
6.2.2.1 The distance from the duct collar for a vertical
exhaust duct or from the end of the 90 degree elbow for a
horizontal exhaust duct to the sampling location shall be 84 in.
If a different sampling location is used, or a different exhaust
configuration is used, an aerosol uniformity test shall be
conducted.
6.2.2.2 The minimum distance from the sampling location
to the nearest duct fitting or fan inlet shall be 24 in.
6.2.3 Exhaust Fan, capable of moving 1000 ft /min (472
L/s) through the filters under test and the additional exhaust
system components at the test static pressure condition. The
FIG. 5 Schematic Diagram of Test Apparatus—Side Elevation
fan shall have a variable frequency drive or other means to
View
control the airflow rate. The exhaust shall be discharged
outdoors.
6.2.4 MakeupAir System, a means for providing makeup air
supports, is discretionary, but the equipment must have ad-
at 75 6 5°F and 50 6 20 % relative humidity to match exhaust
equate capacity to meet the requirements of this test method.
rate without disturbing the airflow pattern near the exhaust
6.2 Test Facility:
hood.
6.2.1 Exhaust Hood:
6.2.5 Heat Source, a uniform electric heat source with a
6.2.1.1 The test installation should have a canopy exhaust
solid metal surface, a minimum 2 ft. deep by 3 ft. wide,
hoodwhichmeetstheserequirements:4ft(1.2m)inwidthand
maintained at an average surface temperature of 375 6 5°F.
depth, minimum 2 ft (0.61 m) in height, wall mounted with the
lower edge of the hood 6 ⁄2 ft (2.0 m) from the floor and with
NOTE 2—A commercial electric griddle with a rated input between 7
a 12 in. (0.305 m) diameter round duct collar mounted on top and 10 kW and been shown to work well as a heat source.
F2519 − 05 (2020)
FIG. 6 Schematic Diagram of Reference Hood
rateversusfanspeedwithandwithoutfiltersinstalledtosetthe
fan speed for proper airflow rate. The airflow and filter static
pressure shall be continuously monitored.
6.3.1.2 Airflow rate may be determined by means ofASME
long-radius flow nozzles with static taps. The dry bulb
temperature, absolute pressure, and relative humidity of the
exhaust airflow shall be measured in the duct immediately
upstream of the flow-measuring device. These values shall be
used for calculation of airflow rate. Measurements shall be
made with and without the test filters installed to set the fan
speed for proper airflow rate at each test condition.
6.3.2 Barometer, for measuring absolute pressure of the air
entering the exhaust hood. The barometer shall have a resolu-
FIG. 7 Schematic Diagram of 90-Degree Elbow to Connect the
tion of 0.2 in. Hg (670 Pa).
Duct Collar on the Canopy Hood to a Horizontal 12 in. Diameter
6.3.3 Differential Pressure Gage,formeasuringthepressure
Round Exhaust Duct
drop across the filters under test. The pressure gage shall have
a range from 0 to 5 in. water (0 to 2.5 kPa), and have an
accuracy of 1 % at full scale.
6.2.5.1 The cooking surface of the heat source shall be 32
6.3.4 Temperature Sensors, industry standard Type T or K
in. (0.81 m) above the floor. The heat source shall be centered
thermocouples, one mounted at the inlet to the particle sam-
under the hood from side to side and from front to back. Any
pling probe in the exhaust duct to measure the temperature of
air gap between the rear of the heat source and the back wall
the exhaust, the other located 6 ⁄2 ft from the floor and 6 ft in
shall be sealed with a horizontal sheet of stainless steel
front of the center of the exhaust hood with radiation shielding
positioned at the same height as the rear of the heat source.
to measure the dry bulb temperature of the makeup air.
6.3 Instrumentation:
6.3.5 Humidity Sensor, relative humidity sensor or dew
6.3.1 Flow Metering Station, installed in the exhaust duct
point hygrometer to determine the relative humidity of the
for measuring the airflow rate through the filters under test.
makeupairataheightof6 ⁄2ftabovethefloorand6ftinfront
Options include a grid of local velocity measurements using
of the center of the exhaust hood.
the log-Tchebycheff method, a flow nozzle, or an orifice plate.
If a nozzle or orifice plate is used, it must be mounted 6.4 Aerosol Generation System:
6.4.1 Other than the requirements of the following
downstream from the particle sampling location.
6.3.1.1 Airflow rate may be determined using velocity subsections, design features of the aerosol generator are
discretionary. Refer to Appendix X2 for guidance.
traverse measurements according to the log-Tchebycheff
method (ISO Standard 3966). Local velocities shall be mea- 6.4.2 The test aerosol shall be polydisperse liquid-phase
sured at the particle sampling location using a pitot tube, hot oleic acid particles generated from a solution. The solution
film anemometer, or hot wire anemometer. Velocity profiles may be pure reagent grade oleic acid or a mixture of reagent
shall be measured without filters installed in the hood and with grade oleic acid and isopropyl alcohol. The aerosol generator
test filters installed. Results shall be used to determine airflow shall provide a stable test aerosol of sufficient concentration
F2519 − 05 (2020)
over the diameter size range to meet the requirements of 6.5.4.2 The particle counter shall measure the aerosol par-
Section 12 without overloading the aerosol particle counter. ticles in its native particle size ranges and then the test aerosol
See 8.4. The aerosol generator shall be designed to ensure that particles shall be reported in 12 size ranges as shown in Table
all alcohol is evaporated from the particles prior to being 1. The particle counter’s correlation of measured response to
introduced into the test section. physicalparticlesizeshallbemonotonicforPSLparticlesfrom
0.30 to 10 mm, such that only one size range shall be indicated
6.4.3 After any alcohol evaporation necessary, the aerosol
for any measured response.
shall be brought to a Boltzman electrostatic charge distribution
6.5.4.3 The particle counter shall be calibrated annually
by a beta or gamma radiation generator with an activity of at
using known size PSL spheres.
least 185 MBq (5 mCi) or a corona discharge ionizer. The
6.5.4.4 The particle counter shall have less than 10 %
corona discharge ionizer shall have a minimum corona current
coincidence loss at a particle counting rate of 300 000 parti-
of 3 µA and shall be balanced to provide equal amounts of
cles⁄min and shall have a minimum inlet volume flow rate of
positive and negative ions.
0.100 cfm. This flow rate shall not change more than 2 % with
6.4.4 The test aerosol shall be injected vertically upward at
a 4.0 in. of water change in the pressure of the sampled air.
a point centered on the heated surface (front to back and side
to side) and from 11 to 13 in. in height above the surface of the
6.6 Data Acquisition System(s), for monitoring and record-
heat source. The injection system design is discretionary
ing the surface temperature distribution on the griddle, the
provided it fulfills the requirement.
temperature and relative humidity of the makeup air, the
temperature in the exhaust duct, and the particle concentration
6.5 Aerosol Sampling and Measurement System:
versus size in the exhaust duct, is discretionary.
6.5.1 Aerosol Sampling Probe, for sampling particles in the
exhaust duct. The probe shall be sharp edged and designed for
7. Reagents and Materials
isokinetic sampling at the given average duct velocity.
7.1 Test Aerosol—The test aerosol shall be liquid oleic acid
6.5.2 The design criterion for the sampling system shall be
particles generated from a solution. The oleic acid shall be
to provide a particle transport of >50 % for 10 µm diameter
reagent grade. The solution may consist of 100 % oleic acid. If
oleic acid particles from the sampling probe inlet within the
necessary, reagent grade isopropyl alcohol may be used in the
exhaust duct to the inlet of the particle counter.
solution to assist the performance of the aerosol generator. The
6.5.3 Diluters, if used, shall provide equal dilution of both
volume of isopropyl alcohol shall be based on the manufac-
samples taken with and without the test filter installed in the
turer’s specification for the generator.
hood. Dilution of just the sample without the filter installed is
disallowed.
8. Preparation of Apparatus
6.5.4 Particle Counters, permitted are optical counters
8.1 Apparatus qualification tests shall verify quantitatively
(OPC) with wide-angle collection optics or other counters
that the test rig and sampling procedures are capable of
demonstrating good correlation in measuring particle size
providing reliable pressure drop and particle size efficiency
efficiencies, such as an aerodynamic particle counter (APC).
measurements.Thetestsshallbeperformedinaccordancewith
AnAPC shall first be tested with oleic acid aerosol to establish
Table 2.
the relationship between the aerodynamic particle size and the
8.1.1 Qualification tests shall be performed for:
light-scattering particle size determined by an OPC. Calibrate
8.1.1.1 Air velocity uniformity in the exhaust duct,
the APC with polystyrene latex (PSL) spheres and use the
8.1.1.2 Aerosol concentration uniformity in the exhaust
relationship to express results as equivalent light-scattering
duct,
size of oleic acid.
8.1.1.3 Aerosol concentration limit in the exhaust duct,
8.1.1.4 Aerosol generator response time,
NOTE 3—Different instruments categorize particle size using different
means.WithanOPC,abeamoflightisusedtomeasurethegeometricsize
8.1.1.5 Particle counter zero,
of the particle, which is called the geometric mean diameter, d.AnAPC
e
8.1.1.6 Particle counter sizing accuracy,
instrument measures the aerodynamic size of the particle, d . The
a
relationship between these two is shown in Eq 1.Therefore, to convert the
reported data from anAPC to an OPC, Eq 2 shall be used. For oleic acid,
TABLE 1 Particle Counter Size Range Boundaries
the density is 1.117 gm/cm .
Geometric Mean
Lower Limit Upper Limit Particle Size
d 5 d ·=ρ (1)
a c
Range (µm) (µm) (µm)
where:
1 0.30 0.40 0.35
2 0.40 0.55 0.47
d = aerodynamic particle size,
a
3 0.55 0.70 0.62
d = geometric particle size, and
e
4 0.70 1.00 0.84
ρ = density of the particle.
5 1.00 1.30 1.14
6 1.30 1.60 1.44
d
a
7 1.60 2.20 1.88
d 5 (2)
e
8 2.20 3.00 2.57
=ρ
9 3.00 4.00 3.46
10 4.00 5.50 4.69
6.5.4.1 Theparticlecountershallbecapableofcountingand
11 5.50 7.00 6.20
sizing individual oleic acid particles in the particle diameter
12 7.00 10.00 8.37
size range.
F2519 − 05 (2020)
TABLE 2 Summary of System Qualification Measurement Requirements
Parameter Requirement
Aerosol Uniformity: Coefficient of variation must be <15%
Based on traverse measurements over the 25-point grid at each test
airflow rate
Upper Concentration Limit: No predetermined level
Based on limiting the concentration to below the level corresponding
to the onset of
coincidence error
Aerosol Generator Response Time No predetermined level
Particle Counter Zero Count Check: <10 counts per minute over the 0.3 to 10 µm range
Based on HEPA filer attached to the instrument’s inlet
Particle Counter Sizing Accuracy Check: Relative maximum must appear in the appropriate sizing channel.
Based on sampling of aerosolized monodispersed PSL spheres of
known size
Aerosol Neutralizer Activity: Radioactivity must be detected.
Based on detection of radioactive source within neutralizer
Heat Source Surface Temperature: Average surface temperature must be 375 ± 5ºF.
Based on thermocouples connected to the cooking surface
TABLE 3 Position of Measurements According to log-
8.1.1.7 Radioactivity of the aerosol neutralizer, and Tchebycheff Rule for a 12-in. Duct
8.1.1.8 Electric heat source surface temperature.
Sample Point Distance from Side Wall
Inlet Opening, in.
8.2 Velocity Uniformity in the Exhaust Duct:
1 0.384
8.2.1 The uniformity of the air velocity in the exhaust duct
2 1.620
at the sampling location shall be determined by three six-point 3 3.852
4 8.148
traverses using the grid points shown in Fig. 8 and specified in
5 10.380
Table 3, in the 12-in. diameter exhaust duct at vertical, and at
6 11.616
60 degrees clockwise and counter-clockwise from the vertical.
The velocity measurements shall be made with an instrument
having an accuracy of 10 % with approximately 10 fpm
resolution.The uniformity test shall be performed at an airflow
8.2.3 The CV (where CV is the coefficient of variation
rate of 1000 cfm.
computed as the standard deviation/mean) of the nineteen
8.2.2 A one-minute average velocity shall be recorded at
corresponding grid point air velocity values shall be less than
each grid point. The average must be based on at least ten
10 %.
readings taken at equal intervals during the 1-min period. The
8.3 Aerosol Concentration Uniformity in the Exhaust Duct:
traverse shall then be repeated two more times to provide
triplicate 1-min averages at each point for the given airflow 8.3.1 The uniformity of the aerosol concentration in the
exhaust duct at the sampling location shall be determined by a
rate. The average of the triplicate readings at each point shall
be computed. twenty six-point traverse using the grid points shown in Fig. 9
and specified in Table 4 in the 12-in. diameter exhaust duct.
The inlet nozzle of the sample probe shall be sharp edged and
of appropriate entrance diameter to maintain isokinetic sam-
pling within 10 % at the test airflow. The uniformity test shall
be performed at an airflow rate of 1000 cfm.
8.3.2 The oleic acid aerosol shall be provided by the aerosol
generator specified in 6.4 and the aerosol shall be injected
vertically upward from a point 12 in. (61 in.) above the center
of the griddle. The aerosol sampling probe shall remain
stationary in its normal center-of-duct sampling location.
8.3.3 The aerosol concentration measurements shall be
made with a particle counter meeting the specifications of
6.5.4. A one-minute sample shall be taken at each grid point
with the aerosol generator operating. After sampling all 26
points, the traverse shall be repeated four more times to
provide a total of five samples at each point. The five values at
each point shall be averaged for each of the particle counter
size ranges.
8.3.4 The CV of the corresponding 26 grid point particle
concentrations shall be less than 15 % in each of the particle
counter size ranges.
FIG. 8 Schematic of Velocity Measurement Locations Within the
Exhaust Duct 8.4 Concentration Limit in the Exhaust Duct:
F2519 − 05 (2020)
an airflow rate of 1000 cfm with the aerosol sampling probe
inlet located at the center of the exhaust duct.
8.5.2 Measure the time interval for the aerosol concentra-
tion to return to the background level after turning off the
generator. The exhaust flow rate shall be maintained at 1000
cfm.
8.5.3 These time intervals shall be used as the minimum
waiting time between (1) activating the aerosol generator and
beginning the particle counter sampling sequence, and (2)
deactivating the aerosol generator and beginning the particle
counter sampling sequence for determination of background
aerosol concentrations.
8.6 Particle Counter Zero:
8.6.1 The zero count of the particle counter shall be verified
to be <10 total counts per sample time, as determined in
12.5.2.2, used during testing in the 0.30 to 10 µm size range
when operating with a HEPA filter attached directly to the
instrument’s inlet.
8.7 Particle Counter Sizing Accuracy:
8.7.1 The sizing accuracy of the particle counter shall be
checked by sampling aerosols containing monodispersed
spheres of known size. Two sizes shall be used; one between
0.3 and 1 µm and the other between 1 and 10 µm.The particles
may be solid polystyrene spheres or liquid drops of known
FIG. 9 Schematic of Particle Concentration Measurement Loca-
composition.Arelativemaximumparticlecountshallappearin
tions Within the Exhaust Duct
theparticlecountersizingchannelthatencompassestheknown
diameter of the monodisperse aerosol.
TABLE 4 Sample Point Locations for Duct Aerosol Spatial
Uniformity Tests for a 12-in. Duct 8.8 Confirmation of the Activity of the Aerosol Neutralizer:
Sample Points Distance from Side Wall Inlet Opening, in. 8.8.1 The activity of the radiation source within the aerosol
neutralizer shall be confirmed by use of an appropriate radia-
1 0.252
2 0.804
tion detection device. The measurement may be relative (as
3 1.416
opposed to absolute) but shall be adequate to indicate the
4 2.124
presence of an active source and shall be capable of being
5 3.000
6 4.272
performed in a repeatable manner.
7 6.000
8.8.2 The measurement shall be repeated annually and
8 7.728
compared to prior measurements to determine if a substantial
9 9.000
10 9.876
decreaseinactivityhasoccurred.Replaceneutralizersshowing
11 10.584
a lack of activity in accordance with the manufacturer’s
12 11.196
recommendations.
13 11.748
8.9 Electric Heat Source Temperature:
8.9.1 The average surface temperature of the plate of the
heat source shall be 375 6 5°F.
8.4.1 Aseries of initial tests shall be performed over a range
of challenge aerosol concentrations, with no filters installed, to
8.10 Summary of Qualification Test Requirements—
determine a total concentration level for the particle size
Qualification test criteria shall conform to Table 2.
efficiency tests that does not overload the particle counter. The
8.11 Apparatus Maintenance—Maintenance items and
lowest total concentration level shall be less than 1 % of the
schedules shall conform to Table 5.
instrument’s stated total concentration limit. The tests shall be
performedwithnofiltersinstalledinthehoodandatanexhaust
9. Preparation of the Test Sample(s)
airflow rate of 1000 cfm.
9.1 The filter device(s) to be tested shall be new (unused)
8.4.2 The aerosol for these tests shall be generated using the
and prepared in accordance with the manufacturer’s recom-
same system and procedures as specified in 10.5.3 for the
mendations.
particle size efficiency tests.
9.2 The number of identical devices to be tested simultane-
8.5 Aerosol Generator and Sampling System Response
ouslyshallequalthenumberofdevicesthatwillspanthewidth
Time:
of the exhaust hood in the test facility.
8.5.1 Measure the time interval for the aerosol concentra-
tion to go from background level to steady test level after 9.3 Install the new, clean filter/device(s) for every series of
turning the aerosol generator on. The test shall be performed at tests. Installation shall be equivalent to a typical kitchen
F2519 − 05 (2020)
TABLE 5 Summary of Apparatus Maintenance Schedule
After a Change That
Maintenance Item (Subsection Reference) Incorporated Into Each Test Bi-Annually May Alter Performance Comment
Pressure drop across empty test section (11.2)X
Background particle count (12.2)X
Particle counter zero check (7.6) X
Particle counter primary calibration using PSL Note 1
Air velocity uniformly (7.2) X
Aerosol uniformity (7.3) X
Generator response time (7.5) X
Overloading test of particle counter (7.4) X
Confirmation of neutralizer radioactivity (7.8) X Note 2
Flow rates, pressure drops, temperature, relative Note 3
humidity, and so forth
Cleaning of test duct and components Note 4
NOTE 1—Calibration performed annually
NOTE 2—Wash the inside of radioactive neutralizer every 1-h of use. Check balance of the corona discharge ionizer monthly, per manufacturer’s
instructions.
NOTE 3—In accordance with manufacturer’s recommendations but at least annually.
NOTE 4—Cleaning intervals of the test duct, aerosol generator system, aerosol sampling lines, and other test components is discretionary.
application with no additional sealing except openings larger 10.3.3 Measure and record the differential pressure between
than ⁄8-in. wide at the ends. the static pressure tap installed in the hood downstream of the
9.3.1 If the devices do not span the entire hood opening test device(s) and the room air in the test facility at a minimum
provided in the test facility, spacers must be installed on each of four airflow rates: 50 %, 75 %, 100 %, and 125 % of test
end to center the test devices in the hood and to prevent air airflow rate.
from passing around the ends.
10.3.4 Install the device(s) in the exhaust hood as described
9.3.2 If the devices cannot be installed in the existing hood in Section 9.
at the test facility, a new 4-ft wide exhaust hood with the
10.3.4.1 If testing removable baffle filter or cartridge filter,
appropriate mounting hardware shall be installed in the facility
install the device(s) in the exhaust hood as described in Section
and characterized as in Section 8, or the mounting hardware in
9.
theexistinghoodshallbechangedtoaccommodatethedevices
10.3.4.2 If testing a hood with a fixed extractor, remove
as they would be installed in the field.
reference hood and install test hood. To save on the number of
set-ups, this may be delayed and done in conjunction with
9.4 At the beginning of every test, the airflow must be
10.4.2.
verified to be within 5 % of that
...