


ASTM D2878-10(2016)
(Test Method)Standard Test Method for Estimating Apparent Vapor Pressures and Molecular Weights of Lubricating Oils
Standard Test Method for Estimating Apparent Vapor Pressures and Molecular Weights of Lubricating Oils
SIGNIFICANCE AND USE
5.1 The vapor pressure of a substance as determined by measurement of evaporation reflects a property of the bulk sample. Little weight is given by the procedure to the presence of low concentrations of volatile impurities.
5.2 Vapor pressure, per se, is a thermodynamic property that is dependent only upon composition and temperature for stable systems. In the present method, composition changes occur during the course of the test so that the contribution of minor amounts of volatile impurities is minimized.
SCOPE
1.1 This test method covers a calculation procedure for converting data obtained by Test Method D972 to apparent vapor pressures and molecular weights. It has been demonstrated to be applicable to petroleum-based and synthetic ester lubricating oils,2 at temperatures of 395 K to 535 K (250 °F to 500 °F). However, its applicability to lubricating greases has not been established.
Note 1: Most lubricants boil over a fairly wide temperature range, a fact recognized in discussion of their vapor pressures. For example, the apparent vapor pressure over the range 0 % to 0.1 % evaporated may be as much as 100 times that over the range 4.9 % to 5.0 % evaporated.
1.2 The values stated in SI units are to be regarded as the standard. In cases in which materials, products, or equipment are available in inch-pound units only, SI units are omitted.
1.3 WARNING—Mercury has been designated by many regulatory agencies as a hazardous material that can cause central nervous system, kidney and liver damage. Mercury, or its vapor, may be hazardous to health and corrosive to materials. Caution should be taken when handling mercury and mercury containing products. See the applicable product Material Safety Data Sheet (MSDS) for details and EPA’s website—http://www.epa.gov/mercury/faq.htm—for additional information. Users should be aware that selling mercury or mercury containing products into your state or country may be prohibited by law.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability or regulatory limitations prior to use. For specific warning statements, see 6.2, 7.1, 8.2, and Annex A2.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: D2878 − 10 (Reapproved 2016)
Standard Test Method for
Estimating Apparent Vapor Pressures and Molecular
Weights of Lubricating Oils
This standard is issued under the fixed designation D2878; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope 2. Referenced Documents
1.1 This test method covers a calculation procedure for 2.1 ASTM Standards:
converting data obtained by Test Method D972 to apparent A240/A240M Specification for Chromium and Chromium-
vapor pressures and molecular weights. It has been demon- Nickel Stainless Steel Plate, Sheet, and Strip for Pressure
strated to be applicable to petroleum-based and synthetic ester Vessels and for General Applications
lubricating oils, at temperatures of 395 K to 535 K (250 °F to D92 Test Method for Flash and Fire Points by Cleveland
500 °F). However, its applicability to lubricating greases has Open Cup Tester
not been established. D972 Test Method for Evaporation Loss of Lubricating
Greases and Oils
NOTE 1—Most lubricants boil over a fairly wide temperature range, a
D2503 TestMethodforRelativeMolecularMass(Molecular
fact recognized in discussion of their vapor pressures. For example, the
Weight) of Hydrocarbons by Thermoelectric Measure-
apparent vapor pressure over the range 0 % to 0.1 % evaporated may be
as much as 100 times that over the range 4.9 % to 5.0 % evaporated.
ment of Vapor Pressure
D2595 Test Method for Evaporation Loss of Lubricating
1.2 The values stated in SI units are to be regarded as the
Greases Over Wide-Temperature Range
standard. In cases in which materials, products, or equipment
D2883 Test Method for Reaction Threshold Temperature of
are available in inch-pound units only, SI units are omitted.
Liquid and Solid Materials
1.3 WARNING—Mercury has been designated by many
E659 Test Method for Autoignition Temperature of Chemi-
regulatory agencies as a hazardous material that can cause
cals
central nervous system, kidney and liver damage. Mercury, or
its vapor, may be hazardous to health and corrosive to
3. Terminology
materials. Caution should be taken when handling mercury and
3.1 Definitions of Terms Specific to This Standard:
mercury containing products. See the applicable product Ma-
3.1.1 apparent vapor pressure (p), n—the time-averaged
terial Safety Data Sheet (MSDS) for details and EPA’s
value of the vapor pressure from the start to the end of the
website—http://www.epa.gov/mercury/faq.htm—for addi-
evaporation test.
tional information. Users should be aware that selling mercury
3.1.1.1 Discussion—While this may include some effects of
or mercury containing products into your state or country may
differences in nonideality of the vapor, heat of vaporization,
be prohibited by law.
surface tension, and viscosity between the m-terphenyl and the
1.4 This standard does not purport to address all of the
lubricating oil, these factors have been demonstrated to be
safety concerns, if any, associated with its use. It is the
negligible.Unlessstated,thisaverageshallcovertherange0to
responsibility of the user of this standard to establish appro-
5 61%.
priate safety and health practices and determine the applica-
3.1.2 cell constant (k), n—the ratio of the amount of
bility or regulatory limitations prior to use. For specific
m-terphenylorlubricatingoilcarriedoffperunitvolumeofgas
warning statements, see 6.2, 7.1, 8.2, and Annex A2.
to that predicted by Dalton’s law.
k 5 22.41 PW/VpM (1)
This test method is under the jurisdiction of Committee D02 on Petroleum
where:
Products, Liquid Fuels, and Lubricants and is the direct responsibility of Subcom-
mittee D02.L0.07 on Engineering Sciences of High Performance Fluids and Solids
k = call constant
(Formally D02.1100).
Current edition approved Jan. 1, 2016. Published February 2016. Originally
approved in 1970. Last previous edition approved in 2010 as D2878 – 10. DOI:
10.1520/D2878-10R16. For referenced ASTM standards, visit the ASTM website, www.astm.org, or
Coburn, J. F., “Lubricant Vapor Pressure Derived from Evaporation Loss,” contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
Transactions, American Society of Lubricating Engineers, ASLTA, Vol 12 , 1969, Standards volume information, refer to the standard’s Document Summary page on
pp. 129–134. the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
D2878 − 10 (2016)
6.5 Flowmeter —A rotameter calibrated to deliver air at a
P = ambient atmospheric pressure, torr
rate of 2.583 g⁄min 6 0.02 g⁄min between 289 K and 302 K
W = mass of lubricant evaporated, g
(60 °F and 85 °F) (2 L⁄min at standard temperature and
V = volume of gas passed through all litres at 273 K and
101.3 kPa (760 torr) pressure). It shall be furnished with a needle valve and
p = apparent vapor pressure, torr mounted as shown in Fig. 1.
M = mole average molecular weight of lubricant vapor,
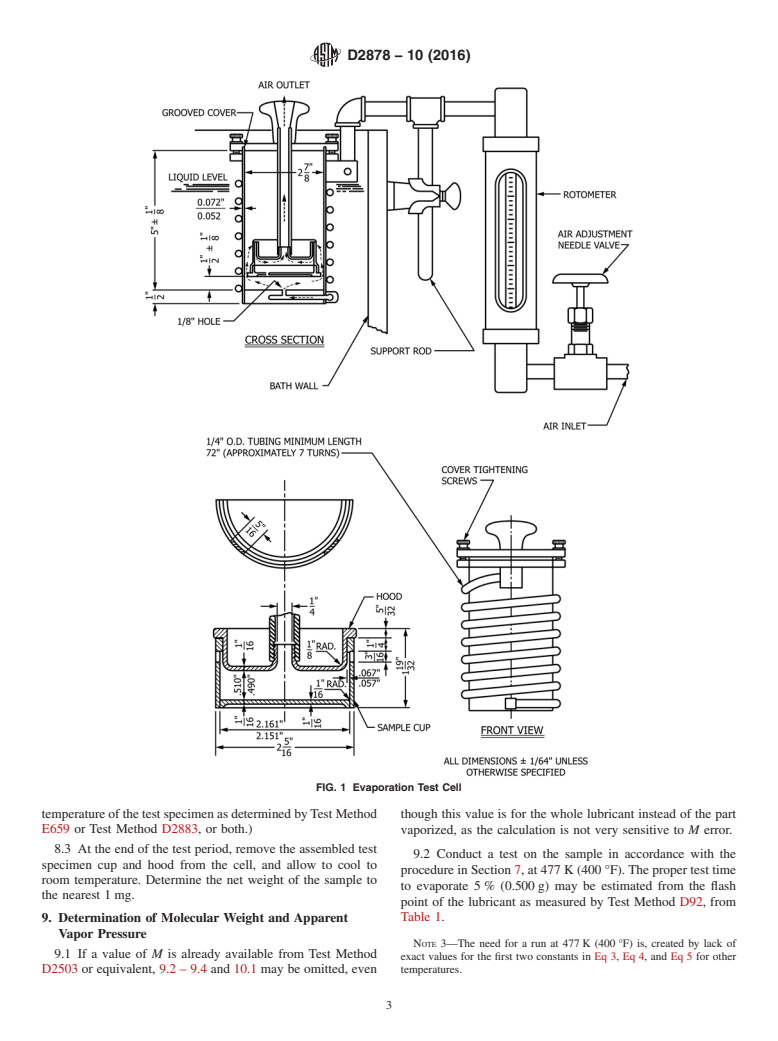
6.6 Oil Sample Cup, as described in Fig. 1 and A1.1.2.
g/mole
T = test temperature, K
7. Calibration of Equipment
Ithasbeenempiricallydeterminedthatfor m-terphenylinair
7.1 ItisassumedthatequipmentconformingtoTestMethod
k 5 0.1266 2 12.60/~ T 2 273! (2)
D972 in design and installation needs no calibration. If
questions arise, carry out the procedure using m-terphenyl
and that the cell constant is independent of the composi-
(Warning—Harmful or fatal if swallowed. See A2.2.) of good
tion of the lubricant.
commercial quality. The following two points shall be deter-
3.1.3 Test Method D972 is normally run with air, which
mined:
may cause changes in easily oxidized fluids. In such cases, use
Temperature Evaporation to Conform
of common reactive gas nitrogen and recalibration to obtain a
K °F Time, h to Eq 2,g
slightly different cell constant (k') is mandatory.
395 250 22 0.267 ± 0.027
420 300 6.5 0.503 ± 0.050
4. Summary of Test Method
If the data do not fall within the above ranges, check flow
4.1 The test is run at the selected temperature for a sufficient rate and temperature. If these are correct, prepare a substitute
time to give the selected amount of evaporation, which is 5 % equation for k' similar to Eq 2 and use it in Section 10. When
6 1 % unless otherwise specified. This evaporation rate is use of nonreactive gas is required, this calibration is necessary
compared with a standard value for pure m-terphenyl to yield as standard cell constants are not valid for gases other than air.
the apparent vapor pressure and molecular weight of the
7.2 If the apparatus specified in Test Method D2595 is to be
lubricating oil as defined in Section 3.
used, it shall be calibrated as described in 7.1.
5. Significance and Use
8. Procedure
5.1 The vapor pressure of a substance as determined by
8.1 Weigh the clean test specimen cup and hood to the
measurement of evaporation reflects a property of the bulk
nearest 1 mg. Transfer, by means of a pipet, 10.00 g 6 0.05 g
sample. Little weight is given by the procedure to the presence
of test specimen to the cup.Assemble the cup and hood, being
of low concentrations of volatile impurities.
careful not to splash oil on the underside of the hood. Weigh
the assembly and record the net test specimen weight to the
5.2 Vaporpressure, per se,isathermodynamicpropertythat
nearest 1 mg.
is dependent only upon composition and temperature for stable
systems. In the present method, composition changes occur 8.2 With cover in place, but without the hood and test
during the course of the test so that the contribution of minor specimen cup attached, allow the evaporation cell to acquire
amounts of volatile impurities is minimized. the temperature of the bath (controlled to 60.5 K (61 °F)) at
which the test is to be made by immersing the cell in it, as
shown in Fig. 1. Allow the cell to remain in the bath at least
6. Apparatus
⁄2 h before beginning the test. During this period, allow clean
6.1 Evaporation Cell, as described in Annex A1.
air (Warning—Compressed gas under high pressure. Use with
6.2 Air Supply System, capable of supplying to the cell the
extreme caution in the presence of combustible material, since
required flow of air free of entrained particles (Warning—
theautoignitiontemperaturesofmostorganiccompoundsinair
Compressedgasunderhighpressure.Usewithextremecaution
are drastically reduced at elevated pressures. SeeAnnex A2.1.)
in the presence of combustible material, since the autoignition
to flow through the cell at the prescribed rate, 2.583 g⁄min 6
temperatures of most organic compounds in air are drastically
0.02 g⁄min (2 L⁄min at standard temperature and pressure), as
reduced at elevated pressures. See Annex A2.1.). A 410 mm
indicated by the rotameter. Then remove the cover, thread and
(16 in.) length of 1 in. diameter pipe packed with glass wool
weighedhoodandsamplecupintoplace,andreplacethecover.
has been found satisfactory for filtering the air.
Tighten the three knurled cover-tightening screws securely to
prevent air leakage under the cover. Pass clean air through the
6.3 Oil Bath, as described in Annex A1.
cell for the required period. (Warning—Do not perform this
NOTE 2—Other constant-temperature baths may be used if the exit air
test with air at temperatures in excess of the autoignition
passing over the grease sample is at the test temperature (60.5 K (1 °F)).
6.4 Temperature Measuring Devices—Resistance
The sole source of supply of the apparatus known to the committee at this time
thermometers, thermocouples, or liquid-in-glass thermometers
is Flowrater meter, Fisher and Porter Co., Hatboro, PA. If you are aware of
calibrated to accuracy within 60.5 ºC (61.0 ºF) may be used.
alternative suppliers, please provide this information to ASTM International
The use of mercury-in-glass thermometers of equal accuracy is
Headquarters.Your comments will receive careful consideration at a meeting of the
permitted, although it is discouraged. responsible technical committee, which you may attend.
D2878 − 10 (2016)
FIG. 1 Evaporation Test Cell
temperature of the test specimen as determined byTest Method though this value is for the whole lubricant instead of the part
E659 or Test Method D2883, or both.) vaporized, as the calculation is not very sensitive to M error.
8.3 At the end of the test period, remove the assembled test
9.2 Conduct a test on the sample in acc
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: D2878 − 10 D2878 − 10 (Reapproved 2016)
Standard Test Method for
Estimating Apparent Vapor Pressures and Molecular
Weights of Lubricating Oils
This standard is issued under the fixed designation D2878; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 This test method covers a calculation procedure for converting data obtained by Test Method D972 to apparent vapor
pressures and molecular weights. It has been demonstrated to be applicable to petroleum-based and synthetic ester lubricating oils,
at temperatures of 395395 K to 535K (250535 K (250 °F to 500°F).500 °F). However, its applicability to lubricating greases has
not been established.
NOTE 1—Most lubricants boil over a fairly wide temperature range, a fact recognized in discussion of their vapor pressures. For example, the apparent
vapor pressure over the range 00 % to 0.1 % evaporated may be as much as 100 times that over the range 4.94.9 % to 5.0 % evaporated.
1.2 The values stated in SI units are to be regarded as the standard. In cases in which materials, products, or equipment are
available in inch-pound units only, SI units are omitted.
1.3 WARNING—Mercury has been designated by many regulatory agencies as a hazardous material that can cause central
nervous system, kidney and liver damage. Mercury, or its vapor, may be hazardous to health and corrosive to materials. Caution
should be taken when handling mercury and mercury containing products. See the applicable product Material Safety Data Sheet
(MSDS) for details and EPA’s website—http://www.epa.gov/mercury/faq.htm—for additional information. Users should be aware
that selling mercury or mercury containing products into your state or country may be prohibited by law.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability or regulatory
limitations prior to use. For specific warning statements, see 6.2, 7.1, 8.2, and Annex A2.
2. Referenced Documents
2.1 ASTM Standards:
A240/A240M Specification for Chromium and Chromium-Nickel Stainless Steel Plate, Sheet, and Strip for Pressure Vessels and
for General Applications
D92 Test Method for Flash and Fire Points by Cleveland Open Cup Tester
D972 Test Method for Evaporation Loss of Lubricating Greases and Oils
D2503 Test Method for Relative Molecular Mass (Molecular Weight) of Hydrocarbons by Thermoelectric Measurement of
Vapor Pressure
D2595 Test Method for Evaporation Loss of Lubricating Greases Over Wide-Temperature Range
D2883 Test Method for Reaction Threshold Temperature of Liquid and Solid Materials
E659 Test Method for Autoignition Temperature of Chemicals
3. Terminology
3.1 Definitions of Terms Specific to This Standard:
3.1.1 apparent vapor pressure (p), n—the time-averaged value of the vapor pressure from the start to the end of the evaporation
test.
This test method is under the jurisdiction of Committee D02 on Petroleum Products, Liquid Fuels, and Lubricants and is the direct responsibility of Subcommittee
D02.L0.07 on Engineering Sciences of High Performance Fluids and Solids (Formally D02.1100).
Current edition approved Oct. 1, 2010Jan. 1, 2016. Published October 2010February 2016. Originally approved in 1970. Last previous edition approved in 20092010 as
D2878–95(2009).D2878 – 10. DOI: 10.1520/D2878-10.10.1520/D2878-10R16.
Coburn, J. F., “Lubricant Vapor Pressure Derived from Evaporation Loss,” Transactions, American Society of Lubricating Engineers, ASLTA, Vol 12 , 1969, pp. 129–134.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
D2878 − 10 (2016)
3.1.1.1 Discussion—
While this may include some effects of differences in nonideality of the vapor, heat of vaporization, surface tension, and viscosity
between the m-terphenyl and the lubricating oil, these factors have been demonstrated to be negligible. Unless stated, this average
shall cover the range 0 to 5 6 1 %.
3.1.2 cell constant (k), n—the ratio of the amount of m-terphenyl or lubricating oil carried off per unit volume of gas to that
predicted by Dalton’s law.
k 5 22.41 PW/VpM (1)
where:
k = call constant
P = ambient atmospheric pressure, torr
W = mass of lubricant evaporated, g
V = volume of gas passed through all litres at 273K and 101.3 kPa (760 torr)
V = volume of gas passed through all litres at 273 K and 101.3 kPa (760 torr)
p = apparent vapor pressure, torr
M = mole average molecular weight of lubricant vapor, g/mole
T = test temperature, K
It has been empirically determined that for m-terphenyl in air
k 5 0.1266 2 12.60/~ T 2 273! (2)
and that the cell constant is independent of the composition of the lubricant.
3.1.3 Test Method D972 is normally run with air, which may cause changes in easily oxidized fluids. In such cases, use of
common reactive gas nitrogen and recalibration to obtain a slightly different cell constant (k') is mandatory.
4. Summary of Test Method
4.1 The test is run at the selected temperature for a sufficient time to give the selected amount of evaporation, which is 55 %
6 1 % unless otherwise specified. This evaporation rate is compared with a standard value for pure m-terphenyl to yield the
apparent vapor pressure and molecular weight of the lubricating oil as defined in Section 3.
5. Significance and Use
5.1 The vapor pressure of a substance as determined by measurement of evaporation reflects a property of the bulk sample.
Little weight is given by the procedure to the presence of low concentrations of volatile impurities.
5.2 Vapor pressure, per se, is a thermodynamic property that is dependent only upon composition and temperature for stable
systems. In the present method, composition changes occur during the course of the test so that the contribution of minor amounts
of volatile impurities is minimized.
6. Apparatus
6.1 Evaporation Cell, as described in Annex A1.
6.2 Air Supply System, capable of supplying to the cell the required flow of air free of entrained particles (Warning—
Compressed gas under high pressure. Use with extreme caution in the presence of combustible material, since the autoignition
temperatures of most organic compounds in air are drastically reduced at elevated pressures. See Annex A2.1.). A 410-mm
(16-in.)410 mm (16 in.) length of 1-in.1 in. diameter pipe packed with glass wool has been found satisfactory for filtering the air.
6.3 Oil Bath, as described in Annex A1.
NOTE 2—Other constant-temperature baths may be used if the exit air passing over the grease sample is at the test temperature (60.5K (1°F)).(60.5 K
(1 °F)).
6.4 Temperature Measuring Devices—Resistance thermometers, thermocouples, or liquid-in-glass thermometers calibrated to
accuracy within 60.5ºC (61.0ºF)60.5 ºC (61.0 ºF) may be used. The use of mercury-in-glass thermometers of equal accuracy
is permitted, although it is discouraged.
6.5 Flowmeter —A rotameter calibrated to deliver air at a rate of 2.5832.583 g ⁄min 6 0.020.02 g ⁄ g/min min between
289289 K and 302K (60 and 85°F) (2302 K (60 °F and 85 °F) (2 L ⁄ L/min min at standard temperature and pressure). It shall be
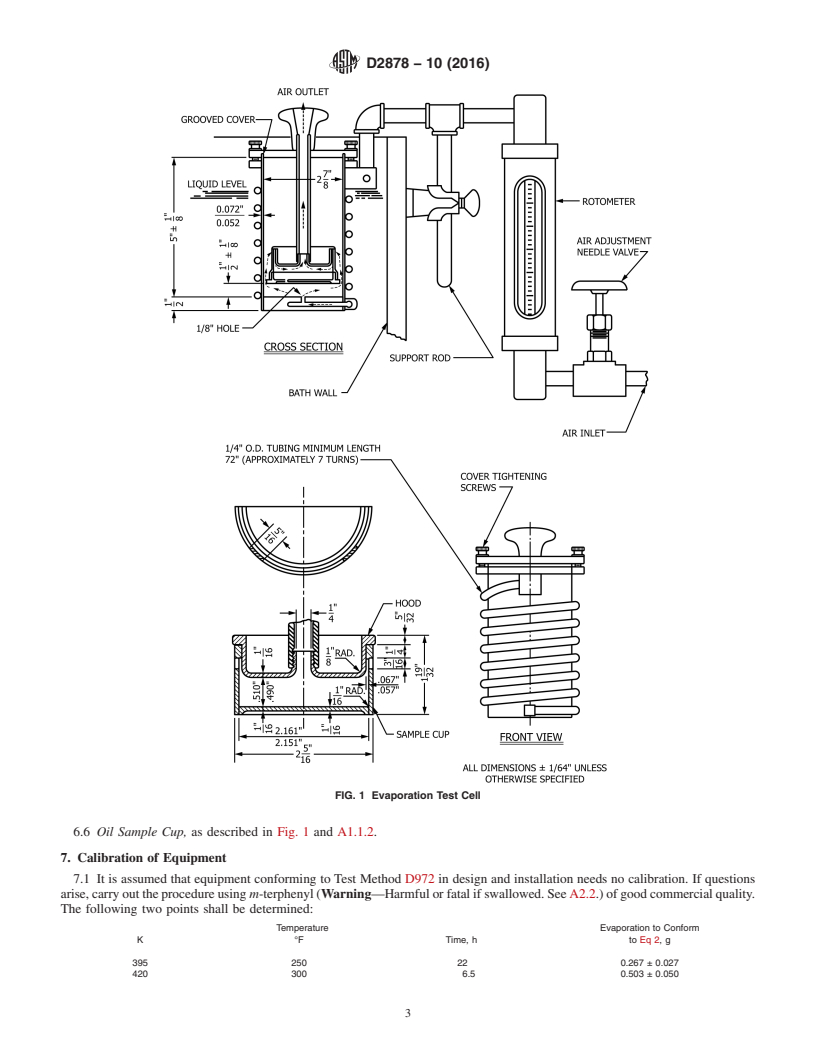
furnished with a needle valve and mounted as shown in Fig. 1.
The sole source of supply of the apparatus known to the committee at this time is Flowrater meter, Fisher and Porter Co., Hatboro, PA. If you are aware of alternative
suppliers, please provide this information to ASTM International Headquarters. Your comments will receive careful consideration at a meeting of the responsible technical
committee, which you may attend.
D2878 − 10 (2016)
FIG. 1 Evaporation Test Cell
6.6 Oil Sample Cup, as described in Fig. 1 and A1.1.2.
7. Calibration of Equipment
7.1 It is assumed that equipment conforming to Test Method D972 in design and installation needs no calibration. If questions
arise, carry out the procedure using m-terphenyl (Warning—Harmful or fatal if swallowed. See A2.2.) of good commercial quality.
The following two points shall be determined:
Temperature Evaporation to Conform
to Eq 2, g
K °F Time, h
395 250 22 0.267 ± 0.027
420 300 6.5 0.503 ± 0.050
D2878 − 10 (2016)
If the data do not fall within the above ranges, check flow rate and temperature. If these are correct, prepare a substitute equation
for k' similar to Eq 2 and use it in Section 10. When use of nonreactive gas is required, this calibration is necessary as standard
cell constants are not valid for gases other than air.
7.2 If the apparatus specified in Test Method D2595 is to be used, it shall be calibrated as described in 7.1.
8. Procedure
8.1 Weigh the clean test specimen cup and hood to the nearest 1 mg. 1 mg. Transfer, by means of a pipet, 10.0010.00 g 6 0.05
g 0.05 g of test specimen to the cup. Assemble the cup and hood, being careful not to splash oil on the underside of the hood. Weigh
the assembly and record the net test specimen weight to the nearest 1 mg.1 mg.
8.2 With cover in place, but without the hood and test specimen cup attached, allow the evaporation cell to acquire the
temperature of the bath (controlled to 60.5K (61°F))60.5 K (61 °F)) at which the test is to be made by immersing the cell in
it, as shown in Fig. 1. Allow the cell to remain in the bath at least ⁄2 h h before beginning the test. During this period, allow clean
air (Warning—Compressed gas under high pressure. Use with extreme caution in the presence of combustible material, since the
autoignition temperatures of most organic compounds in air are drastically reduced at elevated pressures. See Annex A2.1.) to flow
through the cell at the prescribed rate, 2.5832.583 g ⁄min 6 0.020.02 g ⁄ g/minmin (2 L ⁄ (2 L/min min at standard temperature and
pressure), as indicated by the rotameter. Then remove the cover, thread and weighed hood and sample cup into place, and replace
the cover. Tighten the three knurled cover-tightening screws securely to prevent air leakage under the cover. Pass clean air through
the cell for the required period. (Warning—Do not perform this test with air at temperatures in excess of the autoignition
temperature of the test specimen as determined by Test Method E659 or Test Method D2883, or both.)
8.3 At the end of the test period, remove the assembled test specimen cup and hood from the cell, and allow to cool to room
temperature. Determine the net weight of the sample to the nearest 1 mg.1 mg.
9. Determination of Molecular Weight and Apparent Vapor Pressure
9.1 If a value of M is already available from Test Method D2503 or equivalent, 9.2 – 9.4 and 10.1 may be omitted, even though
this value is for the whole lubricant instead of the part vaporized, as the calculation is not very sensitive to M error.
9.2 Conduct a test on the sample in accordance with the procedure in Section 77,, at 477K (400°F).477 K (400 °F). The proper
test time to evaporate 5 % (0.500 g) (0.500 g) may be estimated from the flash point of the lubricant as measured by Test Method
D92, from Table 1.
NOTE 3—The need for a run at 477K (400°F)477 K (400 °F) is, created by lack of exact values for the first two constants in Eq 3, Eq 4, and Eq 5 for
other temperatures.
9.3 For synthetic and redistilled petroleum oils, the variation of W/t with W is not great, and the 5 % point shall be approximated
by linear interpolation of two points taken at different W values. For single-distilled petroleum or unknown oils, three points shall
be plotted, representing the estimated time and also half and twice that time. These readings may all be obtained on one sample
by stop and start operation of the apparatus.
9.4 When a single data point that does not fall within the 55 % 6 1 % evaporated range is used (as is often justifiable on
synthetic oils) or the evaporation is measured at some other level of W, this fact shall be reported in Section 11.
9.5 The test for apparent vapor pressure is conducted in accordance with Section 8 for the estimated time at the selected
temperature. If the 5 6 1 % criterion is not met, proceed as in 9.3.
10. Calculations
10.1 Calculation of Molecular Weight:
10.1.1 Use the evaporation time, t, (in seconds) obtained in 9.3 to evaporate 55 % 6 1 %.
10.1.2 Calculate the molecular weights of lubricants in general as follows:
A
TABLE 1 Estimated Time to Evaporate 5 %, h
Flash Point Test Temperature, K (°F)
K °F 394 (250) 422 (300) 450 (350) 477 (400) 505 (450) 533 (500)
422 300 2.7 0.9 0.3 0.1 . .
450 350 8.1 2.7 0.9 0.3 0.1 .
477 400 24.3 8.1 2.7 0.9 0.3 0.1
505 450 72.9 24.3 8.1 2.7 0.9 0.3
533 500 . 72.9 24.3 8.1 2.7 0.9
561 550 . . 72.9 24.3 8.1 2.7
589 600 . . . 72.9 24.3 8.1
A
This table may be extended by means of equation:
− 1
Estimated Hours = 0.9 log [0.0095(F − 1.8T + 460)]
D2878 − 10 (2016)
logM 5 3.028 2 0.164log 10 335 PW/t (3)
~ !
10.1.3 For lubricants of known composition, slightly greater accuracy is obtained with special equations:
10.1.3.1 For polyol esters:
logM 5 3.181 2 0.207log~10 335 PW/t! (4)
10.1.3.2 For dibasic esters:
logM 5 3.089 2 0.190log 10 335 PW/t (5)
~ !
10.1.3.3 For mineral oils:
logM 5 2.848 2 0.106log 10 335 PW/t (6)
~ !
10.1.4 The molecular weight equations all contain the standard value of k at 477K (400°F) from Table 2. If a change greater
than 63 % in this value is caused by the calibration in Section 7, adjustments shall be made in the constant 10 335 by multiplying
it by the factor (k/k').
10.2 Calculation of Apparent Vapor Pressure:
10.2.1 Use the molecular weight, M, as calculated in 10.1 or predetermined in 9.1 to calculate the vapor pressure as follows:
p 5 672 PW/tkM (7)
where k is obtained from Table 2. Use Eq 2 to extend this table. If a special equation was required in 7.1, use it rather than Table
2 or Eq 2.
10.2.2 For the special case of
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.