


ASTM A391/A391M-07(2012)
(Specification)Standard Specification for Grade 80 Alloy Steel Chain
Standard Specification for Grade 80 Alloy Steel Chain
ABSTRACT
This specification deals with Grade 80 heat-treated alloy steel chain for applications such as slings, lifting assemblies, and load binding. The alloy steel chain shall be made to a fully-killed fine austenitic grain process. Alloy steel chain may be made by the electric welding or gas welding process. The material shall be heat treated which includes quenching and tempering. Material's composition shall conform to the chemical requirements for carbon, phosphorous, sulfur, nickel, chromium, and molybdenum. The material shall conform to the mechanical property requirements for breaking force and elongation and to the dimensional requirements for the appropriate size chain. All chain shall be tested to at least the proof load.
SCOPE
1.1 This specification covers Grade 80 heat-treated alloy steel chain for such applications as slings, lifting assemblies, and load binding. Note 1—This specification does not cover alloy steel chain for pocket wheel applications.
1.2 The Grade designation is 1/10 of the minimum breaking strength in newtons divided by two times the nominal cross-sectional area of the chain in square millimetres.
1.3 The values stated in either SI units or in other units shall be regarded separately as standard. The values stated in each system may not be exact equivalents; therefore, each system must be used independently of the other, without combining values in any way.
General Information
Standards Content (Sample)
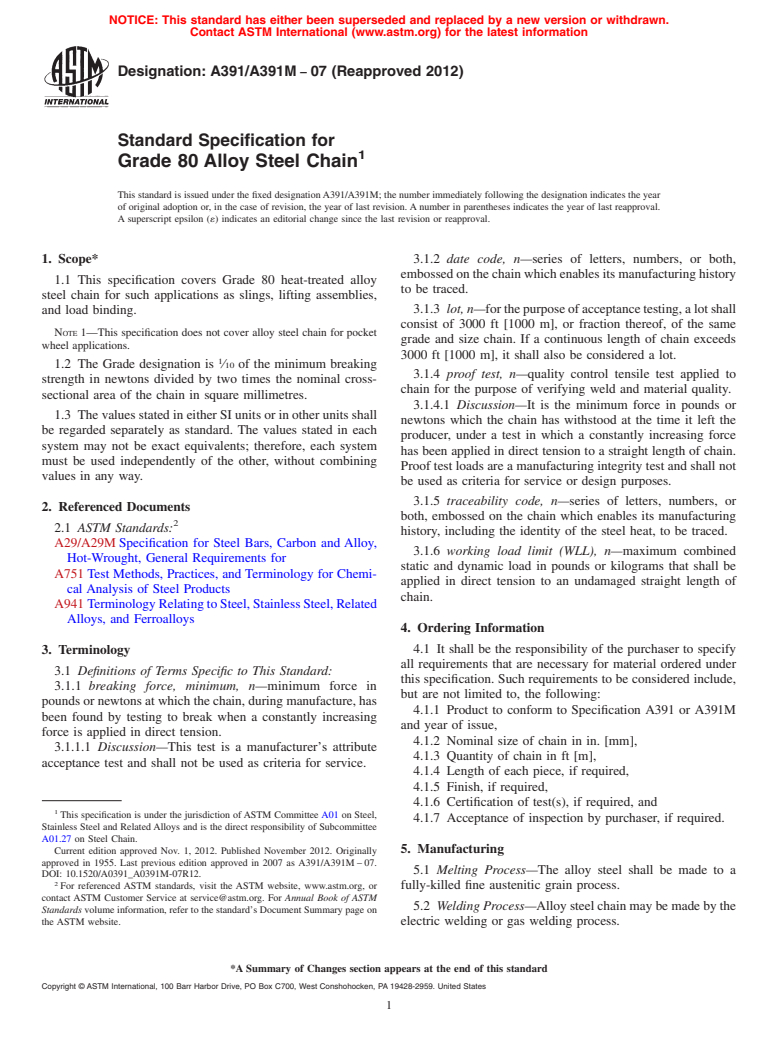
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:A391/A391M −07 (Reapproved 2012)
Standard Specification for
Grade 80 Alloy Steel Chain
This standard is issued under the fixed designationA391/A391M; the number immediately following the designation indicates the year
of original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.
A superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope* 3.1.2 date code, n—series of letters, numbers, or both,
embossedonthechainwhichenablesitsmanufacturinghistory
1.1 This specification covers Grade 80 heat-treated alloy
to be traced.
steel chain for such applications as slings, lifting assemblies,
and load binding. 3.1.3 lot,n—forthepurposeofacceptancetesting,alotshall
consist of 3000 ft [1000 m], or fraction thereof, of the same
NOTE 1—This specification does not cover alloy steel chain for pocket
grade and size chain. If a continuous length of chain exceeds
wheel applications.
3000 ft [1000 m], it shall also be considered a lot.
1.2 The Grade designation is ⁄10 of the minimum breaking
3.1.4 proof test, n—quality control tensile test applied to
strength in newtons divided by two times the nominal cross-
chain for the purpose of verifying weld and material quality.
sectional area of the chain in square millimetres.
3.1.4.1 Discussion—It is the minimum force in pounds or
1.3 ThevaluesstatedineitherSIunitsorinotherunitsshall
newtons which the chain has withstood at the time it left the
be regarded separately as standard. The values stated in each
producer, under a test in which a constantly increasing force
system may not be exact equivalents; therefore, each system
has been applied in direct tension to a straight length of chain.
must be used independently of the other, without combining
Proof test loads are a manufacturing integrity test and shall not
values in any way.
be used as criteria for service or design purposes.
3.1.5 traceability code, n—series of letters, numbers, or
2. Referenced Documents
both, embossed on the chain which enables its manufacturing
2.1 ASTM Standards:
history, including the identity of the steel heat, to be traced.
A29/A29MSpecification for Steel Bars, Carbon and Alloy,
3.1.6 working load limit (WLL), n—maximum combined
Hot-Wrought, General Requirements for
static and dynamic load in pounds or kilograms that shall be
A751Test Methods, Practices, and Terminology for Chemi-
applied in direct tension to an undamaged straight length of
cal Analysis of Steel Products
chain.
A941TerminologyRelatingtoSteel,StainlessSteel,Related
Alloys, and Ferroalloys
4. Ordering Information
4.1 It shall be the responsibility of the purchaser to specify
3. Terminology
all requirements that are necessary for material ordered under
3.1 Definitions of Terms Specific to This Standard:
this specification. Such requirements to be considered include,
3.1.1 breaking force, minimum, n—minimum force in
but are not limited to, the following:
poundsornewtonsatwhichthechain,duringmanufacture,has
4.1.1 Product to conform to Specification A391 or A391M
been found by testing to break when a constantly increasing
and year of issue,
force is applied in direct tension.
4.1.2 Nominal size of chain in in. [mm],
3.1.1.1 Discussion—This test is a manufacturer’s attribute
4.1.3 Quantity of chain in ft [m],
acceptance test and shall not be used as criteria for service.
4.1.4 Length of each piece, if required,
4.1.5 Finish, if required,
4.1.6 Certification of test(s), if required, and
This specification is under the jurisdiction ofASTM Committee A01 on Steel,
4.1.7 Acceptance of inspection by purchaser, if required.
Stainless Steel and RelatedAlloys and is the direct responsibility of Subcommittee
A01.27 on Steel Chain.
Current edition approved Nov. 1, 2012. Published November 2012. Originally 5. Manufacturing
approved in 1955. Last previous edition approved in 2007 as A391/A391M–07.
5.1 Melting Process—The alloy steel shall be made to a
DOI: 10.1520/A0391_A0391M-07R12.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or fully-killed fine austenitic grain process.
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
5.2 Welding Process—Alloysteelchainmaybemadebythe
Standards volume information, refer to the standard’s Document Summary page on
the ASTM website. electric welding or gas welding process.
*A Summary of Changes section appears at the end of this standard
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A391/A391M−07 (2012)
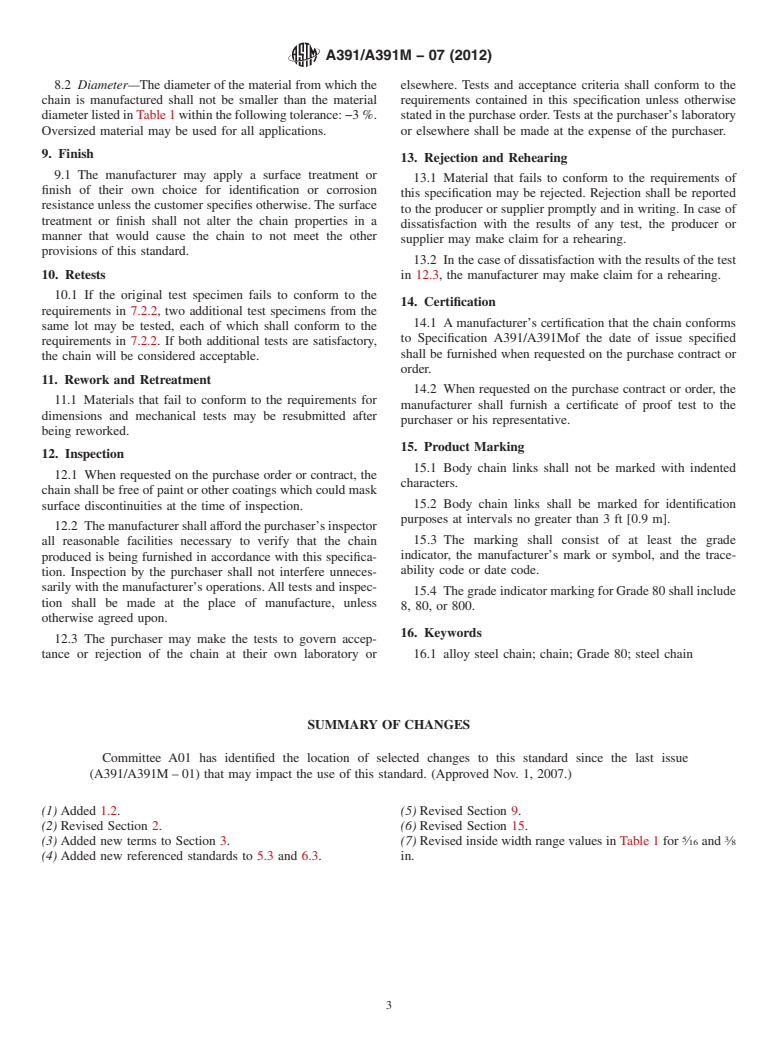
TABLE 2 Mechanical Test Sample Length Requirements
5.3 Heat Treatment—After welding, alloy steel chain shall
be heat treated before applying the proof test. Heat treatment Minimum Number of
Size of Chain Links
shall include quenching and tempering as defined by Termi-
in Test Specimen
nology A941.
⁄32 in. [5.5 mm] 9
Larger than ⁄32 in. [5.5 mm] 7
6. Material Requirements 3
but less than ⁄4 in. [20.0 mm]
⁄4 in. [20.0 mm] and larger 3
6.1 Heat Analysis—The selection and amounts of the alloy-
ing elements in the steel are left to the judgment of the
individual chain manufacturer provided the steel meets the
following criteria: Carbon: 0.35 % max.; Phosphorous:
0.025% max.; Sulfur: 0.025% max. Nickel must be present in
7.2.2 Test specimens shall meet or exceed the minimum
an alloying amount (0.40% min); and at least one of the breaking force values given in Table 1 for the appropriate size
following elements must be present in an alloying amount: chain.
Chromium (0.40% min) or Molybdenum (0.15% min).
7.3 Elongation:
6.2 Product Analysis—The steel used may be analyzed by 7.3.1 All chain must be in the quenched and tempered
the purchaser and shall conform to the requirements of 6.1 condition before the elongation is measured.
subject to the product analysis tolerances specified in Specifi- 7.3.2 The elongation test specimen shall consist of a length
cation A29/A29M.Test samples may be taken from rods, bars,
from the lot containing at least the number of links in Table 2.
or finished chain. Samples for analysis shall be so taken as to 7.3.3 A positive load not exceeding 10% of the proof test
represent the full cross section of the specimen.
shall be applied for determining the original gage length
(L{0}).
6.3 TestMethods,Practices,andTerminologyA751shallbe
7.3.4 The elongation shall be based on the total extension at
used for referee purposes.
fracture. This is expressed as a percentage of the change in
length (∆L) divided by the original gage length (L{0}). The
7. Mechanical Requirements
elongation may be determined by the equation below or by
7.1 Proof Test—Allchainshallbetestedtoatleasttheproof
autographic recorder or side scale.
loadprescribedinTable1fortheappropriatesizechain.When
Elongation ~%! 5 $∆L/L$0%% 3100
so tested it shall withstand these loads without loss of chain
integrity. Links or chain segments not withstanding the proof
where:
test load shall be removed from the chain.
∆L = test specimen final length at fracture – test specimen
7.2 Breaking Force—Thebreakingforcetestspecimenshall
original gage length (L{0}), and
consist of a length from the lot containing at least the number
L{0} = originalgagelength(sumortheinsidelengthsofthe
of links in Table 2. All chain shall be in the quenched and
test chain links, not coun
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.