


ASTM F1110-09(2014)
(Test Method)Standard Test Method for Sandwich Corrosion Test
Standard Test Method for Sandwich Corrosion Test
SIGNIFICANCE AND USE
5.1 The data generated by this test method shall be used to determine whether aircraft structural aluminum alloys are liable to be corroded or damaged by application of the test material during routine maintenance operations.
5.2 Interpretation of the sandwich corrosion test results is based on a comparison of the appearance of faying surfaces of three sets of coupons. One set of test coupons is exposed with reagent water only in the faying surfaces, to establish the baseline (controls) against which the panels exposed to the test material are compared. Disregard corrosion at cut edges of the test coupons.
5.3 The relative corrosion severity rating system is provided in order to allow a numerical classification of the test results and to eliminate the necessity for elaborate weight loss measurements. Pitting corrosion, which is rated 4—extensive (severe) corrosion, may involve only a negligible weight loss.
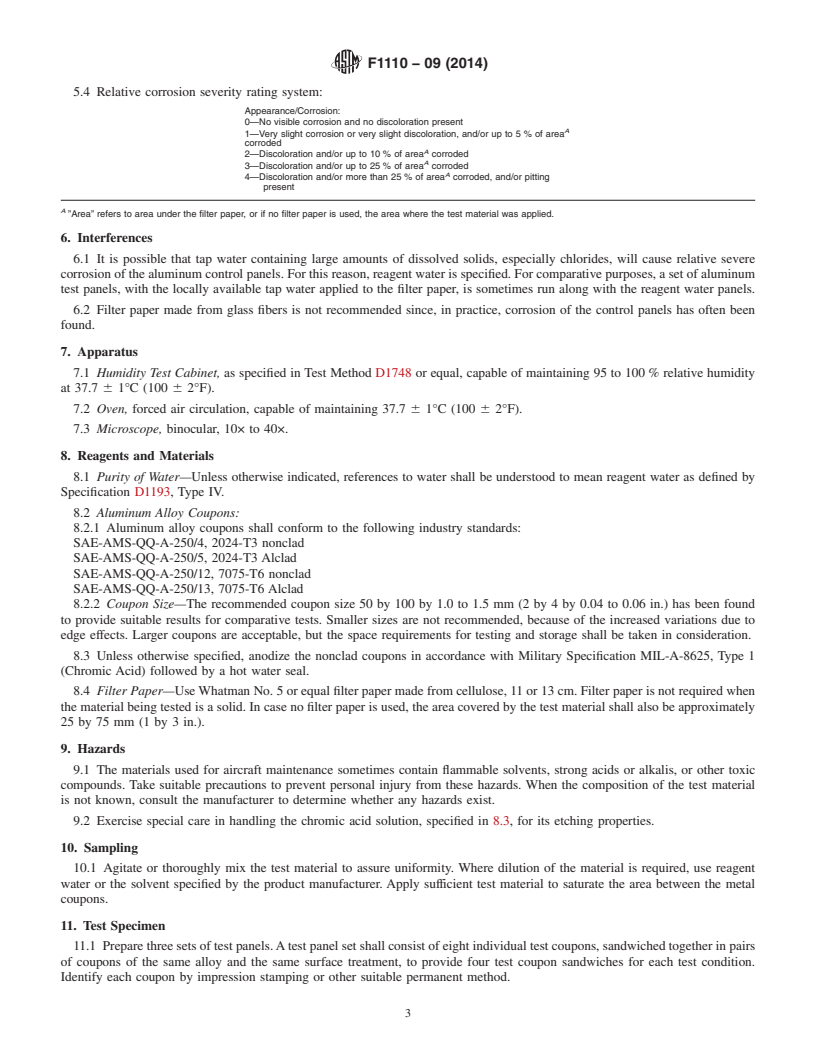
5.4 Relative corrosion severity rating system:
Appearance/Corrosion:
0—No visible corrosion and no discoloration present
1—Very slight corrosion or very slight discoloration, and/or up to 5 % of areaA corroded
2—Discoloration and/or up to 10 % of areaA corroded
3—Discoloration and/or up to 25 % of areaA corroded
4—Discoloration and/or more than 25 % of areaA corroded, and/or pitting
present (A) ”Area” refers to area under the filter paper, or if no filter paper is used, the area where the test material was applied.
SCOPE
1.1 This test method defines the procedure for evaluating the corrosivity of aircraft maintenance chemicals, when present between faying surfaces (sandwich) of aluminum alloys commonly used for aircraft structures. This test method is intended to be used in the qualification and approval of compounds employed in aircraft maintenance operations.
1.2 The values stated in SI units are to be regarded as the standard. The values given in parentheses are for information.
1.3 This standard may involve hazardous materials, operations, and equipment. This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use. Specific hazard statements appear in Section 9.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: F1110 − 09 (Reapproved 2014)
Standard Test Method for
Sandwich Corrosion Test
This standard is issued under the fixed designation F1110; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope 2.3 Military Specification:
MIL-A-8625AnodicCoatingsforAluminumandAlAlloys
1.1 This test method defines the procedure for evaluating
thecorrosivityofaircraftmaintenancechemicals,whenpresent
3. Terminology
between faying surfaces (sandwich) of aluminum alloys com-
3.1 Definitions of Terms Specific to This Standard:
monlyusedforaircraftstructures.Thistestmethodisintended
3.1.1 sandwich corrosion test—a comparative accelerated
to be used in the qualification and approval of compounds
environmentaltestofthecorrosivityofliquidorsolidmaterials
employed in aircraft maintenance operations.
present between faying surfaces of structural aluminum alloys
1.2 The values stated in SI units are to be regarded as the
commonly used in aerospace construction.
standard. The values given in parentheses are for information.
4. Summary of Test Method
1.3 This standard may involve hazardous materials,
operations, and equipment. This standard does not purport to
4.1 Aluminum coupons having clad or anodized nonclad
address all of the safety concerns, if any, associated with its
surfaces are sandwiched together with a filter paper saturated
use. It is the responsibility of the user of this standard to
with the test material between the coupons. The sandwiched
establish appropriate safety and health practices and deter-
coupons are cycled between warm ambient air and warm
mine the applicability of regulatory limitations prior to use.
humid air for 7 days. The coupons are then inspected to
Specific hazard statements appear in Section 9.
determine whether corrosion more severe than that caused by
reagent water has occurred on the surfaces exposed to the test
2. Referenced Documents
material.This test method is used for solutions of dry granular
2.1 ASTM Standards:
material or for liquid materials.
D1193Specification for Reagent Water
5. Significance and Use
D1748Test Method for Rust Protection by Metal Preserva-
tives in the Humidity Cabinet
5.1 The data generated by this test method shall be used to
G46Guide for Examination and Evaluation of Pitting Cor-
determine whether aircraft structural aluminum alloys are
rosion
liable to be corroded or damaged by application of the test
2.2 Industry Standards:
material during routine maintenance operations.
SAE-AMS-QQ-A-250/4Al Alloy 2024, Plate and Sheet
5.2 Interpretation of the sandwich corrosion test results is
SAE-AMS-QQ-A-250/5Al Alloy Alclad 2024, Plate and
based on a comparison of the appearance of faying surfaces of
Sheet
three sets of coupons. One set of test coupons is exposed with
SAE-AMS-QQ-A-250/12Al Alloy 7075, Plate and Sheet
reagent water only in the faying surfaces, to establish the
SAE-AMS-QQ-A-250/13Al Alloy Alclad 7075, Plate and
baseline(controls)againstwhichthepanelsexposedtothetest
Sheet
material are compared. Disregard corrosion at cut edges of the
test coupons.
This test method is under the jurisdiction of ASTM Committee F07 on
5.3 Therelativecorrosionseverityratingsystemisprovided
Aerospace andAircraft and is the direct responsibility of Subcommittee F07.07 on
in order to allow a numerical classification of the test results
Qualification Testing of Aircraft Cleaning Materials.
Current edition approved Dec. 1, 2014. Published December 2014. Originally
and to eliminate the necessity for elaborate weight loss
approved in 1986. Last previous edition approved in 2009 as F1110–09. DOI:
measurements. Pitting corrosion, which is rated 4—extensive
10.1520/F1110-09R14.
(severe) corrosion, may involve only a negligible weight loss.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
Standards volume information, refer to the standard’s Document Summary page on
the ASTM website.
3 4
Available from Society of Automotive Engineers (SAE), 400 Commonwealth Available from Department of Defense Single Stock Point (DODSSP); http://
Dr., Warrendale, PA 15096-0001. dodssp.daps.dla.mil
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
F1110 − 09 (2014)
5.4 Relative corrosion severity rating system: 9. Hazards
Appearance/Corrosion:
9.1 The materials used for aircraft maintenance sometimes
0—No visible corrosion and no discoloration present
contain flammable solvents, strong acids or alkalis, or other
A
1—Very slight corrosion or very slight discoloration, and/or up to 5 % of area
corroded
toxiccompounds.Takesuitableprecautionstopreventpersonal
A
2—Discoloration and/or up to 10 % of area corroded
injury from these hazards. When the composition of the test
A
3—Discoloration and/or up to 25 % of area corroded
A
material is not known, consult the manufacturer to determine
4—Discoloration and/or more than 25 % of area corroded, and/or pitting
present
whether any hazards exist.
A
9.2 Exercise special care in handling the chromic acid
”Area” refers to area under the filter paper, or if no filter paper is used, the area
where the test material was applied.
solution, specified in 8.3, for its etching properties.
6. Interferences
10. Sampling
6.1 It is possible that tap water containing large amounts of
10.1 Agitate or thoroughly mix the test material to assure
dissolvedsolids,especiallychlorides,willcauserelativesevere
uniformity. Where dilution of the material is required, use
corrosion of the aluminum control panels. For this reason,
reagent water or the solvent specified by the product manufac-
reagent water is specified. For comparative purposes, a set of
turer.Applysufficienttestmaterialtosaturatetheareabetween
aluminum test panels, with the locally available tap water
the metal coupons.
applied to the filter paper, is sometimes run along with the
reagent water panels.
11. Test Specimen
6.2 Filter paper made from glass fibers is not recommended
11.1 Prepare three sets of test panels. A test panel set shall
since,inpractice,corrosionofthecontrolpanelshasoftenbeen
consistofeightindividualtestcoupons,sandwichedtogetherin
found.
pairs of coupons of the same alloy and the same surface
treatment,toprovidefourtestcouponsandwichesforeachtest
7. Apparatus
condition. Identify each coupon by impression stamping or
7.1 Humidity Test Cabinet, as specified in Test Method
other suitable permanent method.
D1748 or equal, capable of maintaining 95 to 100% relative
11.2 Clean the panels by solvent wiping, or vapor degreas-
humidity at 37.7 6 1°C (100 6 2°F).
ing. Do not use acid or caustic cleaners. Remove ink stamped
7.2 Oven,forcedaircirculation,capableofmaintaining37.7
markings from the panels. Do not use abrasive materials to
6 1°C (100 6 2°F).
clean the panels.
7.3 Microscope, binocular, 10× to 40×.
11.3 Prepare the test panel sets as follows for each alloy:
11.3.1 Onesetforthecompoundtobetestedatusedilution,
8. Reagents and Materials
11.3.2 One set for the compound to be tested in concen-
8.1 Purity of Water—Unless otherwise indicated, references
trated form and
to water shall be understood to mean reagent water as defined
11.3.3 One set for controls using reagent water.
by Specification D1193, Type IV.
12. Preparation of Apparatus
8.2 Aluminum Alloy Coupons:
8.2.1 Aluminum alloy coupons shall conform to the follow-
12.1 Verify that the humidity cabinet is operating at the
ing in
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: F1110 − 09 F1110 − 09 (Reapproved 2014)
Standard Test Method for
Sandwich Corrosion Test
This standard is issued under the fixed designation F1110; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
1. Scope
1.1 This test method defines the procedure for evaluating the corrosivity of aircraft maintenance chemicals, when present
between faying surfaces (sandwich) of aluminum alloys commonly used for aircraft structures. This test method is intended to be
used in the qualification and approval of compounds employed in aircraft maintenance operations.
1.2 The values stated in SI units are to be regarded as the standard. The values given in parentheses are for information.
1.3 This standard may involve hazardous materials, operations, and equipment. This standard does not purport to address all
of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate
safety and health practices and determine the applicability of regulatory limitations prior to use. Specific hazard statements appear
in Section 9.
2. Referenced Documents
2.1 ASTM Standards:
D1193 Specification for Reagent Water
D1748 Test Method for Rust Protection by Metal Preservatives in the Humidity Cabinet
G46 Guide for Examination and Evaluation of Pitting Corrosion
2.2 Industry Standards:
SAE-AMS-QQ-A-250/4 Al Alloy 2024, Plate and Sheet
SAE-AMS-QQ-A-250/5 Al Alloy Alclad 2024, Plate and Sheet
SAE-AMS-QQ-A-250/12 Al Alloy 7075, Plate and Sheet
SAE-AMS-QQ-A-250/13 Al Alloy Alclad 7075, Plate and Sheet
2.3 Military Specification:
MIL-A-8625 Anodic Coatings for Aluminum and Al Alloys
3. Terminology
3.1 Definitions of Terms Specific to This Standard:
3.1.1 sandwich corrosion test—a comparative accelerated environmental test of the corrosivity of liquid or solid materials
present between faying surfaces of structural aluminum alloys commonly used in aerospace construction.
4. Summary of Test Method
4.1 Aluminum coupons having clad or anodized nonclad surfaces are sandwiched together with a filter paper saturated with the
test material between the coupons. The sandwiched coupons are cycled between warm ambient air and warm humid air for 7 days.
The coupons are then inspected to determine whether corrosion more severe than that caused by reagent water has occurred on
the surfaces exposed to the test material. This test method is used for solutions of dry granular material or for liquid materials.
This test method is under the jurisdiction of ASTM Committee F07 on Aerospace and Aircraft and is the direct responsibility of Subcommittee F07.07 on Qualification
Testing of Aircraft Cleaning Materials.
Current edition approved May 15, 2009Dec. 1, 2014. Published June 2009December 2014. Originally approved in 1986. Last previous edition approved in 20082009 as
F1110 – 08.F1110 – 09. DOI: 10.1520/F1110-09.10.1520/F1110-09R14.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Available from Society of Automotive Engineers (SAE), 400 Commonwealth Dr., Warrendale, PA 15096-0001.
Available from Department of Defense Single Stock Point (DODSSP); http://dodssp.daps.dla.mil
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
F1110 − 09 (2014)
5. Significance and Use
5.1 The data generated by this test method shall be used to determine whether aircraft structural aluminum alloys are liable to
be corroded or damaged by application of the test material during routine maintenance operations.
5.2 Interpretation of the sandwich corrosion test results is based on a comparison of the appearance of faying surfaces of three
sets of coupons. One set of test coupons is exposed with reagent water only in the faying surfaces, to establish the baseline
(controls) against which the panels exposed to the test material are compared. Disregard corrosion at cut edges of the test coupons.
5.3 The relative corrosion severity rating system is provided in order to allow a numerical classification of the test results and
to eliminate the necessity for elaborate weight loss measurements. Pitting corrosion, which is rated 4—extensive (severe)
corrosion, may involve only a negligible weight loss.
F1110 − 09 (2014)
5.4 Relative corrosion severity rating system:
Appearance/Corrosion:
0—No visible corrosion and no discoloration present
A
1—Very slight corrosion or very slight discoloration, and/or up to 5 % of area
corroded
A
2—Discoloration and/or up to 10 % of area corroded
A
3—Discoloration and/or up to 25 % of area corroded
A
4—Discoloration and/or more than 25 % of area corroded, and/or pitting
present
A
”Area” refers to area under the filter paper, or if no filter paper is used, the area where the test material was applied.
6. Interferences
6.1 It is possible that tap water containing large amounts of dissolved solids, especially chlorides, will cause relative severe
corrosion of the aluminum control panels. For this reason, reagent water is specified. For comparative purposes, a set of aluminum
test panels, with the locally available tap water applied to the filter paper, is sometimes run along with the reagent water panels.
6.2 Filter paper made from glass fibers is not recommended since, in practice, corrosion of the control panels has often been
found.
7. Apparatus
7.1 Humidity Test Cabinet, as specified in Test Method D1748 or equal, capable of maintaining 95 to 100 % relative humidity
at 37.7 6 1°C (100 6 2°F).
7.2 Oven, forced air circulation, capable of maintaining 37.7 6 1°C (100 6 2°F).
7.3 Microscope, binocular, 10× to 40×.
8. Reagents and Materials
8.1 Purity of Water—Unless otherwise indicated, references to water shall be understood to mean reagent water as defined by
Specification D1193, Type IV.
8.2 Aluminum Alloy Coupons:
8.2.1 Aluminum alloy coupons shall conform to the following industry standards:
SAE-AMS-QQ-A-250/4, 2024-T3 nonclad
SAE-AMS-QQ-A-250/5, 2024-T3 Alclad
SAE-AMS-QQ-A-250/12, 7075-T6 nonclad
SAE-AMS-QQ-A-250/13, 7075-T6 Alclad
8.2.2 Coupon Size—The recommended coupon size 50 by 100 by 1.0 to 1.5 mm (2 by 4 by 0.04 to 0.06 in.) has been found
to provide suitable results for comparative tests. Smaller sizes are not recommended, because of the increased variations due to
edge effects. Larger coupons are acceptable, but the space requirements for testing and storage shall be taken in consideration.
8.3 Unless otherwise specified, anodize the nonclad coupons in accordance with Military Specification MIL-A-8625, Type 1
(Chromic Acid) followed by a hot water seal.
8.4 Filter Paper—Use Whatman No. 5 or equal filter paper made from cellulose, 11 or 13 cm. Filter paper is not required when
the material being tested is a solid. In case no filter paper is used, the area covered by the test material shall also be approximately
25 by 75 mm (1 by 3 in.).
9. Hazards
9.1 The materials used for aircraft maintenance sometimes contain flammable solvents, strong acids or alkalis, or other toxic
compounds. Take suitable precautions to prevent personal injury from these hazards. When the composition of the test material
is not known, consult the manufacturer to determine whether any hazards exist.
9.2 Exercise special care in handling the chromic acid solution, specified in 8.3, for its etching properties.
10. Sampli
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.