


ASTM E674-12(2016)
(Specification)Standard Specification for Industrial Perforated Plate and Screens (Round Opening Series)
Standard Specification for Industrial Perforated Plate and Screens (Round Opening Series)
ABSTRACT
This specification covers the various sizes of round opening perforated plates and screens for general industrial uses, including the separating or grading of materials according to designated nominal particle size, and lists standards for openings punched with various bar sizes and thicknesses of plate for various grades of service. This specification does not apply to perforated plates or screens with square, hexagon, slotted, or other shaped openings.
SCOPE
1.1 This specification covers the sizes of round opening perforated plate and screens for general industrial uses, including the separating or grading of materials according to designated nominal particle size, and lists standards for openings from 5 in. (125 mm) to 0.020 in. (500 μm) punched with bar sizes and thicknesses of plate for various grades of service. Methods of checking industrial perforated plate and screens are included as information in Appendix X3.
1.2 This specification does not apply to perforated plate or screens with square, hexagon, slotted, or other shaped openings.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical conversions to SI units that are provided for information only and are not considered standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:E674 −12 (Reapproved 2016)
Standard Specification for
Industrial Perforated Plate and Screens (Round Opening
Series)
This standard is issued under the fixed designation E674; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
INTRODUCTION
Industrial perforated plate can be produced in many thousands of combinations of size and shape
of opening, bar size, thickness of material, and type of metal. Such variety is often confusing and, to
the vast majority of perforated plate users, unnecessary, since each usually requires only a very few
specifications.
The purpose of this specification is to simplify this problem by a condensed table of recommended
specifications covering a wide range of openings in which industrial perforated plate is made, with
several recommended bar sizes and thicknesses of plate for each opening, for use in various grades of
service.
By making selections from this specification, the user will be guided to specifications that are being
regularly produced, thus avoiding inadvertent selection of specifications that, because of little or no
demand,areunobtainable,exceptonspecialorder(usuallyquiteexpensiveunlessthequantityordered
is sufficient to justify the cost of special tooling).
Ifauserhasaspecificapplicationforindustrialperforatedplatethatcannotbesolvedbyaselection
from this specification, it is recommended that he consult his perforated plate supplier on the
availability of an acceptable alternative specification.
1. Scope 1.4 This standard does not purport to address all of the
safety concerns, if any, associated with its use. It is the
1.1 This specification covers the sizes of round opening
responsibility of the user of this standard to establish appro-
perforated plate and screens for general industrial uses, includ-
priate safety and health practices and determine the applica-
ing the separating or grading of materials according to desig-
bility of regulatory limitations prior to use.
nated nominal particle size, and lists standards for openings
from 5 in. (125 mm) to 0.020 in. (500 µm) punched with bar
2. Referenced Documents
sizes and thicknesses of plate for various grades of service.
2.1 ASTM Standards:
Methodsofcheckingindustrialperforatedplateandscreensare
E323 Specification for Perforated-Plate Sieves for Testing
included as information in Appendix X3.
Purposes
1.2 This specification does not apply to perforated plate or
E1638 Terminology Relating to Sieves, Sieving Methods,
screens with square, hexagon, slotted, or other shaped open-
and Screening Media
ings. 3
2.2 ISO Standards:
1.3 The values stated in inch-pound units are to be regarded ISO 2194 Industrial screens —Woven wire cloth, perforated
as standard. The values given in parentheses are mathematical plate and electroformed sheet — Designation and nominal
conversions to SI units that are provided for information only sizes of openings
and are not considered standard.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
ThisspecificationisunderthejurisdictionofASTMCommitteeE29onParticle contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
and Spray Characterization and is the direct responsibility of Subcommittee E29.01 Standards volume information, refer to the standard’s Document Summary page on
on Sieves, Sieving Methods, and Screening Media. the ASTM website.
Current edition approved July 1, 2016. Published July 2016. Originally approved Available from International Organization for Standardization (ISO), 1, ch. de
in 1979. Last previous edition approved in 2012 as E674 – 12. DOI: 10.1520/ la Voie-Creuse, Case postale 56, CH-1211, Geneva 20, Switzerland, http://
E0674-12R16. www.iso.ch.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
E674−12 (2016)
2.3 Other Documents: 3.2.11 perforated pattern, n—the patterns that the perfora-
Fed. Std. 123 Marking for Shipments (Civil Agencies) tions are arranged in, usually in a staggered pattern with
Mil-Std-129 Marking for Shipment and Storage midpoints nominally at the vertices of isosceles triangles or
square patterns arranged in line with their midpoints nominally
3. Terminology
at the vertices of squares.
3.1 Definitions—For general terms related to sieves, sieving 3.2.12 screen, n—(1) surface provided with apertures of
methods, and screening media, see Terminology E1638. uniform size and shape; (2) another term used interchangeably
3.2 Definitions of Terms Specific to This Standard: for woven wire cloth; (3) machine provided with one or more
3.2.1 aperture, n—the opening in a screening or sieving screen surfaces.
medium.
3.2.13 screening, v—process of separating a mixture of
3.2.2 bar, n—the metal between perforations. different sizes by means of one or more screen surfaces.
3.2.14 smooth side or punch side, n—surface of the plate
3.2.3 blank, n—unperforated area located other than along
that was uppermost during the punching operation and through
the perimeter of a plate.
which the punch entered the plate.
3.2.4 break-out, n—term applied to the action that occurs
3.2.15 unfinished end pattern, n—condition that occurs with
ahead of the punch in its going through the plate.
somespecificationsofstaggeredpatternperforationsasaresult
3.2.4.1 Discussion—The fracturing of the material results in
of tool design.
a tapered hole with the small dimensions on the punch side.
3.2.15.1 Discussion—On one end of the plate, the pattern
3.2.5 centers, n—dimensional sum of one perforation and
will appear to be incomplete as a result of unperforated holes
one bar or the dimensional distance from the center of one
in the even numbered rows, while on the other end of the same
perforation to the center of an adjacent perforation.
plate, the pattern will appear to be incomplete because of
3.2.6 die side, n—surface of the plate that was against the
unperforated holes in the odd numbered rows (Fig. 2).
die during the punching operation.
4. Standard Specifications
3.2.7 finished end pattern, n—condition that occurs with
4.1 Standard specifications for industrial perforated plate
somespecificationsofstaggeredpatternperforationsasaresult
and screens are listed in Table 1.
of tool design in which the pattern is completed on both ends
of the plate (Fig. 1).
4.2 Openings—The series of standard openings listed in
Table 1 include those of the USA Standard Sieve Series,
3.2.8 gage (also gauge), n—a number designating a specific
Specification E323, and those of the ISO apertures for indus-
thicknessofmetalsheettabulatedinastandardizedseries,each
trial plate screens, ISO 2194, with the addition of those
of which represents a decimal fraction of an inch.
openings in common usage.
3.2.9 margin or border, n—unperforated area located along
4.3 Relationship of Grades—The purpose of the several
the perimeter of a plate.
grades is to provide combinations of opening and bar size for
3.2.10 percent open area, n—theratioofthetotalareaofthe
various types of service, from medium-light to heavy. Since it
apertures to the total area expressed in percentage.
is possible to vary the bar size independently from the plate
thickness, each of the service grades lists up to three combi-
nations of bar and gage for each opening. The entire standard
Available from Standardization Documents Order Desk, DODSSP, Bldg. 4,
series has been designed for a logical relationship of bar size to
Section D, 700 Robbins Ave., Philadelphia, PA 19111-5098, http://
opening in each grade and between grades with the capability
dodssp.daps.dla.mil.
of also being able to vary the plate thickness.
FIG. 1 Finished End Pattern FIG. 2 Unfinished End Pattern
E674−12 (2016)
TABLE 1 USA Standard Specifications for Industrial Perforated Plate and Screens (Round Opening Series)—(U.S. Customary Units)
Perforated
Medium Light Medium Medium Heavy Heavy
Opening
USA
Stan- Indus-
Open- Gage- Open Open- Gage- Open Open- Gage- Open Open- Gage- Open
dard trial Bar, Bar, Bar, Bar,
ing, Steel, Area, ing, Steel, Area, ing, Steel, Area, ing, Steel, Area,
(metric), Stan- in. in. in. in.
in. in. % in. in. % in. in. % in. in. %
mm dard,
in.
1 1 5 5 3 3
125 5 5 ⁄2 ⁄2 74.9 5 ⁄8 ⁄8 71.6 5 ⁄4 ⁄4 68.5 5 1 1 62.9
5 3 3 1 7 5 1 7
125 5 5 ⁄8 ⁄8 71.6 5 ⁄4 ⁄2 68.5 5 ⁄8 ⁄8 65.6 5 1 ⁄8 ⁄8 60.4
5 1 3 5 7 3 1
125 5 5 ⁄8 ⁄2 71.6 5 ⁄4 ⁄8 68.5 5 ⁄8 ⁄4 65.6 5 1 ⁄8 1 60.4
1 1 1 1 5 5 1 3 3 1
... ... 4 ⁄2 ⁄2 ⁄2 73.4 4 ⁄2 ⁄8 ⁄8 69.9 4 ⁄2 ⁄4 ⁄4 66.6 4 ⁄2 1 1 60.7
1 5 3 1 3 1 1 7 5 1 1 7
... ... 4 ⁄2 ⁄8 ⁄8 69.9 4 ⁄2 ⁄4 ⁄2 66.6 4 ⁄2 ⁄8 ⁄8 63.5 4 ⁄2 1 ⁄8 ⁄8 58
1 5 1 1 3 5 1 7 3 1 1
... ... 4 ⁄2 ⁄8 ⁄2 69.9 4 ⁄2 ⁄4 ⁄8 66.6 4 ⁄2 ⁄8 ⁄4 63.5 4 ⁄2 1 ⁄8 158
1 1 1 1 1 5 5 1 3 3 1
106 4 ⁄4 4 ⁄4 ⁄2 ⁄2 72.6 4 ⁄4 ⁄8 ⁄8 68.9 4 ⁄4 ⁄4 ⁄4 65.5 4 ⁄4 1 1 59.4
1 1 5 3 1 3 1 1 7 5 1 1 7
106 4 ⁄4 4 ⁄4 ⁄8 ⁄8 68.9 4 ⁄4 ⁄4 ⁄2 65.5 4 ⁄4 ⁄8 ⁄8 62.3 4 ⁄4 1 ⁄8 ⁄8 56.7
1 1 5 1 1 3 5 1 7 3 1 1
106 4 ⁄4 4 ⁄4 ⁄8 ⁄2 68.9 4 ⁄4 ⁄4 ⁄8 65.5 4 ⁄4 ⁄8 ⁄4 62.3 4 ⁄4 1 ⁄8 1 56.7
1 1 5 5 3 3
100 4 4 ⁄2 ⁄2 71.6 4 ⁄8 ⁄8 67.8 4 ⁄4 ⁄4 64.3 41158
5 3 3 1 7 5 1 7
100 4 4 ⁄8 ⁄8 67.8 4 ⁄4 ⁄2 64.3 4 ⁄8 ⁄8 61 4 1 ⁄8 ⁄8 55.2
5 1 3 5 7 3 1
100 4 4 ⁄8 ⁄2 67.8 4 ⁄4 ⁄8 64.3 4 ⁄8 ⁄4 61 4 1 ⁄8 1 55.2
3 1 1 3 5 5 3 3 3 3 7 7
... ... 3 ⁄4 ⁄2 ⁄2 70.6 3 ⁄4 ⁄8 ⁄8 66.6 3 ⁄4 ⁄4 ⁄4 62.9 3 ⁄4 ⁄8 ⁄8 59.6
3 5 3 3 3 1 3 7 5 3 3
... ... 3 ⁄4 ⁄8 ⁄8 66.6 3 ⁄4 ⁄4 ⁄2 62.9 3 ⁄4 ⁄8 ⁄8 59.6 3 ⁄4 1 ⁄4 48.9
3 5 1 3 3 5 3 7 3 3 7
... ... 3 ⁄4 ⁄8 ⁄2 66.6 3 ⁄4 ⁄4 ⁄8 62.9 3 ⁄4 ⁄8 ⁄4 59.6 3 ⁄4 1 ⁄8 48.9
1 1 1 1 1 5 5 1 3 3 1 7 7
90 3 ⁄2 3 ⁄2 ⁄2 ⁄2 69.4 3 ⁄2 ⁄8 ⁄8 65.2 3 ⁄2 ⁄4 ⁄4 61.5 3 ⁄2 ⁄8 ⁄8 58
1 1 5 3 1 3 1 1 7 5 1 3
90 3 ⁄2 3 ⁄2 ⁄8 ⁄8 65.2 3 ⁄2 ⁄4 ⁄2 61.5 3 ⁄2 ⁄8 ⁄8 58 3 ⁄2 1 ⁄4 54.8
1 1 5 1 1 3 5 1 7 3 1 7
90 3 ⁄2 3 ⁄2 ⁄8 ⁄2 65.2 3 ⁄2 ⁄4 ⁄8 61.5 3 ⁄2 ⁄8 ⁄4 58 3 ⁄2 1 ⁄8 54.8
1 3 3 1 1 1 1 5 5 1 3 3
... ... 3 ⁄4 ⁄8 ⁄8 72.8 3 ⁄4 ⁄2 ⁄2 68.1 3 ⁄4 ⁄8 ⁄8 63.8 3 ⁄4 ⁄4 ⁄4 59.8
1 1 5 1 5 3 1 3 1 1 7 5
... ... 3 ⁄4 ⁄2 ⁄16 68.1 3 ⁄4 ⁄8 ⁄8 63.7 3 ⁄4 ⁄4 ⁄2 59.8 3 ⁄4 ⁄8 ⁄8 56.2
1 1 3 1 5 1 1 3 5 1 7 3
... ... 3 ⁄4 ⁄2 ⁄8 68.1 3 ⁄4 ⁄8 ⁄2 63.7 3 ⁄4 ⁄4 ⁄8 59.8 3 ⁄4 ⁄8 ⁄4 56.2
3 3 1 1 5 5 3 3
75 3 3 ⁄8 ⁄8 71.6 3 ⁄2 ⁄2 66.6 3 ⁄8 ⁄8 62.1 3 ⁄4 ⁄4 58
1 5 5 3 3 1 7 5
75 3 3 ⁄2 ⁄16 66.6 3 ⁄8 ⁄8 62.1 3 ⁄4 ⁄2 58 3 ⁄8 ⁄8 54.3
1 3 5 1 3 5 7 3
75 3 3 ⁄2 ⁄8 66.6 3 ⁄8 ⁄2 62.1 3 ⁄4 ⁄8 58 3 ⁄8 ⁄4 54.3
3 3 3 3 1 1 3 5 5 3 3 3
... ... 2 ⁄4 ⁄8 ⁄8 70.2 2 ⁄4 ⁄2 ⁄2 64.9 2 ⁄4 ⁄8 ⁄8 60.2 2 ⁄4 ⁄4 ⁄4 55.9
3 1 5 3 5 3 3 3 1 3 7 5
... ... 2 ⁄4 ⁄2 ⁄16 64.9 2 ⁄4 ⁄8 ⁄8 60.2 2 ⁄4 ⁄4 ⁄2 55.9 2 ⁄4 ⁄8 ⁄8 52.1
3 1 3 3 5 1 3 3 5 3 7 3
... ... 2 ⁄4 ⁄2 ⁄8 64.9 2 ⁄4 ⁄8 ⁄2 60.2 2 ⁄4 ⁄4 ⁄8 55.9 2 ⁄4 ⁄8 ⁄4 52.1
1 1 3 3 1 1 1 1 5 5 1 3 3
63 2 ⁄2 2 ⁄2 ⁄8 ⁄8 68.5 2 ⁄2 ⁄2 ⁄2 62.9 2 ⁄2 ⁄8 ⁄8 58 2 ⁄2 ⁄4 ⁄4 53.6
1 1 1 5 1 5 3 1 3 1 1 7 5
63 2 ⁄2 2 ⁄2 ⁄2 ⁄16 62.9 2 ⁄2 ⁄8 ⁄8 58 2 ⁄2 ⁄4 ⁄2 53.6 2 ⁄2 ⁄8 ⁄8 49.7
1 1 1 3 1 5 1 1 3 5 1 7 3
63 2 ⁄2 2 ⁄2 ⁄2 ⁄8 62.9 2 ⁄2 ⁄8 ⁄2 58 2 ⁄2 ⁄4 ⁄8 53.6 2 ⁄2 ⁄8 ⁄4 49.7
1 3 3 1 1 1 1 5 5 1 3 3
... ... 2 ⁄4 ⁄8 ⁄8 66.6 2 ⁄4 ⁄2 ⁄2 60.7 2 ⁄4 ⁄8 ⁄8 55.5 2 ⁄4 ⁄4 ⁄4 51
1 1 5 1 5 3 1 3 1 1 7 5
... ... 2 ⁄4 ⁄2 ⁄16 60.7 2 ⁄4 ⁄8 ⁄8 55.5 2 ⁄4 ⁄4 ⁄2 51 2 ⁄4 ⁄8 ⁄8 47
1 1 3 1 5 1 1 3 5 1 7 3
... ... 2 ⁄4 ⁄2 ⁄8 60.7 2 ⁄4 ⁄8 ⁄2 55.5 2 ⁄4 ⁄4 ⁄8 51 2 ⁄4 ⁄8 ⁄4 47
1 1 5 5 1 3 3 1 1 1 1 5 5
53 2 ⁄8 2 ⁄8 ⁄16 ⁄16 68.9 2 ⁄8 ⁄8 ⁄8 65.5 2 ⁄8 ⁄2 ⁄2 59.4 2 ⁄8 ⁄8 ⁄8 54.1
1 1 3 1 1 1 5 1 5 3 1 3 1
53 2 ⁄8 2 ⁄8 ⁄8 ⁄4 65.5 2 ⁄8 ⁄2 ⁄16 59.4 2 ⁄8 ⁄8 ⁄8 54.1 2 ⁄8 ⁄4 ⁄2 49.5
1 1 3 5 1 1 3 1 5 1 1 3 5
53 2 ⁄8 2 ⁄8 ⁄8 ⁄16 65.5 2 ⁄8 ⁄2 ⁄8 59.4 2 ⁄8 ⁄8 ⁄2 54.1 2 ⁄8 ⁄4 ⁄8 49.5
5 5 3 3 1 1 5 5
50 2 2 ⁄16 ⁄16 67.8 2 ⁄8 ⁄8 64.3 2 ⁄2 ⁄2 58 2 ⁄8 ⁄8 52.6
3 1 1 5 5 3 3 1
50 2 2 ⁄8 ⁄4 64.3 2 ⁄2 ⁄16 58 2 ⁄8 ⁄8 52.6 2 ⁄4 ⁄2 47.9
3 5 1 3 5 1 3 5
50 2 2 ⁄8 ⁄16 64.3 2 ⁄2 ⁄8 58 2 ⁄8 ⁄2 52.6 2 ⁄4 ⁄8 47.9
7 5 5 7 3 3 7 1 1 7 5 5
... ... 1 ⁄8 ⁄16 ⁄16 66.6 1 ⁄8 ⁄8 ⁄8 62.9 1 ⁄8 ⁄2 ⁄2 56.5 1 ⁄8 ⁄8 ⁄8 51
7 3 1 7 1 5 7 5 3 7 3 1
... ... 1 ⁄8 ⁄8 ⁄4 62.9 1 ⁄8 ⁄2 ⁄16 56.5 1 ⁄8 ⁄8 ⁄8 51 1 ⁄8 ⁄4 ⁄2 46.2
7 3 5 7 1 3 7 5 1 7 3 5
... ... 1 ⁄8 ⁄8 ⁄16 62.9 1 ⁄8 ⁄2 ⁄8 56.5 1 ⁄8 ⁄8 ⁄2 51 1 ⁄8 ⁄4 ⁄8 46.2
3 3 5 5 3 3 3 3 1 1 3 5 5
45 1 ⁄4 1 ⁄4 ⁄16 ⁄16 65.2 1 ⁄4 ⁄8 ⁄8 61.5 1 ⁄4 ⁄2 ⁄2 54.8 1 ⁄4 ⁄8 ⁄8 49.2
3 3 3 1 3 1 5 3 5 3 3 3 1
45 1 ⁄4 1 ⁄4 ⁄8 ⁄4 61.5 1 ⁄4 ⁄2 ⁄16 54.8 1 ⁄4 ⁄8 ⁄8 49.2 1 ⁄4 ⁄4 ⁄2 44.4
3 3 3 5 3 1 3 3 5 1 3 3 5
45 1 ⁄4 1 ⁄4 ⁄8 ⁄16 61.5 1 ⁄4 ⁄2 ⁄8 54.8 1 ⁄4 ⁄8 ⁄2 49.2 1 ⁄4 ⁄4 ⁄8 44.4
5 1 1 5 5 5 5 3 3 5 1 1
... ... 1 ⁄8 ⁄4 ⁄4 68.1 1 ⁄8 ⁄16 ⁄16 63.7 1 ⁄8 ⁄8 ⁄8 59.8 1 ⁄8 ⁄2 ⁄2 53
5 5 3 5 3 1 5 1 5 5 5 3
... ... 1 ⁄8 ⁄16 ⁄16 63.7 1 ⁄8 ⁄8 ⁄4 59.8 1 ⁄8 ⁄2 ⁄16 53 1 ⁄8 ⁄8 ⁄8 47.3
5 5 1 5 3 5 5 1 3 5 5 1
... ... 1 ⁄8 ⁄16 ⁄4 63.7 1 ⁄8 ⁄8 ⁄16 59.8 1 ⁄8 ⁄2 ⁄8 53 1 ⁄8 ⁄8 ⁄2 47.3
1 1 1 1 1 5 5 1 3 3 1 1 1
37.5 1 ⁄2 1 ⁄2 ⁄4 ⁄4 66.6 1 ⁄2 ⁄16 ⁄16 62.1 1 ⁄2 ⁄8 ⁄8 58 1 ⁄2 ⁄2 ⁄2 51
1 1 5 3 1 3 1 1 1 5 1 5 3
37.5 1 ⁄2 1 ⁄2 ⁄16 ⁄16 62.1 1 ⁄2 ⁄8 ⁄4 58 1 ⁄2 ⁄2 ⁄16 51 1 ⁄2 ⁄8 ⁄8 45.1
1 1 5 1 1 3 5 1 1 3 1 5 1
37.5 1 ⁄2 1 ⁄2 ⁄16 ⁄4 62.1 1 ⁄2 ⁄8 ⁄16 58 1 ⁄2 ⁄2 ⁄8 51 1 ⁄2 ⁄8 ⁄2 45.1
E674−12 (2016)
TABLE1 Continued
Perforated
Medium Light Medium Medium Heavy Heavy
Opening
USA
Stan- Indus-
Open- Gage- Open Open- Gage- Open Open- Gage- Open Open- Gage- Open
dard trial Bar, Bar, Bar, Bar,
ing, Steel, Area, ing, Steel, Area, ing, Steel, Area, ing, Steel, Area,
(metric), Stan- in. in. in. in.
in. in. % in. in. % in. in. % in. in. %
mm dard,
in.
3 1 1 3 5 5 3 3 3 3 1 1
... ... 1 ⁄8 ⁄4 ⁄4 64.9 1 ⁄8 ⁄16 ⁄16 60.2 1 ⁄8 ⁄8 ⁄8 55.9 1 ⁄8 ⁄2 ⁄2 48.7
3 5 3 3 3 1 3 1 5 3 5 3
... ... 1 ⁄8 ⁄16 ⁄16 60.2 1 ⁄8 ⁄8 ⁄4 55.9 1 ⁄8 ⁄2 ⁄16 48.7 1 ⁄8 ⁄8 ⁄8 42.8
3 5 1 3 3 5 3 1 3 3 5 1
... ... 1 ⁄8 ⁄16 ⁄4 60.2 1 ⁄8 ⁄8 ⁄16 55.9 1 ⁄8 ⁄2 ⁄8 48.7 1 ⁄8 ⁄8 ⁄2 42.8
1 1 1 1 1 5 5 1 3 3 1 1 1
31.5 1 ⁄4 1 ⁄4 ⁄4 ⁄4 62.9 1 ⁄4 ⁄16 ⁄16 58 1 ⁄4 ⁄8 ⁄8 53.6 1 ⁄4 ⁄2 ⁄2 46.2
1 1 5 3 1 3 1 1 1 5 1 5 3
31.5 1 ⁄4 1 ⁄4 ⁄16 ⁄16 58 1 ⁄4 ⁄8 ⁄4 53.6 1 ⁄4 ⁄2 ⁄16 46.2 1 ⁄4 ⁄8 ⁄8 40.3
1 1 5 1 1 3 5 1 1 3 1 5 1
31.5 1 ⁄4 1 ⁄4 ⁄16 ⁄4 58 1 ⁄4 ⁄8 ⁄16 53.6 1 ⁄4 ⁄2 ⁄8 46.2 1 ⁄4 ⁄8 ⁄2 40.3
3 3 3 3 1 1 3 5 5 3 3 3
... ... 1 ⁄16 ⁄16 ⁄16 67.6 1 ⁄16 ⁄4 ⁄4 61.8 1 ⁄16 ⁄16 ⁄16 56.8 1 ⁄16 ⁄8 ⁄8 52.3
3 1 3 5 3 3 3 1 3 1 5
... ... 1 ⁄16 ⁄4 8 61.8 1 ⁄16 ⁄16 ⁄16 56.8 1 ⁄16 ⁄8 ⁄4 52.3 1 ⁄16 ⁄2 ⁄16 44.9
3 1 3 3 5 1 3 3 5 3 1 3
... ... 1 ⁄16 ⁄4 ⁄16 61.8 1 ⁄16 ⁄16 ⁄4 56.8 1 ⁄16 ⁄8 ⁄16 52.3 1 ⁄16 ⁄2 ⁄8 44.9
1 3 3 1 1 1 1 5 5 1 3 3
... ... 1 ⁄8 ⁄16 ⁄16 66.6 1 ⁄8 ⁄4 ⁄4 60.7 1 ⁄8 ⁄16 ⁄16 55.5 1 ⁄8 ⁄8 ⁄8 51
1 1 1 5 3 1 3 1 1 1 5
... ... 1 ⁄8 ⁄4 8 60.7 1 ⁄8 ⁄16 ⁄16 55.5 1 ⁄8 ⁄8 ⁄4 51 1 ⁄8 ⁄2 ⁄16 43.4
1 1 3 1 5 1 1 3 5 1 1 3
... ... 1 ⁄8 ⁄4 ⁄16 60.7 1 ⁄8 ⁄16 ⁄4 55.5 1 ⁄8 ⁄8 ⁄16 51 1 ⁄8 ⁄2 ⁄8 43.4
1 1 3 3 1 1 1 1 5 5 1 3 3
26.5 1 ⁄16 1 ⁄16 ⁄16 ⁄16 65.5 1 ⁄16 ⁄4 ⁄4 59.4 1 ⁄16 ⁄16 ⁄16 54.1 1 ⁄16 ⁄8 ⁄8 49.5
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: E674 − 12 E674 − 12 (Reapproved 2016)
Standard Specification for
Industrial Perforated Plate and Screens (Round Opening
Series)
This standard is issued under the fixed designation E674; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
INTRODUCTION
Industrial perforated plate can be produced in many thousands of combinations of size and shape
of opening, bar size, thickness of material, and type of metal. Such variety is often confusing and, to
the vast majority of perforated plate users, unnecessary, since each usually requires only a very few
specifications.
The purpose of this specification is to simplify this problem by a condensed table of recommended
specifications covering a wide range of openings in which industrial perforated plate is made, with
several recommended bar sizes and thicknesses of plate for each opening, for use in various grades of
service.
By making selections from this specification, the user will be guided to specifications that are being
regularly produced, thus avoiding inadvertent selection of specifications that, because of little or no
demand, are unobtainable, except on special order (usually quite expensive unless the quantity ordered
is sufficient to justify the cost of special tooling).
If a user has a specific application for industrial perforated plate that can not be solved by a selection
from this specification, it is recommended that he consult his perforated plate supplier on the
availability of an acceptable alternative specification.
1. Scope*Scope
1.1 This specification covers the sizes of round opening perforated plate and screens for general industrial uses, including the
separating or grading of materials according to designated nominal particle size, and lists standards for openings from 5 in. (125
mm) to 0.020 in. (500 μm) punched with bar sizes and thicknesses of plate for various grades of service. Methods of checking
industrial perforated plate and screens are included as information in Appendix X3.
1.2 This specification does not apply to perforated plate or screens with square, hexagon, slotted, or other shaped openings.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical
conversions to SI units that are provided for information only and are not considered standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use.
2. Referenced Documents
2.1 ASTM Standards:
E323 Specification for Perforated-Plate Sieves for Testing Purposes
E1638 Terminology Relating to Sieves, Sieving Methods, and Screening Media
2.2 ISO Standards:
ISO 2194 Industrial screens — Woven wire cloth, perforated plate and electroformed sheet — Designation and nominal sizes
of openings
This specification is under the jurisdiction of ASTM Committee E29 on Particle and Spray Characterization and is the direct responsibility of Subcommittee E29.01 on
Sieves, Sieving Methods, and Screening Media.
Current edition approved June 15, 2012July 1, 2016. Published June 2012July 2016. Originally approved in 1979. Last previous edition approved in 20112012 as
E674 – 11.E674 – 12. DOI: 10.1520/E0674-12.10.1520/E0674-12R16.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Available from International Organization for Standardization (ISO), 1, ch. de la Voie-Creuse, Case postale 56, CH-1211, Geneva 20, Switzerland, http://www.iso.ch.
*A Summary of Changes section appears at the end of this standard
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
E674 − 12 (2016)
2.3 Other Documents:
Fed. Std. 123 Marking for Shipments (Civil Agencies)
Mil-Std-129 Marking for Shipment and Storage
3. Terminology
3.1 Definitions—For general terms related to sieves, sieving methods, and screening media, see Terminology E1638.
3.2 Definitions of Terms Specific to This Standard:
3.2.1 aperture, n—the opening in a screening or sieving medium.
3.2.2 bar, n—the metal between perforations.
3.2.3 blank, n—unperforated area located other than along the perimeter of a plate.
3.2.4 break-out, n—term applied to the action that occurs ahead of the punch in its going through the plate.
Available from Standardization Documents Order Desk, DODSSP, Bldg. 4, Section D, 700 Robbins Ave., Philadelphia, PA 19111-5098, http://dodssp.daps.dla.mil.
3.2.4.1 Discussion—
The fracturing of the material results in a tapered hole with the small dimensions on the punch side.
3.2.5 centers, n—dimensional sum of one perforation and one bar or the dimensional distance from the center of one perforation
to the center of an adjacent perforation.
3.2.6 die side, n—surface of the plate that was against the die during the punching operation.
3.2.7 finished end pattern, n—condition that occurs with some specifications of staggered pattern perforations as a result of tool
design in which the pattern is completed on both ends of the plate (Fig. 1).
3.2.8 gage (alsogauge)gauge), , n—a number designating a specific thickness of metal sheet tabulated in a standardized series,
each of which represents a decimal fraction of an inch.
3.2.9 margin orborder, , n—unperforated area located along the perimeter of a plate.
3.2.10 percent open area, n—the ratio of the total area of the apertures to the total area expressed in percentage.
3.2.11 perforated pattern, n—the patterns that the perforations are arranged in, usually in a staggered pattern with midpoints
nominally at the vertices of isosceles triangles or square patterns arranged in line with their midpoints nominally at the vertices
of squares.
3.2.12 screen, n—(1) surface provided with apertures of uniform size and shape; (2) another term used interchangeably for
woven wire cloth; (3) machine provided with one or more screen surfaces.
3.2.13 screening, v—process of separating a mixture of different sizes by means of one or more screen surfaces.
3.2.14 smooth side or punch side, n—surface of the plate that was uppermost during the punching operation and through which
the punch entered the plate.
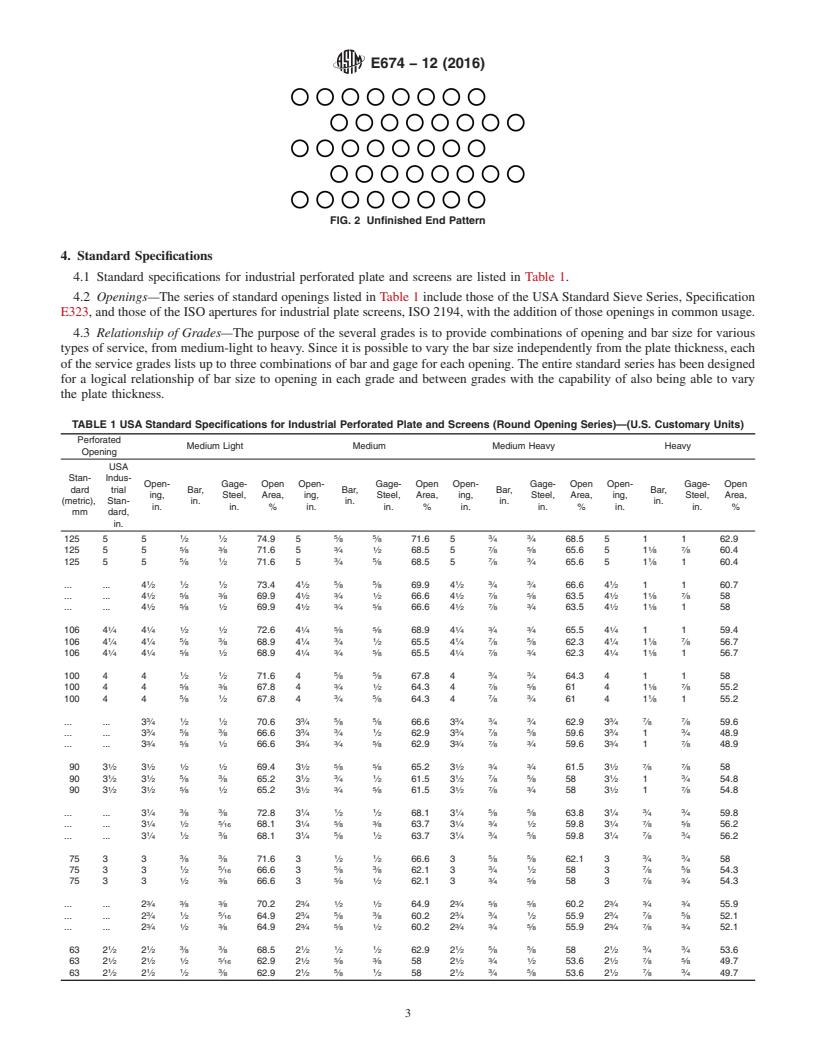
3.2.15 unfinished end pattern, n—condition that occurs with some specifications of staggered pattern perforations as a result of
tool design.
3.2.15.1 Discussion—
On one end of the plate, the pattern will appear to be incomplete as a result of unperforated holes in the even numbered rows, while
on the other end of the same plate, the pattern will appear to be incomplete because of unperforated holes in the odd numbered
rows (Fig. 2).
FIG. 1 Finished End Pattern
E674 − 12 (2016)
FIG. 2 Unfinished End Pattern
4. Standard Specifications
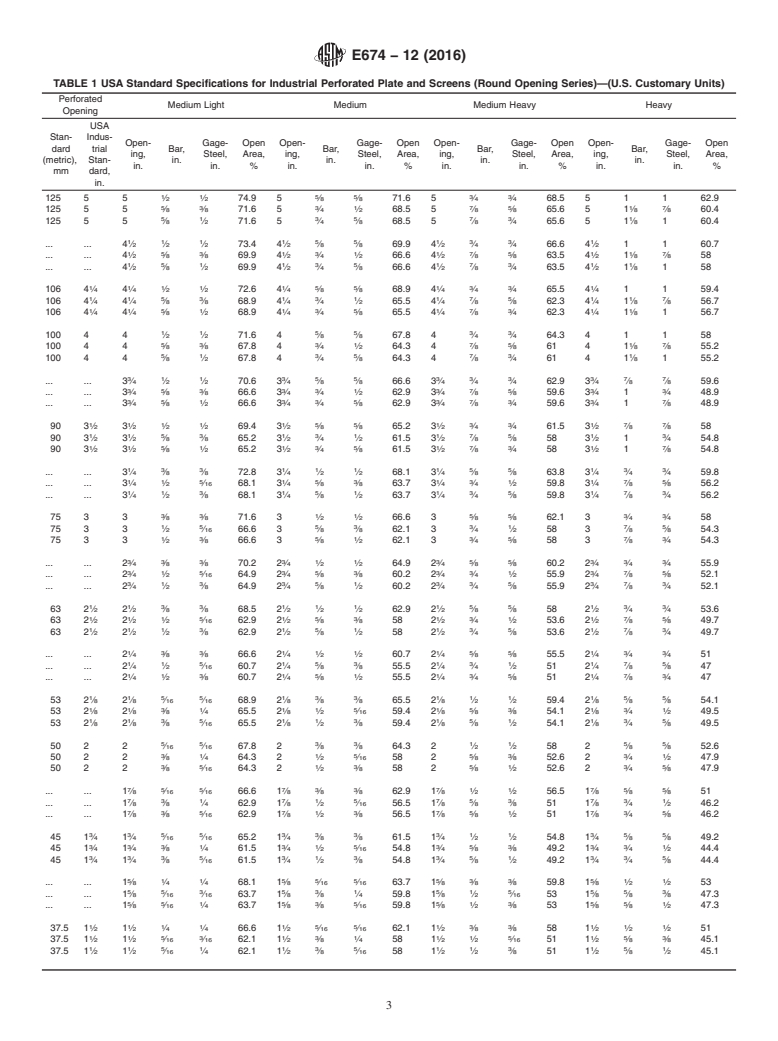
4.1 Standard specifications for industrial perforated plate and screens are listed in Table 1.
4.2 Openings—The series of standard openings listed in Table 1 include those of the USA Standard Sieve Series, Specification
E323, and those of the ISO apertures for industrial plate screens, ISO 2194, with the addition of those openings in common usage.
4.3 Relationship of Grades—The purpose of the several grades is to provide combinations of opening and bar size for various
types of service, from medium-light to heavy. Since it is possible to vary the bar size independently from the plate thickness, each
of the service grades lists up to three combinations of bar and gage for each opening. The entire standard series has been designed
for a logical relationship of bar size to opening in each grade and between grades with the capability of also being able to vary
the plate thickness.
TABLE 1 USA Standard Specifications for Industrial Perforated Plate and Screens (Round Opening Series)—(U.S. Customary Units)
Perforated
Medium Light Medium Medium Heavy Heavy
Opening
USA
Stan- Indus-
Open- Gage- Open Open- Gage- Open Open- Gage- Open Open- Gage- Open
dard trial Bar, Bar, Bar, Bar,
ing, Steel, Area, ing, Steel, Area, ing, Steel, Area, ing, Steel, Area,
(metric), Stan- in. in. in. in.
in. in. % in. in. % in. in. % in. in. %
mm dard,
in.
1 1 5 5 3 3
125 5 5 ⁄2 ⁄2 74.9 5 ⁄8 ⁄8 71.6 5 ⁄4 ⁄4 68.5 5 1 1 62.9
5 3 3 1 7 5 1 7
125 5 5 ⁄8 ⁄8 71.6 5 ⁄4 ⁄2 68.5 5 ⁄8 ⁄8 65.6 5 1 ⁄8 ⁄8 60.4
5 1 3 5 7 3 1
125 5 5 ⁄8 ⁄2 71.6 5 ⁄4 ⁄8 68.5 5 ⁄8 ⁄4 65.6 5 1 ⁄8 1 60.4
1 1 1 1 5 5 1 3 3 1
... ... 4 ⁄2 ⁄2 ⁄2 73.4 4 ⁄2 ⁄8 ⁄8 69.9 4 ⁄2 ⁄4 ⁄4 66.6 4 ⁄2 1 1 60.7
1 5 3 1 3 1 1 7 5 1 1 7
... ... 4 ⁄2 ⁄8 ⁄8 69.9 4 ⁄2 ⁄4 ⁄2 66.6 4 ⁄2 ⁄8 ⁄8 63.5 4 ⁄2 1 ⁄8 ⁄8 58
1 5 1 1 3 5 1 7 3 1 1
... ... 4 ⁄2 ⁄8 ⁄2 69.9 4 ⁄2 ⁄4 ⁄8 66.6 4 ⁄2 ⁄8 ⁄4 63.5 4 ⁄2 1 ⁄8 1 58
1 1 1 1 1 5 5 1 3 3 1
106 4 ⁄4 4 ⁄4 ⁄2 ⁄2 72.6 4 ⁄4 ⁄8 ⁄8 68.9 4 ⁄4 ⁄4 ⁄4 65.5 4 ⁄4 1 1 59.4
1 1 5 3 1 3 1 1 7 5 1 1 7
106 4 ⁄4 4 ⁄4 ⁄8 ⁄8 68.9 4 ⁄4 ⁄4 ⁄2 65.5 4 ⁄4 ⁄8 ⁄8 62.3 4 ⁄4 1 ⁄8 ⁄8 56.7
1 1 5 1 1 3 5 1 7 3 1 1
106 4 ⁄4 4 ⁄4 ⁄8 ⁄2 68.9 4 ⁄4 ⁄4 ⁄8 65.5 4 ⁄4 ⁄8 ⁄4 62.3 4 ⁄4 1 ⁄8 1 56.7
1 1 5 5 3 3
100 4 4 ⁄2 ⁄2 71.6 4 ⁄8 ⁄8 67.8 4 ⁄4 ⁄4 64.3 4 1 1 58
5 3 3 1 7 5 1 7
100 4 4 ⁄8 ⁄8 67.8 4 ⁄4 ⁄2 64.3 4 ⁄8 ⁄8 61 4 1 ⁄8 ⁄8 55.2
5 1 3 5 7 3 1
100 4 4 ⁄8 ⁄2 67.8 4 ⁄4 ⁄8 64.3 4 ⁄8 ⁄4 61 4 1 ⁄8 1 55.2
3 1 1 3 5 5 3 3 3 3 7 7
... ... 3 ⁄4 ⁄2 ⁄2 70.6 3 ⁄4 ⁄8 ⁄8 66.6 3 ⁄4 ⁄4 ⁄4 62.9 3 ⁄4 ⁄8 ⁄8 59.6
3 5 3 3 3 1 3 7 5 3 3
... ... 3 ⁄4 ⁄8 ⁄8 66.6 3 ⁄4 ⁄4 ⁄2 62.9 3 ⁄4 ⁄8 ⁄8 59.6 3 ⁄4 1 ⁄4 48.9
3 5 1 3 3 5 3 7 3 3 7
... ... 3 ⁄4 ⁄8 ⁄2 66.6 3 ⁄4 ⁄4 ⁄8 62.9 3 ⁄4 ⁄8 ⁄4 59.6 3 ⁄4 1 ⁄8 48.9
1 1 1 1 1 5 5 1 3 3 1 7 7
90 3 ⁄2 3 ⁄2 ⁄2 ⁄2 69.4 3 ⁄2 ⁄8 ⁄8 65.2 3 ⁄2 ⁄4 ⁄4 61.5 3 ⁄2 ⁄8 ⁄8 58
1 1 5 3 1 3 1 1 7 5 1 3
90 3 ⁄2 3 ⁄2 ⁄8 ⁄8 65.2 3 ⁄2 ⁄4 ⁄2 61.5 3 ⁄2 ⁄8 ⁄8 58 3 ⁄2 1 ⁄4 54.8
1 1 5 1 1 3 5 1 7 3 1 7
90 3 ⁄2 3 ⁄2 ⁄8 ⁄2 65.2 3 ⁄2 ⁄4 ⁄8 61.5 3 ⁄2 ⁄8 ⁄4 58 3 ⁄2 1 ⁄8 54.8
1 3 3 1 1 1 1 5 5 1 3 3
... ... 3 ⁄4 ⁄8 ⁄8 72.8 3 ⁄4 ⁄2 ⁄2 68.1 3 ⁄4 ⁄8 ⁄8 63.8 3 ⁄4 ⁄4 ⁄4 59.8
1 1 5 1 5 3 1 3 1 1 7 5
... ... 3 ⁄4 ⁄2 ⁄16 68.1 3 ⁄4 ⁄8 ⁄8 63.7 3 ⁄4 ⁄4 ⁄2 59.8 3 ⁄4 ⁄8 ⁄8 56.2
1 1 3 1 5 1 1 3 5 1 7 3
... ... 3 ⁄4 ⁄2 ⁄8 68.1 3 ⁄4 ⁄8 ⁄2 63.7 3 ⁄4 ⁄4 ⁄8 59.8 3 ⁄4 ⁄8 ⁄4 56.2
3 3 1 1 5 5 3 3
75 3 3 ⁄8 ⁄8 71.6 3 ⁄2 ⁄2 66.6 3 ⁄8 ⁄8 62.1 3 ⁄4 ⁄4 58
1 5 5 3 3 1 7 5
75 3 3 ⁄2 ⁄16 66.6 3 ⁄8 ⁄8 62.1 3 ⁄4 ⁄2 58 3 ⁄8 ⁄8 54.3
1 3 5 1 3 5 7 3
75 3 3 ⁄2 ⁄8 66.6 3 ⁄8 ⁄2 62.1 3 ⁄4 ⁄8 58 3 ⁄8 ⁄4 54.3
3 3 3 3 1 1 3 5 5 3 3 3
... ... 2 ⁄4 ⁄8 ⁄8 70.2 2 ⁄4 ⁄2 ⁄2 64.9 2 ⁄4 ⁄8 ⁄8 60.2 2 ⁄4 ⁄4 ⁄4 55.9
3 1 5 3 5 3 3 3 1 3 7 5
... ... 2 ⁄4 ⁄2 ⁄16 64.9 2 ⁄4 ⁄8 ⁄8 60.2 2 ⁄4 ⁄4 ⁄2 55.9 2 ⁄4 ⁄8 ⁄8 52.1
3 1 3 3 5 1 3 3 5 3 7 3
... ... 2 ⁄4 ⁄2 ⁄8 64.9 2 ⁄4 ⁄8 ⁄2 60.2 2 ⁄4 ⁄4 ⁄8 55.9 2 ⁄4 ⁄8 ⁄4 52.1
1 1 3 3 1 1 1 1 5 5 1 3 3
63 2 ⁄2 2 ⁄2 ⁄8 ⁄8 68.5 2 ⁄2 ⁄2 ⁄2 62.9 2 ⁄2 ⁄8 ⁄8 58 2 ⁄2 ⁄4 ⁄4 53.6
1 1 1 5 1 5 3 1 3 1 1 7 5
63 2 ⁄2 2 ⁄2 ⁄2 ⁄16 62.9 2 ⁄2 ⁄8 ⁄8 58 2 ⁄2 ⁄4 ⁄2 53.6 2 ⁄2 ⁄8 ⁄8 49.7
1 1 1 3 1 5 1 1 3 5 1 7 3
63 2 ⁄2 2 ⁄2 ⁄2 ⁄8 62.9 2 ⁄2 ⁄8 ⁄2 58 2 ⁄2 ⁄4 ⁄8 53.6 2 ⁄2 ⁄8 ⁄4 49.7
E674 − 12 (2016)
TABLE 1 Continued
Perforated
Medium Light Medium Medium Heavy Heavy
Opening
USA
Stan- Indus-
Open- Gage- Open Open- Gage- Open Open- Gage- Open Open- Gage- Open
dard trial Bar, Bar, Bar, Bar,
ing, Steel, Area, ing, Steel, Area, ing, Steel, Area, ing, Steel, Area,
(metric), Stan- in. in. in. in.
in. in. % in. in. % in. in. % in. in. %
mm dard,
in.
1 3 3 1 1 1 1 5 5 1 3 3
... ... 2 ⁄4 ⁄8 ⁄8 66.6 2 ⁄4 ⁄2 ⁄2 60.7 2 ⁄4 ⁄8 ⁄8 55.5 2 ⁄4 ⁄4 ⁄4 51
1 1 5 1 5 3 1 3 1 1 7 5
... ... 2 ⁄4 ⁄2 ⁄16 60.7 2 ⁄4 ⁄8 ⁄8 55.5 2 ⁄4 ⁄4 ⁄2 51 2 ⁄4 ⁄8 ⁄8 47
1 1 3 1 5 1 1 3 5 1 7 3
... ... 2 ⁄4 ⁄2 ⁄8 60.7 2 ⁄4 ⁄8 ⁄2 55.5 2 ⁄4 ⁄4 ⁄8 51 2 ⁄4 ⁄8 ⁄4 47
1 1 5 5 1 3 3 1 1 1 1 5 5
53 2 ⁄8 2 ⁄8 ⁄16 ⁄16 68.9 2 ⁄8 ⁄8 ⁄8 65.5 2 ⁄8 ⁄2 ⁄2 59.4 2 ⁄8 ⁄8 ⁄8 54.1
1 1 3 1 1 1 5 1 5 3 1 3 1
53 2 ⁄8 2 ⁄8 ⁄8 ⁄4 65.5 2 ⁄8 ⁄2 ⁄16 59.4 2 ⁄8 ⁄8 ⁄8 54.1 2 ⁄8 ⁄4 ⁄2 49.5
1 1 3 5 1 1 3 1 5 1 1 3 5
53 2 ⁄8 2 ⁄8 ⁄8 ⁄16 65.5 2 ⁄8 ⁄2 ⁄8 59.4 2 ⁄8 ⁄8 ⁄2 54.1 2 ⁄8 ⁄4 ⁄8 49.5
5 5 3 3 1 1 5 5
50 2 2 ⁄16 ⁄16 67.8 2 ⁄8 ⁄8 64.3 2 ⁄2 ⁄2 58 2 ⁄8 ⁄8 52.6
3 1 1 5 5 3 3 1
50 2 2 ⁄8 ⁄4 64.3 2 ⁄2 ⁄16 58 2 ⁄8 ⁄8 52.6 2 ⁄4 ⁄2 47.9
3 5 1 3 5 1 3 5
50 2 2 ⁄8 ⁄16 64.3 2 ⁄2 ⁄8 58 2 ⁄8 ⁄2 52.6 2 ⁄4 ⁄8 47.9
7 5 5 7 3 3 7 1 1 7 5 5
... ... 1 ⁄8 ⁄16 ⁄16 66.6 1 ⁄8 ⁄8 ⁄8 62.9 1 ⁄8 ⁄2 ⁄2 56.5 1 ⁄8 ⁄8 ⁄8 51
7 3 1 7 1 5 7 5 3 7 3 1
... ... 1 ⁄8 ⁄8 ⁄4 62.9 1 ⁄8 ⁄2 ⁄16 56.5 1 ⁄8 ⁄8 ⁄8 51 1 ⁄8 ⁄4 ⁄2 46.2
7 3 5 7 1 3 7 5 1 7 3 5
... ... 1 ⁄8 ⁄8 ⁄16 62.9 1 ⁄8 ⁄2 ⁄8 56.5 1 ⁄8 ⁄8 ⁄2 51 1 ⁄8 ⁄4 ⁄8 46.2
3 3 5 5 3 3 3 3 1 1 3 5 5
45 1 ⁄4 1 ⁄4 ⁄16 ⁄16 65.2 1 ⁄4 ⁄8 ⁄8 61.5 1 ⁄4 ⁄2 ⁄2 54.8 1 ⁄4 ⁄8 ⁄8 49.2
3 3 3 1 3 1 5 3 5 3 3 3 1
45 1 ⁄4 1 ⁄4 ⁄8 ⁄4 61.5 1 ⁄4 ⁄2 ⁄16 54.8 1 ⁄4 ⁄8 ⁄8 49.2 1 ⁄4 ⁄4 ⁄2 44.4
3 3 3 5 3 1 3 3 5 1 3 3 5
45 1 ⁄4 1 ⁄4 ⁄8 ⁄16 61.5 1 ⁄4 ⁄2 ⁄8 54.8 1 ⁄4 ⁄8 ⁄2 49.2 1 ⁄4 ⁄4 ⁄8 44.4
5 1 1 5 5 5 5 3 3 5 1 1
... ... 1 ⁄8 ⁄4 ⁄4 68.1 1 ⁄8 ⁄16 ⁄16 63.7 1 ⁄8 ⁄8 ⁄8 59.8 1 ⁄8 ⁄2 ⁄2 53
5 5 3 5 3 1 5 1 5 5 5 3
... ... 1 ⁄8 ⁄16 ⁄16 63.7 1 ⁄8 ⁄8 ⁄4 59.8 1 ⁄8 ⁄2 ⁄16 53 1 ⁄8 ⁄8 ⁄8 47.3
5 5 1 5 3 5 5 1 3 5 5 1
... ... 1 ⁄8 ⁄16 ⁄4 63.7 1 ⁄8 ⁄8 ⁄16 59.8 1 ⁄8 ⁄2 ⁄8 53 1 ⁄8 ⁄8 ⁄2 47.3
1 1 1 1 1 5 5 1 3 3 1 1 1
37.5 1 ⁄2 1 ⁄2 ⁄4 ⁄4 66.6 1 ⁄2 ⁄16 ⁄16 62.1 1 ⁄2 ⁄8 ⁄8 58 1 ⁄2 ⁄2 ⁄2 51
1 1 5 3 1 3 1 1 1 5 1 5 3
37.5 1 ⁄2 1 ⁄2 ⁄16 ⁄16 62.1 1 ⁄2 ⁄8 ⁄4 58 1 ⁄2 ⁄2 ⁄16 51 1 ⁄2 ⁄8 ⁄8 45.1
1 1 5 1 1 3 5 1 1 3 1 5 1
37.5 1 ⁄2 1 ⁄2 ⁄16 ⁄4 62.1 1 ⁄2 ⁄8 ⁄16 58 1 ⁄2 ⁄2 ⁄8 51 1 ⁄2 ⁄8 ⁄2 45.1
3 1 1 3 5 5 3 3 3 3 1 1
... ... 1 ⁄8 ⁄4 ⁄4 64.9 1 ⁄8 ⁄16 ⁄16 60.2 1 ⁄8 ⁄8 ⁄8 55.9 1 ⁄8 ⁄2 ⁄2 48.7
3 5 3 3 3 1 3 1 5 3 5 3
... ... 1 ⁄8 ⁄16 ⁄16 60.2 1 ⁄8 ⁄8 ⁄4 55.9 1 ⁄8 ⁄2 ⁄16 48.7 1 ⁄8 ⁄8 ⁄8 42.8
3 5 1 3 3 5 3 1 3 3 5 1
... ... 1 ⁄8 ⁄16 ⁄4 60.2 1 ⁄8 ⁄8 ⁄16 55.9 1 ⁄8 ⁄2 ⁄8 48.7 1 ⁄8 ⁄8 ⁄2 42.8
1 1 1 1 1 5 5 1 3 3 1 1 1
31.5 1 ⁄4 1 ⁄4 ⁄4 ⁄4 62.9 1 ⁄4 ⁄16 ⁄16 58 1 ⁄4 ⁄8 ⁄8 53.6 1 ⁄4 ⁄2 ⁄2 46.2
1 1 5 3 1 3 1 1 1 5 1 5 3
31.5 1 ⁄4 1 ⁄4 ⁄16 ⁄16 58 1 ⁄4 ⁄8 ⁄4 53.6 1 ⁄4 ⁄2 ⁄16 46.2 1 ⁄4 ⁄8 ⁄8 40.3
1 1 5 1 1 3 5 1 1 3 1 5 1
31.5 1 ⁄4 1 ⁄4 ⁄16 ⁄4 58 1 ⁄4 ⁄8 ⁄16 53.6 1 ⁄4 ⁄2 ⁄8 46.2 1 ⁄4 ⁄8 ⁄2 40.3
3 3 3 3 1 1 3 5 5 3 3 3
... ... 1 ⁄16 ⁄16 ⁄16 67.6 1 ⁄16 ⁄4 ⁄4 61.8 1 ⁄16 ⁄16 ⁄16 56.8 1 ⁄16 ⁄8 ⁄8 52.3
3 1 3 5 3 3 3 1 3 1 5
... ... 1 ⁄16 ⁄4 8 61.8 1 ⁄16 ⁄16 ⁄16 56.8 1 ⁄16 ⁄8 ⁄4 52.3 1 ⁄16 ⁄2 ⁄16 44.9
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.