

kSIST FprEN 4650:2026
(Main)Aerospace series - Wire and cable marking process, UV Laser
- Abstract
This document is applicable to the marking of aerospace vehicle electrical wires and cables using ultraviolet (UV) lasers.
This document specifies the process requirements for the implementation of UV laser marking of aerospace electrical wires and cables and fibre optic cables to achieve an acceptable quality mark using equipment designed for UV laser wire marking of identification codes on aircraft wire and cable subject to EN 3475 100. Wiring specified as UV laser markable and which has been marked in accordance with this document will conform to the requirements of EN 3838.
This document is applicable to the marking of airframe electrical wires and cables using ultraviolet (UV) lasers. The laser process practices specified in this standard are mandatory.
- Status
- Not Published
- Public Enquiry End Date
- 24-Sep-2025
- Technical Committee
- I13 - Imaginarni 13
- Current Stage
- 5020 - Formal vote (FV) (Adopted Project)
- Start Date
- 21-Jul-2026
- Due Date
- 08-Sep-2026
- Completion Date
- 22-Jul-2026
kSIST FprEN 4650:2026 is a CEN draft European Standard for marking aerospace electrical wires, cables and fibre optic cables with ultraviolet (UV) lasers. It specifies the process requirements and supporting equipment controls for producing acceptable identification marks on aircraft wire and cable. The document is written for equipment suppliers, marking users, purchasers, and inspection or quality teams working with aerospace wiring.
What does kSIST FprEN 4650:2026 specify?
kSIST FprEN 4650:2026 specifies the process requirements for UV laser marking of aerospace vehicle electrical wires and cables, including fibre optic cables, so that the finished mark is acceptable and the wiring remains fit for use. The process practices defined in the standard are mandatory for airframe electrical wires and cables.
The document is organized into scope, normative references, terms and definitions, requirements, quality assurance provisions, test methods, packaging, notes, and Annex A. The requirements distinguish between mask-based and scanning laser marking systems, which matters because the acceptable pulse, fluence, and dot-overlap limits are different for each method.
What are the key requirements of kSIST FprEN 4650:2026?
kSIST FprEN 4650:2026 focuses on keeping the mark legible and permanent while avoiding damage to insulation. It also requires the marking system to be documented, controlled, and verifiable.
Process and equipment control
Clause 4.2 requires the equipment supplier to create a design construction file showing how the equipment meets the Clause 4 requirements. That file has to be maintained and made available to purchasers, so buyers and users can check how the system was designed and what limits it is meant to hold.
Clause 4.4 requires the laser type and laser output control to match the document. In practice, this means the marker needs built-in energy or power measurement and active feedback where needed, so output can stay within the permitted marking range.
Laser wavelength and laser types
Clause 4.3.1 limits marking to short-wavelength UV laser light in the range 240 nm to 380 nm. Direct infrared (IR) marking is not allowed for aerospace electrical or fibre optic wire and cable. This matters because the process is intended to change the insulation colour, not to burn or deeply damage the surface.
Clause 8.7 notes the laser types commonly used for this process: frequency-tripled Q-switched neodymium lasers and XeCl excimer lasers. The standard allows other laser types only if they fully meet the document’s requirements.
Mask-based marking
Clause 4.3.2 requires mask-based marks to be formed by a single laser pulse and to avoid overlap. It also requires a uniform top hat beam profile. The pulse length range is 3 ns to 35 ns, and the fluence range is 0.8 J/cm² to 1.3 J/cm². In practice, the user must keep the system calibrated so the mark stays in this range across font sizes and operating conditions.
Scanning marking
Clause 4.3.3 covers scanning or vector marking systems. Their pulse length range is 5 ns to 150 ns. For Gaussian beams, the average fluence must be at or below 1.3 J/cm²; for uniform top hat beams, the peak fluence must be at or below 0.8 J/cm².
The same clause limits dot overlap to 50 % for Gaussian profile beams and 90 % for uniform top hat beams. This matters because too much overlap can create local hot spots and damage the insulation. The character design must also avoid crossover where possible.
Wire manufacturer’s mark and overmarking
Clause 4.3.4 introduces requirements for the wire manufacturer’s mark. It should be made with a simple font and a lower-contrast appearance than the wire code, so the two marks can be told apart. The standard also allows the wire code to overmark part of the manufacturer’s mark once.
Quality requirements
Clause 4.5 requires the process not to damage the wire or cable or alter the insulation properties outside acceptable limits. It also requires marks to be legible, permanent and of suitable contrast. Contrast is determined in accordance with EN 3475-705, while damage, legibility and permanence are assessed in accordance with EN 3838.
Inspection and calibration
Clause 5 assigns responsibility for inspection to the supplier and ties calibration control to EN ISO 10012 or an equivalent system. The user is also expected to verify laser equipment performance at intervals of not more than 12 months. For process qualification and conformance work, the document sets standard environmental conditions for temperature, pressure and humidity.
What terms does kSIST FprEN 4650:2026 define?
- Fluence - the energy density of a single laser pulse at the wire or cable surface, used to set the marking effect without excess energy.
- Dot overlap - the percentage relationship between dot diameter and dot pitch in scanning systems, used to control how character strokes are built.
- Contrast - the difference in luminance between the mark and its background, which affects how easily the mark can be read.
- Markability - the ability of a wire construction to produce legible identification marks with specified contrast under this process.
- UV laser - a laser that produces radiation in the ultraviolet range, which the standard uses for direct marking.
- IR laser - a laser that produces infrared radiation, mentioned mainly because direct IR marking is excluded.
- Wire manufacturer’s mark - the identification mark applied by the wire or cable manufacturer at production, such as a product identifier or batch information.
Who uses kSIST FprEN 4650:2026?
kSIST FprEN 4650:2026 is used by laser marking equipment suppliers, aerospace wire and cable manufacturers, airframe wiring suppliers, purchasers, and quality or inspection staff. Suppliers use it to design and document the marker, define output control, and prove that the machine meets the process limits.
Users and inspectors use it to set up the marking process, verify fluence and overlap, check contrast, and confirm that the marks remain legible and permanent. Purchasers use it to judge whether a supplier’s marking process is complete and suitable for aerospace wire identification.
What changed in kSIST FprEN 4650:2026 from the previous edition?
kSIST FprEN 4650:2026:2025 supersedes EN 4650:2023. The European foreword states three main changes: Clause 4 has been majorly revised, the scanning marking requirements have been expanded and updated for applied laser fluence and dot overlap, and a new section has been added for the wire manufacturer’s mark.
The foreword also says Annex A has been consolidated for dot measurement and dot overlap guidance covering high and low overlap.
Which standards are used with kSIST FprEN 4650:2026?
- EN 3475-100 - referenced in the scope as the general test-method basis for aircraft electrical cables.
- EN 3475-705 - gives the contrast measurement method used for mark contrast checks.
- EN 3475-706 - provides laser markability guidance for aerospace wires and cables.
- EN 3838 - defines requirements and tests for user-applied markings on aircraft electrical cables, including damage, legibility and permanence checks.
- EN ISO 10012 - sets requirements for measurement management systems and supports the calibration and measurement control expected for this process.
What does the kSIST FprEN 4650:2026 document contain?
kSIST FprEN 4650:2026 contains a requirements section, a quality assurance section, detailed test methods, practical notes on the marking process, and a normative Annex A. Table 1 links the verification and quality conformance tests to mask-based and scanning marker types, while the test methods section explains how to check wavelength, pulse length, fluence, dot overlap, residual IR, laser type, output control, insulation damage, legibility, permanence and contrast.
Annex A gives the calculation method for dot overlap and explains Gaussian and uniform top hat fluence profiles. The notes section explains how the process works, which wire constructions are markable, what the marks look like, and how wavelength, pulse length, pulse repetition rate and laser type relate to practical marking.
Relations
- Effective Date
- 25-Dec-2024
Get Certified
Connect with accredited certification bodies for this standard

BUREAU VERITAS Certification Germany
Bureau Veritas certification in Germany.
Element Materials Technology
Materials testing and product certification.

AQMS Ltd.
AQMS provides ISO certification to SMEs across the UK.
Sponsored listings
Frequently Asked Questions
kSIST FprEN 4650:2026 is a draft published by the Slovenian Institute for Standardization (SIST). Its full title is "Aerospace series - Wire and cable marking process, UV Laser". This standard covers: This document is applicable to the marking of aerospace vehicle electrical wires and cables using ultraviolet (UV) lasers. This document specifies the process requirements for the implementation of UV laser marking of aerospace electrical wires and cables and fibre optic cables to achieve an acceptable quality mark using equipment designed for UV laser wire marking of identification codes on aircraft wire and cable subject to EN 3475 100. Wiring specified as UV laser markable and which has been marked in accordance with this document will conform to the requirements of EN 3838. This document is applicable to the marking of airframe electrical wires and cables using ultraviolet (UV) lasers. The laser process practices specified in this standard are mandatory.
This document is applicable to the marking of aerospace vehicle electrical wires and cables using ultraviolet (UV) lasers. This document specifies the process requirements for the implementation of UV laser marking of aerospace electrical wires and cables and fibre optic cables to achieve an acceptable quality mark using equipment designed for UV laser wire marking of identification codes on aircraft wire and cable subject to EN 3475 100. Wiring specified as UV laser markable and which has been marked in accordance with this document will conform to the requirements of EN 3838. This document is applicable to the marking of airframe electrical wires and cables using ultraviolet (UV) lasers. The laser process practices specified in this standard are mandatory.
kSIST FprEN 4650:2026 is classified under the following ICS (International Classification for Standards) categories: 49.060 - Aerospace electric equipment and systems. The ICS classification helps identify the subject area and facilitates finding related standards.
kSIST FprEN 4650:2026 has the following relationships with other standards: It is inter standard links to SIST EN 4650:2023. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
kSIST FprEN 4650:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
oSIST prEN 4650:2025
01-september-2025
Aeronavtika - Postopek označevanja žic in kablov z UV-laserjem
Aerospace series - Wire and cable marking process, UV Laser
Luft- und Raumfahrt - Leitungs- und Kabelkennzeichnungsverfahren durch UV-Laser
Série aérospatiale - Procédé de marquage des fils et câbles par laser UV
Ta slovenski standard je istoveten z: prEN 4650
ICS:
49.060 Letalska in vesoljska Aerospace electric
električna oprema in sistemi equipment and systems
oSIST prEN 4650:2025 en,fr,de
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
oSIST prEN 4650:2025
oSIST prEN 4650:2025
DRAFT
EUROPEAN STANDARD
prEN 4650
NORME EUROPÉENNE
EUROPÄISCHE NORM
July 2025
ICS 49.060 Will supersede EN 4650:2023
English Version
Aerospace series - Wire and cable marking process, UV
Laser
Série aérospatiale - Procédé de marquage des fils et Luft- und Raumfahrt - Leitungs- und
câbles par laser UV Kabelkennzeichnungsverfahren durch UV-Laser
This draft European Standard is submitted to CEN members for enquiry. It has been drawn up by the Technical Committee ASD-
STAN.
If this draft becomes a European Standard, CEN members are bound to comply with the CEN/CENELEC Internal Regulations
which stipulate the conditions for giving this European Standard the status of a national standard without any alteration.
This draft European Standard was established by CEN in three official versions (English, French, German). A version in any other
language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC
Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
Recipients of this draft are invited to submit, with their comments, notification of any relevant patent rights of which they are
aware and to provide supporting documentation.
Warning : This document is not a European Standard. It is distributed for review and comments. It is subject to change without
notice and shall not be referred to as a European Standard.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2025 CEN All rights of exploitation in any form and by any means reserved Ref. No. prEN 4650:2025 E
worldwide for CEN national Members.
oSIST prEN 4650:2025
prEN 4650:2025 (E)
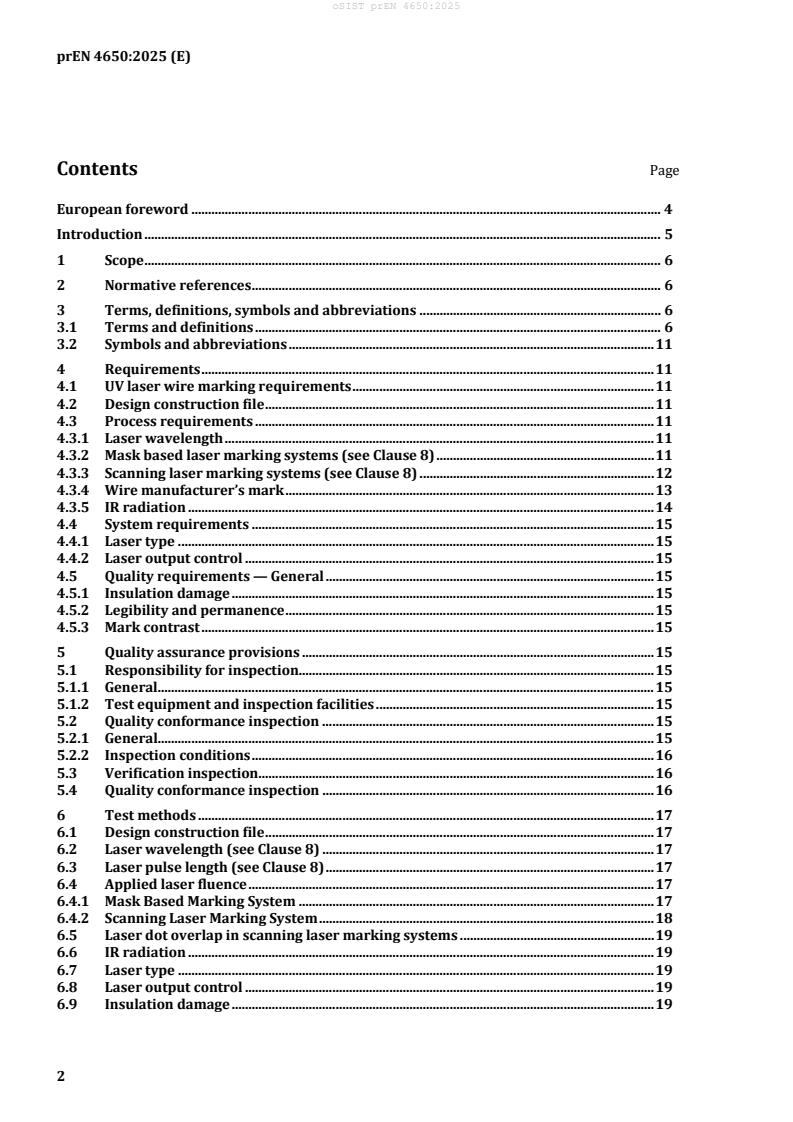
Contents Page
European foreword . 4
Introduction . 5
1 Scope . 6
2 Normative references . 6
3 Terms, definitions, symbols and abbreviations . 6
3.1 Terms and definitions . 6
3.2 Symbols and abbreviations . 11
4 Requirements . 11
4.1 UV laser wire marking requirements . 11
4.2 Design construction file . 11
4.3 Process requirements . 11
4.3.1 Laser wavelength . 11
4.3.2 Mask based laser marking systems (see Clause 8) . 11
4.3.3 Scanning laser marking systems (see Clause 8) . 12
4.3.4 Wire manufacturer’s mark . 13
4.3.5 IR radiation . 14
4.4 System requirements . 15
4.4.1 Laser type . 15
4.4.2 Laser output control . 15
4.5 Quality requirements — General . 15
4.5.1 Insulation damage . 15
4.5.2 Legibility and permanence . 15
4.5.3 Mark contrast . 15
5 Quality assurance provisions . 15
5.1 Responsibility for inspection. 15
5.1.1 General. 15
5.1.2 Test equipment and inspection facilities . 15
5.2 Quality conformance inspection . 15
5.2.1 General. 15
5.2.2 Inspection conditions . 16
5.3 Verification inspection . 16
5.4 Quality conformance inspection . 16
6 Test methods . 17
6.1 Design construction file . 17
6.2 Laser wavelength (see Clause 8) . 17
6.3 Laser pulse length (see Clause 8) . 17
6.4 Applied laser fluence . 17
6.4.1 Mask Based Marking System . 17
6.4.2 Scanning Laser Marking System . 18
6.5 Laser dot overlap in scanning laser marking systems . 19
6.6 IR radiation . 19
6.7 Laser type . 19
6.8 Laser output control . 19
6.9 Insulation damage . 19
oSIST prEN 4650:2025
prEN 4650:2025 (E)
6.10 Legibility and permanence. 19
6.11 Mark contrast measurements . 19
7 Packaging . 19
8 Notes . 19
8.1 Principle of the marking process . 19
8.1.1 General . 19
8.1.2 Mask-based laser marking systems . 20
8.1.3 Scanning laser marking systems . 20
8.2 Markability of wire constructions . 21
8.3 Properties of UV laser-marked insulation materials . 21
8.3.1 General . 21
8.3.2 Mark depth . 21
8.3.3 Mark permanence . 22
8.3.4 Mark colour. 22
8.3.5 Polymer insulation background colour . 22
8.3.6 Fungus . 22
8.4 Laser wavelength . 22
8.5 Pulse length . 23
8.6 Pulse repetition rate . 23
8.7 Laser type . 23
Annex A (normative) Information for dot overlap measurement methods for laser scanning
marking and laser beam distribution profiles . 24
Bibliography . 27
oSIST prEN 4650:2025
prEN 4650:2025 (E)
European foreword
This document (prEN 4650:2025) has been prepared by ASD-STAN.
After enquiries and votes carried out in accordance with the rules of this Association, this document has
received the approval of the National Associations and the Official Services of the member countries of
ASD, prior to its presentation to CEN.
This document is currently submitted to the CEN Enquiry.
This document will supersede EN 4650:2023.
prEN 4650:2025 includes the following significant technical changes with respect to EN 4650:2023-03:
— Major revision of Clause 4:
o expanded and updated, requirements for laser scanning marking systems including applied laser
fluence and dot overlap;
o new section added for wire manufacturer’s mark;
— Annex A:
o consolidated dot measurement and dot overlap for high and low overlap.
oSIST prEN 4650:2025
prEN 4650:2025 (E)
Introduction
Ultraviolet (UV) laser wire marking was developed in 1987 to provide a safe, permanent means of
marking thin wall insulations; it is now the aerospace industry standard method for marking wire
identification codes on to the surface of electrical wires and cables. It provides a simple, convenient,
environmentally friendly, cost-effective means of marking and identifying wires and jacketed cables.
While a few larger airframe manufacturers have developed process standards and specifications for their
own use during the introduction of this technology, there has been variability in the issues covered within
these specifications and there has been no comprehensive standard process document developed for
general use. The intended use of this document is to serve directly as a process standard for use by laser
wire marking concerns. It can also serve as a model set of comprehensive requirements for use by
organizations who intend to develop in-house laser marking process specifications or serve as a mean
for evaluating the adequacy and completeness of such specifications by procuring activities.
oSIST prEN 4650:2025
prEN 4650:2025 (E)
1 Scope
This document is applicable to the marking of aerospace vehicle electrical wires and cables using
ultraviolet (UV) lasers.
This document specifies the process requirements for the implementation of UV laser marking of
aerospace electrical wires and cables and fibre optic cables to achieve an acceptable quality mark using
equipment designed for UV laser wire marking of identification codes on aircraft wire and cable subject
to EN 3475-100, Aerospace series — Cables, electrical, aircraft use — Test methods — Part 100: General.
Wiring specified as UV laser markable, and which has been marked in accordance with this document,
will conform to the requirements of EN 3838.
This document is applicable to the marking of airframe electrical wires and cables using ultraviolet (UV)
lasers. The laser process practices defined in this document are mandatory.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 3475-705, Aerospace series — Cables, electrical, aircraft use — Test methods — Part 705: Contrast
measurement
EN 3838, Aerospace series — Requirements and tests on user-applied markings on aircraft electrical cables
EN ISO 10012, Measurement management systems — Requirements for measurement processes and
measuring equipment (ISO 10012)
3 Terms, definitions, symbols and abbreviations
For the purposes of this document, the following terms and definitions apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp/
— IEC Electropedia: available at https://www.electropedia.org/
3.1 Terms and definitions
3.1.1
cable
electrical cable, unless noted as a fibre optic cable, two or more insulated conductors, solid or stranded,
contained in a common covering, or two or more insulated conductors twisted or molded together
without common covering, or one insulated conductor with a metallic covering shield or outer conductor
3.1.2
component
electrical wire or multi-conductor cable or fibre optic cable
3.1.3
contrast
measurement relating to the difference in luminance of the mark and its associated background according
to a precise formula
oSIST prEN 4650:2025
prEN 4650:2025 (E)
3.1.4
damage
an unacceptable reduction in the mechanical or electrical properties of the insulation (i.e., specifically a
measurable reduction in the performance of the wire or cable that is outside of its defined specification
or is otherwise unacceptable)
3.1.5
dot overlap
dot overlap for scanning laser systems is defined in relation to the diameter, D, of the laser beam/dot at
the surface of the wire, and the distance, d, between the centres of the adjacent dots
Note 1 to entry: the percentage overlap = (1-(d/D)) x 100 %
3.1.6
excimer
gas laser deriving its name from the term “excited dimer”
Note 1 to entry: the laser is energized by means of an electrical discharge in a specialized mixture of rare gases and
halogens. Excimer lasers are available, operating at a number of discrete wavelengths throughout the UV, the most
common of which are 193 nm, 248 nm, 308 nm and 351 nm. The wavelength is dependant only on the gas mix used;
308 nm is commonly used for UV laser wire marking.
3.1.7
fibre optic cable
cable that is designed to transmit light waves between a light transmission source and a receiver
Note 1 to entry: in signal applications, the transmitter and receiver include devices that are used to convert
between optical and electronic pulses. Typical cables include a glass or plastic core, a layer of cladding having a
lower refractive index to refract or totally reflect light inward at the core/cladding boundary, a buffer, strength
members and jacketing to protect the inner cable from environmental damage.
3.1.8
fluence
energy density, measured in joules per square centimeter (J/cm ), of a single pulse of the laser beam,
which is at the surface of the wire insulation or cable jacket
3.1.9
font
defining shape and style of a character set for printing or marking
3.1.10
gauge
wire size specified for a wire in a wire harness assembly by the wire harness assembly drawing
3.1.11
harmonic generation
use of non-linear optical processes to change the wavelength of a laser, enabling the output of an infrared
laser to be converted to shorter wavelengths
Note 1 to entry: in the case of neodymium (Nd) lasers this results in a frequency doubled output at 532 nm in the
green and a frequency tripled output at 355 nm in the UV, which is used for wire marking.
oSIST prEN 4650:2025
prEN 4650:2025 (E)
3.1.12
harness
assembly of any number of wires, electrical/optical cables and/or groups and their terminations which
is designed and fabricated so as to allow for installation and removal as a unit
Note 1 to entry: a harness may be an open harness or a protected harness.
3.1.13
infrared
IR
electromagnetic radiation in the wavelength range from approximately 700 nm to in excess of 10 000 nm
3.1.14
insulation
outer polymer covering of an electrical wire or multi-conductor cable or fibre optic cable
3.1.15
IR laser
laser that produces a beam of radiation in the IR range
3.1.16
jacket
outer protective covering for a cable
3.1.17
laser
acronym for light amplification by the stimulated emission of radiation, a source of intense
monochromatic light in the ultraviolet, visible or infrared region of the spectrum
Note 1 to entry: The “active” or lasing medium may be a solid, liquid or gas. The laser beam is generated by
energizing the active medium using an external power source, which is most commonly electrical or optical.
3.1.18
laser average power
optical power, measured in Watts (W), delivered by the laser source
3.1.19
laser pulse energy
optical energy, measured in Joules (J) contained in each laser pulse
3.1.20
laser pulse length
time interval between the laser energy crossing half the maximum energy on the rising and the falling
edges of the pulse; referred to as FWHM – full width half maximum
−9
Note 1 to entry: pulse lengths are measured in nanoseconds (ns). 1 ns = 10 s.
3.1.21
laser pulse rate
number of laser pulses delivered per second, measured in Hertz (Hz). Also referred to as the laser pulse
frequency or repetition rate
oSIST prEN 4650:2025
prEN 4650:2025 (E)
3.1.22
legibility
properties of a mark that enable it to be easily and correctly read
3.1.23
luminance
quantitative measurement of the visible light reflected from a surface, in this case the wire or cable
insulation
3.1.24
mark
meaningful alphanumeric or machine-readable mark applied to the surface of a wire or cable jacket
3.1.25
markability
ability of a wire construction to be marked to provide legible identification marks of a specified contrast
when marked in accordance with this document
3.1.26
neodymium Nd
elemental metal that forms the active laser material in the most common type of solid-state laser
Note 1 to entry: the neodymium is held in an optically transparent solid “host” material, and is energized by optical
input, either from a flash lamp or from the optical output from a diode laser. The host material does not play a direct
role but can slightly influence the laser wavelength. Typical host materials are specialized crystal materials, such as
yttrium aluminium garnet (YAG), yttrium lithium fluoride (YLF) and yttrium vanadate (YVO ). These lasers are
commonly referred to as Nd:YAG, Nd:YLF and Nd:YVO respectively. The primary wavelength of Nd solid state lasers
is in the infrared (IR) at a wavelength of approximately 1 064 nm. The IR output of such lasers can be conveniently
reduced to lower wavelengths suitable for wire marking by use of harmonic generation.
3.1.27
purchaser
activity that can issue a purchase order or contract
3.1.28
Q-switched laser
laser that retains and circulates the laser energy internally within the laser until a signal is sent to open
the “Q-switch”, usually an electro-optic component
Note 1 to entry: The Q-switch acts like a gate that when opened allows the trapped laser beam to exit on a
nanosecond timescale. This technique is routinely used on long pulse solid state lasers to create short laser pulses
such as those required for UV laser wire marking.
3.1.29
quality conformance
tests performed on production samples at a specified frequency to ensure that the requirements of this
document are met
3.1.30
quality conformance inspection
process that includes measurements, non-destructive tests, analysis, and associated data that will
provide verification that a particular individual component continually conforms to the requirements
defined in the standard
oSIST prEN 4650:2025
prEN 4650:2025 (E)
3.1.31
supplier
original equipment manufacturer (OEM) or value-added manufacturer which has design and production
control of the processes used to produce the final product in accordance with the standard
3.1.32
ultraviolet
UV
electromagnetic radiation in the wavelength range from approximately 200 nm to 400 nm
3.1.33
UV laser
laser that produces a beam of radiation in the UV range
3.1.34
verification inspection
process that demonstrates that a product is capable of fully conforming to all the requirements defined
in a standard
Note 1 to entry: verification inspection includes definition of the measurements, tests, analysis, and associated data
that provides consistent rationale for acceptance of a particular supplier's design as meeting the standard
requirements typically prior to acquisition by the purchaser.
3.1.35
wavelength λ
distance between repeating units of a wave pattern
EXAMPLE The distance between the crest of one wave and the crest of an adjacent wave.
Note 1 to entry: laser wavelength is typically measured in nanometers (nm).
Note 2 to entry: λ = c/f
Where:
c is the velocity of light;
f is the frequency.
3.1.36
wire
single metallic conductor of solid, stranded or tinsel construction, designed to carry current in an electric
circuit, but not having a metallic covering, sheath or shield
Note 1 to entry: for the purpose of this specification, “wire” refers to “insulated electric wire”.
3.1.37
wire code
wire circuit identification number or code assigned to a specific wire in a wire harness assembly and
marked on the insulation surface
3.1.38
wire manufacturer’s mark
mark applied to a wire or cable by the manufacturer at the time of production, that may include the
product identifier, batch/lot number or date of manufacture
oSIST prEN 4650:2025
prEN 4650:2025 (E)
3.2 Symbols and abbreviations
−9
nm
nanometer, 10 m;
−9
ns
nanosecond, 10 s;
ETFE ethylenetetrafluoroethylene;
PFA perfluoroalkoxy fluoropolymer;
PTFE polytetrafluoroethylene;
PVDF polyvinylidene difluoride/polyvinylidene fluoride.
4 Requirements
4.1 UV laser wire marking requirements
The laser requirements for marking aerospace wire and cable are grouped under:
a) process requirements, i.e. those characteristics that affect the marking process in terms of the mark
characteristics and quality; and
b) system requirements, i.e. those characteristics that affect the performance of equipment in terms of
its operational use.
4.2 Design construction file
The equipment supplier shall create a design construction file that records the relevant design details of
the equipment and demonstrates clearly how all the requirements of Clause 4 are met. A copy of this
design construction file shall be maintained and made available to purchasers as required.
4.3 Process requirements
4.3.1 Laser wavelength
Short wavelength UV laser light, in the range 240 nm to 380 nm only shall be used for marking
(see Clause 8). Long wavelength infrared (IR) laser radiation shall not be used for the direct marking of
aerospace electrical or fibre optic wire and cable.
4.3.2 Mask based laser marking systems (see Clause 8)
4.3.2.1 General
Laser marks generated by mask-based processes shall be formed by a single pulse of the laser and shall
not overlap. Only laser beams with a uniform top hat profile shall be employed for mask marking.
WARNING — Multiple overlapping marks may cause wire insulation damage, particularly on extruded
ETFE and PVDF materials.
4.3.2.2 Laser pulse length (see Clause 8)
Lasers with pulse lengths between 3 ns and 35 ns shall be used for marking.
oSIST prEN 4650:2025
prEN 4650:2025 (E)
4.3.2.3 Applied laser fluence (see Clause 8)
The equipment supplier shall be responsible for designing the system to ensure that the equipment
delivers the required fluence to achieve the optimum mark contrast and quality without impairing the
wire characteristics. The user shall be responsible for ensuring that the equipment is maintained and
calibrated to continue to deliver the required fluence.
2 2
The equipment shall be set to mark at a fluence in the range 0,8 J/cm to 1,3 J/cm . The specified fluence
shall be the fluence measured at the top centre of the wire surface, as marked. These marking fluences
shall be used unless the wire type under test is specified for marking at a different fluence.
The laser fluence delivered to the wire shall remain within the specified range under all standard
operating conditions at all times during the entirety of the marking process and for all different font sizes;
this shall be inclusive of any pulse to pulse variations in laser energy.
In ensuring that the equipment delivers and operates within the required fluence at all times the supplier
shall design the equipment taking into account:
a) the laser shot to shot pulse energy variation;
b) short to long term drift in laser power output;
c) the laser beam intensity profile, ensuring that that part of the beam used for marking the wires shall
be of sufficiently uniform intensity and without any hot spots that would result in the maximum
fluence being exceeded within the beam profile when projected on to a flat surface at the focal point
of the beam delivery system.
Laser markers set to operate in the specified fluence range will produce the maximum mark contrast on
any given aerospace wire or cable. It is not possible to increase the mark contrast by increasing the
fluence above this range. End users shall not attempt to do this.
WARNING — Potential for wire damage, if excessive fluence is used for wire marking.
4.3.3 Scanning laser marking systems (see Clause 8)
4.3.3.1 Laser pulse length
The pulse lengths of scanning laser marking systems shall be between 5 ns and 150 ns.
4.3.3.2 Applied laser fluence
The equipment supplier shall be responsible for designing the system to ensure that the equipment
delivers the required fluence to achieve the optimum mark contrast and quality without impairing the
wire characteristics.
The equipment supplier shall provide clear, concise instructions on how to maintain, operate and
calibrate the laser marker within the design parameters. The user shall be responsible for ensuring that
the equipment is maintained and calibrated in accordance with the supplier's instructions.
For laser markers employing Gaussian beams, the equipment shall be set to mark at an average
fluence ≤ 1,3 J/cm , while respecting the 50 % limit for dot overlap noted in 4.3.3.3.
For laser markers employing uniform top hat beams, the equipment shall be set to mark at a peak
fluence ≤ 0,8 J/cm , while respecting the 90 % limit for dot overlap noted in 4.3.3.3.
The specified fluence shall be the fluence measured at the top centre of the wire surface, as marked.
These marking fluences shall be used unless the wire type under test is specified for marking at a different
fluence.
oSIST prEN
...