


ASTM E1077-01(2005)
(Test Method)Standard Test Methods for Estimating the Depth of Decarburization of Steel Specimens
Standard Test Methods for Estimating the Depth of Decarburization of Steel Specimens
SIGNIFICANCE AND USE
These test methods are used to detect surface losses in carbon content due to heating at elevated temperatures, as in hot working or heat treatment.
Results of such tests may be used to qualify material for shipment according to agreed upon guidelines between purchaser and manufacturer, for guidance as to machining allowances, or to assess the influence of processing upon decarburization tendency.
Screening tests are simple, fast, low-cost tests designed to separate non-decarburized samples from those with appreciable decarburization. Based on the results of such tests, the other procedures may be utilized as applicable.
Microscopical tests require a metallographically pol-ished cross section to permit reasonably accurate determina-tion of the depth and nature of the decarburization present. Several methods may be employed for estimation of the depth of decarburization. The statistical accuracy of each varies with the amount of effort expended.
Microindentation hardness methods are employed on polished cross sections and are most suitable for hardened specimens with reasonably uniform microstructures. This procedure can be used to define the depth to a specific minimum hardness or the depth to a uniform hardness.
Chemical analytical methods are limited to specimens with simple, uniform shapes and are based on analysis of incremental turnings or after milling at fixed increments.
Microscopical tests are generally satisfactory for determining the suitability of material for intended use, specification acceptance, manufacturing control, development, or research.
SCOPE
1.1 These test methods cover procedures for estimating the depth of decarburization of steels irrespective of the composition, matrix microstructure, or section shape. The following basic procedures may be used:
1.1.1 Screening methods.
1.1.2 Microscopical methods.
1.1.3 Microindentation hardness methods.
1.1.4 Chemical analysis methods.
1.2 In case of a dispute, the rigorous quantitative or lineal analysis method (see 7.3.5 and 7.3.6) shall be the referee method. These methods can be employed with any cross-sectional shape. The chemical analytical methods generally reveal a greater depth of decarburization than the microscopical methods but are limited to certain simple shapes and by availability of equipment. These techniques are generally reserved for research studies. The microindentation hardness method is suitable for accurate measurements of hardened structures with relatively homogeneous microstructures.
1.3 The values stated in SI units are to be regarded as standard. The inch-pound equivalents are in parentheses and may be approximate.
1.4This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: E1077 − 01(Reapproved 2005)
Standard Test Methods for
Estimating the Depth of Decarburization of Steel
Specimens
This standard is issued under the fixed designation E1077; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision.Anumber in parentheses indicates the year of last reapproval.A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the Department of Defense.
INTRODUCTION
These test methods may be used to estimate the average or greatest depth of decarburization in
hardened or non-hardened steel products. The test methods described range from simple screening
tests to more statistically rigorous test methods depending upon the needs of the investigation.
1. Scope 2. Referenced Documents
1.1 These test methods cover procedures for estimating the
2.1 ASTM Standards:
depth of decarburization of steels irrespective of the
A941TerminologyRelatingtoSteel,StainlessSteel,Related
composition, matrix microstructure, or section shape. The
Alloys, and Ferroalloys
following basic procedures may be used:
E3Guide for Preparation of Metallographic Specimens
1.1.1 Screening methods.
E7Terminology Relating to Metallography
1.1.2 Microscopical methods.
E340Test Method for Macroetching Metals and Alloys
1.1.3 Microindentation hardness methods.
E350Test Methods for Chemical Analysis of Carbon Steel,
1.1.4 Chemical analysis methods.
Low-Alloy Steel, Silicon Electrical Steel, Ingot Iron, and
Wrought Iron
1.2 In case of a dispute, the rigorous quantitative or lineal
E384Test Method for Knoop and Vickers Hardness of
analysis method (see 7.3.5 and 7.3.6) shall be the referee
Materials
method. These methods can be employed with any cross-
E407Practice for Microetching Metals and Alloys
sectional shape. The chemical analytical methods generally
E415Test Method for Atomic Emission Vacuum Spectro-
reveal a greater depth of decarburization than the microscopi-
cal methods but are limited to certain simple shapes and by metric Analysis of Carbon and Low-Alloy Steel
E1951Guide for Calibrating Reticles and Light Microscope
availability of equipment. These techniques are generally
reserved for research studies. The microindentation hardness Magnifications
method is suitable for accurate measurements of hardened
structures with relatively homogeneous microstructures. 3. Terminology
1.3 The values stated in SI units are to be regarded as 3.1 Definitions:
standard. The inch-pound equivalents are in parentheses and
3.1.1 Fordefinitionsoftermsusedinthesetestmethods,see
may be approximate.
Terminology E7 and Terminology A941.
1.4 This standard does not purport to address all of the 3.2 Definitions of Terms Specific to This Standard:
safety concerns, if any, associated with its use. It is the
3.2.1 average depth of decarburization—the mean value of
responsibility of the user of this standard to establish appro-
five or more measurements of the total depth of decarburiza-
priate safety and health practices and determine the applica-
tion.
bility of regulatory limitations prior to use.
3.2.2 average free-ferrite depth—the mean value of five or
more measurements of the depth of complete decarburization.
These test methods are under the jurisdiction of ASTM Committee E04 on
Metallography and are the direct responsibility of Subcommittee E04.14 on
Quantitative Metallography. For referenced ASTM standards, visit the ASTM website, www.astm.org, or
Current edition approved May 1, 2005. Published May 2005. Originally contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
´1
approved in 1985. Last previous edition approved in 2001 as E1077–01 . DOI: Standards volume information, refer to the standard’s Document Summary page on
10.1520/E1077-01R05. the ASTM website.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
E1077 − 01 (2005)
3.2.3 complete decarburization—loss of carbon content at 5.7 Microscopical tests are generally satisfactory for deter-
the surface of a steel specimen to a level below the solubility miningthesuitabilityofmaterialforintendeduse,specification
limit of carbon in ferrite so that only ferrite is present. acceptance, manufacturing control, development, or research.
3.2.4 free-ferrite depth—theperpendiculardistancefromthe
6. Sampling
surface of the specimen to that location where the structure is
6.1 Samples should be taken at locations that are represen-
no longer fully ferritic, that is, other transformation products
tative of the bulk specimen. The location and number of
are observed.
samplestakendependsonthenatureofthematerialtobetested
NOTE 1—The term free ferrite has also been used to describe globular,
and will be defined upon agreements between manufacturer
isolated grains of proeutectoid ferrite in the microstructure of medium-
and purchaser.
carbon hypoeutectoid steels.
6.2 Specimens for screening tests using bulk hardness tests,
3.2.5 maximum depth of decarburization—the largest mea-
such as the Rockwell test, should be small enough so that they
sured value of the total depth of decarburization.
can be properly supported on the anvil of the tester. The
3.2.6 partial decarburization—loss of carbon content at the
specimen surface should not be altered except for scale
surface of a steel specimen to a level less than the bulk carbon
removal (if present) using a method that will not alter the
content of the unaffected interior but greater than the room
subsurface metal.
temperature solubility limit of carbon in ferrite.
6.3 Specimens for the microscopical methods or for micro-
3.2.7 total depth of decarburization—the perpendicular dis-
indentation hardness tests or for macroscopic screening meth-
tance from the specimen surface to that location in the interior
ods should be cut from the bulk specimen perpendicular to the
wherethebulkcarboncontentisreached;thatis,thesumofthe
longitudinalaxisoftheproductsothatmeasurementsaremade
depths of complete and partial decarburization.
on a transverse plane.This procedure permits determination of
the variation of decarburization around the periphery of the
4. Summary of Test Method
specimen.
4.1 Thesetestmethodsaredesignedtodetectchangesinthe
6.3.1 Forspecimensuptoabout2.5-cm(1-in.)diameter,the
microstructure, hardness, or carbon content at the surface of
entire cross section is polished and examined. For larger cross
steel sections due to decarburization. The depth of decarbur-
sections, one or more specimens shall be prepared to assess
ization is determined as the depth where a uniform
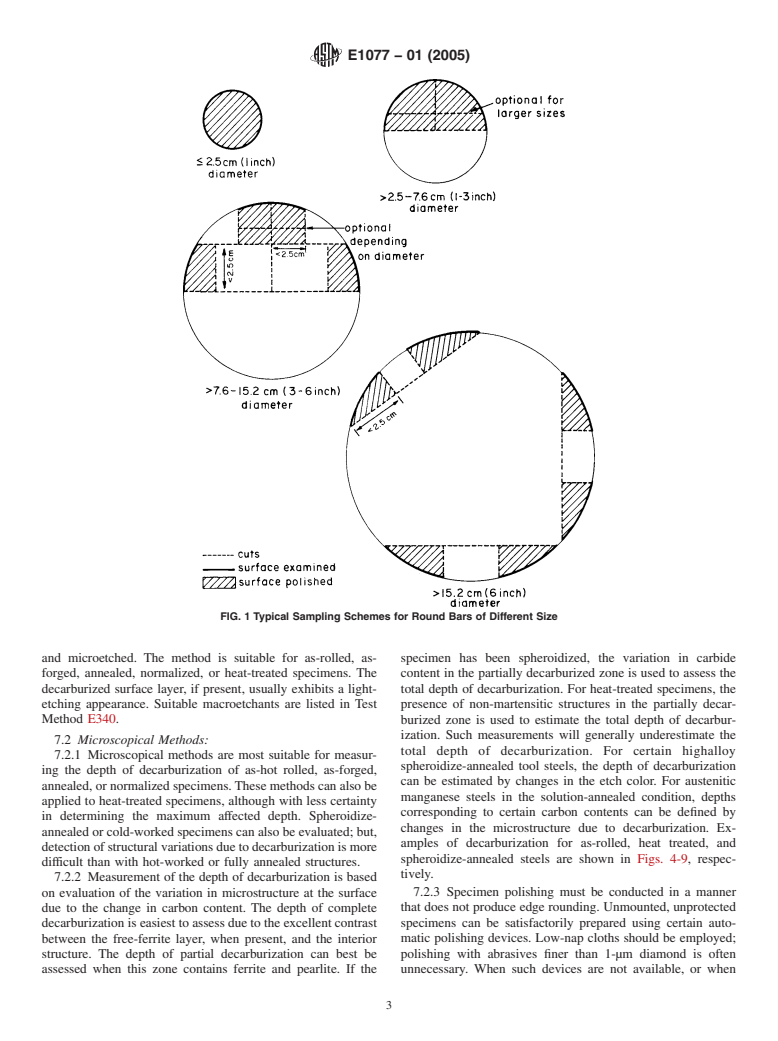
variations in surface decarburization. Figs. 1-3 show examples
microstructure, hardness, or carbon content, typical of the
of typical sampling schemes that may be used for larger
interior of the specimen, is observed.
sections; the sampling scheme for large sections should be
determined upon mutual agreement between manufacturer and
5. Significance and Use
purchaser.
5.1 These test methods are used to detect surface losses in
6.4 Specimens for chemical analytical methods must be of
carbon content due to heating at elevated temperatures, as in
sufficient length so that the weight of incremental turnings is
hot working or heat treatment.
adequate for chemical analysis or the size of milled surfaces is
5.2 Resultsofsuchtestsmaybeusedtoqualifymaterialfor
large enough for sparking yet small enough to fit in the
shipment according to agreed upon guidelines between pur-
specimen holder.
chaser and manufacturer, for guidance as to machining
allowances, or to assess the influence of processing upon
7. Procedure
decarburization tendency.
7.1 Screening Methods:
5.3 Screening tests are simple, fast, low-cost tests designed
7.1.1 Bulk Surface Hardness—Forhardenedspecimens,par-
to separate non-decarburized samples from those with appre- ticularly those in the as-quenched condition, a short section of
ciable decarburization. Based on the results of such tests, the
the material to be heat treated is cut and heat treated in the
other procedures may be utilized as applicable. same manner, or along with, the material of interest. The test
specimen,howeverisnottempered.Anyscaleonthetestpiece
5.4 Microscopical tests require a metallographically pol-
is removed by wire brushing, glass-bead blasting, etc., and
ished cross section to permit reasonably accurate determina-
hardness tested, usually with the Rockwell C scale. The
tion of the depth and nature of the decarburization present.
presence of decarburization is indicated by the difference
Several methods may be employed for estimation of the depth
between the surface hardness and the theoretical maximum
of decarburization.The statistical accuracy of each varies with
hardness for the carbon content of the steel. This method is
the amount of effort expended.
most suitable for those steels with bulk carbon contents below
5.5 Microindentation hardness methods are employed on
about 0.55% carbon but will detect gross decarburization in
polished cross sections and are most suitable for hardened
steels with higher bulk carbon contents. The method is not
specimens with reasonably uniform microstructures. This pro-
suitable for steels that cannot be quench-hardened, for
cedure can be used to define the depth to a specific minimum
example, low-carbon steels.
hardness or the depth to a uniform hardness.
7.1.2 Macroscopical Etch Appearance—The presence of
5.6 Chemical analytical methods are limited to specimens decarburization is indicated by a difference in etching contrast
with simple, uniform shapes and are based on analysis of between the surface and the interior of the specimen. A
incremental turnings or after milling at fixed increments. transverse section can be ground and macroetched or polished
E1077 − 01 (2005)
FIG. 1 Typical Sampling Schemes for Round Bars of Different Size
and microetched. The method is suitable for as-rolled, as- specimen has been spheroidized, the variation in carbide
forged, annealed, normalized, or heat-treated specimens. The content in the partially decarburized zone is used to assess the
decarburized surface layer, if present, usually exhibits a light- total depth of decarburization. For heat-treated specimens, the
etching appearance. Suitable macroetchants are listed in Test presence of non-martensitic structures in the partially decar-
Method E340.
burized zone is used to estimate the total depth of decarbur-
ization. Such measurements will generally underestimate the
7.2 Microscopical Methods:
total depth of decarburization. For certain highalloy
7.2.1 Microscopical methods are most suitable for measur-
spheroidize-annealed tool steels, the depth of decarburization
ing the depth of decarburization of as-hot rolled, as-forged,
can be estimated by changes in the etch color. For austenitic
annealed,ornormalizedspecimens.Thesemethodscanalsobe
manganese steels in the solution-annealed condition, depths
applied to heat-treated specimens, although with less certainty
corresponding to certain carbon contents can be defined by
in determining the maximum affected depth. Spheroidize-
changes in the microstructure due to decarburization. Ex-
annealedorcold-workedspecimenscanalsobeevaluated;but,
amples of decarburization for as-rolled, heat treated, and
detectionofstructuralvariationsduetodecarburizationismore
spheroidize-annealed steels are shown in Figs. 4-9, respec-
difficult than with hot-worked or fully annealed structures.
tively.
7.2.2 Measurement of the depth of decarburization is based
7.2.3 Specimen polishing must be conducted in a manner
on evaluation of the variation in microstructure at the surface
due to the change in carbon content. The depth of complete that does not produce edge rounding. Unmounted, unprotected
specimens can be satisfactorily prepared using certain auto-
decarburizationiseasiesttoassessduetotheexcellentcontrast
between the free-ferrite layer, when present, and the interior matic polishing devices. Low-nap cloths should be employed;
polishing with abrasives finer than 1-µm diamond is often
structure. The depth of partial decarburization can best be
assessed when this zone contains ferrite and pearlite. If the unnecessary. When such devices are not available, or when
E1077 − 01 (2005)
FIG. 2 Typical Sampling Schemes for Square Bars of Different Size
specimens are small or of an inconvenient shape for such contentisabove1.16%.Etchingwithnitalorpicralwillreveal
3, 4
devices, specimens should be mounted in clamps or in various the pearlite. Figs. 10 and 11 illustrates these conditions.
plastic media. With some mounting media, edge preservation
7.3 Measurement:
may be inadequate. The compression mounting epoxy materi-
7.3.1 The depth of complete or partial decarburization, or
als generally provide the best edge retention of the commonly
both, can be assessed in a variety of ways depending on the
available plastics. Electrolytic or electroless plating provides
desired accuracy. Measurements can be made using an ocular
optimum edge retention and is recommended for critical work.
micrometer reticle, a screw (Filar) micrometer ocular, or with
Polishing must be practiced using techniques that produce a
a scale placed against a ground-glass projection screen. Mea-
true representation of the surface microstructure, as described
surements can be made on the image or on photographs.
in Guide E3.
Measurements can also be made using image analysis tech-
7.2.4 Etching should be conducted using standard etchants,
niques. The accuracy of the measurement device should be
(see Test Methods E407) such as nital or picral, based on the
established using a stage micrometer. Light microscope cali-
experience of the rater with the material being tested. Special
bration procedures can be found in Guide E1951.
etchantscanbeusedifdictatedbythesituationencountered.In
7.3.2 The optimum magnification for measurement must be
such cases, agreement should be obtained between manufac-
chosen based on the observed structure. It may be helpful to
turer and purchaser.
scan the specimen at low magnification for the measurement.
7.2.5 For solution-annealed austenitic manganese steels,
The magnification used should be high enough to permit
epsilon martensite will be present in the surface region where
the carbon content is below about 0.5% carbon.This structure
is best revealed by etching first with 2% nital for 5 s and then
Sedriks,A.J.,andMulhearn,T.O.,“AusteniticManganeseSteel:Structureand
Properties of Decarburized Layer,” Journal of the Iron and Steel Institute, V
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.