


ISO/ASTM FDIS 52957
(Main)Additive manufacturing of ceramics — Design — Design guidelines
General Information
- Abstract
This document specifies ceramic part properties, design freedom, strengths and applications of additively manufactured parts made of ceramic materials. It aims at product planners and designers and provides the necessary basic knowledge about ceramic parts and the possibilities specific to additively manufactured ceramics, including strengths and limitations of the most commonly utilized ceramic additive manufacturing methods. In-depth previous knowledge in these areas is not assumed.
- Status
- Not Published
- Technical Committee
- ISO/TC 261 - Additive manufacturing
- Drafting Committee
- ISO/TC 261 - Additive manufacturing
- Current Stage
- 5020 - FDIS ballot initiated: 2 months. Proof sent to secretariat
- Start Date
- 11-Aug-2026
- Completion Date
- 11-Aug-2026
Buy Documents
ISO/ASTM FDIS 52957 - Additive manufacturing of ceramics — Design — Design guidelines
REDLINE ISO/ASTM FDIS 52957 - Additive manufacturing of ceramics — Design — Design guidelines
ISO/ASTM FDIS 52957 - Fabrication additive de céramiques — Conception — Lignes directrices relatives à la conception
Overview
ISO/ASTM FDIS 52957:2026, titled Additive manufacturing of ceramics - Design - Design guidelines, provides essential design directives for planning and producing ceramic components via additive manufacturing (AM). Developed jointly by ISO and ASTM, this standard targets product planners, design engineers, and manufacturers who seek fundamental understanding of ceramic AM part properties, design freedoms, process strengths, and unique application areas. The guidelines address capabilities and constraints of the most widely utilized AM methods for ceramics, offering foundational knowledge without the need for deep prior expertise.
Key Topics
- Ceramic Part Properties: Ceramics used in AM are characterized by high hardness, thermal resistance, corrosion and wear resistance, and low density. However, unlike metals, ceramics generally lack plastic deformation-parts fail after their elastic limit is exceeded.
- Design Freedom in AM:
- Complex Geometries: AM enables production of intricate structures, undercuts, and internal features not feasible with traditional ceramic manufacturing.
- Integration of Functions: Designers can combine multiple mechanical and thermal features within a single part, leveraging AM for function-driven, consolidated components.
- Topology Optimization: Material usage can be minimized through automated geometry optimization, supporting lightweight and performance-oriented designs.
- Limitations & Considerations:
- Brittleness and Load Capacity: Ceramics excel in compressive strength but have lower tensile strength. Sharp notches, small radii, and stress concentrations should be minimized to avoid early failure.
- Sintering Shrinkage: Significant shrinkage occurs during the debinding and sintering steps, necessitating careful dimension scaling during green body design.
- Layer Anisotropy: The mechanical properties of AM ceramic parts can vary with build orientation due to their layer-by-layer construction.
- Surface Finish and Porosity:
- Parts often require post-processing to achieve desired surface specifications and tolerances.
- Controlled porosity and channel integration are possible for specialized applications, but depend on process limitations and feedstock selection.
Applications
Additive manufacturing unlocks new potential for technical ceramics across diverse sectors. Key application areas include:
- Medical and Dental: Custom implants and surgical tools leveraging ceramics' biocompatibility and wear resistance.
- Aerospace and Automotive: Lightweight, heat-resistant components for engines, sensors, and insulation.
- Electronics: High-durability, precision parts such as insulators and substrates.
- Industrial and Process Engineering: Wear parts, nozzles, and seals with enhanced corrosion and abrasion resistance.
- Research and Prototyping: Rapid iteration of complex, function-integrated ceramic components not achievable by traditional methods.
By following the design guidelines in ISO/ASTM FDIS 52957, designers can efficiently harness AM's capabilities while accounting for material and process-specific requirements.
Related Standards
Understanding ceramic additive manufacturing design in context requires familiarity with several supporting standards:
- ISO/ASTM 52900: General principles and vocabulary for additive manufacturing.
- ISO/ASTM 52910: Broader design requirements and guidelines for AM.
- ISO/ASTM 52915: Specification for Additive Manufacturing File Format (AMF), critical for digital part definition.
- ISO/ASTM 52921: Terminology for AM coordinate systems and test methodologies.
- ISO 2768-1 & ISO 2768-2: General tolerances for linear, angular, and geometrical dimensions.
For specific AM process knowledge, such as vat photopolymerization or binder jetting of ceramics, sector-specific guides and process standards should be reviewed.
Practical Value
ISO/ASTM FDIS 52957 empowers designers and engineers by:
- Clarifying material-specific challenges and opportunities in ceramic AM.
- Providing actionable recommendations to maximize part performance and reliability.
- Facilitating innovation through advanced design freedoms, while minimizing trial-and-error.
- Enabling consistent, high-quality outcomes by harmonizing terminology and basic expectations.
Utilizing these design guidelines improves success rates in the additive manufacturing of ceramic parts, ultimately reducing risk, cost, and time-to-market for advanced ceramic applications.
Relations
- Effective Date
- 12-Feb-2026
Buy Documents
ISO/ASTM FDIS 52957 - Additive manufacturing of ceramics — Design — Design guidelines
REDLINE ISO/ASTM FDIS 52957 - Additive manufacturing of ceramics — Design — Design guidelines
ISO/ASTM FDIS 52957 - Fabrication additive de céramiques — Conception — Lignes directrices relatives à la conception
Get Certified
Connect with accredited certification bodies for this standard

DVS-ZERT GmbH
German welding certification society.
CARES (UK Certification Authority for Reinforcing Steels)
UK certification for reinforcing steels and construction.
EWF/IIW (European/International Welding Federation)
International welding personnel certification.
Sponsored listings
Frequently Asked Questions
ISO/ASTM FDIS 52957 is a draft published by the International Organization for Standardization (ISO). Its full title is "Additive manufacturing of ceramics — Design — Design guidelines". This standard covers: This document specifies ceramic part properties, design freedom, strengths and applications of additively manufactured parts made of ceramic materials. It aims at product planners and designers and provides the necessary basic knowledge about ceramic parts and the possibilities specific to additively manufactured ceramics, including strengths and limitations of the most commonly utilized ceramic additive manufacturing methods. In-depth previous knowledge in these areas is not assumed.
This document specifies ceramic part properties, design freedom, strengths and applications of additively manufactured parts made of ceramic materials. It aims at product planners and designers and provides the necessary basic knowledge about ceramic parts and the possibilities specific to additively manufactured ceramics, including strengths and limitations of the most commonly utilized ceramic additive manufacturing methods. In-depth previous knowledge in these areas is not assumed.
ISO/ASTM FDIS 52957 is classified under the following ICS (International Classification for Standards) categories: 25.030 - Additive manufacturing. The ICS classification helps identify the subject area and facilitates finding related standards.
ISO/ASTM FDIS 52957 has the following relationships with other standards: It is inter standard links to FprEN ISO/ASTM 52957. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
ISO/ASTM FDIS 52957 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
FINAL DRAFT
International
Standard
ISO/ASTM
FDIS
ISO/TC 261
Additive manufacturing of
Secretariat: DIN
ceramics — Design — Design
Voting begins on:
guidelines
2026-08-11
Fabrication additive de céramiques — Conception — Lignes
Voting terminates on:
directrices relatives à la conception
2026-10-06
RECIPIENTS OF THIS DRAFT ARE INVITED TO SUBMIT,
WITH THEIR COMMENTS, NOTIFICATION OF ANY
RELEVANT PATENT RIGHTS OF WHICH THEY ARE AWARE
AND TO PROVIDE SUPPOR TING DOCUMENTATION.
IN ADDITION TO THEIR EVALUATION AS
BEING ACCEPTABLE FOR INDUSTRIAL, TECHNO
ISO/CEN PARALLEL PROCESSING LOGICAL, COMMERCIAL AND USER PURPOSES, DRAFT
INTERNATIONAL STANDARDS MAY ON OCCASION HAVE
TO BE CONSIDERED IN THE LIGHT OF THEIR POTENTIAL
TO BECOME STAN DARDS TO WHICH REFERENCE MAY BE
MADE IN NATIONAL REGULATIONS.
Reference number
FINAL DRAFT
International
Standard
ISO/ASTM
FDIS
ISO/TC 261
Additive manufacturing of
Secretariat: DIN
ceramics — Design — Design
Voting begins on:
guidelines
Fabrication additive de céramiques — Conception — Lignes
Voting terminates on:
directrices relatives à la conception
RECIPIENTS OF THIS DRAFT ARE INVITED TO SUBMIT,
WITH THEIR COMMENTS, NOTIFICATION OF ANY
RELEVANT PATENT RIGHTS OF WHICH THEY ARE AWARE
© ISO/ASTM International 2026
AND TO PROVIDE SUPPOR TING DOCUMENTATION.
All rights reserved. Unless otherwise specified, or required in the context of its implementation, no part of this publication may
IN ADDITION TO THEIR EVALUATION AS
be reproduced or utilized otherwise in any form or by any means, electronic or mechanical, including photocopying, or posting on
BEING ACCEPTABLE FOR INDUSTRIAL, TECHNO
ISO/CEN PARALLEL PROCESSING
LOGICAL, COMMERCIAL AND USER PURPOSES, DRAFT
the internet or an intranet, without prior written permission. Permission can be requested from either ISO at the address below
INTERNATIONAL STANDARDS MAY ON OCCASION HAVE
or ISO’s member body in the country of the requester. In the United States, such requests should be sent to ASTM International.
TO BE CONSIDERED IN THE LIGHT OF THEIR POTENTIAL
ISO copyright office ASTM International TO BECOME STAN DARDS TO WHICH REFERENCE MAY BE
MADE IN NATIONAL REGULATIONS.
CP 401 • Ch. de Blandonnet 8 100 Barr Harbor Drive, PO Box C700
CH-1214 Vernier, Geneva West Conshohocken, PA 19428-2959, USA
Phone: +41 22 749 01 11 Phone: +610 832 9634
Fax: +610 832 9635
Email: copyright@iso.org Email: khooper@astm.org
Website: www.iso.org Website: www.astm.org
Published in Switzerland Reference number
© ISO/ASTM International 2026 – All rights reserved
ii
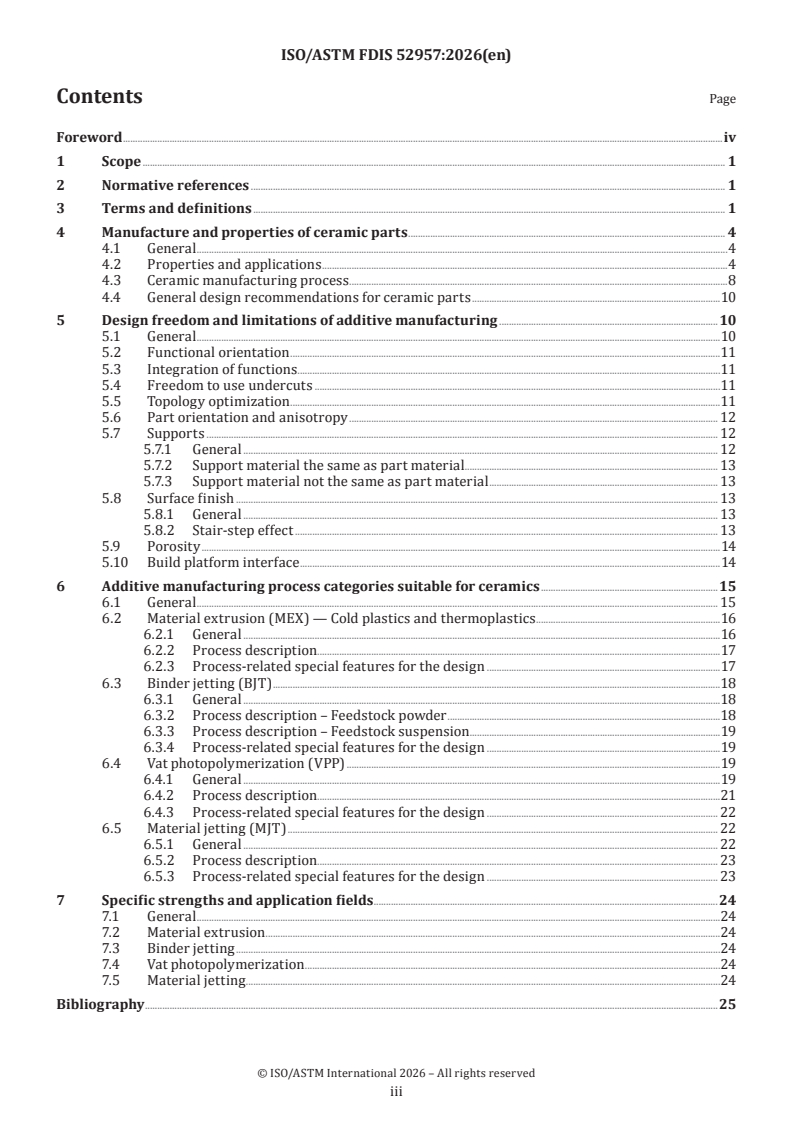
Contents Page
Foreword .iv
1 Scope . 1
2 Normative references . 1
3 Terms and definitions . 1
4 Manufacture and properties of ceramic parts . 4
4.1 General .4
4.2 Properties and applications .4
4.3 Ceramic manufacturing process .8
4.4 General design recommendations for ceramic parts .10
5 Design freedom and limitations of additive manufacturing .10
5.1 General .10
5.2 Functional orientation .11
5.3 Integration of functions . .11
5.4 Freedom to use undercuts .11
5.5 Topology optimization .11
5.6 Part orientation and anisotropy . 12
5.7 Supports . 12
5.7.1 General . 12
5.7.2 Support material the same as part material . 13
5.7.3 Support material not the same as part material . 13
5.8 Surface finish . 13
5.8.1 General . 13
5.8.2 Stair-step effect . 13
5.9 Porosity .14
5.10 Build platform interface .14
6 Additive manufacturing process categories suitable for ceramics .15
6.1 General . 15
6.2 Material extrusion (MEX) — Cold plastics and thermoplastics .16
6.2.1 General .16
6.2.2 Process description .17
6.2.3 Process-related special features for the design .17
6.3 Binder jetting (BJT) .18
6.3.1 General .18
6.3.2 Process description – Feedstock powder .18
6.3.3 Process description – Feedstock suspension .19
6.3.4 Process-related special features for the design .19
6.4 Vat photopolymerization (VPP) .19
6.4.1 General .19
6.4.2 Process description .21
6.4.3 Process-related special features for the design . 22
6.5 Material jetting (MJT) . 22
6.5.1 General . 22
6.5.2 Process description . 23
6.5.3 Process-related special features for the design . 23
7 Specific strengths and application fields .24
7.1 General .24
7.2 Material extrusion .24
7.3 Binder jetting .24
7.4 Vat photopolymerization .24
7.5 Material jetting . .24
Bibliography .25
© ISO/ASTM International 2026 – All rights reserved
iii
Foreword
The International Organization for Standardization (ISO) is a worldwide federation of national standards
bodies (ISO member bodies). The work of preparing International Standards is normally carried out through
ISO technical committees. Each member body interested in a subject for which a technical committee
has been established has the right to be represented on that committee. International organizations,
governmental and non-governmental, in liaison with ISO, also take part in the work. ISO collaborates closely
with the International Electrotechnical Commission (IEC) on all matters of electrotechnical standardization.
The procedures used to develop this document and those intended for its further maintenance are described
in the ISO/IEC Directives, Part 1. In particular, the different approval criteria needed for the different types
of ISO document should be noted. This document was drafted in accordance with the editorial rules of the
ISO/IEC Directives, Part 2 (see www.iso.org/directives).
ISO draws attention to the possibility that the implementation of this document may involve the use of (a)
patent(s). ISO takes no position concerning the evidence, validity or applicability of any claimed patent
rights in respect thereof. As of the date of publication of this document, ISO had not received notice of (a)
patent(s) which may be required to implement this document. However, implementers are cautioned that
this may not represent the latest information, which may be obtained from the patent database available at
www.iso.org/patents. ISO shall not be held responsible for identifying any or all such patent rights.
Any trade name used in this document is information given for the convenience of users and does not
constitute an endorsement.
For an explanation of the voluntary nature of standards, the meaning of ISO specific terms and expressions
related to conformity assessment, as well as information about ISO's adherence to the World Trade
Organization (WTO) principles in the Technical Barriers to Trade (TBT), see www.iso.org/iso/foreword.html.
This document was prepared by Technical Committee ISO/TC 261, Additive manufacturing, in cooperation
with ASTM Committee F42, Additive Manufacturing Technologies, on the basis of a partnership agreement
between ISO and ASTM International with the aim to create a common set of ISO/ASTM standards on
Additive Manufacturing, in collaboration with the European Committee for Standardization (CEN) Technical
Committee CEN/TC 438, Additive manufacturing, in accordance with the Agreement on technical cooperation
between ISO and CEN (Vienna Agreement).
Any feedback or questions on this document should be directed to the user’s national standards body. A
complete listing of these bodies can be found at www.iso.org/members.html.
© ISO/ASTM International 2026 – All rights reserved
iv
FINAL DRAFT International Standard ISO/ASTM FDIS 52957:2026(en)
Additive manufacturing of ceramics — Design — Design
guidelines
1 Scope
This document specifies part properties, design freedom, strengths and applications of additively
manufactured (AM) ceramic materials. It is aimed at product planners and designers and provides the
necessary basic knowledge about ceramics and the possibilities specific to AM ceramics, including strengths
and limitations of the most utilized ceramic AM process categories. In-depth previous knowledge in these
areas is not assumed.
2 Normative references
The following document is referred to in the text in such a way that some or all their content constitutes
requirements of this document. For dated references, only the edition cited applies. For undated references,
the latest edition of the referenced document (including any amendments) applies.
ISO/ASTM 52900, Additive manufacturing — General principles — Fundamentals and vocabulary
3 Terms and definitions
For the purposes of this document, the terms and definitions given in ISO/ASTM 52900 and the following
apply:
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https:// www .iso .org/ obp
— IEC Electropedia: available at https:// www .electropedia .org/
3.1
binder system
mixture of different organic or inorganic materials that after curing/drying/solidification bind the
particulate material together forming the green body (3.8) before shaping
3.2
brown body
green body (3.8) that has undergone pyrolysis/debinding (3.4)
Note 1 to entry: The brown body has very low mechanical strength, as the individual particles adhere to each other
solely due to surface forces as well as frictional and positive locking.
3.3
ceramic
any material that is classified as an inorganic, non-metallic crystalline solid
3.4
cleaning
removal of adhering excess of feedstock from the green body (3.8)
3.5
debinding
process of removing all binder from the green body (3.8)
© ISO/ASTM International 2026 – All rights reserved
3.6
downskin angle
δ
angle between the build platform plane and a downskin area, D, whose value lies between 0° (parallel to the
build platform) and 90° (perpendicular to the build platform)
Note 1 to entry: See Figure 1.
Key
D downskin area
U upskin area
n normal vector
Figure 1 — Upskin angle, υ, and downskin angle, δ, according to VDI 3405 Blatt 3.2
3.7
granulate
solid, flowable feedstock for powder bed-based AM processes
Note 1 to entry: Granulate is a specially produced compound of many individual powder particles that has significantly
improved flow properties compared to a standard powder.
3.8
green body
part in intermediate state of processing, where the intended geometrical shape is given, but the bonding of
the intended part material is yet to be established (which occurs during sintering (3.14))
Note 1 to entry: For multi-step ceramic processes, the green body typically will consist of a powder held together by
the binder system.
Note 2 to entry: The mechanical properties of a green body made from powder materials are essentially determined
by the binder system.
3.9
green machining
machining of the green body (3.8) to attain the desired geometry or surface quality
Note 1 to entry: Green processing can include the removal of supports and the integration of special geometric
features.
3.10
hard machining
machining of the sintered part (3.13) to achieve the desired geometry, dimension or surface quality to the
final dimension
Note 1 to entry: Due to the high hardness of the sintered part, hard machining is very time-consuming and places very
high demands on the machining processes and tools.
© ISO/ASTM International 2026 – All rights reserved
3.11
infiltration
process where a fluid material (liquid, vapor or slurry) is introduced into the connected pores of a porous
ceramic preform
3.12
shrinkage
volume reduction of a part without mass change during sintering (3.14)
Note 1 to entry: Volume reduction due to material removal (machining) is not referred to as shrinkage.
3.13
sintered part
part after sintering (3.14) with the final (ceramic (3.3)) properties
3.14
sintering
thermal process for compacting and bonding the (ceramic (3.3)) particles, taking place at temperatures
below the melting temperature
Note 1 to entry: Generally, sintering is accompanied by shrinkage.
Note 2 to entry: The temperature during sintering is above the debinding temperature but below the melting
temperature of the ceramic material.
3.15
suspension
liquid feedstock with suspended particulate (i.e. ceramic (3.3) powder)
EXAMPLE Slip, ink, paste, slurry, etc.
Note 1 to entry: The suspension can be solidified by removing components of the binder system or initiating cross-
linking reactions.
3.16
undercut
design feature, such as a horizontal protrusion, cavity or internal channel, that juts out from the main body
and cannot be produced without supports
3.17
upskin angle
υ
angle between the build platform plane and an upskin area, U, whose value lies between 0° (parallel to the
build platform) and 90° (perpendicular to the build platform)
Note 1 to entry: See Figure 1.
3.18
white machining
machining of the white body to realize the desired geometry or surface quality
Note 1 to entry: The subsequent shrinkage during sintering should be considered and compensated for by an
appropriate oversize.
Note 2 to entry: White machining processing can include the removal of supports and the integration of special
geometric features.
© ISO/ASTM International 2026 – All rights reserved
3.19
white body
green body (3.8) or brown body (3.2) in which initial sintering (3.14) of the particles, including the formation
of sinter necks, has been initiated by thermal treatment
Note 1 to entry: The mechanical strength of the white body is significantly higher than that of the brown body, but still
significantly lower than that of the sintered part.
4 Manufacture and properties of ceramic parts
4.1 General
In this clause, the properties and applications are first presented (see 4.2). Then the ceramic manufacturing
process is explained (see 4.3), from which general design recommendations are then derived (see 4.4).
4.2 Properties and applications
The specific properties of ceramic materials, which in various relationships typically cannot be matched by
other materials, offer versatile applications.
Compared to metals, ceramic materials can offer higher hardness, thermal resistance, corrosion resistance
and wear resistance, as well as lower density and thermal expansion. An essential difference between
ceramic materials and metals is that ceramics usually do not show plastic deformation but fail after elastic
deformation when the load limit is exceeded. An example are MAX (M AX ) phases, which can show plastic
n+1 n
deformation when a load is applied.
An overview of the properties of ceramic materials is given in Table 1. The last column lists properties of
structural steel for comparison. The properties listed in Table 1 can vary depending on the processing and
raw materials utilized.
NOTE Polymeric materials are not included due to their distinctly different material properties.
[3][4]
Table 1 — Overview of typical properties of ceramic parts in comparison with structural steel
Material
Porcelain Aluminium Zirconium Silicon ni- Silicon car- Structural
Material property
oxide oxide tride bide steel
a b c
(>99 %) (3Y-TZP) (SSiN) (SSiC) St 37
Density
2,2 3,9 5…6 3,2…3,3 3,08…3,15 7,8
in g/cm
Hardness (Vickers)
5…9 13…23 10…14 14…18 22…34 2…4
in GPa
Flexural strength
50 300…450 500…1,000 700…1,000 260…500 340…470
in MPa
Young’s modulus
60 300 200…210 290…330 350…450 200…210
in GPa
Fracture toughness
– 4…5,5 5,8…10,5 5…8,5 3,0…4,8 200
1/2
in MPa m
Thermal expansion
4…7 7…8 10…12,5 2,5…3,5 4,0…4,8 10…12
–6 –1
in 10 K
a
3Y-TZP – tetragonally stabilized zirconium oxide with 3 % molar content of yttrium oxide.
b
SiN – silicon nitride.
c
SiC – silicon carbide.
© ISO/ASTM International 2026 – All rights reserved
Figure 2 through Figure 5 illustrate the relationship between different properties for selected ceramics
compared to metals. In this way, characteristics of ceramic materials can be both quickly compared among
[3][4]
each other as well as to metals .
The literature values used in Figure 2 through Figure 5 were determined with standardized test specimens
from conventional manufacturing processes and are to provide general guideline comparisons. In AM, there
are different manufacturing process categories and material formulations, which means that the property
values can vary greatly. Porosity is particularly affected by this. For example, density and flexural strength
decrease as porosity increases. Because of this, it is advised that the investigator research the more specific
values for their ceramic system.
Key
X density, in g/cm
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 2 — Relationship between density and flexural strength for selected ceramics compared to
[3]
metals
© ISO/ASTM International 2026 – All rights reserved
Key
X young’s modulus, in GPa
Y hardness, in GPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 3 — Relationship between Young’s modulus and hardness for selected ceramics compared to
[3]
metal
© ISO/ASTM International 2026 – All rights reserved
Key
‒1 ‒1
X thermal conductivity, in Wm ·K
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 4 — Relationship between thermal conductivity and flexural strength for selected ceramics
[3]
compared to metals
© ISO/ASTM International 2026 – All rights reserved
Key
‒1 ‒6
X coefficient of expansion, in 10 K
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 5 — Relationship between coefficient of expansion and flexural strength for selected
[3]
ceramics compared to metals
4.3 Ceramic manufacturing process
The same basic process principle applies to all ceramic materials for conventional and AM (see Figure 6).
From the mostly powdery feedstock, it is first prepared from which a green body is created during the
subsequent shaping process. The green body corresponds to a composite material consisting of an organic
matrix and ceramic particles embedded in it. With AM, the green body is built up layer-by-layer based on a
CAD model. In conventional manufacturing, a tool (i.e. a mould) should be created for shaping.
© ISO/ASTM International 2026 – All rights reserved
Figure 6 — Schematic representation of the production process for technical ceramics
Subsequently, debinding and sintering of the parts are necessary to realize the ceramic properties in the
part. For AM parts, these two processes correspond to those conventionally manufactured, whereby the
process control should be adapted to the respective decomposition properties of the binder systems used as
well as to the realized volume fraction of ceramic material in the feedstock.
During debinding, all organic components are removed from the green body to allow complete compaction
of the material during final sintering. Shrinkage usually occurs during the process of sintering and can also
occur during debinding. Shrinkage can be compensated for by scaling up the green body dimensions, as
this is reproducible with a homogeneous distribution of particles in the green body, but not necessarily the
same in all spatial axes. While debinding is carried out purely thermally (usually in a temperature range
between 100 °C and 500 °C) or by means of a combination of solvent extraction or catalytic decomposition
of the organic components followed by thermal decomposition, sintering requires significantly higher
temperatures (usually >1 000 °C).
Machining is possible on the green body, the sintered white body, or on the sintered part, whereby the
demands on the machining process and tools increase from the green to the sintered body, but no further
shrinkage occurs on the sintered body. When machining the green or white body, the subsequent shrinkage
should be considered and compensated for accordingly.
© ISO/ASTM International 2026 – All rights reserved
Sintering leads to compaction and consolidation of the shaped body through the formation of material
bridges between the powder particles. Shrinkage occurs when internal porosity is filled and the volume
of the body decreases. Typical values for shrinkage in one spatial direction (linear shrinkage) are between
10 % and 20 %. Shrinkage depends on the characteristics of the feedstock and process control variables.
For volume shrinkage, this results in shrinkage of approximately 35 % to 65 %. The shrinkage should be
considered in the design of the green body by means of volume scaling.
In addition to traditional sintering, other process categories can be employed that are used to enhance the
densification of the ceramic once it has undergone initial sintering. For example, using a Hot Isostatic Press
(HIP), you can improve performance and achieve optimized grain growth control of the final part, which is
typically desired for high reliability applications like aerospace and medical.
4.4 General design recommendations for ceramic parts
Ductile materials compensate for local overloads with elastic strain according to Hooke’s Law and with the
plastic deformation behaviour. This does not apply to hard and brittle materials as they are not fault tolerant
and therefore less resilient under load. This means that there are significant differences in the load capacity
of parts made of ductile and brittle materials, such as metals and ceramics, respectively. This requires
different design guidelines.
Ceramic materials generally exhibit high compressive strength but low tensile strength. This behaviour
contrasts with the load capacity of metals and should be considered as a fundamental distinction when
designing parts. The second important aspect is the sintering process and the associated shrinkage. Due
to the complete lack of a ceramic’s ability to plasticly deform, ceramics fail spontaneously after elastic
deformation and when local material strength is reached. High stresses occur especially in small radii, sharp
edges, steps, shoulders, bores. This is further dramatized when sharp points or linear forces are applied.
Therefore, when designing a ceramic part, it is advisable to avoid geometric shapes that act as notches
(stress concentrations). A particular strength of ceramic materials is their high compressive strength. A
primary goal of a design suitable for ceramics should therefore be to make optimal use of this property
and to keep the number of areas in which the part is subjected to tensile and/or bending stress minimized.
Stress concentrations in tensile areas should be avoided.
These principles are often not given sufficient attention. There is frequently a desire to have a part that was
originally designed to be fabricated with metallic materials, to then be fabricated as a ceramic equivalent.
However, this can not only increase the manufacturing costs but also questions the feasibility of the
production in some cases. The difference in material properties should dictate how the part is intended to
be used in application, and therefore how it is designed and processed.
The following rules can be summarized as general design recommendations:
— avoid tensile stresses through geometric design;
— avoid notches, edges, and minimize surface roughness;
— avoid accumulations of material;
— consider build space size and shrinkage: due to shrinkage, the sintered parts are smaller than the
available build volume. If necessary, two parts can be joined together to form one larger, monolithic final
part.
5 Design freedom and limitations of additive manufacturing
5.1 General
The design rules for ceramic parts that can be found in the literature, generally refer to conventional ceramic
manufacturing processes. These rules thus consider the special features of the common primary moulding
processes of pressing and casting as well as the limitations of machining. In doing so, the advantages of AM
© ISO/ASTM International 2026 – All rights reserved
remain unused. The success of AM ceramic parts depends decisively on the consistent use of the advantages
of this technology, such as:
— functional orientation (see 5.2);
— integration of functions (see 5.3);
— freedom to use undercuts (see 5.4);
Other AM factors that can affect design that should also be considered are:
— Topology optimization (see 5.5);
— Part orientation and anisotropy (see 5.6);
— Supports (see 5.7);
— Surface finish (see 5.8);
— Porosity (see 5.9);
— Build platform interface (see 5.10).
5.2 Functional orientation
When designing a ceramic part for AM, the function should determine the geometry. Therefore, the design
of a part should first start from the functional features. These can be both connecting elements or other
non-connecting elements. The connecting elements can be freely combined in AM within the process-related
specifications. Their usage is essential to show added value to conventional manufacturing. The production
of openwork surfaces is possible without additional effort.
5.3 Integration of functions
AM allows for great geometric freedom. It should be used to combine design elements and, for example, to
use a support at the same time as a primary structure for heat transfer. Additionally, complex lattices could
be used to vary the part density throughout its volume, allowing not only for support variation of internal
features, but to also control centre of mass of the final part.
5.4 Freedom to use undercuts
With AM, the problem of support of undercuts practically no longer occurs. Penetrating holes and drill holes
can be manufactured regardless of accessibility. It is only necessary to ensure that the non-fused feedstock
and the material of the support can be removed from the holes. The production of any curves is possible.
Scaffold structures can be designed and finished as desired within wide limits.
5.5 Topology optimization
Topology optimization is a method by which a basic shape for parts under mechanical load can be optimized
in such a way that the material input is minimal. The method essentially consists of the following steps:
a) determination of the external dimensions of the part;
b) determination of all acting forces and fixed points;
c) calculation of the stresses occurring in the “volume” under the effect of force;
d) reduction of the volume according to the occurring stresses;
e) calculation of an optimal design proposal by software.
If a topology optimization is carried out based on an FEA simulation, geometric patterns are often created
that cannot be realised by means of conventional shaping, or only with a great deal of effort. This is why
© ISO/ASTM International 2026 – All rights reserved
AM processes, which allow for a maximum of geometric freedom without the use of tools or moulds, are the
obvious choice. The methods of topology optimization have been developed, and corresponding software
solutions are available.
The implementations have been developed for the field of plastics and metals and have proven their value,
especially regarding the aspect of lightweight design.
For the design of ceramic parts, however, not only the stresses occurring during application but also the
forces already acting during sintering due to shrinkage should be considered. Consequently, a topology-
optimized ceramic part should be evaluated and, if necessary, revised according to the design guidelines
presented here before production. Sharp internal angles and blind holes can lead to resin build up and are
difficult to clean out, so attention should be focused on these specific areas during topology optimization
and design in general. Uncured resin, leftover powder, or non-uniformly extruded paste that is trapped in
these regions can cause anisotropic sintering behaviour and put the fidelity of the final part at risk.
5.6 Part orientation and anisotropy
In AM, one layer is always consolidated, and this layer is bonded to the adjacent layers, so there is an inherent
difference in strength between two layers and within a layer.
Generally, the material bonding and thus the strength is higher in a layer than between layers. Due to the
layer-by-layer structure in AM, there is an inherent anisotropy of material properties in the green body. This
effect depends on the process, material and part and can be significantly reduced by proper process control.
In some cases, however, the sintered part still exhibits anisotropies. The anisotropy should therefore be
considered when designing the part and when orienting it in the build space.
5.7 Supports
5.7.1 General
AM parts can require supports, depending on the process and geometry. Reasons for the need for supports
include:
— overhangs, small downskin angles;
— connecting surface to the build platform being too small, e.g. with free-form geometries;
— necessary rigidity of the green body;
— forces experienced during the AM process.
When designing the supports, care should be taken to ensure that no parts of the supports are connected to
functional surfaces. Figure 7 shows two example situations where supports are warranted. The left diagram
shows the importance of using supports when the downskin angle is less than 45°, a common threshold
value, as measured from the horizontal. The right diagram shows a perpendicular overhang, which is only
achievable (without overhangs) for a very short overhang length. Furthermore, supports should be designed
such that the effort to remove them is minimized.
© ISO/ASTM International 2026 – All rights reserved
Key
1 support structure
2 a > threshold
Figure 7 — Downskin areas (overhangs) that require supports
5.7.2 Support material the same as part material
Since AM processes for ceramic parts usually produce green bodies first, it is possible to manually remove
the supports in this soft state.
Under certain circumstances, supports on the part are needed to avoid deformation during sintering. In this
case, the supports are usually removed after sintering using a grinding apparatus.
5.7.3 Support material not the same as part material
In this case, the support should be removed before sintering. The support material is selected to be removable
from the part chemically or thermally. This is usually gentler on the part than mechanical removal of the
support.
If the support does not have to be removed mechanically, there are further degrees of freedom for its design
and thus also for the design of the part. Thus, supports with lattice structures in cavities can also serve as
stiffeners.
Lattice structures for supports can be designed in a wide range. The thinnest geometry that can be produced
should not be undercut. If necessary, make sure that loose feedstock can be removed. Especially with fine
structures, the build direction and the associated stair-step effect (see 5.8) should also be considered.
5.8 Surface finish
5.8.1 General
The surface quality of AM parts is influenced primarily by the layer-by-layer structure (stair-step effect) and
secondarily by the particle size of the feedstock. Depending on the application, post-processing, usually in
the form of Computer Numerical Control (CNC) milling, is often necessary.
The deviations in dimensional accuracy and positional accuracy of AM parts should be considered. For
functional surfaces, an oversize for reworking should therefore be provided, if necessary. Required
dimensional accuracy can be adjusted by specific finishing strategies.
5.8.2 Stair-step effect
Due to the layer-by-layer production, the 3D geometry of the part is converted into an approximate contour
before production, resulting in a deviation, the so-called stair-step effect (also called staircase effect). The
stair-step effect depends largely on the layer thickness, which the surface finish positively scales with (see
Figure 8).
© ISO/ASTM International 2026 – All rights reserved
Figure 8 — Stair-step effect with different layer thicknesses
5.9 Porosity
The porosity of AM ceramic parts depends on the process and material parameters. Highly filled feedstock
with densely packed fine ceramic powder particles, or preceramic compounds with a high ceramic yield,
enable porosities of the sintered part to be close to zero. Consequently, processes with liquid or plastic
feedstock are particularly suitable for producing dense parts. The prerequisite for this is correct execution
of the subsequent thermal processing for defect-free debinding and sintering to achieve full density.
Additionally, infiltration can be employed to achieve high density.
If a certain degree of porosity is desired in the material, it is possible to add placeholder components that can
be burnt out, melted out or leached out. Also, the addition of coarse, possibly anisotropic powder particles to
the feedstock to artificially create pores in the material. At the same time or alternatively, it is also possible
to stop the sintering process before the maximum density is reached, provided that the temperature in the
final application of the part is significantly below the sintering temperature. Powder bed processes usually
use coarse, less sinter-active and thus poorly compacting raw materials. These are thus particularly suitable
for the implementation of an isotropic material porosity.
AM also enables the intentionally designed integration of macroscopic pores and pore channels into the parts,
e.g. to open new functionalities or to create lightweight structures. Here, the process-related limitations
of the manufacturing process categories should be considered, e.g. minimum web widths, minimum hole
diameters and the removal of excess feedstock.
5.10 Build platform interface
Strong consideration should be taken when designing how the part interfaces with the build platform. Part
removal can be tedious and lead to build surface defects in the green body that will remain with the part
until fully sintered. Due to the brittle nature of ceramics, even the smallest defect on the surface of a part can
be a failure initiation site and therefore should be avoided at all costs during the design stage. To mitigate
this risk, it is recommended to design supports that keep the part from interfacing with the platform and
where the supports can be removed later.
NOTE Some AM processes naturally avoid this risk due to how they function, such as with binder jetting and
powder bed fusion, which have a powder bed surrounding the part that provides natural support. The most at-risk
processes are vat photopolymerization and material extrusion.
© ISO/ASTM International 2026 – All rights reserved
6 Additive manufacturing process categories suitable for ceramics
6.1 General
An overview of the suitable manufacturing process categories for AM is given in Table 2. The properties of
the individual process categories are described in detail in 6.2 to 6.5. Three other manufacturing process
categories for producing ceramics additively from ISO/ASTM 52900 are not mentioned (directed energy
deposition, powder bed fusion and sheet lamination), primari
...
ISO/TC 261
Secretariat: DIN
Date: 2026-06-01xx
Additive manufacturing of ceramics — Design — Design guidelines
Fabrication additive de céramiques — Conception — Lignes directrices relatives à la conception
FDIS stage
TThhiis drs draafftt i is s susubbmmiitttteed d ttoo aa ppaarraallellel l vvoottee i inn IISSOO,, CCEEN.N.
© ISO/ASTM International 2026
All rights reserved. Unless otherwise specified, or required in the context of its implementation, no part of this publication
may be reproduced or utilized otherwise in any form or by any means, electronic or mechanical, including photocopying,
or posting on the internet or an intranet, without prior written permission. Permission can be requested from either ISO
at the address below or ISO’s member body in the country of the requester. In the United States, such requests should be
sent to ASTM International.
ISO copyright office ASTM International
CP 401 • Ch. de Blandonnet 8 100 Barr Harbor Drive, PO Box C700
CH-1214 Vernier, Geneva West Conshohocken, PA 19428-2959, USA
Phone: + 41 22 749 01 11 Phone: +610 832 9634
Fax: +41 22 749 09 47 Fax: +610 832 9635
Email: Email: khooper@astmE-mail: copyright@iso.org
Website: www.iso.org Website:
Published in Switzerland
© ISO/ASTM 2026 – All rights reserved
ii
Contents
Foreword . iv
1 Scope . 1
2 Normative references . 1
3 Terms and definitions . 1
4 Manufacture and properties of ceramic parts . 4
4.1 General . 4
4.2 Properties and applications . 4
4.3 Ceramic manufacturing process . 9
4.4 General design recommendations for ceramic parts . 11
5 Design freedom and limitations of additive manufacturing . 12
5.1 General . 12
5.2 Functional orientation . 12
5.3 Integration of functions . 12
5.4 Freedom to use undercuts . 12
5.5 Topology optimization . 12
5.6 Part orientation and anisotropy . 13
5.7 Supports . 13
5.8 Surface finish . 14
5.9 Porosity . 15
5.10 Build platform interface . 15
6 Additive manufacturing process categories suitable for ceramics . 16
6.1 General . 16
6.2 Material extrusion (MEX) — Cold plastics and thermoplastics . 18
6.3 Binder jetting (BJT) . 19
6.4 Vat photopolymerization (VPP) . 21
6.5 Material jetting (MJT) . 23
7 Specific strengths and application fields . 25
7.1 General . 25
7.2 Material extrusion . 25
7.3 Binder jetting . 25
7.4 Vat photopolymerization . 25
7.5 Material jetting . 25
Bibliography . 27
© ISO/ASTM 2026 – All rights reserved
iii
Foreword
The International Organization for Standardization (ISO) is a worldwide federation of national standards
bodies (ISO member bodies). The work of preparing International Standards is normally carried out through
ISO technical committees. Each member body interested in a subject for which a technical committee has been
established has the right to be represented on that committee. International organizations, governmental and
non-governmental, in liaison with ISO, also take part in the work. ISO collaborates closely with the
International Electrotechnical Commission (IEC) on all matters of electrotechnical standardization.
The procedures used to develop this document and those intended for its further maintenance are described
in the ISO/IEC Directives, Part 1. In particular, the different approval criteria needed for the different types of
ISO document should be noted. This document was drafted in accordance with the editorial rules of the
ISO/IEC Directives, Part 2 (see www.iso.org/directives).
ISO draws attention to the possibility that the implementation of this document may involve the use of (a)
patent(s). ISO takes no position concerning the evidence, validity or applicability of any claimed patent rights
in respect thereof. As of the date of publication of this document, ISO had not received notice of (a) patent(s)
which may be required to implement this document. However, implementers are cautioned that this may not
represent the latest information, which may be obtained from the patent database available at
www.iso.org/patents. ISO shall not be held responsible for identifying any or all such patent rights.
Any trade name used in this document is information given for the convenience of users and does not
constitute an endorsement.
For an explanation of the voluntary nature of standards, the meaning of ISO specific terms and expressions
related to conformity assessment, as well as information about ISO's adherence to the World Trade
Organization (WTO) principles in the Technical Barriers to Trade (TBT), see
www.iso.org/iso/foreword.html.The committee responsible for this
This document iswas prepared by Technical Committee ISO/TC 261, Additive manufacturing, in cooperation
with ASTM Committee F42, Additive Manufacturing Technologies, on the basis of a partnership agreement
between ISO and ASTM International with the aim to create a common set of ISO/ASTM standards on Additive
Manufacturing, in collaboration with the European Committee for Standardization (CEN) Technical
Committee CEN/TC 438, Additive manufacturing, in accordance with the Agreement on technical cooperation
between ISO and CEN (Vienna Agreement).
Any feedback or questions on this document should be directed to the user’s national standards body. A
complete listing of these bodies can be found at www.iso.org/members.html.
© ISO/ASTM 2026 – All rights reserved
iv
Additive manufacturing of ceramics — Design — Design guidelines
1 Scope
This document specifies part properties, design freedom, strengths and applications of additively
manufactured (AM) ceramic materials. It is aimed at product planners and designers and provides the
necessary basic knowledge about ceramics and the possibilities specific to AM ceramics, including strengths
and limitations of the most utilized ceramic AM process categories. In-depth previous knowledge in these
areas is not assumed.
2 Normative references
The following document is referred to in the text in such a way that some or all their content constitutes
requirements of this document. For dated references, only the edition cited applies. For undated references,
the latest edition of the referenced document (including any amendments) applies.
ISO/ASTM 52900, Additive manufacturing — General principles — Fundamentals and vocabulary
ISO/ASTM 52910, Additive manufacturing — Design — Requirements, guidelines and recommendations
ISO/ASTM 52915:20, Specification for Additive Manufacturing File Format (AMF)
ISO/ASTM 52921-13, Standard Terminology for Additive Manufacturing – Coordinate Systems and Test
Methodologies
ASTM WK83109, New Guide for Additive Manufacturing – Design – Vat Photopolymerization
ISO 2768-1, General tolerances — Part 1: Tolerances for linear and angular dimensions without individual
tolerance indications
ISO 2768-2, General tolerances – Part 2: Geometrical tolerances for features without individual tolerance
indications
3 Terms and definitions
For the purposes of this document, the terms and definitions given in ISO/ASTM 52900 and the following
apply:
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— — ISO Online browsing platform: available at https://www.iso.org/obp
— — IEC Electropedia: available at https://www.electropedia.org/
3.1 3.1
binder system
mixture of different organic or inorganic materials that after curing/drying/solidification bind the particulate
material together forming the green body (3.8) before shaping
3.2 3.2
brown body
green body (3.8) that has undergone pyrolysis/debinding (3.4)
© ISO/ASTM 2026 – All rights reserved
Note 1 to entry: The brown body has very low mechanical strength, as the individual particles adhere to each other
solely due to surface forces as well as frictional and positive locking. In some cases, decomposition products of some
binders can assist with strengthening the brown body.
3.3 3.3
ceramic
any material that classifiesis classified as an inorganic, non-metallic crystalline solid
3.4 3.4
cleaning
removal of adhering excess of feedstock from the green body (3.8)
3.5 3.5
debinding
process of removing all binder from the green body (3.8)
3.6 3.6
downskin angle,
δ
angle between the build platform plane and a downskin area, D, whose value lies between 0° (parallel to the
build platform) and 90° (perpendicular to the build platform). Reference Figure 1.)
Note 1 to entry: See Figure 152957_ed1fig1.EPS
.
Key
D downskin area
U upskin area
⇀𝑛𝑛 normal vector
Figure 1 — — Upskin angle (, υ), and downskin angle (, δ), according to VDI 3405- Blatt 3.2
3.7 3.7
granulate
solid, flowable feedstock for powder bed-based AM processes
Note 1 to entry: Granulate is a specially produced compound of many individual powder particles that has significantly
improved flow properties compared to a standard powder.
3.8 3.8
green body
part in intermediate state of processing, where the intended geometrical shape is given, but the bonding of the
intended part material is yet to be established (which occurs during sintering (3.14)))
© ISO/ASTM 2026 – All rights reserved
Note 1 to entry: For multi-step ceramic processes, the green body typically will consist of a powder held together by the
binder system.
Note 2 to entry: The mechanical properties of a green body made from powder materials are essentially determined by
the binder system.
3.9 3.9
green machining
machining of the green body (3.8) to attain the desired geometry or surface quality
Note 1 to entry: Green processing can include the removal of supports and the integration of special geometric features.
3.10 3.10
hard machining
machining of the sintered part (3.13) to achieve the desired geometry, dimension, or surface quality to the
final dimension
Note 1 to entry: Due to the high hardness of the sintered part, hard machining is very time-consuming and places very
high demands on the machining processes and tools.
3.11 3.11
infiltration
process where a fluid material (liquid, vapor, or slurry) is introduced into the connected pores of a porous
ceramic preform
3.12 3.12
shrinkage
volume reduction of a part without mass change during sintering (3.14)
Note 1 to entry: Volume reduction due to material removal (machining) is not referred to as shrinkage.
3.13 3.13
sintered part
part after sintering (3.14) with the final (ceramic (3.3))) properties
3.14 3.14
sintering
thermal process for compacting and bonding the (ceramic (3.3))) particles, taking place at temperatures below
the melting temperature
Note 1 to entry: Generally, sintering is accompanied by shrinkage.
Note 2 to entry: The temperature during sintering is above the debinding temperature but below the melting
temperature of the ceramic material.
3.15 3.15
suspension
liquid feedstock with suspended particulate (i.e. ceramic (3.3) powder)
EXAMPLESEXAMPLE Slip, ink, paste, slurry, etc.
Note 1 to entry: The suspension can be solidified by removing components of the binder system or initiating cross-
linking reactions.
© ISO/ASTM 2026 – All rights reserved
3.16 3.16
undercut
design feature, such as a horizontal protrusion, cavity or internal channel, that juts out from the main body
and cannot be produced without supports
3.17 3.17
upskin angle,
υ
angle between the build platform plane and an upskin area, U, whose value lies between 0° (parallel to the
build platform) and 90° (perpendicular to the build platform). Reference Figure 1.)
Note 1 to entry: See Figure 13.18.
3.18
white machining
machining of the white body to realize the desired geometry or surface quality
Note 1 to entry: The subsequent shrinkage during sintering should be considered and compensated for by an
appropriate oversize.
Note 2 to entry: White machining processing can include the removal of supports and the integration of special
geometric features.
3.19
white body
green body (3.8) or brown body (3.2) in which initial sintering (3.14) of the particles, including the formation
of sinter necks, has been initiated by thermal treatment
Note 1 to entry: The mechanical strength of the white body is significantly higher than that of the brown body, but still
significantly lower than that of the sintered part.
4 Manufacture and properties of ceramic parts
4.1 General
In this clause, the properties and applications are first presented (see 4.24.2).). Then the ceramic
manufacturing process is explained (see 4.34.3),), from which general design recommendations are then
derived (see 4.44.4).).
4.2 Properties and applications
The specific properties of ceramic materials, which in various relationships typically cannot be matched by
other materials, offer versatile applications.
Compared to metals, ceramic materials can offer higher hardness, thermal resistance, corrosion resistance
and wear resistance, as well as lower density and thermal expansion. An essential difference between ceramic
materials and metals is that ceramics usually do not show plastic deformation but fail after elastic deformation
when the load limit is exceeded. An example are MAX (M AX ) phases, which can show plastic deformation
n+1 n
when a load is applied.
An overview of the properties of ceramic materials is given in Table 1Table 1. The last column lists properties
of structural steel for comparison. The properties listed in Table 1Table 1 can vary depending on the
processing and raw materials utilized. Note – Polymeric materials aren’t included due to their distinctly
different material properties.
NOTE Polymeric materials are not included due to their distinctly different material properties.
© ISO/ASTM 2026 – All rights reserved
Table 1 — 1 — Overview of typical properties of ceramic parts in comparison with structural
[[3]][[4] [3][4]]
steel
Material
Porcelain Aluminium Zirconium Silicon Silicon Structural
Material property
oxide oxide nitride carbide steel
a b c
(> 99 %) (3Y-TZP) (SSiN) (SSiC) St 37
Density
2,2 3,9 5…6 3,2…3,3 3,08…3,15 7,8
in g/cm
Hardness (Vickers)
5…9 13…23 10…14 14…18 22…34 2…4
in GPa
Flexural strength
50 300…450 500…1,000 700…1,000 260…500 340…470
in MPa
Young’s modulus
60 300 200…210 290…330 350…450 200…210
in GPa
Fracture toughness
– 4…5,5 5,8…10,5 5…8,5 3,0…4,8 200
1/2
in MPa m
Thermal expansion
4…7 7…8 10…12,5 2,5…3,5 4,0…4,8 10…12
–6 –1
in 10 K
a 3Y-TZP – tetragonally stabilized zirconium oxide with 3 % molar content of yttrium oxide.
b SiN – silicon nitride.
c SiC – silicon carbide.
Figure 2Figure 2 through Figure 5Figure 5 illustrate the relationship between different properties for selected
ceramics compared to metals. In this way, characteristics of ceramic materials can be both quickly compared
[3][4] [3][4]
among each other as well as to metals .
The literature values used in Figure 2Figure 2 through Figure 5Figure 5 were determined with standardized
test specimens from conventional manufacturing processes and are to provide general guideline comparisons.
In AM, there are different manufacturing process categories and material formulations, which means that the
property values can vary greatly. Porosity is particularly affected by this. For example, density and flexural
strength decrease as porosity increases. Because of this, it is advised that the investigator research the more
specific values for their ceramic system.
© ISO/ASTM 2026 – All rights reserved
52957_ed1fig2.EPS
Key
X density, in g/cm
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 2 — — Relationship between density and flexural strength for selected ceramics compared to
[3 [3]]
metals
© ISO/ASTM 2026 – All rights reserved
52957_ed1fig3.EPS
Key
X young’s modulus, in GPa
Y hardness, in GPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 3 — — Relationship between Young’s modulus and hardness for selected ceramics compared
[3 [3]]
to metal
© ISO/ASTM 2026 – All rights reserved
52957_ed1fig4.EPS
Key
‒1 ‒1
X thermal conductivity, in Wm ·K
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 4 — — Relationship between thermal conductivity and flexural strength for selected ceramics
[3 [3]]
compared to metals
© ISO/ASTM 2026 – All rights reserved
52957_ed1fig5.EPS
Key
‒1 ‒6
X coefficient of expansion, in 10 K
Y flexural strength, in MPa
1 silicon nitride
2 silicate ceramics
3 silicon carbide
4 aluminium oxide
5 zirconium oxide
6 metals
Figure 5 — — Relationship between coefficient of expansion and flexural strength for selected
[3 [3]]
ceramics compared to metals
4.3 Ceramic manufacturing process
The same basic process principle applies to all ceramic materials for conventional and AM (see
Figure 6Figure 6).). From the mostly powdery feedstock, it is first prepared from which a green body is created
during the subsequent shaping process. The green body corresponds to a composite material consisting of an
organic matrix and ceramic particles embedded in it. With AM, the green body is built up layer-by-layer based
on a CAD model. In conventional manufacturing, a tool (i.e.,. a moldmould) should be created for shaping.
© ISO/ASTM 2026 – All rights reserved
52957_ed1fig6.EPS
Figure 6 — — Schematic representation of the production process for technical ceramics
Subsequently, debinding and sintering of the parts are necessary to realize the ceramic properties in the part.
For AM parts, these two processes correspond to those conventionally manufactured, whereby the process
control should be adapted to the respective decomposition properties of the binder systems used as well as
to the realized volume fraction of ceramic material in the feedstock.
During debinding, all organic components are removed from the green body to allow complete compaction of
the material during final sintering. Shrinkage usually occurs during the process of sintering and can also occur
during debinding. Shrinkage can be compensated for by scaling up the green body dimensions, as this is
reproducible with a homogeneous distribution of particles in the green body, but not necessarily the same in
all spatial axes. While debinding is carried out purely thermally (usually in a temperature range between
100 °C and 500 °C) or by means of a combination of solvent extraction or catalytic decomposition of the
organic components followed by thermal decomposition, sintering requires significantly higher temperatures
(usually >1, 000 °C).
© ISO/ASTM 2026 – All rights reserved
Machining is possible on the green body, the sintered white body, or on the sintered part, whereby the
demands on the machining process and tools increase from the green to the sintered body, but no further
shrinkage occurs on the sintered body. When machining the green or white body, the subsequent shrinkage
should be considered and compensated for accordingly.
Sintering leads to compaction and consolidation of the shaped body through the formation of material bridges
between the powder particles. Shrinkage occurs when internal porosity is filled and the volume of the body
decreases. Typical values for shrinkage in one spatial direction (linear shrinkage) are between 10 % and 20 %.
Shrinkage depends on the characteristics of the feedstock and process control variables. For volume
shrinkage, this results in shrinkage of approximately 35 % to 65 %. The shrinkage should be considered in the
design of the green body by means of volume scaling.
In addition to traditional sintering, other process categories can be employed that are used to enhance the
densification of the ceramic once it has undergone initial sintering. For example, using a Hot Isostatic Press
(HIP), you can improve performance and achieve optimized grain growth control of the final part, which is
typically desired for high reliability applications like aerospace and medical.
4.4 General design recommendations for ceramic parts
Ductile materials compensate for local overloads with elastic strain according to Hooke’s Law and with the
plastic deformation behaviour. This does not apply to hard and brittle materials as they are not fault tolerant
and therefore less resilient under load. This means that there are significant differences in the load capacity
of parts made of ductile and brittle materials, such as metals and ceramics, respectively. This requires different
design guidelines.
Ceramic materials generally exhibit high compressive strength but low tensile strength. This behaviour
contrasts with the load capacity of metals and should be considered as a fundamental distinction when
designing parts. The second important aspect is the sintering process and the associated shrinkage. Due to the
complete lack of a ceramic’s ability to plasticly deform, ceramics fail spontaneously after elastic deformation
and when local material strength is reached. High stresses occur especially in small radii, sharp edges, steps,
shoulders, bores. This is further dramatized when sharp points or linear forces are applied.
Therefore, when designing a ceramic part, it is advisable to avoid geometric shapes that act as notches (stress
concentrations). A particular strength of ceramic materials is their high compressive strength. A primary goal
of a design suitable for ceramics should therefore be to make optimal use of this property and to keep the
number of areas in which the part is subjected to tensile and/or bending stress minimized. Stress
concentrations in tensile areas should be avoided.
These principles are often not given sufficient attention. There is frequently a desire to have a part that was
originally designed to be fabricated with metallic materials, to then be fabricated as a ceramic equivalent.
However, this can not only increase the manufacturing costs but also questions the feasibility of the
production in some cases. The difference in material properties should dictate how the part is intended to be
used in application, and therefore how it is designed and processed.
The following rules can be summarized as general design recommendations:
— — Avoidavoid tensile stresses through geometric design;
— — Avoidavoid notches, edges, and minimize surface roughness;
— — Avoidavoid accumulations of material;
— — Considerconsider build space size and shrinkage: Duedue to shrinkage, the sintered parts are smaller
than the available build volume. If necessary, two parts can be joined together to form one larger,
monolithic final part.
© ISO/ASTM 2026 – All rights reserved
5 Design freedom and limitations of additive manufacturing
5.1 General
The design rules for ceramic parts that can be found in the literature, generally refer to conventional ceramic
manufacturing processes. These rules thus consider the special features of the common primary
moldingmoulding processes of pressing and casting as well as the limitations of machining. In doing so, the
advantages of AM remain unused. The success of AM ceramic parts depends decisively on the consistent use
of the advantages of this technology, such as:
— — functional orientation (see 5.25.2));
— — integration of functions (see 5.35.3));
— — freedom to use undercuts (see 5.45.4));
Other AM factors that can affect design that should also be considered are:
— — Topology optimization (see 5.55.5));
— — Part orientation and anisotropy (see 5.65.6));
— — Supports (see 5.75.7));
— — Surface finish (see 5.85.8));
— — Porosity (see 5.95.9));
— — Build platform interface (see 5.105.10)).
5.2 Functional orientation
When designing a ceramic part for AM, the function should determine the geometry. Therefore, the design of
a part should first start from the functional features. These can be both connecting elements or other non-
connecting elements. The connecting elements can be freely combined in AM within the process-related
specifications. Their usage is essential to show added value to conventional manufacturing. The production of
openwork surfaces is possible without additional effort.
5.3 Integration of functions
AM allows for great geometric freedom. It should be used to combine design elements and, for example, to use
a support at the same time as a primary structure for heat transfer. Additionally, complex lattices could be
used to vary the part density throughout its volume, allowing not only for support variation of internal
features, but to also control centercentre of mass of the final part.
5.4 Freedom to use undercuts
With AM, the problem of support of undercuts practically no longer occurs. Penetrating holes and drill holes
can be manufactured regardless of accessibility. It is only necessary to ensure that the non-fused feedstock
and the material of the support can be removed from the holes. The production of any curves is possible.
Scaffold structures can be designed and finished as desired within wide limits.
5.5 Topology optimization
Topology optimization is a method by which a basic shape for parts under mechanical load can be optimized
in such a way that the material input is minimal. The method essentially consists of the following steps:
© ISO/ASTM 2026 – All rights reserved
a) — Determinationdetermination of the external dimensions of the part;
b) — Determinationdetermination of all acting forces and fixed points;
c) — Calculationcalculation of the stresses occurring in the “volume” under the effect of force;
d) — Reductionreduction of the volume according to the occurring stresses;
e) — Calculationcalculation of an optimal design proposal by software.
If a topology optimization is carried out based on an FEA simulation, geometric patterns are often created that
cannot be realised by means of conventional shaping, or only with a great deal of effort. This is why AM
processes, which allow for a maximum of geometric freedom without the use of tools or moldsmoulds, are the
obvious choice. The methods of topology optimization have been developed, and corresponding software
solutions are available.
The implementations have been developed for the field of plastics and metals and have proven their value,
especially regarding the aspect of lightweight design.
For the design of ceramic parts, however, not only the stresses occurring during application but also the forces
already acting during sinterin
...
PROJET FINAL
Norme
internationale
ISO/ASTM
FDIS
ISO/TC 261
Fabrication additive de
Secrétariat: DIN
céramiques — Conception — Lignes
Début de vote:
directrices relatives à la conception
2026-08-11
Additive manufacturing of ceramics — Design — Design
Vote clos le:
guidelines
2026-10-06
LES DESTINATAIRES DU PRÉSENT PROJET SONT
INVITÉS À PRÉSENTER, AVEC LEURS OBSERVATIONS,
NOTIFICATION DES DROITS DE PROPRIÉTÉ DONT ILS
AURAIENT ÉVENTUELLEMENT CONNAISSANCE ET À
FOURNIR UNE DOCUMENTATION EXPLICATIVE.
OUTRE LE FAIT D’ÊTRE EXAMINÉS POUR
ÉTABLIR S’ILS SONT ACCEPTABLES À DES FINS
INDUSTRIELLES, TECHNOLOGIQUES ET COM-MERCIALES,
AINSI QUE DU POINT DE VUE DES UTILISATEURS, LES
PROJETS DE NORMES
TRAITEMENT PARALLÈLE ISO/CEN
INTERNATIONALES DOIVENT PARFOIS ÊTRE CONSIDÉRÉS
DU POINT DE VUE DE LEUR POSSI BILITÉ DE DEVENIR DES
NORMES POUVANT
SERVIR DE RÉFÉRENCE DANS LA RÉGLEMENTATION
NATIONALE.
Numéro de référence
PROJET FINAL
Norme
internationale
ISO/ASTM
FDIS
ISO/TC 261
Fabrication additive de
Secrétariat: DIN
céramiques — Conception — Lignes
Début de vote:
directrices relatives à la conception
2026-08-11
Additive manufacturing of ceramics — Design — Design
Vote clos le:
guidelines
2026-10-06
LES DESTINATAIRES DU PRÉSENT PROJET SONT
INVITÉS À PRÉSENTER, AVEC LEURS OBSERVATIONS,
NOTIFICATION DES DROITS DE PROPRIÉTÉ DONT ILS
DOCUMENT PROTÉGÉ PAR COPYRIGHT
AURAIENT ÉVENTUELLEMENT CONNAISSANCE ET À
FOURNIR UNE DOCUMENTATION EXPLICATIVE.
© ISO/ASTM International 2026
OUTRE LE FAIT D’ÊTRE EXAMINÉS POUR
ÉTABLIR S’ILS SONT ACCEPTABLES À DES FINS
Tous droits réservés. Sauf prescription différente ou nécessité dans le contexte de sa mise en œuvre, aucune partie de cette
INDUSTRIELLES, TECHNOLOGIQUES ET COM-MERCIALES,
publication ne peut être reproduite ni utilisée sous quelque forme que ce soit et par aucun procédé, électronique ou mécanique,
AINSI QUE DU POINT DE VUE DES UTILISATEURS, LES
y compris la photocopie, ou la diffusion sur l’internet ou un intranet, sans autorisation écrite soit de l’ISO à l’adresse ci-après,
PROJETS DE NORMES
TRAITEMENT PARALLÈLE ISO/CEN
INTERNATIONALES DOIVENT PARFOIS ÊTRE CONSIDÉRÉS
soit d’un organisme membre de l’ISO dans le pays du demandeur. Aux États-Unis, les demandes doivent être adressées à ASTM
DU POINT DE VUE DE LEUR POSSI BILITÉ DE DEVENIR DES
International.
NORMES POUVANT
ISO copyright office ASTM International SERVIR DE RÉFÉRENCE DANS LA RÉGLEMENTATION
NATIONALE.
Case postale 401 • Ch. de Blandonnet 8 100 Barr Harbor Drive, PO Box C700
CH-1214 Vernier, Genève West Conshohocken, PA 19428-2959, USA
Tél.: +41 22 749 01 11 Tél.: +610 832 9634
Fax: +610 832 9635
E-mail: copyright@iso.org E-mail: khooper@astm.org
Web: www.iso.org Web: www.astm.org
Publié en Suisse Numéro de référence
© ISO/ASTM International 2026 – Tous droits réservés
ii
Sommaire Page
Avant-propos .iv
1 Domaine d’application . 1
2 Références normatives . 1
3 Termes et définitions . 1
4 Fabrication et propriétés des pièces en céramique . 4
4.1 Généralités .4
4.2 Propriétés et applications . .4
4.3 Procédé de fabrication céramique .9
4.4 Recommandations générales de conception pour pièces en céramique .11
5 Liberté de conception et limites de la fabrication additive.12
5.1 Généralités . 12
5.2 Orientation fonctionnelle . 12
5.3 Intégration des fonctions . 12
5.4 Liberté d'utiliser des dégagements . 12
5.5 Optimisation de la topologie . 13
5.6 Orientation et anisotropie des pièces . 13
5.7 Support . 13
5.7.1 Généralités . 13
5.7.2 Matériau de support identique au matériau de la pièce .14
5.7.3 Matériau de support non identique au matériau de la pièce .14
5.8 Finition de surface .14
5.8.1 Généralités .14
5.8.2 Effet d’escalier . 15
5.9 Porosité . 15
5.10 Interface de la plateforme de fabrication.16
6 Catégories de procédés de fabrication additive adaptées aux céramiques .16
6.1 Généralités .16
6.2 Extrusion de matériau (MEX) — Plastiques et thermoplastiques à froid .18
6.2.1 Généralités .18
6.2.2 Description du procédé .18
6.2.3 Caractéristiques spéciales liées au procédé pour la conception .19
6.3 Projection de liant (BJT) .19
6.3.1 Généralités .19
6.3.2 Description du procédé – Matière première en poudre . 20
6.3.3 Description du procédé – Matière première en suspension . 20
6.3.4 Caractéristiques spéciales liées au procédé pour la conception . 20
6.4 Photopolymérisation en cuve (VPP) . 20
6.4.1 Généralités . 20
6.4.2 Description du procédé . 22
6.4.3 Caractéristiques spéciales liées au procédé de conception . 23
6.5 Projection de matériau (MJT) . 23
6.5.1 Généralités . 23
6.5.2 Description du procédé .24
6.5.3 Caractéristiques spéciales liées au procédé pour la conception .24
7 Points forts et champs d'application spécifiques .25
7.1 Généralités . 25
7.2 Extrusion de matériau . 25
7.3 Projection de liant . 25
7.4 Photopolymérisation en cuve . 25
7.5 Projection de matériau . 26
Bibliographie .27
© ISO/ASTM International 2026 – Tous droits réservés
iii
Avant-propos
L'Organisation internationale de normalisation (ISO) est une fédération mondiale d'organismes nationaux
de normalisation (comités membres de l'ISO). L'élaboration des Normes internationales est en général
confiée aux comités techniques de l'ISO. Chaque comité membre intéressé par une étude a le droit de faire
partie du comité technique créé à cet effet. Les organisations internationales, gouvernementales et non
gouvernementales, en liaison avec l'ISO participent également aux travaux. L'ISO collabore étroitement avec
la Commission électrotechnique internationale (IEC) en ce qui concerne la normalisation électrotechnique.
Les procédures utilisées pour élaborer le présent document et celles destinées à sa mise à jour sont
décrites dans les Directives ISO/IEC, Partie 1. Il convient, en particulier, de prendre note des différents
critères d'approbation requis pour les différents types de documents ISO. Le présent document a
été rédigé conformément aux règles de rédaction données dans les Directives ISO/IEC, Partie 2 (voir
www.iso.org/directives).
L'ISO attire l'attention sur le fait que la mise en application du présent document peut entraîner l'utilisation
d'un ou de plusieurs brevets. L'ISO ne prend pas position quant à la preuve, à la validité et à l'applicabilité de
tout droit de brevet revendiqué à cet égard. À la date de publication du présent document, l'ISO n'avait pas
reçu notification qu'un ou plusieurs brevets pouvaient être nécessaires à sa mise en application. Toutefois,
il y a lieu d'avertir les responsables de la mise en application du présent document que des informations
plus récentes sont susceptibles de figurer dans la base de données de brevets, disponible à l'adresse
www.iso.org/brevets. L'ISO ne saurait être tenue pour responsable de ne pas avoir identifié tout ou partie de
tels droits de brevet.
Les appellations commerciales éventuellement mentionnées dans le présent document sont données pour
information, par souci de commodité, à l’intention des utilisateurs et ne sauraient constituer un engagement.
Pour une explication de la nature volontaire des normes, la signification des termes et expressions
spécifiques de l'ISO liés à l'évaluation de la conformité, ou pour toute information au sujet de l'adhésion de
l'ISO aux principes de l’Organisation mondiale du commerce (OMC) concernant les obstacles techniques au
commerce (OTC), voir www.iso.org/avant-propos.
Le présent document a été élaboré par le comité technique ISO/TC 261, Fabrication additive, en coopération
avec le comité ASTM F42, Technologies de fabrication additive, dans le cadre d'un accord de partenariat entre
l'ISO et ASTM International dans le but de créer un ensemble commun de normes ISO/ASTM sur la fabrication
additive, et en collaboration avec le comité technique CEN/TC 438, Fabrication additive, du Comité européen
de normalisation (CEN) conformément à l'Accord de coopération technique entre l'ISO et le CEN (Accord de
Vienne).
Il convient que l'utilisateur adresse tout retour d'information ou toute question concernant le présent
document à l'organisme national de normalisation de son pays. Une liste exhaustive desdits organismes se
trouve à l'adresse www.iso.org/fr/members.html.
© ISO/ASTM International 2026 – Tous droits réservés
iv
PROJET FINAL Norme internationale ISO/ASTM FDIS 52957:2026(fr)
Fabrication additive de céramiques — Conception — Lignes
directrices relatives à la conception
1 Domaine d’application
Le présent document spécifie les propriétés des pièces, la liberté de conception, les points forts et les
applications des matériaux céramiques fabriqués additivement (FA). Il s’adresse aux planificateurs et aux
concepteurs de produits et fournit les connaissances de base nécessaires sur les céramiques et les possibilités
spécifiques aux céramiques en FA, y compris les points forts et les limites des catégories de procédés de FA
les plus utilisées. Des connaissances préalables approfondies dans ces domaines ne sont pas présumées.
2 Références normatives
Les documents suivants sont cités dans le texte de sorte qu’ils constituent, pour tout ou partie de leur
contenu, des exigences du présent document. Pour les références datées, seule l’édition citée s’applique. Pour
les références non datées, la dernière édition du document de référence s'applique (y compris les éventuels
amendements).
ISO/ASTM 52900, Fabrication additive — Principes généraux — Fondamentaux et vocabulaire
3 Termes et définitions
Pour l'application du présent document, les termes et les définitions de l'ISO/ASTM 52900 ainsi que les
suivants s'appliquent.
L'ISO et l'IEC tiennent à jour des bases de données terminologiques destinées à être utilisées en normalisation,
consultables aux adresses suivantes:
— ISO Online browsing platform: disponible à l'adresse https:// www .iso .org/ obp
— IEC Electropedia: disponible à l'adresse https:// www .electropedia .org/
3.1
système de liant
mélange de différentes matières organiques ou inorganiques qui après durcissement/séchage/solidi-fication
lie le matériau particulaire ensemble en formant l’ébauche (3.8) avant la mise en forme
3.2
corps brun
ébauche (3.8) ayant subi une pyrolyse/un déliantage (3.4)
Note 1 à l'article: Le corps brun a une très faible résistance mécanique, car les particules individuelles adhèrent les
unes aux autres uniquement en raison des forces de surface ainsi que du frottement et du verrouillage positif.
3.3
céramique
tout matériau qui est classifié comme un solide cristallin inorganique et non métallique
3.4
déliantage
retrait d'excédent de matière première adhérant à l'ébauche (3.8)
© ISO/ASTM International 2026 – Tous droits réservés
3.5
déliantage
processus d'élimination de tous les composants organiques de l’ébauche (3.8)
3.6
angle de la contre-dépouille
δ
angle entre le plan de la plateforme de fabrication et la surface de contre-dépouille, D, dont la valeur est
comprise entre 0° (parallèlement à la plateforme de fabrication) et 90° (perpendiculairement à la plateforme
de fabrication).
Note 1 à l'article: Voir la Figure 1.
Légende
D surface de contre-dépouille
U surface de dépouille
n vecteur normal
Figure 1 — Angle de la dépouille, υ, et angle de la contre-dépouille, δ, selon VDI 3405 Blatt 3.2
3.7
granulé
matière première solide et apte à l'écoulement pour les procédés de FA sur lit de poudre
Note 1 à l'article: Le granulé est un composé spécialement fabriqué à partir de nombreuses particules de poudre
individuelles, dont les propriétés d'écoulement sont considérablement améliorées par rapport à une poudre standard.
3.8
ébauche
pièce dans un état de traitement intermédiaire, où la forme géométrique voulue est donnée, mais la liaison
avec le matériau de la pièce voulue est encore à établir (ce qui a lieu pendant le frittage (3.14))
Note 1 à l'article: Pour les procédés céramiques à plusieurs étapes, l'ébauche va généralement consister en une poudre
maintenue par le système de liant.
Note 2 à l'article: Les caractéristiques mécaniques d'une ébauche faite à partir de matériaux en poudre sont
essentiellement déterminées par le système de liant.
3.9
usinage à cru
usinage de l’ébauche (3.8) pour obtenir la géométrie ou la qualité de surface souhaitée
Note 1 à l'article: L'usinage à cru peut comprendre l'élimination de supports et l'intégration de caractéristiques
géométriques spéciales.
© ISO/ASTM International 2026 – Tous droits réservés
3.10
usinage dur
usinage de la pièce frittée (3.13) pour obtenir la géométrie, les dimensions ou la qualité de surface de la
dimension finale souhaitée
Note 1 à l'article: En raison de la dureté élevée de la pièce frittée, l'usinage dur prend beaucoup de temps et impose des
contraintes très élevées aux procédés et aux outils d'usinage.
3.11
infiltration
processus au cours duquel un matériau fluide (liquide, vapeur ou barbotine) est introduit dans les pores
connectées d'une préforme en céramique poreuse
3.12
rétrécissement
réduction du volume d'une pièce sans altération de la masse pendant le frittage (3.14)
Note 1 à l'article: La réduction du volume due à l'enlèvement de matière (usinage) n'est pas appelée rétrécissement.
3.13
pièce frittée
pièce après frittage (3.14) avec les propriétés (céramiques (3.3)) finales
3.14
frittage
procédé thermique de compactage et d’adhésion des particules (céramiques (3.3)), se déroulant à des
températures inférieures à la température de fusion
Note 1 à l'article: En général, le frittage s'accompagne d'un rétrécissement.
Note 2 à l'article: La température pendant le frittage est supérieure à la température de déliantage mais inférieure à la
température de fusion du matériau céramique.
3.15
suspension
matière première liquide avec particules en suspension (c'est-à-dire de la poudre de céramiques (3.3))
EXEMPLE Barbotine, encre, pâte, boue, etc.
Note 1 à l'article: La suspension peut être solidifiée en éliminant les composants du système de liant ou en initiant des
réactions de réticulation.
3.16
dégagement
caractéristique de conception, telle qu'une protrusion horizontale, une cavité ou un canal interne qui
dépasse du corps principal et ne peut être produite sans supports
3.17
angle de la dépouille
υ
angle entre le plan de la plateforme de fabrication et la surface de dépouille U dont la valeur est comprise
entre 0° (parallèlement à la plateforme de fabrication) et 90° (perpendiculairement à la plateforme de
fabrication)
Note 1 à l'article: Voir la Figure 1.
3.18
usinage blanc
usinage du corps blanc pour obtenir la géométrie ou la qualité de surface souhaitée
Note 1 à l'article: Il convient que le rétrécissement qui s'ensuit pendant le frittage soit pris en compte et compensé par
un surdimensionnement approprié.
© ISO/ASTM International 2026 – Tous droits réservés
Note 2 à l'article: L'usinage blanc peut comprendre l'élimination des supports et l'intégration de caractéristiques
géométriques spéciales.
3.19
corps blanc
ébauche (3.8) ou corps brun (3.2) dans lequel le frittage (3.14) initial des particules, y compris la formation
de cols de frittage, a été initié par un traitement thermique
Note 1 à l'article: La résistance mécanique du corps blanc est nettement supérieure à celle du corps brun, mais reste
nettement inférieure à celle de la pièce frittée.
4 Fabrication et propriétés des pièces en céramique
4.1 Généralités
Dans le présent article, les propriétés et les applications sont d'abord présentées (voir 4.2). Le procédé de
fabrication de la céramique est ensuite expliqué (voir 4.3), ce qui permet de dégager des recommandations
générales relatives à la conception (voir 4.4).
4.2 Propriétés et applications
Les propriétés spécifiques des matériaux céramiques, qui ne peuvent généralement pas être égalées par
d'autres matériaux, offrent des applications polyvalentes.
Par rapport aux métaux, les matériaux céramiques peuvent offrir une dureté, une résistance thermique,
une résistance à la corrosion et une résistance à l'usure plus élevées, ainsi qu'une densité et une dilatation
thermique plus faibles. Une différence essentielle entre les matériaux céramiques et les métaux est que les
céramiques ne présentent généralement pas de déformation plastique, mais présentent une défaillance
après une déformation élastique lorsque la limite de charge est dépassée. Les phases MAX (M AX ) en sont
n+1 n
un exemple qui démontre la déformation plastique lorsqu'une charge est appliquée.
Le Tableau 1 donne un aperçu des propriétés des matériaux céramiques. La dernière colonne énumère les
propriétés de l'acier de construction à des fins de comparaison. Les propriétés énumérées dans le Tableau 1
peuvent varier en fonction de la transformation et des matériaux bruts utilisés.
NOTE Les matériaux polymériques ne sont pas inclus en raison de leurs propriétés de matériaux distinctement
différentes.
© ISO/ASTM International 2026 – Tous droits réservés
Tableau 1 — Aperçu des propriétés typiques des pièces en céramique par rapport à l'acier de
[3],[4]
construction
Matériau
Propriétés des maté-
Porcelaine Oxyde d'alu- Oxyde de Nitrure de Carbure de Acier de
riaux
minium zirconium silicium silicium construction
a b c
(>99 %) (3Y-TZP) (SSiN) (SSiC) St 37
Densité
2,2 3,9 5.6 3,2…3,3 3,08…3,15 7,8
en g/cm
Dureté (Vickers)
5…9 13…23 10…14 14…18 22…34 2…4
en GPa
Résistance à la
flexion
50 300…450 500…1 000 700…1 000 260…500 340…470
en MPa
Module de Young
60 300 200…210 290…330 350…450 200…210
en GPa
Ténacité à la rupture
– 4…5,5 5,8…10,5 5…8,5 3,0…4,8 200
1/2
en MPa m
Dilatation thermique
4…7 7…8 10…12,5 2,5…3,5 4,0…4,8 10…12
−6 –1
en 10 K
a
3Y-TZP – oxyde de zirconium stabilisé tétragonalement avec une teneur molaire de 3 % d'oxyde d'yttrium.
b
SiN - nitrure de silicium.
c
SiC - carbure de silicium.
La Figure 2 à la Figure 5 illustrent la relation entre les différentes propriétés des céramiques sélectionnées
par rapport à celles des métaux. De cette manière, les caractéristiques des matériaux céramiques peuvent
[3],[4]
être rapidement comparées entre elles et avec celles des métaux .
Les valeurs indiquées dans la littérature utilisées à la Figure 2 à la Figure 5 ont été déterminées à l'aide
d'éprouvettes normalisées issues de procédés de fabrication conventionnels et ont à fournir des comparaisons
de lignes directrices générales. Dans la FA, il existe différentes catégories de procédés de fabrication et
formulations de matériaux, ce qui signifie que les valeurs des propriétés peuvent varier considérablement.
La porosité est particulièrement affectée par ce phénomène. Par exemple, la densité et la résistance à la
flexion diminuent lorsque la porosité augmente. Pour cette raison, il est conseillé que le chercheur recherche
les valeurs spécifiques pour leur système céramique.
© ISO/ASTM International 2026 – Tous droits réservés
Légende
X densité, en g/cm
Y résistance à la flexion, en MPa
1 nitrure de silicium
2 céramiques silicatées
3 carbure de silicium
4 oxyde d'aluminium
5 oxyde de zirconium
6 métaux
Figure 2 — Relation entre la densité et la résistance à la flexion pour les céramiques sélectionnées
[3]
par rapport aux métaux
© ISO/ASTM International 2026 – Tous droits réservés
Légende
X module de Young, en GPa
Y dureté, en GPa
1 nitrure de silicium
2 céramiques silicatées
3 carbure de silicium
4 oxyde d'aluminium
5 oxyde de zirconium
6 métaux
Figure 3 — Relation entre le module de Young et la dureté pour les céramiques sélectionnées par
[3]
rapport au métal
© ISO/ASTM International 2026 – Tous droits réservés
Légende
‒1 ‒1
X conductivité thermique, en Wm K
Y résistance à la flexion, en MPa
1 nitrure de silicium
2 céramiques silicatées
3 carbure de silicium
4 oxyde d'aluminium
5 oxyde de zirconium
6 métaux
Figure 4 — Relation entre la conductivité thermique et la résistance à la flexion pour les céramiques
[3]
sélectionnées par rapport aux métaux
© ISO/ASTM International 2026 – Tous droits réservés
Légende
‒1 ‒6
X coefficient de dilatation, en 10 K
Y résistance à la flexion, en MPa
1 nitrure de silicium
2 céramiques silicatées
3 carbure de silicium
4 oxyde d'aluminium
5 oxyde de zirconium
6 métaux
Figure 5 — Relation entre le coefficient de dilatation et la résistance à la flexion pour les céramiques
[3]
sélectionnées par rapport aux métaux
4.3 Procédé de fabrication céramique
Le même principe de procédé de base s'applique à tous les matériaux céramiques pour la fabrication
conventionnelle et la FA (voir la Figure 6). À partir des matières premières essentiellement poudreuses, il est
d’abord préparé à partir de laquelle une ébauche est créée au cours du procédé de mise en forme ultérieur.
L’ébauche correspond à un matériau composite composé d'une matrice organique et de particules de
céramique incorporées. Avec la FA, l’ébauche est fabriquée couche par couche sur la base d'un modèle CAO.
Dans la fabrication conventionnelle, il convient qu’un outil (c'est-à-dire un moule) soit créé pour la mise en
forme.
© ISO/ASTM International 2026 – Tous droits réservés
Figure 6 — Représentation schématique du processus de production des céramiques techniques
Ensuite, le déliantage et le frittage des pièces sont nécessaires pour obtenir les propriétés céramiques
de la pièce. Pour les pièces FA, ces deux procédés correspondent à ceux qui sont fabriqués de manière
conventionnelle, pour lesquels il convient que le contrôle du processus soit adapté aux propriétés de
décomposition respectives des systèmes de liants utilisés ainsi qu'à la fraction volumique réalisée du
matériau céramique dans la matière première.
Lors du déliantage, tous les composants organiques sont retirés de l’ébauche afin de permettre un compactage
complet du matériau lors du frittage final. Le rétrécissement se produit généralement pendant le procédé
de frittage et peut également se produire pendant le déliantage. Le rétrécissement peut être compensé
en augmentant les dimensions de l’ébauche, car il est reproductible avec une distribution homogène des
particules dans l’ébauche, mais pas nécessairement la même dans tous les axes spatiaux. Alors que le
déliantage est réalisé uniquement thermiquement (généralement dans une plage de température comprise
entre 100 °C et 500 °C) ou par une combinaison d'extraction par solvant ou de décomposition catalytique des
composants organiques suivie d'une décomposition thermique, le frittage exige des températures nettement
plus élevées (généralement > 1 000 °C).
L'usinage est possible sur l’ébauche, le corps blanc fritté ou la pièce frittée, les exigences du procédé
d'usinage et des outils augmentant de l’ébauche au corps fritté, mais aucun rétrécissement supplémentaire
ne se produit plus sur le corps fritté. Lors de l'usinage de l’ébauche ou du corps blanc, il convient de prendre
en compte le rétrécissement ultérieur et de le compenser en conséquence.
© ISO/ASTM International 2026 – Tous droits réservés
Le frittage entraîne le compactage et la consolidation du corps formé par la formation de ponts de matière
entre les particules de poudre. Le rétrécissement se produit lorsque la porosité interne est remplie et
que le volume du corps diminue. Les valeurs typiques de rétrécissement dans une direction spatiale
(rétrécissement linéaire) se situent entre 10 % et 20 %. Le rétrécissement dépend des caractéristiques de la
matière première et des variables de contrôle du processus. Dans le cas d'un rétrécissement de volume, cela
se traduit par un rétrécissement d'environ 35 % à 65 %. Il convient que le rétrécissement soit pris en compte
dans la conception de l’ébauche au moyen d'une mise à l'échelle du volume.
En plus du frittage traditionnel, d'autres catégories de procédés peuvent être employées qui sont utilisées
pour augmenter la densification de la céramique après qu'elle a été soumise à un frittage initial. Par exemple,
utiliser une presse isostatique à chaud (Hot Isostatic Press – HIP), peut améliorer la performance et obtenir
un contrôle optimisé du grossissement de grain de la pièce finale, ce qui est généralement souhaité pour des
applications à haute fiabilité comme l'aérospatiale et le médical.
4.4 Recommandations générales de conception pour pièces en céramique
Les matériaux ductiles compensent les surcharges locales par une déformation élastique selon la loi de
Hooke et par le comportement de déformation plastique. Cela ne s'applique pas aux matériaux durs et
fragiles, car ils ne sont pas tolérants aux pannes et ainsi moins résilient sous la charge. Cela signifie qu'il
existe des différences significatives dans la capacité de charge des pièces composées de matériaux ductiles
et fragiles, tels que les métaux et les céramiques, respectivement. Cela exige des lignes directrices relatives
à la conception différentes.
Les matériaux céramiques présentent généralement une résistance élevée à la compression, mais une faible
résistance à la traction. Ce comportement contraste avec la capacité de charge des métaux et il convient
de considérer comme une distinction fondamentale lors de la conception des pièces. Le deuxième aspect
important est le procédé de frittage et le rétrécissement associé. En raison de l'absence totale de capacité de
déformation plastique, les céramiques présentent une défaillance spontanément après déformation élastique
et lorsque la résistance locale du matériau est atteinte. Les contraintes élevées se produisent surtout dans
les petits rayons, les arêtes vives, les marches, les épaulements, les alésages. Ce phénomène est d'autant plus
dramatique lorsque des points aigus ou des forces linéaires sont appliqués.
Par conséquent, lors de la conception d'une pièce en céramique, il est conseillé d'éviter les formes géométriques
qui agissent comme des encoches (concentrations de contraintes). Les matériaux céramiques se distinguent
notamment par leur grande résistance à la compression. Il convient donc que l'un des principaux objectifs
d'une conception adaptée aux céramiques soit d'utiliser de façon optimale cette propriété et de minimiser
le nombre de zones dans lesquelles la pièce est soumise à des contraintes de traction et/ou de flexion. Il
convient d'éviter les concentrations de contraintes dans les zones de traction.
Ces principes ne sont souvent pas suffisamment pris en compte. Il est fréquemment souhaité qu'une pièce
conçue à l'origine pour être fabriquée avec des matériaux métalliques soit ensuite fabriquée en un équivalent
céramique. Toutefois, cela peut non seulement augmenter les coûts de fabrication, mais aussi remettre en
question la faisabilité de la production dans certains cas. Il convient que la différence de propriétés des
matériaux dicte la manière dont la pièce est destinée à être utilisée dans l'application, et donc la manière
dont elle est conçue et traitée.
Les règles suivantes peuvent être résumées comme des recommandations générales relatives à la conception:
— éviter les contraintes de traction grâce à la conception géométrique;
— éviter les encoches, les arêtes et minimiser la rugosité de surface;
— éviter les accumulations de matériaux;
— tenir compte de la taille et du rétrécissement de l'espace de fabrication: en raison du rétrécissement,
les pièces frittées sont plus petites que le volume de fabrication disponible. Si nécessaire, deux pièces
peuvent être jointes pour former une pièce finale monolithique plus grande.
© ISO/ASTM International 2026 – Tous droits réservés
5 Liberté de conception et limites de la fabrication additive
5.1 Généralités
Les règles de conception des pièces en céramique que l'on peut trouver dans la littérature se réfèrent
généralement aux procédés de fabrication de céramique conventionnels. Ces règles prennent donc en
considération les particularités des procédés de moulage primaires courants, à savoir le pressage et le
moulage, ainsi que des limites de l'usinage. Ce faisant, les avantages de la FA restent inexploités. Le succès
des pièces de FA céramique dépend de manière décisive de l'utilisation cohérente des avantages de cette
technologie, tels que:
— l'orientation fonctionnelle (voir 5.2);
— l'intégration des fonctions (voir 5.3);
— la liberté d'utiliser des dégagements (voir 5.4);
D'autres facteurs de FA qui peuvent affecter la conception qu'il convient de considérer également sont:
— l'optimisation de la topologie (voir 5.5);
— l'orientation de la pièce et l'anisotropie (voir 5.6);
— les supports (voir 5.7);
— les finitions de surface (voir 5.8);
— la porosité (voir 5.9);
— l'interface de la plateforme de fabrication (voir 5.10).
5.2 Orientation fonctionnelle
Lors de la conception d'une pièce en céramique pour la FA, il convient que la fonction détermine la géométrie.
Par conséquent, il convient que la conception d'une pièce commence par les caractéristiques fonctionnelles.
Ils peuvent tous les deux être des éléments de connexion ou d'autres éléments de non connexion. Les
éléments de connexion peuvent être combinés librement dans la FA, dans le respect des spécifications liées
au procédé. Leur utilisation est essentielle pour apporter une valeur ajoutée à la fabrication conventionnelle.
La production de surfaces ajourées est possible sans effort supplémentaire.
5.3 Intégration des fonctions
La FA permet une grande liberté géométrique. Il convient qu’elle soit utilisée pour combiner des éléments
de conception et, par exemple, pour utiliser un support en même temps qu'une structure primaire pour le
transfert de chaleur. En outre, des treillis complexes pourraient être utilisés pour faire varier la densité de la
pièce dans tout son volume, ce qui permettrait non seulement de faire varier le support des caractéristiques
internes, mais aussi de contrôler le centre de masse de la pièce finale.
5.4 Liberté d'utiliser des dégagements
Avec la FA, le problème des supports des dégagements n'existe pratiquement plus. Les trous pénétrants et
les trous de perçage peuvent être réalisés indépendamment de l'accessibilité. Il suffit de s'assurer que la
matière première non fusionné et le matériau du support peuvent être retirés des trous. La production de
toutes les courbes est possible. Les structures d'échafaudage peuvent être conçues et finies à volonté dans
de larges limites.
© ISO/ASTM International 2026 – Tous droits réservés
5.5 Optimisation de la topologie
L'optimisation de la topologie est une méthode avec laquelle une forme de base pour pièces soumises à
charge mécanique peut être optimisée de manière à minimiser l'entrée de matériaux. La méthode consiste
essentiellement en les étapes suivantes:
a) détermination des dimensions extérieures de la pièce;
b) détermination de toutes les forces agissantes et des points fixes;
c) calcul des contraintes se produisant dans le «volume» sous l'effet de la force;
d) réduction du volume en fonction des contraintes subies;
e) calcul d'une proposition de conception optimale par logiciel.
Lorsqu'une optimisation de la topologie est réalisée sur la base d'une simulation par MEF, on obtient souvent
des motifs géométriques qui ne peuvent pas être réalisés au moyen d'une mise en forme conventionnelle,
ou seulement au prix d'un effort considérable. C'est pourquoi les procédés de FA, qui permettent une liberté
géométrique maximale sans outils ni moules, s'imposent. Les méthodes d'optimisation de la topologie ont
été développées et les solutions logicielles correspondantes sont disponibles.
Les implémentations ont été développées pour le domaine des plastiques et des métaux et ont prouvé leur
valeur, en particulier en ce qui concerne l'aspect de la conception allégée.
Pour la conception des pièces en céramique, il convient toutefois de prendre en compte non seulement les
contraintes survenant lors de l'application, mais aussi les forces agissant déjà pendant le frittage en raison
du rétrécissement. Par conséquent, il convient qu’une pièce en céramique optimisée sur le plan topologique
soit évaluée et, si nécessaire, révisée selon les lignes directrices relatives à la conception présentées ici
avant d'être produite. Des angles aigus internes et des trous borgnes peuvent conduire à une accumulation
de résine et sont difficiles à nettoyer, ainsi il convient de prêter attention à ces zones spécifiques lors de
l'optimisation de la topologie et pendant la conception en général. Une résine non durcie, de la poudre
résiduelle ou une pâte extrudée non uniformément piégée dans ces régions peut causer un comportement de
frittage anisotrope et compromettre la fidélité de la pièce.
5.6 Orientation et anisotropie des pièces
En FA, une couche est toujours consolidée, et cette couche est liée aux couches adjacentes, de sorte qu'il
existe une différence inhérente de résistance entre deux couches et à l'intérieur d'une couche.
En général, l’adhésion du matériau et donc la résistance sont plus élevées dans une couche qu'entre
les couches. En raison de la structure couche par couche en FA, il existe une anisotropie inhérente des
propriétés des matériaux dans l’ébauche. Cet effet dépend du procédé, du matériau et de la pièce et peut être
considérablement réduit par une commande de procédé adéquate. Dans certains cas, cependant, la pièce
frittée présente encore des anisotropies. Il convient donc que l'anisotropie soit prise en compte lors de la
conception de la pièce et de son orientation dans l'espace de fabrication.
5.7 Support
5.7.1 Généralités
Les pièces FA peuvent exiger des supports, en fonction du procédé et de la géométrie. Les supports sont
nécessaires pour les raisons suivantes:
— les porte-à-faux, les petits angles de la contre-dépouille;
— la surface de raccordement à la plateforme de fabrication est trop petite, par exemple dans le cas de
géométries de forme libre;
— la rigidité nécessaire de l’ébauche;
© ISO/ASTM International 2026 – Tous droits réservés
— les forces expérimentées au cours du procédé de FA.
Lors de la conception des supports, il convient de veiller à ce qu'aucune partie des supports ne soit reliée à
des surfaces fonctionnelles. La Figure 7 illustre deux exemples de situations où les supports sont justifiés. Le
diagramme de gauche démontre l'importance d'utiliser des supports lorsque l'angle de la contre-dépouille
est inférieur à 45°, une valeur de seuil commune, comme mesuré depuis l'horizontale. Le diagramme de
droite démontre un porte-à-faux perpendiculaire, qui est uniquement atteignable (sans porte-à-faux) pour
une longueur de porte-à-faux très courte. Par ailleurs, il convient que les supports soient conçus de façon à
minimiser l'effort nécessaire pour les retirer.
Légende
1 structure de support
2 a > seuil
Figure 7 — Zones de contre-dépouille (porte-à-faux) qui requièrent des supports
5.7.2 Matériau de support identique au matériau de la pièce
Comme les procédés de FA pour les pièces en céramiques produisent généralement d'abord des ébauches, il
est possible de retirer manuellement les supports dans cet état mou.
Dans certaines circonstances, des supports sur la pièce sont nécessaires afin d'éviter toute déformation
pendant le frittage. Dans ce cas, les supports sont généralement retirés après le frittage à l'aide d'un appareil
de meulage.
5.7.3 Matériau de support non identique au matériau de la pièce
Dans ce cas, il convient de retirer le support avant le frittage. Le matériau de support est choisi pour être
détaché de la pièce par voie chimique ou thermique. Cette méthode est généralement plus douce pour la
pièce que l'enlèvement mécanique du support.
Si le support ne nécessite pas d’être retiré mécaniquement, il existe d'autres degrés de liberté pour sa
conception et, par conséquent, pour la conception de la pièce. Ainsi, les supports avec des structures en
treillis dans les cavités peuvent également servir de raidisseurs.
Les structures en treillis pour les supports peuvent être
...