


ASTM D3931-08(2015)
(Test Method)Standard Test Method for Determining Strength of Gap-Filling Adhesive Bonds in Shear by Compression Loading
Standard Test Method for Determining Strength of Gap-Filling Adhesive Bonds in Shear by Compression Loading
SIGNIFICANCE AND USE
4.1 Structural design based on strength-of-materials principles requires knowledge of the mechanical properties of the structural components, including adhesives. By nature of their use, the most important property of adhesive is shear strength.
4.2 Shear strength measured by this test method is suitable for use in adhesive development, manufacturing quality control, and in materials performance specifications, as well as structural design.
SCOPE
1.1 This test method covers the determination of comparative shear properties of gap-filling adhesives in wood-to-wood joints at specified thicknesses of bondline in the dry condition, when tested on standard specimens under specified conditions of preparation, conditioning, and loading in compression. This test method is intended as an evaluation of gap-filling adhesives such as those used to bond plywood to lumber, lumber to lumber, and other similar materials in building constructions.
1.2 This test method also may be used to determine shear properties of gap-filling adhesives in species of wood and in thicknesses of bondline other than those specified for the comparative tests of shear properties within this test method. All procedures specified herein are applicable, excepting requirements for wood species and specific gravity, and thicknesses of bondlines.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical conversions to SI units that are provided for information only and are not considered standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory limitations prior to use.
General Information
Buy Standard
Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation: D3931 − 08 (Reapproved 2015)
Standard Test Method for
Determining Strength of Gap-Filling Adhesive Bonds in
Shear by Compression Loading
This standard is issued under the fixed designation D3931; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope D1151 Practice for Effect of Moisture and Temperature on
Adhesive Bonds
1.1 This test method covers the determination of compara-
E171 Practice for Conditioning and Testing Flexible Barrier
tive shear properties of gap-filling adhesives in wood-to-wood
Packaging
joints at specified thicknesses of bondline in the dry condition,
when tested on standard specimens under specified conditions
3. Terminology
of preparation, conditioning, and loading in compression. This
test method is intended as an evaluation of gap-filling adhe-
3.1 Definitions:
sives such as those used to bond plywood to lumber, lumber to
3.1.1 gap-filling adhesive, n—an adhesive capable of form-
lumber, and other similar materials in building constructions.
ing and maintaining a bond between surfaces that are not
1.2 This test method also may be used to determine shear close-fitting.
properties of gap-filling adhesives in species of wood and in
3.1.1.1 Discussion—Close-fitting is relative to a given ma-
thicknesses of bondline other than those specified for the
terial and industry; for example, standards in construction
comparative tests of shear properties within this test method.
differ from standards in electronics. Some adhesives will bond
All procedures specified herein are applicable, excepting re-
by bridging without completely filling the gap; others by filling
quirements for wood species and specific gravity, and thick-
the gap completely.
nesses of bondlines.
1.3 The values stated in inch-pound units are to be regarded 4. Significance and Use
as standard. The values given in parentheses are mathematical
4.1 Structural design based on strength-of-materials prin-
conversions to SI units that are provided for information only
ciples requires knowledge of the mechanical properties of the
and are not considered standard.
structural components, including adhesives. By nature of their
1.4 This standard does not purport to address all of the
use, the most important property of adhesive is shear strength.
safety concerns, if any, associated with its use. It is the
4.2 Shear strength measured by this test method is suitable
responsibility of the user of this standard to establish appro-
for use in adhesive development, manufacturing quality
priate safety and health practices and determine the applica-
control, and in materials performance specifications, as well as
bility of regulatory limitations prior to use.
structural design.
2. Referenced Documents
2 5. Apparatus
2.1 ASTM Standards:
D143 Test Methods for Small Clear Specimens of Timber
5.1 Testing Machine, having a capacity of about 15 000 lb
D905 Test Method for Strength Properties of Adhesive
(6818 kg) in compression or of sufficient capacity to test the
Bonds in Shear by Compression Loading
adhesive in use. The machine shall be fitted with a shearing
tool containing a self-aligning seat to ensure uniform lateral
distribution of the load. The machine shall be capable of
This test method is under the jurisdiction of ASTM Committee D14 on maintaining a uniform rate of loading such that the load may be
Adhesives and is the direct responsibility of Subcommittee D14.70 on Construction
applied with a continuous motion of the movable head to
Adhesives.
maximum load at a rate of 9.20 in. (5.0 mm)/min with a
Current edition approved April 1, 2015. Published April 2015. Originally
permissible variation of 625 %. The shearing tool shown in
approved in 1980. Last previous edition approved in 2008 as D3931 – 08. DOI:
10.1520/D3931-08R15.
Fig. 1 of Test Method D905 has been found satisfactory. Locate
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
the testing machine in an atmosphere such that the moisture
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM
content of the specimens, developed under the conditions
Standards volume information, refer to the standard’s Document Summary page on
the ASTM website. prescribed in 7.3, is not noticeably altered during testing.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
D3931 − 08 (2015)
6. Test Specimen and Sample samples in accordance with the final measurement section
under radial and tangential shrinkage and the weighing section
6.1 Test specimens for adhesive bonds shall conform to the
under moisture determination in Test Methods D143. Surface
form and dimensions shown in Fig. 1. Prepare bonded assem-
the blocks just prior to gluing, preferably with a hand-feed
blies as described in 7.1. Prepare test specimens for testing as
jointer. Make sure the surfaces remain unsanded and free from
described in 7.2.
dirt.
6.2 Determine mean shear strengths of bonds at bondline
7.1.2 Use spacer strips to control bondlines to specified
thicknesses of 0.006 and 0.060 in. (0.15 and 1.52 mm). Tests
thicknesses between blocks. Spacers shall be wood veneer or
for strengths of bonds at other thicknesses, in addition to those
1 1
plastic, and measure approximately ⁄2 by 3 ⁄2 in. (13 by 89
specified, shall be optional upon agreement between the
mm) long. Place spacers crosswise at the ends and center of the
manufacturer and the user.
lower test joint block. Apply adhesive in sufficient quantity to
6.3 Test a minimum of 28 specimens, representing seven ensure squeezeout at the ends of the joint when blocks are
different bonded assemblies, to determine mean shear strengths
under pressure (Note 2).
of bonds at each bondline thickness.
NOTE 2—If the adhesive is to be applied as an extruded bead, the bead
3 1
should be ⁄8 to ⁄2 in. (10 to 13 mm) in diameter to ensure squeezeout in
7. Procedure
bondline thicknesses near 0.060 in. (1.5 mm). Use a smaller diameter bead
7.1 Preparation of Bonded Assemblies: of adhesive for thinner bondlines.
7.1.1 Prepare bonded assemblies with hard maple blocks
7.1.2.1 Take care to avoid air entrapment in the bondline.
(Acer saccharum or Acer nigrum) conditioned as described in
Do not spread the adhesive closer than ⁄2 in. (13 mm) to any
7.3. The blocks shall have a minimum specific gravity of 0.65,
spacer because adhesive may be entrapped between block and
based on ovendry weight and ovendry volume (Note 1).
spacer, thereby increasing bondline thickness. Assemble the
blocks immediately, unless specified otherwise by agreement
NOTE 1—A method for selecting maple blocks of satisfactory specific
gravity is described in the Appendix of Test Method D905. For reference
between the manufacturer and user of the adhesive. Apply a
tests, the specific gravity of blocks may be determined in accordance with
15-lb (7.0-kg) load uniformly over the entire bond area to
the Weight and Moisture Content Section under Nail Withdrawal of Test
ensure firm contact between spacers and blocks of the assem-
Methods D143.
bly. Maintain the pressure on test joints at the conditions
7.1.1.1 These blocks shall be straight-grained and free of
prescribed in 7.1.
defects, including knots, splits, birdseye, short grain, decay,
7.1.3 Curing time for bonded assemblies shall be as speci-
and any unusual discoloration within the shearing area. The
fied by the manufacturer of the adhesive, or else 30 days in the
blocks shall be of suitable size so that four test specimens can
standard atmosphere (7.3.1).
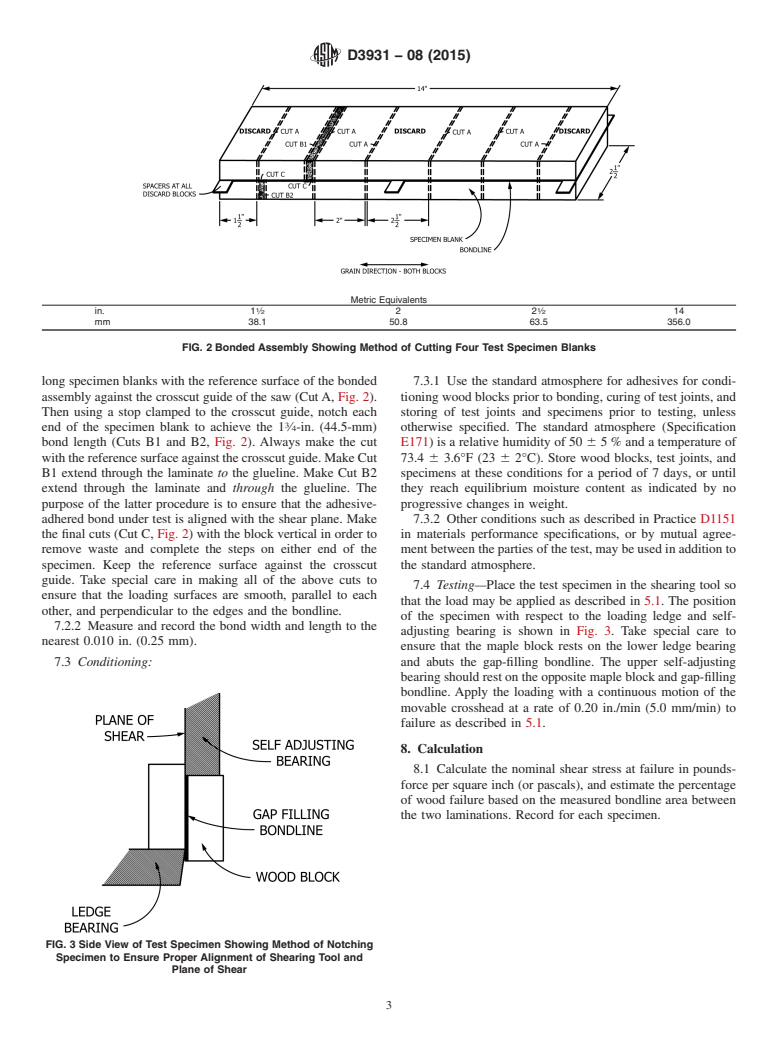
be cut from one test joint, as shown in Fig. 2. Blocks
3 1
7.2 Preparation of Test Specimens:
approximately ⁄4 by 2 ⁄2 by 14 in. (19 by 63 by 356 mm) have
been found to be satisfactory for this purpose. The moisture 7.2.1 Joint one edge of each bonded assembly to use as a
content shall be from 8 to 10 % (conditions prescribed in 7.3.1) reference surface in further cutting. Rip-saw the other edge to
based on ovendry weight as determined on representative reduce the width of the assembly to 2 in. (51 mm). Cut 2-in.
Metric Equivalents
1 3 3
in. 0.064 ⁄4 ⁄4 1 ⁄4 2
mm 1.63 6.35 19.05 44.45 50.80
FIG. 1 Form and Dimensions of Test Specimen
D3931 − 08 (2015)
Metric Equivalents
1 1
in. 1 ⁄2 2 2 ⁄2 14
mm 38.1 50.8 63.5 356.0
FIG. 2 Bonded Assembly Showing Method of Cutting Four Test Specimen Blanks
long specimen blanks with the reference surface of the bonded 7.3.1 Use the standard atmosphere for adhesives for condi-
assembly against the crosscut guide of the saw (Cut A, Fig. 2). tioning wood blocks prior to bonding, curing of test joints, and
Then using a stop clamped to the crosscut guide, notch each storing of test joints and specimens prior to testing, unless
end of the specimen blank to achieve the 1 ⁄4-in. (44.5-mm) otherwise specified. The standard atmosphere (Specification
bond length (Cuts B1 and B2, Fig. 2). Always make the cut E171) is a relative humidity of 50 6 5 % and a temperature of
with the reference surface against the crosscut guide. Make Cut 73.4 6 3.6°F (23 6 2°C). Store wood blocks, test joints, and
B1 extend through the laminate to the glueline. Make Cut B2 specimens at these c
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: D3931 − 08 D3931 − 08 (Reapproved 2015)
Standard Test Method for
Determining Strength of Gap-Filling Adhesive Bonds in
Shear by Compression Loading
This standard is issued under the fixed designation D3931; the number immediately following the designation indicates the year of
original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval. A
superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
1. Scope
1.1 This test method covers the determination of comparative shear properties of gap-filling adhesives in wood-to-wood joints
at specified thicknesses of bondline in the dry condition, when tested on standard specimens under specified conditions of
preparation, conditioning, and loading in compression. This test method is intended as an evaluation of gap-filling adhesives such
as those used to bond plywood to lumber, lumber to lumber, and other similar materials in building constructions.
1.2 This test method also may be used to determine shear properties of gap-filling adhesives in species of wood and in
thicknesses of bondline other than those specified for the comparative tests of shear properties within this test method. All
procedures specified herein are applicable, excepting requirements for wood species and specific gravity, and thicknesses of
bondlines.
1.3 The values stated in inch-pound units are to be regarded as standard. The values given in parentheses are mathematical
conversions to SI units that are provided for information only and are not considered standard.
1.4 This standard does not purport to address all of the safety concerns, if any, associated with its use. It is the responsibility
of the user of this standard to establish appropriate safety and health practices and determine the applicability of regulatory
limitations prior to use.
2. Referenced Documents
2.1 ASTM Standards:
D143 Test Methods for Small Clear Specimens of Timber
D905 Test Method for Strength Properties of Adhesive Bonds in Shear by Compression Loading
D1151 Practice for Effect of Moisture and Temperature on Adhesive Bonds
E171 Practice for Conditioning and Testing Flexible Barrier Packaging
3. Terminology
3.1 Definitions:
3.1.1 gap-filling adhesive, n—an adhesive capable of forming and maintaining a bond between surfaces that are not close-fitting.
This test method is under the jurisdiction of ASTM Committee D14 on Adhesives and is the direct responsibility of Subcommittee D14.70 on Construction Adhesives.
Current edition approved April 1, 2008April 1, 2015. Published May 2008April 2015. Originally approved in 1980. Last previous edition approved in 20052008 as
D3931 - 93a (2005).D3931 – 08. DOI: 10.1520/D3931-08.10.1520/D3931-08R15.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’sstandard’s Document Summary page on the ASTM website.
3.1.1.1 Discussion—
Close-fitting is relative to a given material and industry; for example, standards in construction differ from standards in electronics.
Some adhesives will bond by bridging without completely filling the gap; others by filling the gap completely.
4. Significance and Use
4.1 Structural design based on strength-of-materials principles requires knowledge of the mechanical properties of the structural
components, including adhesives. By nature of their use, the most important property of adhesive is shear strength.
4.2 Shear strength measured by this test method is suitable for use in adhesive development, manufacturing quality control, and
in materials performance specifications, as well as structural design.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
D3931 − 08 (2015)
5. Apparatus
5.1 Testing Machine, having a capacity of about 15 000 lb (6818 kg) in compression or of sufficient capacity to test the adhesive
in use. The machine shall be fitted with a shearing tool containing a self-aligning seat to ensure uniform lateral distribution of the
load. The machine shall be capable of maintaining a uniform rate of loading such that the load may be applied with a continuous
motion of the movable head to maximum load at a rate of 9.20 in. (5.0 mm)/min with a permissible variation of 625 %. The
shearing tool shown in Fig. 1 of Test Method D905 has been found satisfactory. Locate the testing machine in an atmosphere such
that the moisture content of the specimens, developed under the conditions prescribed in 7.3, is not noticeably altered during
testing.
6. Test Specimen and Sample
6.1 Test specimens for adhesive bonds shall conform to the form and dimensions shown in Fig. 1. Prepare bonded assemblies
as described in 7.1. Prepare test specimens for testing as described in 7.2.
6.2 Determine mean shear strengths of bonds at bondline thicknesses of 0.006 and 0.060 in. (0.15 and 1.52 mm). Tests for
strengths of bonds at other thicknesses, in addition to those specified, shall be optional upon agreement between the manufacturer
and the user.
6.3 Test a minimum of 28 specimens, representing seven different bonded assemblies, to determine mean shear strengths of
bonds at each bondline thickness.
7. Procedure
7.1 Preparation of Bonded Assemblies:
7.1.1 Prepare bonded assemblies with hard maple blocks (Acer saccharum or Acer nigrum) conditioned as described in 7.3. The
blocks shall have a minimum specific gravity of 0.65, based on ovendry weight and ovendry volume (Note 1).
NOTE 1—A method for selecting maple blocks of satisfactory specific gravity is described in the Appendix of Test Method D905. For reference tests,
the specific gravity of blocks may be determined in accordance with the Weight and Moisture Content Section under Nail Withdrawal of Test Methods
D143.
7.1.1.1 These blocks shall be straight-grained and free of defects, including knots, splits, birdseye, short grain, decay, and any
unusual discoloration within the shearing area. The blocks shall be of suitable size so that four test specimens can be cut from one
3 1
test joint, as shown in Fig. 2. Blocks approximately ⁄4 by 2 ⁄2 by 14 in. (19 by 63 by 356 mm) have been found to be satisfactory
for this purpose. The moisture content shall be from 8 to 10 % (conditions prescribed in 7.3.1) based on ovendry weight as
determined on representative samples in accordance with the final measurement section under radial and tangential shrinkage and
the weighing section under moisture determination in Test Methods D143. Surface the blocks just prior to gluing, preferably with
a hand-feed jointer. Make sure the surfaces remain unsanded and free from dirt.
Metric Equivalents
1 3 3
in. 0.064 ⁄4 ⁄4 1 ⁄4 2
mm 1.63 6.35 19.05 44.45 50.80
FIG. 1 Form and Dimensions of Test Specimen
D3931 − 08 (2015)
Metric Equivalents
1 1
in. 1 ⁄2 2 2 ⁄2 14
mm 38.1 50.8 63.5 356.0
FIG. 2 Bonded Assembly Showing Method of Cutting Four Test Specimen Blanks
7.1.2 Use spacer strips to control bondlines to specified thicknesses between blocks. Spacers shall be wood veneer or plastic,
1 1
and measure approximately ⁄2 by 3 ⁄2 in. (13 by 89 mm) long. Place spacers crosswise at the ends and center of the lower test joint
block. Apply adhesive in sufficient quantity to ensure squeezeout at the ends of the joint when blocks are under pressure (Note 2).
3 1
NOTE 2—If the adhesive is to be applied as an extruded bead, the bead should be ⁄8 to ⁄2 in. (10 to 13 mm) in diameter to ensure squeezeout in bondline
thicknesses near 0.060 in. (1.5 mm). Use a smaller diameter bead of adhesive for thinner bondlines.
7.1.2.1 Take care to avoid air entrapment in the bondline. Do not spread the adhesive closer than ⁄2 in. (13 mm) to any spacer
because adhesive may be entrapped between block and spacer, thereby increasing bondline thickness. Assemble the blocks
immediately, unless specified otherwise by agreement between the manufacturer and user of the adhesive. Apply a 15-lb (7.0-kg)
load uniformly over the entire bond area to ensure firm contact between spacers and blocks of the assembly. Maintain the pressure
on test joints at the conditions prescribed in 7.1.
7.1.3 Curing time for bonded assemblies shall be as specified by the manufacturer of the adhesive, or else 30 days in the
standard atmosphere (7.3.1).
7.2 Preparation of Test Specimens:
7.2.1 Joint one edge of each bonded assembly to use as a reference surface in further cutting. Rip-saw the other edge to reduce
the width of the assembly to 2 in. (51 mm). Cut 2-in. long specimen blanks with the reference surface of the bonded assembly
against the crosscut guide of the saw (Cut A, Fig. 2). Then using a stop clamped to the crosscut guide, notch each end of the
specimen blank to achieve the 1 ⁄4-in. (44.5-mm) bond length (Cuts B1 and B2, Fig. 2). Always make the cut with the reference
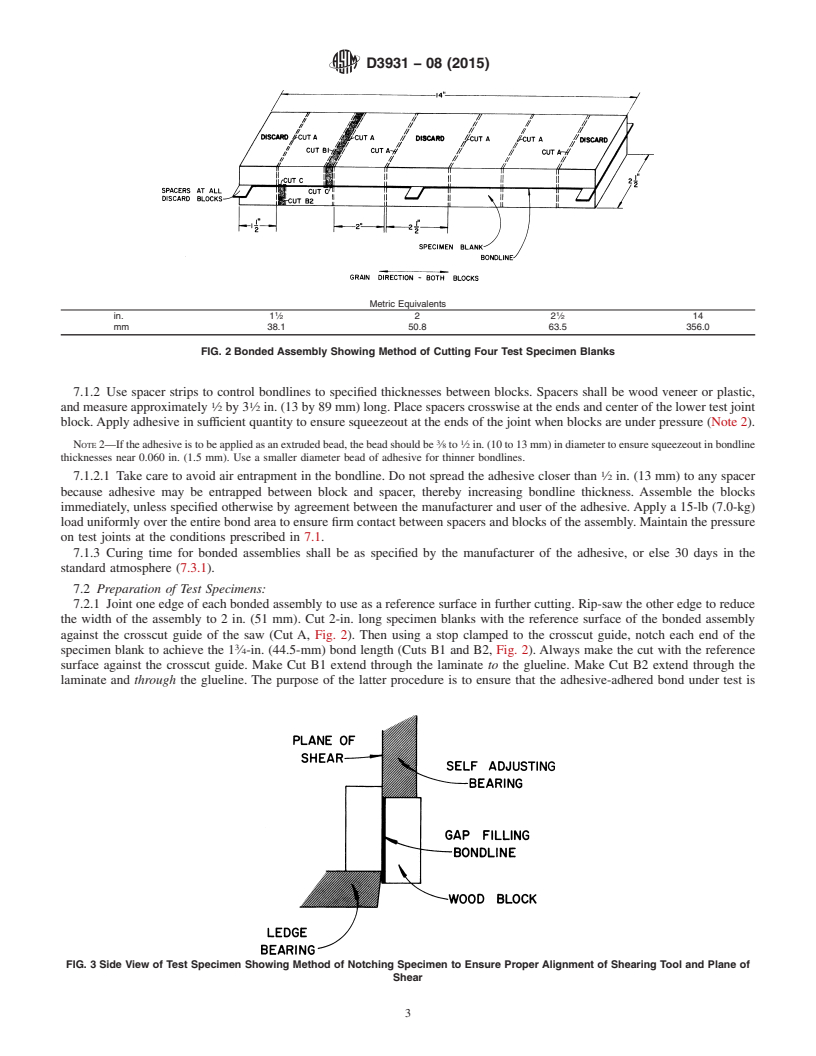
surface against the crosscut guide. Make Cut B1 extend through the laminate to the glueline. Make Cut B2 extend through the
laminate and through the glueline. The purpose of the latter procedure is to ensure that the adhesive-adhered bond under test is
FIG. 3 Side View of Test Specimen Showing Method of Notching Specimen to Ensure Proper Alignment of Shearing Tool and Plane of
Shear
D3931 − 08 (2015)
aligned with the shear plane. Make the final cuts (Cut C, Fig. 2) with the block vertical in order to remove waste and
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.