


ASTM A48/A48M-03(2021)
(Specification)Standard Specification for Gray Iron Castings
Standard Specification for Gray Iron Castings
ABSTRACT
This specification covers gray iron castings intended for general engineering use where tensile strength is a major consideration. Castings are classified on the basis of the tensile strength of the iron in separately cast test bars. The surface of the casting shall be free of adhering sand, scale, cracks, and hot tears, as determined by visual examination. The test bars are designated into S, A, B, and C categories, according to the thickness of its controlling wall section. The casting shall be subjected to a tension test to determine its tensile strength.
SCOPE
1.1 This specification covers gray iron castings intended for general engineering use where tensile strength is a major consideration. Castings are classified on the basis of the tensile strength of the iron in separately cast test bars.
1.1.1 This specification subordinates chemical composition to tensile strength.
1.2 Castings produced to this specification are graded on the basis of minimum tensile strength obtained in special test coupons designed to standardize cooling rate. The tensile strength developed in certain casting sections may vary from test coupon values (see X1.2).
1.3 The values stated in either SI units or inch-pound units are to be regarded separately as standard. The values stated in each system may not be exact equivalents; therefore, each system shall be used independently of the other. Combining values from the two systems may result in nonconformance with the standard.
1.4 This international standard was developed in accordance with internationally recognized principles on standardization established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
General Information
Buy Standard

Standards Content (Sample)
NOTICE: This standard has either been superseded and replaced by a new version or withdrawn.
Contact ASTM International (www.astm.org) for the latest information
Designation:A48/A48M −03 (Reapproved 2021)
Standard Specification for
Gray Iron Castings
This standard is issued under the fixed designation A48/A48M; the number immediately following the designation indicates the year
of original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval.
A superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
This specification replaces Federal Specification QQ-I-652.
1. Scope 2.2 Military Standard:
MIL-STD-129 Marking for Shipment and Storage
1.1 This specification covers gray iron castings intended for
2.3 Federal Standard:
general engineering use where tensile strength is a major
Federal Standard No. 123 Marking for Shipment (Civil
consideration. Castings are classified on the basis of the tensile
Agencies)
strength of the iron in separately cast test bars.
1.1.1 This specification subordinates chemical composition
3. Terminology
to tensile strength.
3.1 Definitions:
1.2 Castings produced to this specification are graded on the
3.1.1 Definitions for many terms common to gray iron
basis of minimum tensile strength obtained in special test
castings are found in Terminology A644.
coupons designed to standardize cooling rate. The tensile
strength developed in certain casting sections may vary from
4. Classification
test coupon values (see X1.2).
4.1 Castings ordered and produced in accordance with this
1.3 The values stated in either SI units or inch-pound units
specificationareclassifiedintoanumberofgradesbasedonthe
are to be regarded separately as standard. The values stated in
properties of separately cast test bars (Tables 1 and 2). Each
each system may not be exact equivalents; therefore, each
class is designated by a number followed by a letter. The
system shall be used independently of the other. Combining number indicates the minimum tensile strength of the sepa-
values from the two systems may result in nonconformance
rately cast test bar, and the letter indicates the size of the test
with the standard. bar. Examples of proper designations are as follows:
Gray Iron Castings, ASTM Specification A48, Class 30B.
1.4 This international standard was developed in accor-
Gray Iron Castings, ASTM Specification A48, Class 40C.
dance with internationally recognized principles on standard-
ization established in the Decision on Principles for the
5. Ordering Information
Development of International Standards, Guides and Recom-
5.1 Orders for material to this specification shall include the
mendations issued by the World Trade Organization Technical
following information:
Barriers to Trade (TBT) Committee.
5.1.1 ASTM designation number and year of issue,
5.1.2 Class of iron required (see 4.1 and Tables 1 and 2),
2. Referenced Documents
5.1.3 The size of the separately cast test bar (letter
2.1 ASTM Standards:
classification—A, B, C, or S) that best represents the thickness
A644 Terminology Relating to Iron Castings
of the controlling section of the casting (see Table 3),
E8/E8M Test Methods for Tension Testing of Metallic Ma-
5.1.4 The tension test specimen (B or C) to be machined
terials
from test bar C (see 13.3, Table 4, and Fig. 1),
5.1.5 The tension test specimen to be machined from test
bar S (see 13.4, Table 4, and Fig. 1),
This specification is under the jurisdiction of ASTM Committee A04 on Iron
5.1.6 Lot size (see Section 10),
CastingsandisthedirectresponsibilityofSubcommitteeA04.01onGreyandWhite
5.1.7 Special requirements (see Section 6),
Iron Castings.
5.1.8 Saving tested specimens or unbroken test bars (see
Current edition approved Sept. 1, 2021. Published September 2021. Originally
15.1), and
approved in 1905. Last previous edition approved in 2016 as A48/
A48M – 03 (2016). DOI: 10.1520/A0048_A0048M-03R21.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or
contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Available from Standardization Documents Order Desk, DODSSP, Bldg. 4,
Standards volume information, refer to the standard’s Document Summary page on Section D, 700 Robbins Ave., Philadelphia, PA 19111-5098, http://
the ASTM website. www.dodssp.daps.mil.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A48/A48M−03 (2021)
TABLE 1 Requirements for Tensile Strength of Gray Cast Irons in TABLE 2 Requirements for Tensile Strength of Gray Cast Irons in
Separately Cast Test Bars (Inch-Pound) Separately Cast Test Bars (Metric)
Tensile Strength, Nominal Test Bar Tensile Strength, Nominal Test Bar
Class Class
min, ksi Diameter, in. min, ksi [MPa] Diameter, in. [mm]
No. 20 A 20 0.8 No. 150A 150 20 to 22
No. 20 B 1.2 No. 150B 30
No. 20 C 2.0 No. 150C 50
A A
No. 20 S Bars S No. 150S Bars S
No. 25 A 25 0.88 No. 175A 175 20 to 22
No. 25 B 1.2 No. 175B 30
No. 25 C 2.0 No. 175C 50
A A
No. 25 S Bars S No. 175S Bars S
No. 30 A 30 0.88 No. 200A 200 20 to 22
No. 30 B 1.2 No. 200B 30
No. 30 C 2.0 No. 200C 50
A A
No. 30 S Bars S No. 200S Bars S
No. 35 A 35 0.88 No. 225A 225 20 to 22
No. 35 B 1.2 No. 225B 30
No. 35 C 2.0 No. 225C 50
A A
No. 35 S Bars S No. 225S Bars S
No. 40 A 40 0.88 No. 250A 250 20 to 22
No. 40 B 1.2 No. 250B 30
No. 40 C 2.0 No. 250C 50
A A
No. 40 S Bars S No. 250S Bars S
No. 45 A 45 0.88 No. 275A 275 20 to 22
No. 45 B 1.2 No. 275B 30
No. 45 C 2.0 No. 275C 50
A A
No. 45 S Bars S No. 275S Bars S
No. 50 A 50 0.88 No. 300A 300 20 to 22
No. 50 B 1.2 No. 300B 30
No. 50 C 2.0 No. 300C 50
A A
No. 50 S Bars S No. 300S Bars S
No. 55 A 55 0.88 No. 325A 325 20 to 22
No. 55 B 1.2 No. 325B 30
No. 55 C 2.0 No. 325C 50
A A
No. 55 S Bars S No. 325S Bars S
No. 60 A 60 0.88 No. 350A 350 20 to 22
No. 60 B 1.2 No. 350B 30
No. 60 C 2.0 No. 350C 50
A A
No. 60 S Bars S No. 350S Bars S
A
All dimensions of test bar S shall be as agreed upon between the manufacturer
No. 375A 375 20 to 22
and the purchaser.
No. 375B 30
No. 375C 50
A
No. 375S Bars S
5.1.9 Special preparation for delivery (see Section 19).
No. 400A 400 20 to 22
No. 400B 30
6. Special Requirements
No. 400C 50
A
6.1 When agreed upon in writing between the manufacturer
No. 400S Bars S
and the purchaser, it may be necessary for the castings to meet A
All dimensions of test bar S shall be as agreed upon between the manufacturer
and the purchaser.
special requirements as to hardness, chemical composition,
microstructure, pressure tightness, radiographic soundness,
dimensions, surface finish, and so forth.
9. Workmanship and Finish
7. Tensile Requirements
9.1 The surface of the casting shall be free of adhering sand,
7.1 Test bars representing castings conforming to this speci-
scale, cracks, and hot tears, as determined by visual examina-
fication shall meet the requirements for tensile strength as
tion.
described in Tables 1 and 2.
9.2 No repairing by plugging or welding of any kind shall
8. Dimensional Requirements
be permitted unless written permission is granted by the
purchaser.
8.1 The castings shall conform to the dimensions or draw-
ings furnished by the purchaser or, if there are no drawings, to
10. Sampling
the dimensions predicted by the pattern equipment supplied by
the purchaser. 10.1 A lot shall consist of one of the following:
A48/A48M−03 (2021)
TABLE 3 Separately Cast Test Bars for Use When a Specific
11.5 When castings are stress-relieved, annealed, or other-
Correlation Has Not Been Established Between the Test Bar and
wise heat-treated, test bars shall receive the same thermal
the Casting
treatment and shall be treated adjacent to the castings they
Thickness of the Wall of the Controlling
Test Bar represent.
Section of the Casting, in. [mm]
Under 0.25 [under 5] S
12. Number of Tests and Retests
0.25 to 0.50 [5 to 14] A
0.51 to 1.00 [15 to 25] B
12.1 The tension test shall be conducted in accordance with
1.01 to 2 [26 to 50] C
Over 2 [over 50] S
Test Methods E8/E8M.
12.2 One tension test shall be performed on each lot and
shall conform to the tensile requirements specified.
10.1.1 All the metal poured from a single heating in a
12.3 If the results of a valid test fail to conform to the
batch-type melting furnace.
requirements of this specification, two retests shall be made. If
10.1.2 All the metal from two or more batch-type melting
either retest fails to meet the specification requirements, the
furnaces poured into a single ladle or a single casting.
castings represented by these test specimens shall be rejected.
10.1.3 All the metal poured from a continuous melting
A valid test is one wherein the specimen has been properly
furnace for a given period of time between changes in charge,
prepared and appears to be sound and on which the approved
processing conditions, or aim-for chemistry or 4 h, whichever
test procedure has been followed.
is the shorter period.
12.4 Ifsufficientseparatelycasttestpiecesarenotavailable,
10.1.3.1 The purchaser may agree to extend the 4-h time
the manufacturer shall have the option of removing a test
period to8hifthe manufacturer can demonstrate sufficient
specimen from a location of representative casting, as agreed
process control to warrant such an extension.
upon between the manufacturer and purchaser.
11. Cast Test Bars
12.5 If the first test results indicate that a heat treatment is
11.1 Test bars shall be separate castings poured from the
needed to meet the test requirements, the entire lot of castings
same lot as the castings they represent and shall have dimen-
and the representative test specimens shall be heat treated
sions as shown in Table 4. Allowance may be made for
together. Testing shall proceed in accordance with 12.1 – 12.3.
reasonablepatterndraftwithinthetolerancesshowninTable4.
12.6 If, after testing, a test specimen shows evidence of a
Test bars A, B, and C are all standard test bars in the form of
defect, the results of the test may be invalidated and another
simple cylinders. Test bar S is special and is intended for use
made on a specimen from the same lot.
where the standard bars are not satisfactory.
11.2 The test bars shall be cast in dried, baked, or chemi-
13. Tension Test Specimens
cally bonded molds made mainly of an aggregate of siliceous
13.1 For test barA, the tension test specimenA, as shown in
sand with appropriate binders. The average grain size of the
Fig. 1, shall be machined concentric with the axis of the test
sand shall approximate that of the sand in which the castings
bar.
are poured. Molds for the test bars shall be approximately at
room temperature when poured. More than one test bar may be
13.2 For test
...
This document is not an ASTM standard and is intended only to provide the user of an ASTM standard an indication of what changes have been made to the previous version. Because
it may not be technically possible to adequately depict all changes accurately, ASTM recommends that users consult prior editions as appropriate. In all cases only the current version
of the standard as published by ASTM is to be considered the official document.
Designation: A48/A48M − 03 (Reapproved 2016) A48/A48M − 03 (Reapproved 2021)
Standard Specification for
Gray Iron Castings
This standard is issued under the fixed designation A48/A48M; the number immediately following the designation indicates the year
of original adoption or, in the case of revision, the year of last revision. A number in parentheses indicates the year of last reapproval.
A superscript epsilon (´) indicates an editorial change since the last revision or reapproval.
This standard has been approved for use by agencies of the U.S. Department of Defense.
This specification replaces Federal Specification QQ-I-652.
1. Scope
1.1 This specification covers gray iron castings intended for general engineering use where tensile strength is a major
consideration. Castings are classified on the basis of the tensile strength of the iron in separately cast test bars.
1.1.1 This specification subordinates chemical composition to tensile strength.
1.2 Castings produced to this specification are graded on the basis of minimum tensile strength obtained in special test coupons
designed to standardize cooling rate. The tensile strength developed in certain casting sections may vary from test coupon values
(see X1.2).
1.3 The values stated in either SI units or inch-pound units are to be regarded separately as standard. The values stated in each
system may not be exact equivalents; therefore, each system shall be used independently of the other. Combining values from the
two systems may result in non-conformancenonconformance with the standard.
1.4 This international standard was developed in accordance with internationally recognized principles on standardization
established in the Decision on Principles for the Development of International Standards, Guides and Recommendations issued
by the World Trade Organization Technical Barriers to Trade (TBT) Committee.
2. Referenced Documents
2.1 ASTM Standards:
A644 Terminology Relating to Iron Castings
E8E8/E8M Test Methods for Tension Testing of Metallic Materials [Metric] E0008_E0008M
2.2 Military Standard:
MIL-STD-129 Marking for Shipment and Storage
2.3 Federal Standard:
Federal Standard No. 123 Marking for Shipment (Civil Agencies)
3. Terminology
3.1 Definitions:
This specification is under the jurisdiction of ASTM Committee A04 on Iron Castings and is the direct responsibility of Subcommittee A04.01 on Grey and White Iron
Castings.
Current edition approved Nov. 1, 2016Sept. 1, 2021. Published November 2016September 2021. Originally approved in 1905. Last previous edition approved in 20122016
as A48/A48M – 03 (2012).(2016). DOI: 10.1520/A0048_A0048M-03R16.10.1520/A0048_A0048M-03R21.
For referenced ASTM standards, visit the ASTM website, www.astm.org, or contact ASTM Customer Service at service@astm.org. For Annual Book of ASTM Standards
volume information, refer to the standard’s Document Summary page on the ASTM website.
Available from Standardization Documents Order Desk, DODSSP, Bldg. 4, Section D, 700 Robbins Ave., Philadelphia, PA 19111-5098, http://www.dodssp.daps.mil.
Copyright © ASTM International, 100 Barr Harbor Drive, PO Box C700, West Conshohocken, PA 19428-2959. United States
A48/A48M − 03 (2021)
3.1.1 Definitions for many terms common to gray iron castings are found in Terminology A644.
4. Classification
4.1 Castings ordered and produced in accordance with this specification are classified into a number of grades based on the
properties of separately cast test bars (Tables 1 and 2). Each class is designated by a number followed by a letter. The number
indicates the minimum tensile strength of the separately cast test bar, and the letter indicates the size of the test bar. Examples of
proper designations are as follows:
Gray Iron Castings, ASTM Specification A48, Class 30B.
Gray Iron Castings, ASTM Specification A48, Class 40C.
5. Ordering Information
5.1 Orders for material to this specification shall include the following information:
5.1.1 ASTM designation number and year of issue,
TABLE 1 Requirements for Tensile Strength of Gray Cast Irons in
Separately Cast Test Bars (Inch-Pound)
Tensile Strength, Nominal Test Bar
Class
min, ksi Diameter, in.
No. 20 A 20 0.8
No. 20 B 1.2
No. 20 C 2.0
A
No. 20 S Bars S
No. 25 A 25 0.88
No. 25 B 1.2
No. 25 C 2.0
A
No. 25 S Bars S
No. 30 A 30 0.88
No. 30 B 1.2
No. 30 C 2.0
A
No. 30 S Bars S
No. 35 A 35 0.88
No. 35 B 1.2
No. 35 C 2.0
A
No. 35 S Bars S
No. 40 A 40 0.88
No. 40 B 1.2
No. 40 C 2.0
A
No. 40 S Bars S
No. 45 A 45 0.88
No. 45 B 1.2
No. 45 C 2.0
A
No. 45 S Bars S
No. 50 A 50 0.88
No. 50 B 1.2
No. 50 C 2.0
A
No. 50 S Bars S
No. 55 A 55 0.88
No. 55 B 1.2
No. 55 C 2.0
A
No. 55 S Bars S
No. 60 A 60 0.88
No. 60 B 1.2
No. 60 C 2.0
A
No. 60 S Bars S
A
All dimensions of test bar S shall be as agreed upon between the manufacturer
and the purchaser.
A48/A48M − 03 (2021)
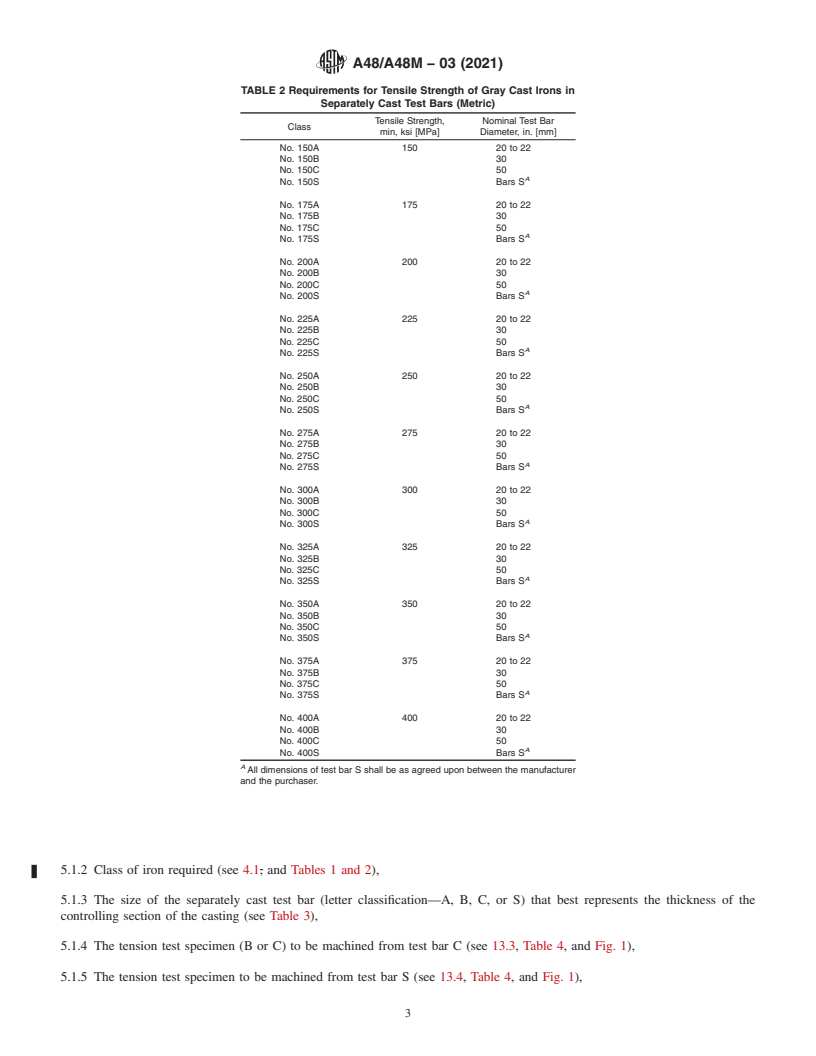
TABLE 2 Requirements for Tensile Strength of Gray Cast Irons in
Separately Cast Test Bars (Metric)
Tensile Strength, Nominal Test Bar
Class
min, ksi [MPa] Diameter, in. [mm]
No. 150A 150 20 to 22
No. 150B 30
No. 150C 50
A
No. 150S Bars S
No. 175A 175 20 to 22
No. 175B 30
No. 175C 50
A
No. 175S Bars S
No. 200A 200 20 to 22
No. 200B 30
No. 200C 50
A
No. 200S Bars S
No. 225A 225 20 to 22
No. 225B 30
No. 225C 50
A
No. 225S Bars S
No. 250A 250 20 to 22
No. 250B 30
No. 250C 50
A
No. 250S Bars S
No. 275A 275 20 to 22
No. 275B 30
No. 275C 50
A
No. 275S Bars S
No. 300A 300 20 to 22
No. 300B 30
No. 300C 50
A
No. 300S Bars S
No. 325A 325 20 to 22
No. 325B 30
No. 325C 50
A
No. 325S Bars S
No. 350A 350 20 to 22
No. 350B 30
No. 350C 50
A
No. 350S Bars S
No. 375A 375 20 to 22
No. 375B 30
No. 375C 50
A
No. 375S Bars S
No. 400A 400 20 to 22
No. 400B 30
No. 400C 50
A
No. 400S Bars S
A
All dimensions of test bar S shall be as agreed upon between the manufacturer
and the purchaser.
5.1.2 Class of iron required (see 4.1, and Tables 1 and 2),
5.1.3 The size of the separately cast test bar (letter classification—A, B, C, or S) that best represents the thickness of the
controlling section of the casting (see Table 3),
5.1.4 The tension test specimen (B or C) to be machined from test bar C (see 13.3, Table 4, and Fig. 1),
5.1.5 The tension test specimen to be machined from test bar S (see 13.4, Table 4, and Fig. 1),
A48/A48M − 03 (2021)
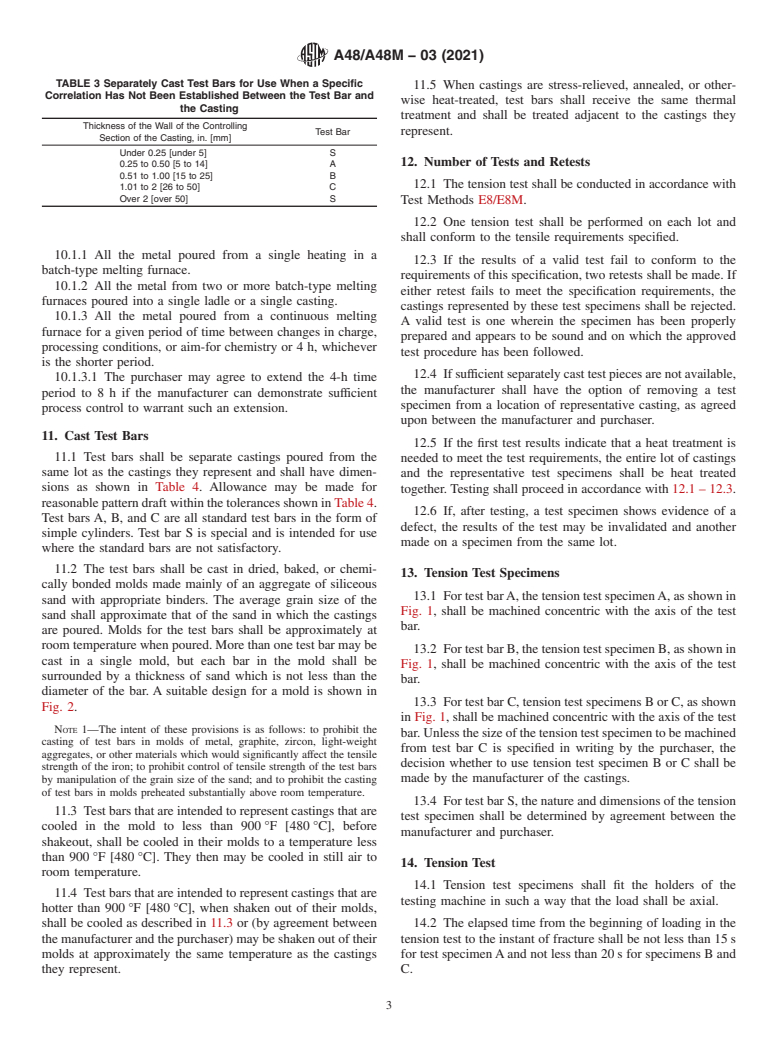
TABLE 3 Separately Cast Test Bars for Use When a Specific
Correlation Has Not Been Established Between the Test Bar and
the Casting
Thickness of the Wall of the Controlling
Test Bar
Section of the Casting, in. [mm]
Under 0.25 [under 5] S
0.25 to 0.50 [5 to 14] A
0.51 to 1.00 [15 to 25] B
1.01 to 2 [26 to 50] C
Over 2 [over 50] S
5.1.6 Lot size (see Section 10),
5.1.7 Special requirements (see Section 6),
5.1.8 Saving tested specimens or unbroken test bars (see 15.1), and
5.1.9 Special preparation for delivery (see Section 19).
6. Special Requirements
6.1 When agreed upon in writing between the manufacturer and the purchaser, it may be necessary for the castings to meet special
requirements as to hardness, chemical composition, microstructure, pressure tightness, radiographic soundness, dimensions,
surface finish, and so forth.
7. Tensile Requirements
7.1 Test bars representing castings conforming to this specification shall meet the requirements for tensile strength as described
in Tables 1 and 2.
8. Dimensional Requirements
8.1 The castings shall conform to the dimensions or drawings furnished by the purchaser,purchaser or, if there are no drawings,
to the dimensions predicted by the pattern equipment supplied by the purchaser.
9. Workmanship and Finish
9.1 The surface of the casting shall be free of adhering sand, scale, cracks, and hot tears, as determined by visual examination.
9.2 No repairing by plugging or welding of any kind shall be permitted unless written permission is granted by the purchaser.
10. Sampling
10.1 A lot shall consist of one of the following:
10.1.1 All the metal poured from a single heating in a batch type batch-type melting furnace.
10.1.2 All the metal from two or more batch type batch-type melting furnaces poured into a single ladle or a single casting.
10.1.3 All the metal poured from a continuous melting furnace for a given period of time between changes in charge, processing
conditions, or aim-for chemistry or 4 h, whichever is the shorter period.
10.1.3.1 The purchaser may agree to extend the 4-h time period to 8 h if the manufacturer can demonstrate sufficient process
control to warrant such an extension.
11. Cast Test Bars
11.1 Test bars shall be separate castings poured from the same lot as the castings they represent and shall have dimensions as
A48/A48M − 03 (2021)
TABLE 4 Diameters and Lengths of Cast Test Bars
As-Cast Diameter, in. [mm] Length, in. [mm]
Test Bar
Nominal Minimum Maximum
Minimum (Bottom) Maximum (Top)
(Mid-Length) (Specified) (Recommended)
A 0.88 [22.4] 0.85 [21.6] 0.96 [24.4] 5.0 [125] 6.0 [150]
B 1.20 [30.5] 1.14 [29.0] 1.32 [33.5] 6.0 [150] 9.0 [230]
C 2.00 [50.8] 1.90 [48.3] 2.10 [53.3] 7.0 [175] 10.0 [255]
A
S . . . . . . . . . . . . . . .
A
All dimensions of test bar S shall be as agreed upon by the manufacturer and the purchaser.
Tension Test Tension Test Tension Test
Dimensions, in. [mm]
Specimen A Specimen B Specimen C
G—Length of parallel, min 0.50 [13] 0.75 [19] 1.25 [32]
D—Diameter 0.500 ± 0.010 0.750 ± 0.015 1.25 ± 0.025
[13 ± 0.25] [20 ± 0.4] [30 ± 0.6]
R—Radius of fillet, min 1 [25] 1 [25] 2 [50]
1 1 1
A—Length of reduced section, min 1 ⁄4 [32] 1 ⁄2 [38] 2 ⁄4 [57]
3 3
L—Over-all length, min 3 ⁄4 [95] 4 [100] 6 ⁄8 [160]
7 1 7
C—Diameter of end section, approx ⁄8 [20] 1 ⁄4 [20] 1 ⁄8 [47]
1 1 5
E—Length of shoulder, min ⁄4 [6] ⁄4 [6] ⁄16 [8]
5 1 15 1 7 1
F—Diameter of shoulder ⁄8 ± ⁄64 ⁄16 ± ⁄64 1 ⁄16 ± ⁄64
[16 ± 0.4] [24 ± 0.4] [36 ± 0.4]
A A A
B—Length of end section
A
Optional to fit holders on testing machine. If threaded, root diameter shall not be less than dimension F.
FIG. 1 Tension-TestTension Test Specimens
shown in Table 4. Allowance may be made for reasonable pattern draft within the tolerances shown in Table 4. Test bars A, B, and
C are all standard test bars in the form of simple cylinders. Test bar S is special and is intended for use where the standard bars
are not satisfactory.
11.2 The test bars shall be cast in dried, baked, or chemically bonded molds made mainly of an aggregate of siliceous sand with
appropriate binders. The average grain size of the sand shall approximate that of the sand in which the castings are poured. Molds
for the test bars shall be approximately at room temperature when poured. More than one test bar may be cast in a single mold,
but each bar in the mold shall be surrounded by a thickness of sand which is not less than the diameter of the bar. A suitable design
for a mold is shown in Fig. 2.
NOTE 1—The intent of these provisions is as follows: to prohibit the casting of test bars in molds of metal, graphite, zircon, light-weight aggregates, or
other materials which would significantly affect the tensile strength of the iron; to prohibit control of tensile strength of the test bars by manipulation of
the grain size of the sand; and to prohibit the casting of test bars in molds preheated substantially above room temperature.
11.3 Test bars that are intended to represent castings that are cooled in the mold to less than 900°F [480°C],900 °F [480 °C], before
shakeout, shall be cooled in their molds to a temperature less than 900°F [480°C].900 °F [480 °C]. They then may be cooled in
still air to room temperature.
A48/A48M − 03 (2021)
Required Features: Optional Features:
1. Material—Aggregate of dry siliceous sand. 1. Number of test bars in a single mold—Two suggested.
2. Position—Bars vertical. 2. Design of pouring cup.
3. L—See Table 4. 3. P—2 in. [50 mm], suggested.
4. D—See Table 4. 4. N— ⁄16 in. [8 mm] in diameter, suggested.
5. W—Not less than diameter D. f5. M = 1.5 N, suggested.
FIG. 2 Suitable Design and Dimensions for Mold for Separately Cast Cylindrical Test Bars for Gray Iron
11.4 Test bars that are intended to represent castings that are hotter than 900°F [480°C],900 °F [480 °C], when shaken out of their
molds, shall be cooled as described in 11.3 or (by agreement between the manufacturer and the purchaser) may be shaken out of
their molds at approximately the same temperature as the castings they represent.
11.5 When castings are stress-relieved, annealed, or otherwise heat-treated, test bars shall receive the same thermal treatment and
shall be treated adjacent to the castings they represent.
12. Number of Tests and Retests
12.1 The tension test shall be conducted in accordance with Test MethodMethods E8E8/E8M.
12.2 One tension test shall be performed on each lot and shall conform to the tensile requirements specified.
12.3 If the results of a valid test fail to conform to the requirements of this specification, two retests shall be made. If either retest
fails to meet the specification requirements, the castings represented by these test specimens shall be rejected. A valid test is one
wherein the specimen has been properly prepared and appears to be sound and on which the approved test procedure has been
followed.
12.4 If sufficient separately cast test pieces are not available, the manufacturer shall have the option of removing a test specimen
from a location of representative casting, as agreed upon between the manufacturer and purchaser.
12.5 If the first test results indicate that a heat treatment is needed to meet the test requirements, the entire lot of castings and the
representative test specimens shall be heat treated together. Testing shall proceed in accordance with 12.1 – 12.3.
12.6 If, after testing, a test specimen shows evidence of a defect, the results of the test may be invalidated and another made on
a specimen from the same lot.
13. Tension Test Specimens
13.1 For test Barbar A, the tension-test tension test specimen A, as shown in Fig. 1, shall be machined concentric with the axis
of the test bar.
A48/A48M − 03 (2021)
13.2 For test Barbar B, the tension test specimen B, as shown in Fig. 1, shall be machined concentric with the axis of the test bar.
13.3 For test Barbar C, tension test specimens B or C, as shown in Fig. 1, shall be ma
...
Questions, Comments and Discussion
Ask us and Technical Secretary will try to provide an answer. You can facilitate discussion about the standard in here.