

EN 6104:2026
(Main)Aerospace series - Rivets, solid, in aluminium or aluminium alloy - Inch series - Technical specification
- Abstract
This document specifies the characteristics and quality assurance requirements for solid rivets and slugs made in aluminium or aluminium alloys, inch series, for aerospace application. This document is applicable to the following aluminium alloys: 1050A-H14, 2017A-T42, 2117-T42, 5056A-H32 and 7050-T73.
- Status
- Published
- Publication Date
- 28-Jul-2026
- Technical Committee
- ASD-STAN - Aerospace
- Drafting Committee
- ASD-STAN/D 3/S 2 - Fasteners
- Current Stage
- 6060 - Definitive text made available (DAV) - Publishing
- Start Date
- 29-Jul-2026
- Completion Date
- 29-Jul-2026
EN 6104:2026 is a CEN European Standard for aerospace solid rivets and slugs made from aluminium or aluminium alloy in the inch series. It specifies the product characteristics and quality assurance requirements for aerospace application, for the alloys 1050A-H14, 2017A-T42, 2117-T42, 5056A-H32 and 7050-T73.
What does EN 6104:2026 specify?
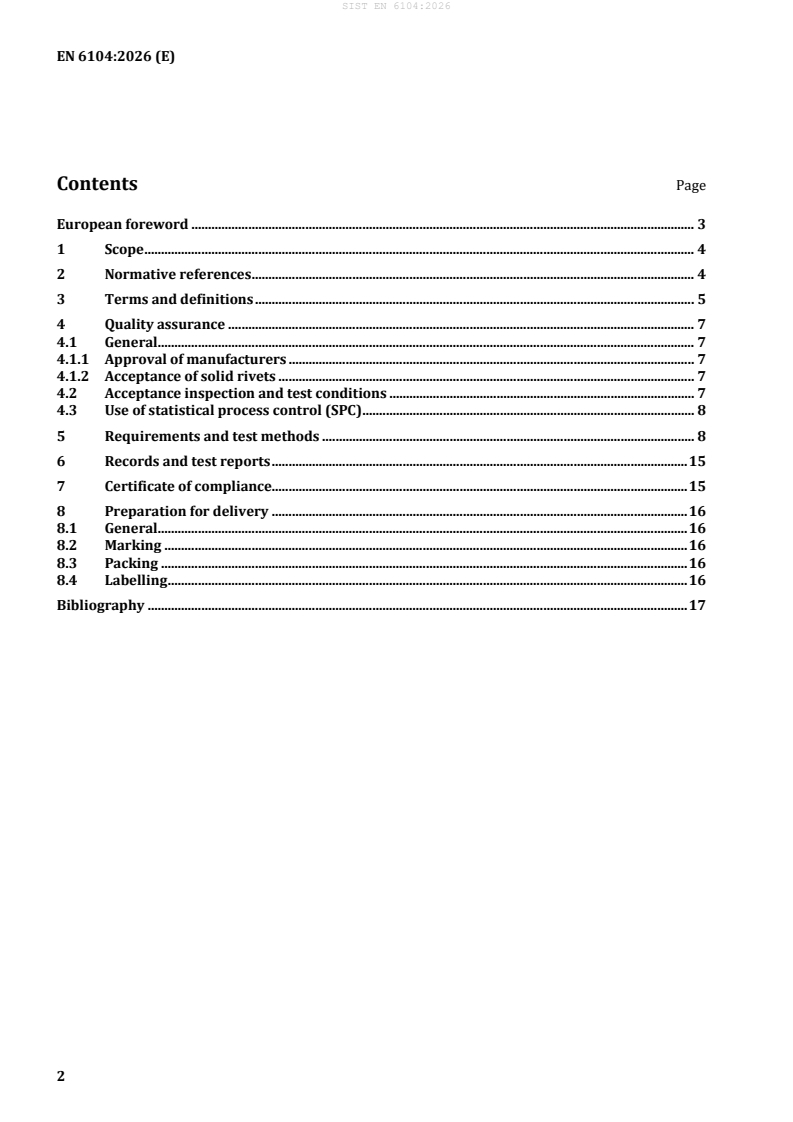
EN 6104:2026 specifies the characteristics and quality assurance requirements for solid rivets and slugs in aluminium or aluminium alloy for aerospace use. It is organized into clauses 1 to 8, followed by a bibliography, so a user can move from scope and definitions to testing, records, certification and delivery conditions.
| Clause | What it covers |
|---|---|
| 1 | Scope |
| 2 | Normative references |
| 3 | Terms and definitions |
| 4 | Quality assurance |
| 5 | Requirements and test methods |
| 6 | Records and test reports |
| 7 | Certificate of compliance |
| 8 | Preparation for delivery |
The document is focused on the inch series and on the named alloy conditions. That matters in practice because purchase, qualification and inspection have to match the alloy and product form covered by the standard.
What are the key requirements of EN 6104:2026?
Quality assurance and batch acceptance
EN 6104:2026 requires manufacturers to be approved production organizations for aerospace products and to operate a quality management system such as EN 9100 or an equivalent aerospace accepted system. In practice, the manufacturer is responsible for continuous conformance, not just for one-off inspection.
Acceptance inspections and tests are done on each batch, with random sampling from the batch. The standard also allows repeated testing after a correctable cause is removed, but the reason and action have to be recorded.
The document also allows statistical process control (SPC) as an alternative basis for demonstrating conformity, if the manufacturer can justify it with process analysis, control charts and audit planning. That matters when a producer wants to use stable process data instead of full final sampling.
Product characteristics and test methods
EN 6104:2026 links each key characteristic to a test method in Table 1. Material has to match the applicable material standard, dimensions are checked with suitable measuring equipment, and head protrusion is measured by NAS 9800 with a projection method used in disputes.
Heat treatment has to follow SAE AMS2770, with checks for intergranular corrosion, hydrogen porosity, eutectic melting and, for 7050-T73, electrical conductivity and tensile strength. For the user, this means the heat-treatment route and metallurgical condition are part of acceptance, not just the finished shape.
Workmanship requirements in clause 5.3.2 reject cracks, blistering, material separation, embedded chips, double rings and certain cold shuts, while allowing limited surface discontinuities within the table limits. That is important for aerospace assembly because surface damage can affect installation and service performance.
Mechanical and metallurgical performance
EN 6104:2026 specifies shear strength requirements and says shear testing is performed in accordance with ASTM B565. It also defines a driveability test, using a squeezing setup and visual examination of the upset tail after forming.
Clause 5.5 requires grain size control using ASTM E112, except for the alloys where no grain size requirement applies. In practice, this gives buyers and inspectors a way to check that the material condition is suitable for aerospace rivet performance.
Records, certification and delivery
EN 6104:2026 requires a test report for each batch in accordance with EN 10204:2004, 3.1. It also requires a certificate of compliance with each shipment, including the key test results and sample sizes, plus grain size when applicable and surface treatment, and for 7050-T73 the EC and tensile results when applicable.
Delivery preparation covers cleanliness, packing, and labelling. Packaging has to follow ASTM D3951, protect against damage and corrosion, and carry batch identification, quantity and recipient information.
What terms does EN 6104:2026 define?
- Batch - a quantity of finished rivets made by the same process, from one alloy heat, with the same size code and heat-treated together.
- Rivet wire sample - a length of wire taken from each end of the coil used to make the batch, and heat-treated with it.
- Rivet sample - a rivet taken at random from the batch for inspection or testing.
- Crack - a rupture in the material that can run in any direction and may be intercrystalline or transcrystalline.
- Defect - a failure to meet a requirement related to the intended use of the product.
- Major defect - a defect likely to cause failure or materially reduce usability.
- Minor defect - a defect unlikely to materially reduce usability.
- Sampling plan - the plan used to select one or more samples from a batch for acceptance testing.
Who uses EN 6104:2026?
EN 6104:2026 is used by aerospace rivet manufacturers, their quality teams, procurement staff, and customer inspectors. It is also relevant to qualification bodies and certification authorities because the document ties approval, batch acceptance and documentation together.
For a buyer, the standard helps define what to ask for in a specification, test report and certificate of compliance. For a manufacturer, it sets the inspection method, sample basis and packaging rules that have to be built into production and release.
Which standards are used with EN 6104:2026?
EN 6104:2026 uses several external standards for testing, sampling and documentation:
- EN 2002-001 - tensile testing at ambient temperature.
- EN 10204:2004 - types of inspection documents.
- ISO 2859-1 - attribute sampling plans and AQL-based inspection.
- ISO 7870-1 / ISO 7870-2 / ISO 7870-3 - control chart guidance for SPC.
- ASTM B193 - resistivity / electrical conductivity measurement.
- ASTM B565 - shear testing of aluminium rivets and wire.
- ASTM D3951 - commercial packaging practice.
- ASTM E112 - average grain size measurement.
- ASTM G110 - intergranular corrosion resistance test.
- NAS 9800 - head protrusion gaging.
- SAE AMS2770 - heat treatment of wrought aluminium alloy parts.
The bibliography also points to related wire standards for the alloys covered by the document: EN 2114, EN 2115, EN 2116, EN 2117 and EN 3115. EN 9100, ISO 3534-2 and ANSI/ASQ Z1.4 are also named as related references for quality systems, statistics and sampling.
What does the EN 6104:2026 document contain?
EN 6104:2026 contains a requirements table that ties each characteristic to a test method, acceptance basis and sampling approach. It also contains defect classification tables and sampling plans for major and minor visual and dimensional characteristics.
The document includes figures for the driveability test sample, the steel test jig and the target squeeze condition. Those figures matter because they tell the laboratory or production inspector how to set up the test, not just what result is acceptable.
It also contains clauses on batch records, batch test reports, certificates of compliance, marking, packing and labelling. In practice, those sections support traceability, incoming inspection and shipment release.
Get Certified
Connect with accredited certification bodies for this standard

BUREAU VERITAS Certification Germany
Bureau Veritas certification in Germany.
Element Materials Technology
Materials testing and product certification.

AQMS Ltd.
AQMS provides ISO certification to SMEs across the UK.
Sponsored listings
Frequently Asked Questions
EN 6104:2026 is a standard published by the European Committee for Standardization (CEN). Its full title is "Aerospace series - Rivets, solid, in aluminium or aluminium alloy - Inch series - Technical specification". This standard covers: This document specifies the characteristics and quality assurance requirements for solid rivets and slugs made in aluminium or aluminium alloys, inch series, for aerospace application. This document is applicable to the following aluminium alloys: 1050A-H14, 2017A-T42, 2117-T42, 5056A-H32 and 7050-T73.
This document specifies the characteristics and quality assurance requirements for solid rivets and slugs made in aluminium or aluminium alloys, inch series, for aerospace application. This document is applicable to the following aluminium alloys: 1050A-H14, 2017A-T42, 2117-T42, 5056A-H32 and 7050-T73.
EN 6104:2026 is classified under the following ICS (International Classification for Standards) categories: 49.030.60 - Rivets. The ICS classification helps identify the subject area and facilitates finding related standards.
EN 6104:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
01-oktober-2026
Aeronavtika - Trde kovice iz aluminija ali aluminijeve zlitine - Palčna serija -
Tehnična specifikacija
Aerospace series - Rivets, solid, in aluminium or aluminium alloy - Inch series -
Technical specification
Luft- und Raumfahrt - Vollniete aus Aluminium oder Aluminiumlegierung - Zoll-Reihe -
Technische Lieferbedingung
Série aérospatiale - Rivets ordinaires en aluminium ou en alliage d´aluminium - Série en
inches - Spécification technique
Ta slovenski standard je istoveten z: EN 6104:2026
ICS:
49.025.20 Aluminij Aluminium
49.030.60 Kovice Rivets
77.150.10 Aluminijski izdelki Aluminium products
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
EN 6104
EUROPEAN STANDARD
NORME EUROPÉENNE
July 2026
EUROPÄISCHE NORM
ICS 49.030.60
English Version
Aerospace series - Rivets, solid, in aluminium or
aluminium alloy - Inch series - Technical specification
Série aérospatiale - Rivets pleins en aluminium ou en Luft- und Raumfahrt - Vollniete aus Aluminium oder
aluminium ou en alliage d'aluminium - Série en inches - Aluminiumlegierung - Zoll-Reihe - Technische
Spécification technique Lieferbedingungen
This European Standard was approved by CEN on 15 June 2026.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this
European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references
concerning such national standards may be obtained on application to the CEN-CENELEC Management Centre or to any CEN
member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by
translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC Management
Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2026 CEN All rights of exploitation in any form and by any means reserved Ref. No. EN 6104:2026 E
worldwide for CEN national Members.
Contents Page
European foreword . 3
1 Scope . 4
2 Normative references . 4
3 Terms and definitions . 5
4 Quality assurance . 7
4.1 General. 7
4.1.1 Approval of manufacturers . 7
4.1.2 Acceptance of solid rivets . 7
4.2 Acceptance inspection and test conditions . 7
4.3 Use of statistical process control (SPC) . 8
5 Requirements and test methods . 8
6 Records and test reports . 15
7 Certificate of compliance. 15
8 Preparation for delivery . 16
8.1 General. 16
8.2 Marking . 16
8.3 Packing . 16
8.4 Labelling . 16
Bibliography . 17
European foreword
This document (EN 6104:2026) has been prepared by ASD-STAN.
After enquiries and votes carried out in accordance with the rules of this Association, this document has
received the approval of the National Associations and the Official Services of the member countries of
ASD-STAN, prior to its presentation to CEN.
This European Standard shall be given the status of a national standard, either by publication of an
identical text or by endorsement, at the latest by January 2027, and conflicting national standards shall
be withdrawn at the latest by January 2027.
Attention is drawn to the possibility that some of the elements of this document may be the subject of
patent rights. CEN shall not be held responsible for identifying any or all such patent rights.
Any feedback and questions on this document should be directed to the users’ national standards body.
A complete listing of these bodies can be found on the CEN website.
According to the CEN-CENELEC Internal Regulations, the national standards organizations of the
following countries are bound to implement this European Standard: Austria, Belgium, Bulgaria, Croatia,
Cyprus, Czech Republic, Denmark, Estonia, Finland, France, Germany, Greece, Hungary, Iceland, Ireland,
Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Republic of North
Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and the United
Kingdom.
1 Scope
This document specifies the characteristics and quality assurance requirements for solid rivets and slugs
made in aluminium or aluminium alloys, inch series, for aerospace application. This document is
applicable to the following aluminium alloys: 1050A-H14, 2017A-T42, 2117-T42, 5056A-H32 and
7050-T73.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 2002-001, Aerospace series — Metallic materials — Test methods — Part 001: Tensile testing at
ambient temperature
EN 10204:2004, Metallic products — Types of inspection documents
ISO 2859-1, Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by
acceptance quality limit (AQL) for lot-by-lot inspection
ISO 7870-1, Control charts — Part 1: General guidelines
ISO 7870-2, Control charts — Part 2: Shewhart control charts
ISO 7870-3, Control charts — Part 3: Acceptance control charts
ASTM B193, Standard test method for resistivity of electrical conductor materials
ASTM B565, Standard test method for shear testing of aluminium and aluminium-alloy rivets and
cold-heading wire and rods
ASTM D3951, Standard practice for commercial packaging
ASTM E112, Standard test methods for determining average grain size
ASTM G110, Standard practice for evaluating intergranular corrosion resistance of heat treatable
aluminium alloys by immersion in sodium chloride and hydrogen peroxide solution
NAS 9800, Head protrusion gaging, 100 ° flush head fasteners, gage block, gage diameters and stylus
SAE AMS2770, Heat treatment of wrought aluminium alloy parts
Published by: American Society for Testing and Materials (ASTM international), available at:
https://www.astm.org/.
Published by Aerospace Industries Association (AIA), available at: https://www.aia-aerospace.org/.
Published by: Society of Automotive Engineers (SAE), available at: https://www.sae.org/.
3 Terms and definitions
For the purposes of this document, the following terms and definitions apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp
— IEC Electropedia: available at https://www.electropedia.org/
3.1
batch
quantity of finished rivets, manufactured using the same process, from a single material cast (single heat
of alloy), having the same standard number, diameter and length code, heat treated together to the same
specified condition and produced as one continuous run
3.2
rivet wire sample
length of wire, sampled at each end of the coil used for the manufacture of rivets of the batch
Note 1 to entry: The rivet wire samples undergo the same heat treatments as the rivets of the batch, at the same
time.
3.3
rivet sample
rivet sampled at random from the batch
3.4
crack
rupture in the material, which can extend in any direction and which can be intercrystalline or
transcrystalline in character
3.5
seam
longitudinal open surface defect
3.6
lap
surface defect caused by folding over metal fins or sharp corners and then forming them into the surface
3.7
cold shut
doubling over of metal, which can occur during the cold heading operation
3.8
double ring
discontinuity, which is wide but shallow and open to the surface at both ends of the discontinuity
3.9
pit
small cavity in a metal surface caused by non-uniform electro deposition or by corrosion
3.10
inclusion
non-metallic particles originating from the aluminium alloy making process
Note 1 to entry: They can exist as discrete particles or strings of particles extending in a longitudinal direction.
3.11
material separation
any loss of material from preformed head induced by installation of the rivet
3.12
defect
non-fulfilment of a requirement related to an intended or specified use
3.13
major defect
defect that is likely to result in a failure or to reduce materially the usability of the considered product for
its intended purpose
3.14
minor defect
defect that is not likely to reduce materially the usability of the considered product for its intended
purpose, or that represents a departure from established specification having little bearing on the
effective use or operation of this product
3.15
hydrogen porosity
high temperature oxidation
Note 1 to entry: Racks and fixtures used should be constructed to preclude entrapment of water.
Note 2 to entry: Ammonium fluoroborate or equivalent can be used in air furnace as necessary.
3.16
blistering
defect in the metal on or near the surface, resulting from expansion of gas or entrapped lubricant from
forging process in a sub-surface zone
3.17
eutectic melting
mixture of different phases with eutectic composition, which melts below the solidus temperature of the
alloy
Note 1 to entry: Eutectic melting is characterized by small rosettes in the microstructure or by outlined grain
boundaries, particularly at triple intersections. It can occur when raw material is not homogenized or worked
properly
3.18
intergranular corrosion
selective corrosion attack along grain boundaries or closely adjacent regions without appreciable attack
of the grains
3.19
sampling plan
plan according to which one or more samples are taken from a batch in order to do acceptance tests to
demonstrate conformity of the batch
4 Quality assurance
4.1 General
4.1.1 Approval of manufacturers
The manufacturer’s operations shall be an approved production organization for aerospace products and
shall demonstrate that it has implemented and is able to maintain a quality management system (e.g. in
accordance with EN 9100 or an equivalent aerospace accepted and established quality management
system). The purpose of these procedures is to ensure that a manufacturer has a quality management
system in place and is capable of continuous production of solid rivets complying with the specified
quality requirements.
The Certification Authorities, or their appointed representative, who may be the prime contractor, shall
grant the approval of the manufacturer.
4.1.2 Acceptance of solid rivets
The purpose of acceptance inspections and tests of a solid rivet is to check, as simply as possible, using a
method which is inexpensive but the most representative of the actual conditions of use, with the
uncertainty inherent in statistical sampling, that the solid rivets satisfy the requirements of this
document.
Acceptance inspections and tests shall be carried out by the manufacturer, or under his responsibility.
The manufacturer is responsible for the quality of the solid rivets manufactured to this specification and
adherence to this specification.
4.2 Acceptance inspection and test conditions
Acceptance inspections and tests (requirements, methods, numbers of solid rivets) are specified in
Table 1. They shall be carried out on each batch. Solid rivets shall be selected from the batch to be tested
by random sampling.
Each solid rivet may be submitted to several inspections or tests, provided that none of its characteristics
has been altered during any of these inspections or tests.
The solid rivets to be subjected to destructive inspections or tests may be those on which non-destructive
inspections o
...