

ISO 17779:2026
(Main)Brazing — Specification and qualification of brazing procedures for metallic materials
- Abstract
This document specifies requirements for the specification and qualification of brazing procedures for brazing of metallic materials. This document specifies requirements for brazing of the test piece, testing of the test specimen, essential variables and their range of qualification, acceptance criteria, brazing procedure qualification record (BPQR) and brazing procedure specification (BPS). This document does not cover testing of residual stresses, corrosion resistance and impact properties. This document applies to the following brazing processes according to ISO 4063:2023 with local and global heating: 911 Infrared brazing; 912 Flame brazing, torch brazing; 913 Laser beam brazing; 914 Electron beam brazing; 916 Induction brazing; 918 Resistance brazing; 919 Diffusion brazing; 921 Furnace brazing; 922 Vacuum brazing; 923 Dip-bath brazing; 924 Salt-bath brazing; 925 Flux bath brazing; 926 Immersion brazing; 972 Arc weld brazing. This document does not apply to brazing for aerospace applications covered by ISO 11745.
- Status
- Published
- Publication Date
- 19-Oct-2026
- Technical Committee
- ISO/TC 44/SC 11 - Qualification requirements for welding and allied processes personnel
- Drafting Committee
- ISO/TC 44/SC 11/WG 3 - Brazing qualification
- Current Stage
- 6060 - International Standard published
- Start Date
- 20-Oct-2026
- Completion Date
- 20-Oct-2026
ISO 17779:2026, published by ISO, specifies how to prepare and qualify brazing procedures for metallic materials. It covers the brazing test piece, testing of the test specimen, essential variables, acceptance criteria, the brazing procedure qualification record (BPQR) and the brazing procedure specification (BPS). Engineers, quality managers, buyers and examiners use it to qualify a brazing method and to turn that qualification into a controlled production instruction.
What does ISO 17779:2026 specify?
ISO 17779:2026 specifies the requirements for procedure specification and procedure qualification for brazing of metallic materials. The document is aimed at production brazing where the process, test piece, inspection and records must be defined and repeatable.
The scope applies to brazing processes with local and global heating, including infrared brazing, flame or torch brazing, laser beam brazing, electron beam brazing, induction brazing, resistance brazing, diffusion brazing, furnace brazing, vacuum brazing, dip-bath brazing, salt-bath brazing, flux bath brazing, immersion brazing and arc weld brazing. It excludes testing of residual stresses, corrosion resistance and impact properties, and it excludes aerospace brazing covered by ISO 11745.
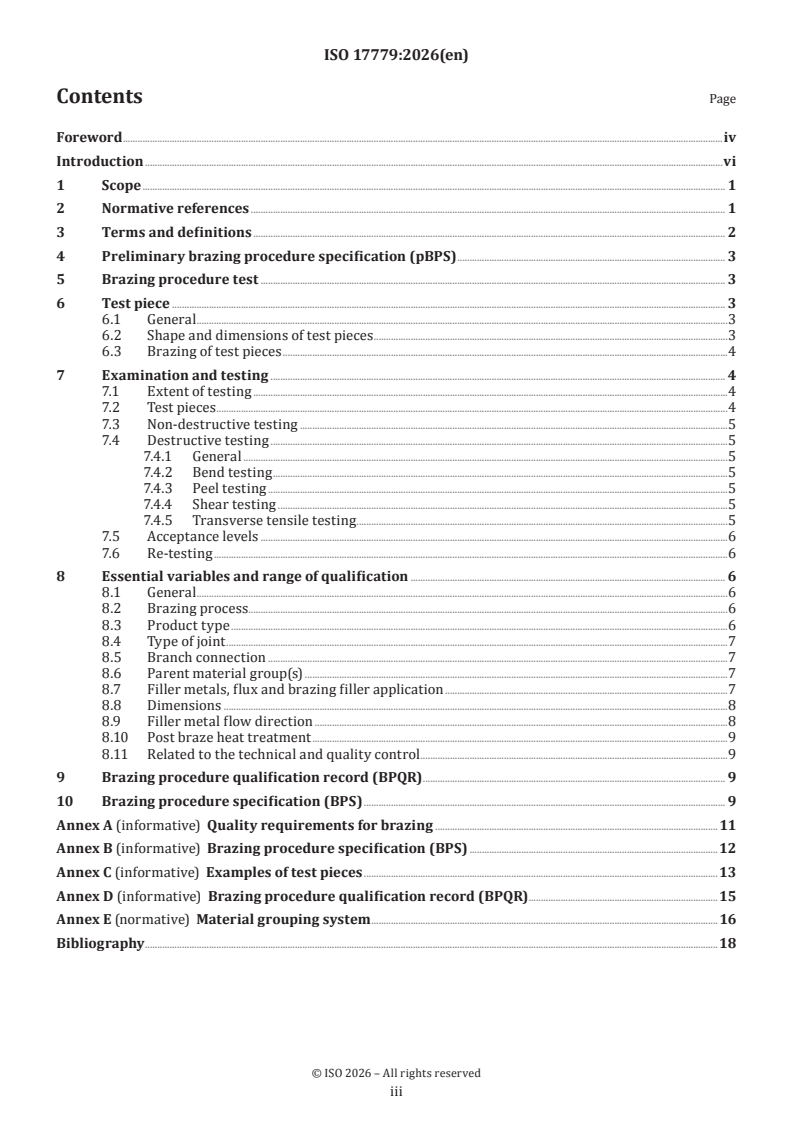
The document is organized into Clauses 1 to 10, followed by informative Annexes A to D, a normative Annex E, and informative Annex ZA.
| Annex | What it covers |
|---|---|
| A | Quality requirements for brazing |
| B | Example BPS form |
| C | Examples of test pieces |
| D | Example BPQR format |
| E | Material grouping system |
| ZA | Relationship to EU Directive 2014/68/EU |
What are the key requirements of ISO 17779:2026?
ISO 17779:2026 builds qualification around a preliminary brazing procedure specification (pBPS), a brazing procedure test, and then a qualified BPS supported by a BPQR. In practice, the document first defines the planned procedure, then proves it on test pieces, and finally turns the proven conditions into a controlled work instruction.
Procedure planning and qualification
Clause 4 requires a pBPS before qualification starts. Clause 5 then ties the brazing and testing of test pieces to Clauses 6 and 7, and says a brazer or brazing operator who completes the procedure test satisfactorily is considered qualified for the appropriate range in ISO 13585, provided the relevant testing requirements are met. That matters because qualification is not just a lab result - it links the tested method to the person doing the brazing.
Test pieces and witnessing
Clause 6 requires the test piece to use a joint design proposed in the pBPS and representative of intended production. If no application standard gives the shape and dimensions, the contracting parties agree them; the document gives typical lap, butt and sleeve-type examples in Annex C. Brazing and testing of the test pieces must be witnessed by an examiner or an examining body, which is important where third-party verification is needed.
Examination, testing and acceptance
Clause 7 sets the minimum examination and test programme. Visual testing is required, non-destructive testing is carried out before the test specimens are cut, and destructive testing is selected according to joint type - for example bend, peel, shear or tensile testing. Acceptance is based on ISO 18279:2023, with quality level B applying in general, quality level C applying to excess braze metal, and no imperfection passing through the joint length. If results fail, Clause 7.6 allows limited retesting under defined conditions.
Essential variables and range of qualification
Clause 8 is the heart of the document. A new qualification test covers only one brazing process, and changes outside the qualified range require requalification. The clause controls the process itself, product type, joint type, branch connection, parent material group, filler metal and flux, dimensions, filler metal flow direction, and post-braze heat treatment.
For example, filler metals are classified to ISO 17672, fluxes to ISO 18496, and the document distinguishes between filler metal forms and filler metal application. Thickness and joint overlap are qualification variables, and flow direction is also controlled. Clause 8.6 uses the Annex E material grouping system so that one test can qualify related parent materials within the same M-number grouping. Clause 8.10 makes post-braze heat-treatment changes a requalification trigger.
Records and production instructions
Clause 9 requires the BPQR to record the test results, including any retests, and to include the BPS items plus any rejectable features under Clause 7. A qualified BPQR is signed and dated by the examiner or examining body. Clause 10 requires the BPS to give the information needed to make the joint in production, including manufacturer identification, parent material and filler metal data, joint design, process details, cleaning, heating conditions, and degree of mechanisation. The tolerances in the BPS may be narrower than the full qualification range, which matters because production instructions often need tighter control than the qualification envelope.
What terms does ISO 17779:2026 define?
- Brazing - a joining process that uses filler metal with a liquidus temperature above 450 °C.
- Brazing procedure specification (BPS) - a qualified document that states the variables needed to repeat production brazing.
- Preliminary brazing procedure specification (pBPS) - the initial document that states the required variables before qualification is complete.
- Brazing procedure qualification record (BPQR) - the record of the qualification test results and related data.
- Manufacturer - the workshop, site, or both, operating under the same technical and quality management.
- Examiner - the person appointed to verify conformance with the applicable standard.
- Examining body - the organization appointed to verify conformance with the applicable standard.
- Test piece - the brazed assembly used for testing purposes.
Who uses ISO 17779:2026?
ISO 17779:2026 is used by manufacturers, workshops and sites that braze metallic materials and need a documented procedure qualification. It is also used by brazing engineers, quality managers and examiners who prepare the pBPS, witness testing, assess acceptance, and issue the BPQR and BPS.
It is relevant in industries that use brazed metallic components where procedure control matters, including pressure equipment applications covered by Annex ZA. Buyers and contracting parties use it to define what testing, documentation and witnessing are required before production starts.
What changed in ISO 17779:2026 from the previous edition?
ISO 17779:2026 is the second edition and it cancels and replaces ISO 17779:2021. The changes stated in the document are:
- requirements clarified throughout
- the introduction revised to match ISO/DIS 15614-1 wording
- the Annex A reference moved from the scope to 7.5
- the ISO 857-2 reference removed from the scope
- the scope revised by removing the statement that the principles could be applied to other brazing processes and materials not listed
- normative references in Clause 2 updated
- 3.4 revised to avoid a circular definition
- use of technically equivalent standards removed in 7.2, 7.3 and 7.4.2 to 7.4.5
- Table 4 footnotes revised for clarity
- use of equivalent standards removed in 8.7
- ISO 11745 added to the bibliography
Which standards are used with ISO 17779:2026?
ISO 17779:2026 refers to several standards that supply process identification, test methods, terminology, consumables and operator qualification:
- ISO 4063:2023 - gives the brazing process reference numbers used in the scope and qualification rules.
- ISO 18279:2023 - gives the imperfection assessment basis used for acceptance.
- EN 12797 - provides destructive test methods for brazed joints.
- EN 12799 - provides non-destructive examination methods for brazed joints.
- ISO 857-2 - provides brazing vocabulary and the definition of brazing.
- ISO/TR 25901-1 - provides general welding and allied-process terms used in the definitions.
- ISO 13585 - links procedure qualification to qualification testing of brazers and brazing operators.
- ISO 17672 - classifies brazing filler metals.
- ISO 18496 - classifies brazing fluxes.
- ISO 11745 - is the aerospace brazing qualification document named in the scope as outside this document’s application.
What does the ISO 17779:2026 document contain?
ISO 17779:2026 contains the qualification workflow, the minimum examination and testing scheme, and the rules for defining the qualified range of a brazing procedure. Clause 7 includes the test matrix for lap, butt and T-joints, and it points to visual, radiographic, metallographic, bend, peel, shear and tensile testing as applicable.
The annexes add practical material that supports use in design, testing and audits. Annex B gives a sample BPS format, Annex D gives a sample BPQR format, and Annex C shows example test pieces such as lap joints, butt joints, simple lap or socket joints, multiple joints and T-joints. Annex E sets out the material grouping system used to reduce the number of qualification tests, and Annex A lists the quality topics that should be agreed before contract. Annex ZA links the standard to the essential requirements of EU Directive 2014/68/EU for pressure equipment.
Relations
- Effective Date
- 12-Feb-2026
- Effective Date
- 08-Nov-2025
- Effective Date
- 07-Jun-2025
Get Certified
Connect with accredited certification bodies for this standard

DVS-ZERT GmbH
German welding certification society.
CARES (UK Certification Authority for Reinforcing Steels)
UK certification for reinforcing steels and construction.
EWF/IIW (European/International Welding Federation)
International welding personnel certification.
Sponsored listings
Frequently Asked Questions
ISO 17779:2026 is a standard published by the International Organization for Standardization (ISO). Its full title is "Brazing — Specification and qualification of brazing procedures for metallic materials". This standard covers: This document specifies requirements for the specification and qualification of brazing procedures for brazing of metallic materials. This document specifies requirements for brazing of the test piece, testing of the test specimen, essential variables and their range of qualification, acceptance criteria, brazing procedure qualification record (BPQR) and brazing procedure specification (BPS). This document does not cover testing of residual stresses, corrosion resistance and impact properties. This document applies to the following brazing processes according to ISO 4063:2023 with local and global heating: 911 Infrared brazing; 912 Flame brazing, torch brazing; 913 Laser beam brazing; 914 Electron beam brazing; 916 Induction brazing; 918 Resistance brazing; 919 Diffusion brazing; 921 Furnace brazing; 922 Vacuum brazing; 923 Dip-bath brazing; 924 Salt-bath brazing; 925 Flux bath brazing; 926 Immersion brazing; 972 Arc weld brazing. This document does not apply to brazing for aerospace applications covered by ISO 11745.
This document specifies requirements for the specification and qualification of brazing procedures for brazing of metallic materials. This document specifies requirements for brazing of the test piece, testing of the test specimen, essential variables and their range of qualification, acceptance criteria, brazing procedure qualification record (BPQR) and brazing procedure specification (BPS). This document does not cover testing of residual stresses, corrosion resistance and impact properties. This document applies to the following brazing processes according to ISO 4063:2023 with local and global heating: 911 Infrared brazing; 912 Flame brazing, torch brazing; 913 Laser beam brazing; 914 Electron beam brazing; 916 Induction brazing; 918 Resistance brazing; 919 Diffusion brazing; 921 Furnace brazing; 922 Vacuum brazing; 923 Dip-bath brazing; 924 Salt-bath brazing; 925 Flux bath brazing; 926 Immersion brazing; 972 Arc weld brazing. This document does not apply to brazing for aerospace applications covered by ISO 11745.
ISO 17779:2026 is classified under the following ICS (International Classification for Standards) categories: 25.160.01 - Welding, brazing and soldering in general. The ICS classification helps identify the subject area and facilitates finding related standards.
ISO 17779:2026 has the following relationships with other standards: It is inter standard links to prEN ISO 17779, ISO 21219-7:2024, ISO 17779:2021. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
ISO 17779:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
International
Standard
ISO 17779
Second edition
Brazing — Specification and
2026-10
qualification of brazing procedures
for metallic materials
Brasage fort — Descriptif et qualification d'un mode opératoire
de brasage fort pour les matériaux métalliques
Reference number
© ISO 2026
All rights reserved.
This ISO publication is protected by copyright and is owned by ISO and/or its licensors.
The content of this ISO publication is provided under licence, not sold. Use is subject to the applicable licence terms issued by ISO,
an ISO member body, or an authorized third-party distributor.
Except as required for implementation or expressly permitted by a separate licence, no part of this ISO publication may be
reproduced, distributed, modified, used, or made available in any form or by any means – electronic or mechanical, including
photocopying, scanning, recording, or posting on internal or external digital platforms.
Any use beyond the scope of the granted rights is prohibited and may result in legal action.
ISO copyright office
CP 401 • CH-1214 Vernier, Geneva
Phone: +41 22 749 01 11
Email: copyright@iso.org
Website: www.iso.org
Published in Switzerland
ii
Contents Page
Foreword .iv
Introduction .vi
1 Scope . 1
2 Normative references . 1
3 Terms and definitions . 2
4 Preliminary brazing procedure specification (pBPS) . 3
5 Brazing procedure test . 3
6 Test piece . 3
6.1 General .3
6.2 Shape and dimensions of test pieces .3
6.3 Brazing of test pieces .4
7 Examination and testing . 4
7.1 Extent of testing .4
7.2 Test pieces . .4
7.3 Non-destructive testing .5
7.4 Destructive testing .5
7.4.1 General .5
7.4.2 Bend testing .5
7.4.3 Peel testing .5
7.4.4 Shear testing .5
7.4.5 Transverse tensile testing .5
7.5 Acceptance levels .6
7.6 Re-testing .6
8 Essential variables and range of qualification . 6
8.1 General .6
8.2 Brazing process.6
8.3 Product type .6
8.4 Type of joint .7
8.5 Branch connection .7
8.6 Parent material group(s) .7
8.7 Filler metals, flux and brazing filler application .7
8.8 Dimensions .8
8.9 Filler metal flow direction .8
8.10 Post braze heat treatment .9
8.11 Related to the technical and quality control .9
9 Brazing procedure qualification record (BPQR) . 9
10 Brazing procedure specification (BPS) . 9
Annex A (informative) Quality requirements for brazing .11
Annex B (informative) Brazing procedure specification (BPS) .12
Annex C (informative) Examples of test pieces .13
Annex D (informative) Brazing procedure qualification record (BPQR) .15
Annex E (normative) Material grouping system .16
Bibliography .18
iii
Foreword
ISO (the International Organization for Standardization) is a worldwide federation of national standards
bodies (ISO member bodies). The work of preparing International Standards is normally carried out through
ISO technical committees. Each member body interested in a subject for which a technical committee
has been established has the right to be represented on that committee. International organizations,
governmental and non-governmental, in liaison with ISO, also take part in the work. ISO collaborates closely
with the International Electrotechnical Commission (IEC) on all matters of electrotechnical standardization.
The procedures used to develop this document and those intended for its further maintenance are described
in the ISO/IEC Directives, Part 1. In particular, the different approval criteria needed for the different types
of ISO document should be noted. This document was drafted in accordance with the editorial rules of the
ISO/IEC Directives, Part 2 (see www.iso.org/directives).
ISO draws attention to the possibility that the implementation of this document may involve the use of (a)
patent(s). ISO takes no position concerning the evidence, validity or applicability of any claimed patent
rights in respect thereof. As of the date of publication of this document, ISO had not received notice of (a)
patent(s) which may be required to implement this document. However, implementers are cautioned that
this may not represent the latest information, which may be obtained from the patent database available at
www.iso.org/patents. ISO shall not be held responsible for identifying any or all such patent rights.
Any trade name used in this document is information given for the convenience of users and does not
constitute an endorsement.
For an explanation of the voluntary nature of standards, the meaning of ISO specific terms and expressions
related to conformity assessment, as well as information about ISO's adherence to the World Trade
Organization (WTO) principles in the Technical Barriers to Trade (TBT), see www.iso.org/iso/foreword.html.
This document was prepared by Technical Committee ISO/TC 44, Welding and allied processes, Subcommittee
SC 11, Qualification requirements for welding and allied processes personnel, in collaboration with the European
Committee for Standardization (CEN) Technical Committee CEN/TC 121, Welding and allied processes, in
accordance with the Agreement on technical cooperation between ISO and CEN (Vienna Agreement).
This second edition cancels and replaces the first edition (ISO 17779:2021), which has been technically
revised.
The main changes are as follows:
— in general, all requirements have been clarified by use of suitable revisions;
— introduction has been revised to match text used in ISO/DIS 15614-1;
— reference to Annex A has been moved from the scope to 7.5;
— reference to ISO 857-2 has been deleted from the scope;
— scope revised by removing the statement: “The principles of this document can be applied to other
brazing processes and brazing of materials not listed";
— normative references in Clause 2 have been updated;
— in 7.2, 7.3, 7.4.2, 7.4.3, 7.4.4 and 7.4.5, the use of technically equivalent standards is no longer permitted
— in Table 4, the footnotes have been revised for clarity;
— in 8.7, the use of other standards that provide equivalent technical conditions is no longer permitted;
— ISO 11745 has been added to a new bibliography.
Any feedback or questions on this document should be directed to the user’s
national standards body. A complete listing of these bodies can be found at
iv
www.iso.org/members.html. Official interpretations of ISO/TC 44 documents, where they exist, are
available from this page: https://committee.iso.org/sites/tc44/home/interpretation.html.
v
Introduction
The purpose of this document is to provide a general set of rules for brazing procedure qualification
independent of product or application.
All new brazing procedure qualification tests are intended to be performed in accordance with this
document. Specification and qualification of brazing procedures that were made in accordance with previous
editions of this document may be used for any application for which the current edition is specified. In this
case, the ranges of qualification of previous editions remain applicable.
Where additional tests need to be carried out to make the qualification technically equivalent, it is only
necessary to perform the additional tests on a test piece which should be made in accordance with this
document.
vi
International Standard ISO 17779:2026(en)
Brazing — Specification and qualification of brazing
procedures for metallic materials
1 Scope
This document specifies requirements for the specification and qualification of brazing procedures for
brazing of metallic materials.
This document specifies requirements for brazing of the test piece, testing of the test specimen, essential
variables and their range of qualification, acceptance criteria, brazing procedure qualification record
(BPQR) and brazing procedure specification (BPS).
This document does not cover testing of residual stresses, corrosion resistance and impact properties.
This document applies to the following brazing processes according to ISO 4063:2023 with local and global
heating:
— 911 Infrared brazing;
— 912 Flame brazing, torch brazing;
— 913 Laser beam brazing;
— 914 Electron beam brazing;
— 916 Induction brazing;
— 918 Resistance brazing;
— 919 Diffusion brazing;
— 921 Furnace brazing;
— 922 Vacuum brazing;
— 923 Dip-bath brazing;
— 924 Salt-bath brazing;
— 925 Flux bath brazing;
— 926 Immersion brazing;
— 972 Arc weld brazing.
This document does not apply to brazing for aerospace applications covered by ISO 11745.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content constitutes
requirements of this document. For dated references, only the edition cited applies. For undated references,
the latest edition of the referenced document (including any amendments) applies.
ISO 4063:2023, Welding, brazing, soldering and cutting — Nomenclature of processes and reference numbers
ISO 18279:2023, Brazing — Imperfections in brazed joints
EN 12797, Brazing — Destructive tests of brazed joints
EN 12799, Brazing — Non-destructive examination of brazed joints
ISO 857-2, Welding and allied processes — Vocabulary — Part 2: Soldering and brazing processes and related
terms
ISO 13585, Brazing — Qualification testing of brazers and brazing operators
ISO 17672, Brazing — Filler metals
ISO 18496, Brazing — Fluxes for brazing — Classification and technical delivery conditions
ISO/TR 25901-1, Welding and allied processes — Vocabulary — Part 1: General terms
3 Terms and definitions
For the purposes of this document, the terms and definitions given in ISO 857-2, ISO/TR 25901-1 and the
following apply.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https:// www .iso .org/ obp
— IEC Electropedia: available at https:// www .electropedia .org/
3.1
brazing
joining process using filler metal with a liquidus temperature above 450 °C
[SOURCE: ISO 857-2:2005, 3.1.2.]
3.2
brazing procedure specification
BPS
document that has been qualified and provides the required variables of the brazing procedure to ensure
repeatability during production brazing
3.3
preliminary brazing procedure specification
pBPS
document containing the required variables of the brazing procedure which is not yet qualified
3.4
brazing procedure qualification record
BPQR
record comprising all necessary data from qualification of a brazing procedure
3.5
manufacturer
workshop or site or both which is (are) under the same technical and quality management
3.6
examiner
person who has been appointed to verify conformance with the applicable standard
Note 1 to entry: In certain cases, an external independent examiner can be required.
[SOURCE: ISO/TR 25901-1:2016, 2.5.29, modified — compliance has been changed to conformance.]
3.7
examining body
organization that has been appointed to verify conformance with the applicable standard
Note 1 to entry: In certain cases, an external independent examining body can be required.
[SOURCE: ISO/TR 25901-1:2016, 2.5.30, modified — compliance has been changed to conformance.]
3.8
filler metal
added metal applied to brazed joints
Note 1 to entry: Filler metal can be in the form of wire, inserts, powder, pastes, foil, etc.
3.9
flux
non-metallic material which, when molten, promotes wetting by removing existing oxide or other detrimental
films from the surfaces to be joined and prevents their re-formation during the joining operation
[SOURCE: ISO 857-2:2005, 3.2.2]
3.10
test piece
brazed assembly which is used for testing purposes
3.11
test specimen
part or portion cut from the test piece in order to perform specified destructive testing
[SOURCE: ISO/TR 25901-1:2016, 2.2.1.6]
4 Preliminary brazing procedure specification (pBPS)
A preliminary brazing procedure specification shall be prepared. An example pBPS form is shown in
Annex B.
5 Brazing procedure test
The brazing and testing of test pieces shall be in accordance with Clause 6 and Clause 7.
A brazer or brazing operator who undertakes the brazing procedure test satisfactorily in accordance with
this document shall be considered qualified for the appropriate range of qualification in accordance with
ISO 13585, provided that the relevant testing requirements are met.
6 Test piece
6.1 General
The test piece or pieces shall be brazed using a type of joint design proposed in the pBPS and be representative
for the intended production.
6.2 Shape and dimensions of test pieces
If not specified in an application standard, the shape and dimension of the test piece shall be agreed by the
contracting parties.
The test piece is typically a basic lap or butt joint in sheet material or a sleeve joint in tube.
NOTE Examples of applicable joint configurations are given in Annex C.
The size of the test piece shall be sufficient to allow all required tests to be carried out. Additional test pieces
may be prepared in order to allow for additional tests and/or for re-testing specimens.
6.3 Brazing of test pieces
Preparation and brazing of test pieces shall be carried out in accordance with the pBPS, and under the
general conditions of bra
...