

SIST EN 10346:2026
(Main)Continuously hot-dip coated steel flat products for cold forming - Technical delivery conditions
- Abstract
This document specifies requirements for continuously hot-dip coated products made of low carbon steels for cold forming, of steels for construction and steels with high proof strength for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ), zinc-magnesium alloy (ZM), aluminium-silicon alloy (AS) or aluminium (A) and for continuously hot-dip coated products made of multiphase steels for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA) or zinc-magnesium alloy (ZM) in thicknesses of 0,20 mm ≤ t ≤ 6,5 mm.
By agreement at the time of enquiry and order, this document is applicable to continuously hot-dip coated flat products of an expanded validity range defined for thicknesses t < 0,20 mm with agreed mechanical properties and test specimens, adhesion of coating and surface condition requirements. This document is applicable to strip of all widths and to sheets cut from it (≥600 mm width) and cut lengths (<600 mm width).
NOTE The products covered by this document are used where cold formability, high strength, a defined minimum yield strength and/or corrosion resistance are the most important factors. Corrosion resistance of the product is depending on coating type and coating thickness, hence to its mass (see also 7.3.2). The products covered by this document can be used as substrates for organic coated flat products specified in EN 10169 for building and general engineering applications.
- Status
- Not Published
- Public Enquiry End Date
- 30-Jul-2025
- Technical Committee
- IFEK - Ferrous metals
- Current Stage
- 6060 - National Implementation/Publication (Adopted Project)
- Start Date
- 26-Oct-2026
- Due Date
- 31-Dec-2026
SIST EN 10346:2026 is the Slovenian standard from SIST for continuously hot-dip coated steel flat products for cold forming. It specifies technical delivery conditions for low carbon steels, steels for construction, steels with high proof strength and multiphase steels, with zinc, zinc-iron alloy, zinc-aluminium alloy, zinc-magnesium alloy, aluminium-silicon alloy or aluminium coatings. Engineers, buyers and quality teams use SIST EN 10346:2026 to agree the steel grade, coating, mechanical properties, surface condition, inspection and delivery details for strip, sheet and cut lengths.
What does SIST EN 10346:2026 specify?
SIST EN 10346:2026 covers continuously hot-dip coated flat products in thicknesses from 0.20 mm to 6.5 mm. It also allows, by agreement at enquiry and order, an expanded validity range below 0.20 mm with agreed mechanical properties, test specimens, coating adhesion and surface condition requirements.
SIST EN 10346:2026 applies to strip of all widths, sheets cut from strip with widths of 600 mm and above, and cut lengths below 600 mm. The note in the scope links the products to cold formability, high strength, minimum yield strength and corrosion resistance, and identifies them as potential substrates for organic coated flat products according to EN 10169.
The document is organized into clauses on scope, normative references, terms and definitions, classification and designation, purchaser information, manufacturing and processing, requirements, inspection, marking, packing, and storage and transportation.
| Annex | What it covers |
|---|---|
| Annex A | Reference method for determining the coating mass of zinc, zinc-iron, zinc-aluminium and zinc-magnesium coatings |
| Annex B | Reference method for determining the coating mass of aluminium-silicon and aluminium coatings |
| Annex C | Reference method for determining the mass of the Al-Fe-Si alloy layer |
| Annex D | Tensile test results and coating impact |
| Annex E | Steel designations for multiphase steels for cold forming |
What are the key requirements of SIST EN 10346:2026?
Product families and designation
SIST EN 10346:2026 groups the products into low carbon steels for cold forming, steels for construction, steels with high proof strength for cold forming, and multiphase steels for cold forming. It classifies them by forming ability, minimum proof strength or minimum tensile strength, depending on the family.
This matters because the grade family drives the expected forming behaviour and the way the product is specified. The steel names and steel numbers follow EN 10027-1 and EN 10027-2, so purchasers can order the exact grade and coating combination instead of describing the product loosely.
Chemical composition and mechanical properties
SIST EN 10346:2026 gives the cast analysis limits in Tables 1 to 5 and, when agreed, the permitted deviations for product analysis in Table 6. It also sets mechanical property requirements in Tables 7 to 11, with different values for low carbon steels, construction steels, high proof strength steels and multiphase steels.
In practice, this means the purchaser can ask for verification of the product analysis, and the manufacturer must control the steel chemistry against the table limits. For mechanical testing, the document ties the required tensile properties to the product family, thickness range and test direction, and it also covers plastic strain ratio r, strain hardening exponent n and, where relevant, bake-hardening index BH.
SIST EN 10346:2026 also states when properties remain valid after the agreed date of availability. That is important for storage and inventory control, because some grades keep their specified properties only for a limited time after delivery.
Coatings, coating mass and surface condition
SIST EN 10346:2026 allows coatings identified as Z, ZF, ZA, ZM, AS and A, and Table 12 gives the standard coating masses. The document also allows other coating masses or different masses on each surface if agreed at enquiry and order.
This matters because coating mass affects corrosion resistance, but thicker coatings can reduce formability and weldability. The standard therefore links the coating choice to the intended process and service environment, and it requires the coating mass to be checked by a triple spot test or, where applicable, a single spot test.
The coating finish and surface quality are also controlled. For zinc-coated products the finish can be normal spangle N or minimized spangle M, while surface qualities A, B and C describe increasing control of appearance and suitability for paint finishing. Surface treatment can be chemically passivated C, oiled O, chemically passivated and oiled CO, phosphated P, phosphated and oiled PO, or sealed S.
Inspection, sampling and delivery
SIST EN 10346:2026 makes non-specific inspection the default unless the order asks for specific testing and inspection documents. It refers to EN 10204 for inspection documents and sets a test unit of up to 30 t, or a fraction of 30 t, of the same grade, thickness, coating mass and surface condition.
The document specifies sampling, tensile testing, r and n determinations, bake-hardening testing, surface inspection and coating mass testing. In disputes, the coating mass is checked by the reference methods in Annex A, B or C. This matters for acceptance testing, incoming inspection and supplier quality claims.
What terms does SIST EN 10346:2026 define?
- Nominal (specified) thickness - the ordered thickness of the metallic coated product, including both the steel core and the coating.
- Steel core thickness - the nominal thickness minus the metallic coating layers; this is the design thickness used for calculations in EN 1993-1-3.
- Coating mass - the total mass of coating on both surfaces, expressed in g/m², and used together with the coating symbol to identify the coating.
- Bake-hardening steel (B) - a steel that increases in proof strength after heating in the defined bake-hardening condition.
- Dual-phase steel with improved formability (XH) - a dual-phase steel mainly made of ferrite and martensite with small amounts of bainite and retained austenite.
- Complex-phase steel with improved formability (CH) - a steel mainly made of martensite, bainite and retained austenite.
- Transformation induced plasticity steel (T) - a ferritic steel containing retained austenite that transforms during forming, increasing work hardening.
- Steel for construction - a steel with minimum strength levels and no special demand for suitability for cold forming.
Who uses SIST EN 10346:2026?
SIST EN 10346:2026 is used by steel producers, coil coaters, fabricators, purchasers and inspection laboratories that buy, make or test hot-dip coated flat products for cold forming. It is also used by quality managers and buyers who need to specify grade, coating, surface quality, inspection documents and packaging in an order.
The standard is relevant where cold formability, strength, corrosion resistance and controlled surface appearance matter. The scope and notes point to building and general engineering applications, and the product designations also support users who need advanced high strength steels for forming and subsequent processing.
What changed in SIST EN 10346:2026 from the previous edition?
SIST EN 10346:2026 replaces EN 10346:2015. The foreword lists these significant changes:
- the scope and normative references were updated;
- EN 10373, EN 1090-4, EN 1993-1-1 and EN 1993-1-3 were added as normative references;
- definitions were added in Clause 3;
- hot-dip aluminium coating was added and hot-dip aluminium-zinc alloy coating was deleted;
- new steel families XH, CH and AH were added;
- options for S550GDR and S650GDR were added in Clause 5.2;
- new construction grades S500GD, S550GDR and S650GDR were added;
- new micro-alloyed grades HX600LAD and HX700LAD were added;
- minimum proportional elongation requirements were added for certain construction and micro-alloyed grades at thicknesses of 3.0 mm and above;
- new cold-rolled and hot-rolled multiphase steels were added;
- informative Annex D on tensile test results and coating impact was added;
- informative Annex E on steel designations for multiphase steels for cold forming was added.
Which standards are used with SIST EN 10346:2026?
| Standard | What it contributes |
|---|---|
| EN 10020 | Definition and classification of grades of steel |
| EN 10021 | General technical delivery conditions for steel products |
| EN 10027-1 | Steel names |
| EN 10027-2 | Steel numbers |
| EN 10049 | Measurement of roughness average Ra and peak count RPc |
| EN 10079 | Definitions of steel products |
| EN 10143 | Tolerances on dimensions and shape |
| EN 10204 | Types of inspection documents |
| EN 10325 | Determination of yield strength increase by heat treatment, used for BH |
| EN ISO 6892-1 | Tensile testing at room temperature |
| EN ISO 10113 | Determination of plastic strain ratio r |
| EN ISO 10275 | Determination of strain hardening exponent n |
| EN 10373 | Alternative model-based determination of physical and mechanical properties |
| EN 1090-4 | Technical requirements for cold-formed structural steel elements and structures |
| EN 1993-1-1 | General rules for design of steel structures |
| EN 1993-1-3 | Rules for cold-formed members and sheeting |
| EN 10169 | Organic coated flat products, named as a downstream application for these substrates |
What does the SIST EN 10346:2026 document contain?
SIST EN 10346:2026 contains composition tables, mechanical property tables, coating mass tables, coating finish and surface quality tables, inspection rules and delivery information. Tables 1 to 6 set chemistry, Tables 7 to 11 set mechanical properties, Table 12 sets coating masses, and Tables 13 to 15 set surface finish and quality combinations.
It also contains the specimen and test provisions needed for quality control, including tensile test setup, r and n determination, bake-hardening index testing, surface inspection and coating mass measurement. Annex D adds a figure comparing three tensile test calculation methods on coated steel, and Annex E maps the multiphase steel names and numbers to VDA 239-100 designations.
For coating mass disputes, Annex A, Annex B and Annex C provide the reference chemical methods. The document therefore supports specification, production control, acceptance testing and supplier documentation without reproducing the full normative tables in the ordering process.
Relations
- Referred By
SIST EN 845-2:2004 - Specification for ancillary components for masonry - Part 2: Lintels - Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Referred By
SIST EN 16475-2:2017 - Chimneys - Accessories - Part 2: Chimney fans - Requirements and test methods - Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
- Effective Date
- 21-Oct-2026
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.
Inštitut za kovinske materiale in tehnologije
Institute of Metals and Technology. Materials testing, metallurgical analysis, NDT.
Sponsored listings
Frequently Asked Questions
SIST EN 10346:2026 is a draft published by the Slovenian Institute for Standardization (SIST). Its full title is "Continuously hot-dip coated steel flat products for cold forming - Technical delivery conditions". This standard covers: This document specifies requirements for continuously hot-dip coated products made of low carbon steels for cold forming, of steels for construction and steels with high proof strength for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ), zinc-magnesium alloy (ZM), aluminium-silicon alloy (AS) or aluminium (A) and for continuously hot-dip coated products made of multiphase steels for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA) or zinc-magnesium alloy (ZM) in thicknesses of 0,20 mm ≤ t ≤ 6,5 mm. By agreement at the time of enquiry and order, this document is applicable to continuously hot-dip coated flat products of an expanded validity range defined for thicknesses t < 0,20 mm with agreed mechanical properties and test specimens, adhesion of coating and surface condition requirements. This document is applicable to strip of all widths and to sheets cut from it (≥600 mm width) and cut lengths (<600 mm width). NOTE The products covered by this document are used where cold formability, high strength, a defined minimum yield strength and/or corrosion resistance are the most important factors. Corrosion resistance of the product is depending on coating type and coating thickness, hence to its mass (see also 7.3.2). The products covered by this document can be used as substrates for organic coated flat products specified in EN 10169 for building and general engineering applications.
This document specifies requirements for continuously hot-dip coated products made of low carbon steels for cold forming, of steels for construction and steels with high proof strength for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ), zinc-magnesium alloy (ZM), aluminium-silicon alloy (AS) or aluminium (A) and for continuously hot-dip coated products made of multiphase steels for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA) or zinc-magnesium alloy (ZM) in thicknesses of 0,20 mm ≤ t ≤ 6,5 mm. By agreement at the time of enquiry and order, this document is applicable to continuously hot-dip coated flat products of an expanded validity range defined for thicknesses t < 0,20 mm with agreed mechanical properties and test specimens, adhesion of coating and surface condition requirements. This document is applicable to strip of all widths and to sheets cut from it (≥600 mm width) and cut lengths (<600 mm width). NOTE The products covered by this document are used where cold formability, high strength, a defined minimum yield strength and/or corrosion resistance are the most important factors. Corrosion resistance of the product is depending on coating type and coating thickness, hence to its mass (see also 7.3.2). The products covered by this document can be used as substrates for organic coated flat products specified in EN 10169 for building and general engineering applications.
SIST EN 10346:2026 is classified under the following ICS (International Classification for Standards) categories: 77.140.50 - Flat steel products and semi-products. The ICS classification helps identify the subject area and facilitates finding related standards.
SIST EN 10346:2026 has the following relationships with other standards: It is inter standard links to SIST EN 845-2:2004, SIST EN 845-3:2013, SIST EN 1090-4:2018, SIST ENV 13381-5:2003, SIST EN 1090-2:2018+A1:2024, SIST EN 840-5:2020, SIST EN 1856-2:2009, SIST EN 13964:2004, SIST EN 1995-1-1:2005, SIST EN 16475-2:2017, SIST EN 14782:2006, SIST EN 845-3:2004+A1:2008, SIST EN 13071-1:2008, SIST EN 508-1:2021, SIST EN 505:2013. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
SIST EN 10346:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
oSIST prEN 10346:2025
01-julij-2025
Kontinuirno vroče prevlečeni jekleni ploščati izdelki za hladno preoblikovanje -
Tehnični dobavni pogoji
Continuously hot-dip coated steel flat products for cold forming - Technical delivery
conditions
Kaltgewalzte kontinuierlich schmelztauchveredelte Flacherzeugnisse aus Stahl -
Technische Lieferbedingungen
Produits plats en acier revêtus en continu par immersion à chaud pour formage à froid -
Conditions techniques de livraison
Ta slovenski standard je istoveten z: prEN 10346
ICS:
77.140.50 Ploščati jekleni izdelki in Flat steel products and semi-
polizdelki products
oSIST prEN 10346:2025 en,fr,de
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
oSIST prEN 10346:2025
oSIST prEN 10346:2025
DRAFT
EUROPEAN STANDARD
prEN 10346
NORME EUROPÉENNE
EUROPÄISCHE NORM
May 2025
ICS 77.140.50 Will supersede EN 10346:2015
English Version
Continuously hot-dip coated steel flat products for cold
forming - Technical delivery conditions
Produits plats en acier revêtus en continu par Kaltgewalzte kontinuierlich schmelztauchveredelte
immersion à chaud pour formage à froid - Conditions Flacherzeugnisse aus Stahl - Technische
techniques de livraison Lieferbedingungen
This draft European Standard is submitted to CEN members for enquiry. It has been drawn up by the Technical Committee
CEN/TC 459/SC 9.
If this draft becomes a European Standard, CEN members are bound to comply with the CEN/CENELEC Internal Regulations
which stipulate the conditions for giving this European Standard the status of a national standard without any alteration.
This draft European Standard was established by CEN in three official versions (English, French, German). A version in any other
language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC
Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
Recipients of this draft are invited to submit, with their comments, notification of any relevant patent rights of which they are
aware and to provide supporting documentation.
Warning : This document is not a European Standard. It is distributed for review and comments. It is subject to change without
notice and shall not be referred to as a European Standard.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2025 CEN All rights of exploitation in any form and by any means reserved Ref. No. prEN 10346:2025 E
worldwide for CEN national Members.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
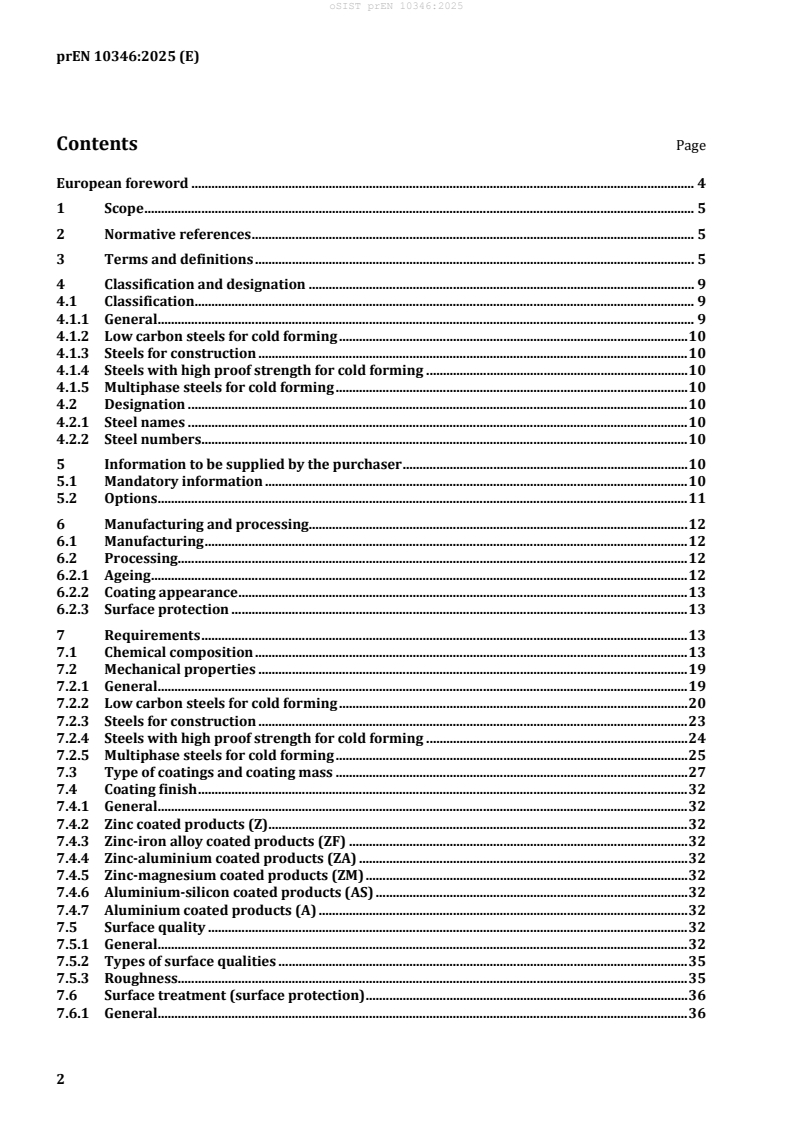
Contents Page
European foreword . 4
1 Scope . 5
2 Normative references . 5
3 Terms and definitions . 5
4 Classification and designation . 9
4.1 Classification . 9
4.1.1 General . 9
4.1.2 Low carbon steels for cold forming . 10
4.1.3 Steels for construction . 10
4.1.4 Steels with high proof strength for cold forming . 10
4.1.5 Multiphase steels for cold forming . 10
4.2 Designation . 10
4.2.1 Steel names . 10
4.2.2 Steel numbers . 10
5 Information to be supplied by the purchaser . 10
5.1 Mandatory information . 10
5.2 Options . 11
6 Manufacturing and processing. 12
6.1 Manufacturing . 12
6.2 Processing . 12
6.2.1 Ageing . 12
6.2.2 Coating appearance . 13
6.2.3 Surface protection . 13
7 Requirements . 13
7.1 Chemical composition . 13
7.2 Mechanical properties . 19
7.2.1 General . 19
7.2.2 Low carbon steels for cold forming . 20
7.2.3 Steels for construction . 23
7.2.4 Steels with high proof strength for cold forming . 24
7.2.5 Multiphase steels for cold forming . 25
7.3 Type of coatings and coating mass . 27
7.4 Coating finish . 32
7.4.1 General . 32
7.4.2 Zinc coated products (Z) . 32
7.4.3 Zinc-iron alloy coated products (ZF) . 32
7.4.4 Zinc-aluminium coated products (ZA) . 32
7.4.5 Zinc-magnesium coated products (ZM) . 32
7.4.6 Aluminium-silicon coated products (AS) . 32
7.4.7 Aluminium coated products (A) . 32
7.5 Surface quality . 32
7.5.1 General . 32
7.5.2 Types of surface qualities . 35
7.5.3 Roughness . 35
7.6 Surface treatment (surface protection) . 36
7.6.1 General . 36
oSIST prEN 10346:2025
prEN 10346:2025 (E)
7.6.2 Chemical passivation (C) . 36
7.6.3 Oiling (O) . 36
7.6.4 Chemical passivation and oiling (CO) . 36
7.6.5 Phosphating (P) . 37
7.6.6 Sealing (S) . 37
7.7 Coil breaks and bends (kinks) . 37
7.7.1 Freedom from coil breaks . 37
7.7.2 Bends (kinks) by winding on coiler drums . 37
7.8 Stretcher strains . 37
7.9 Coating mass . 37
7.10 Adhesion of coating . 38
7.11 Surface condition . 38
7.12 Tolerances on dimensions and shape . 38
7.13 Suitability for further processing . 38
8 Inspection . 38
8.1 Types of inspection and inspection documents. 38
8.2 Test units . 39
8.3 Tests to be carried out . 39
8.4 Sampling . 39
8.5 Test methods . 40
8.5.1 Tensile test . 40
8.5.2 Plastic strain ratio and hardening exponent . 41
8.5.3 Bake hardening index . 41
8.5.4 Surface inspection . 41
8.5.5 Coating mass . 41
8.6 Retests . 41
9 Marking . 41
10 Packing . 42
11 Storage and transportation . 42
Annex A (normative) Reference method for determination of the zinc, zinc-iron, zinc-
aluminium and zinc-magnesium coating mass . 43
Annex B (normative) Reference method for determination of the aluminium-silicon and
aluminium coating mass . 45
Annex C (normative) Reference method for determination of the mass of the Al-Fe-Si alloy
layer . 46
Annex D (informative) Tensile test results and coating impact . 47
Annex E (informative) Steel designations for multiphase steels for cold forming . 49
Bibliography . 51
oSIST prEN 10346:2025
prEN 10346:2025 (E)
European foreword
This document (prEN 10346:2025) has been prepared by Technical Committee CEN/TC 459/SC 9
“Coated and uncoated flat products to be used for cold forming”, the secretariat of which is held by
AFNOR.
This document is currently submitted to the CEN Enquiry.
This document will supersede EN 10346:2015.
prEN 10346:2025 includes the following significant technical changes with respect to EN 10346:2015:
— scope and normative references have been updated;
— addition of normative reference to:
o EN 10373, Determination of the physical and mechanical properties of steels using models;
o EN 1090-4, Execution of steel structures and aluminium structures - Part 4: Technical
requirements for cold-formed structural steel elements and cold-formed structures for roof, ceiling,
floor and wall applications
o EN 1993-1-1, Eurocode 3 - Design of steel structures - Part 1-1: General rules and rules for buildings
o EN 1993-1-3, Eurocode 3 - Design of steel structures - Part 1-3: General rules - Supplementary rules
for cold-formed members and sheeting
— definitions have been added in Clause 3;
— addition of hot-dip aluminium coating and deletion of hot-dip aluminium-zinc alloy coating;
— addition of three new steel families: dual-phase steels with improved formability (XH), complex-
phase steels with improved formability (CH) and multi-phase steels with improved formability (AH);
— addition of options referring to new steel grades S550GDR and S650GDR in Clause 5.2;
— addition of three new steel grades for construction: S500GD, S550GDR and S650GDR;
— addition of two new micro-alloyed steel grades: HX600LAD and HX700LAD;
— addition of minimum requirements regarding proportional elongation of steel grades for
construction and micro-alloyed steel grades with thickness ≥ 3,0 mm;
— addition of cold-rolled multiphase steels for cold forming: HCT780XG, HCT1180X, HCT1180XG,
HCT590XH, HCT780XH, HCT980XH, HCT1180XH, HCT1180C, HCT980CH, HCT1180CH, HCT1370CH,
HCT980AH and HCT1180AH;
— addition of hot-rolled multiphase steels for cold forming: HDT760C and HDT950C;
— addition of an informative Annex about tensile tests results and coating impact;
— addition of an informative Annex about steel designations for multiphase steels for cold forming.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
1 Scope
This document specifies requirements for continuously hot-dip coated products made of low carbon
steels for cold forming, of steels for construction and of steels with high proof strength for cold forming
coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), zinc-magnesium alloy (ZM),
aluminium-silicon alloy (AS) or aluminium (A) and for continuously hot-dip coated products made of
multiphase steels for cold forming coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA) or
zinc-magnesium alloy (ZM) in thicknesses of 0,20 mm ≤ t ≤ 6,5 mm.
By agreement at the time of enquiry and order, this document is applicable to continuously hot-dip coated
flat products of an expanded validity range defined for thicknesses t < 0,20 mm with agreed mechanical
properties and test specimens, adhesion of coating and surface condition requirements. This document
applies to strip of all widths and to sheets cut from it (≥600 mm width) and cut lengths (<600 mm width).
NOTE The products covered by this document are used where cold formability, high strength, a defined
minimum yield strength and/or corrosion resistance are the most important factors. Corrosion resistance of the
product is depending on coating type and coating thickness, hence to its mass (see also 7.3.2). The products covered
by this document can be used as substrates for organic coated flat products specified in EN 10169 for building and
general engineering applications.
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 10020, Definition and classification of grades of steel
EN 10021, General technical delivery conditions for steel products
EN 10027-1, Designation systems for steels — Part 1: Steel names
EN 10027-2, Designation systems for steels — Part 2: Numerical system
EN 10049, Measurement of roughness average Ra and peak count RPc on metallic flat products
EN 10079, Definition of steel products
EN 10143, Continuously hot-dip coated steel sheet and strip — Tolerances on dimensions and shape
EN 10204, Metallic products — Types of inspection documents
EN 10325, Steel — Determination of yield strength increase by the effect of heat treatment [Bake-
Hardening-Index]
EN ISO 6892-1, Metallic materials — Tensile testing — Part 1: Method of test at room temperature
(ISO 6892-1)
EN ISO 10113, Metallic materials — Sheet and strip — Determination of plastic strain ratio (ISO 10113)
EN ISO 10275, Metallic materials — Sheet and strip — Determination of tensile strain hardening exponent
(ISO 10275)
3 Terms and definitions
For the purposes of this document, the terms and definitions given in EN 10020, EN 10021, EN 10079,
EN 10204 and the following apply.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp/
— IEC Electropedia: available at https://www.electropedia.org/
NOTE General definitions and guidelines for the protection of iron and steel can be found in EN ISO 14713-1.
3.1
nominal (specified) thickness
ordered thickness of the metallic coated product
Note 1 to entry: Nominal thickness includes both steel core and coating (t )
nom
3.2
steel core thickness
nominal (specified) thickness minus the metallic coating layers
Note 1 to entry: The steel core thickness is in accordance with the definition in EN 1993-1-3 (t ). It is the design
cor
thickness for calculations in accordance with EN 1993-1-3.
3.3
hot-dip zinc coating
Z
application of a zinc coating by immersing the prepared strip in a molten bath of zinc
Note 1 to entry: The zinc content is at least 98,5 mass %.
Note 2 to entry: See also 7.4.2.
3.4
hot-dip zinc-iron alloy coating
ZF
application of a zinc-iron coating by immersing the prepared strip in a molten bath of zinc and a
subsequent annealing
Note 1 to entry: The zinc content of the bath is at least 99 mass %.
Note 2 to entry: The annealing produces an iron-zinc coating with an iron content of normally 8 mass % to 12 mass
%.
Note 3 to entry: See also 7.4.3.
3.5
hot-dip zinc-aluminium coating
ZA
application of a zinc-aluminium coating by immersing the prepared strip in a molten bath of zinc-
aluminium
Note 1 to entry: The composition of the bath is approximately 5 mass % aluminium, small amounts of mischmetal
and the balance zinc.
Note 2 to entry: See also 7.4.4.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
3.6
hot dip zinc-magnesium coating
ZM
application of a zinc-magnesium coating by immersing the prepared strip in a molten bath of zinc-
aluminium-magnesium
Note 1 to entry: The composition of the bath is sum of aluminium and magnesium from 1,5 mass % to 8 mass %,
containing minimum of 0,2 mass % magnesium and the balance zinc.
Note 2 to entry: For information on chemical composition and density, the manufacturer can be asked for advice.
Note 3 to entry: Due to differences in coating bath chemistry, the properties provided by each coating can differ
(e.g surface aspect, processability, corrosion resistance) and the manufacturer can be asked for advice.
Note 4 to entry: See also 7.4.5.
3.7
hot-dip aluminium-silicon alloy coating
AS
application of an aluminium-silicon coating by immersing the prepared strip in a molten bath of
aluminium-silicon
Note 1 to entry: The composition of the bath is 8 to 11 mass % silicon, up to 5 mass % iron, up to 1 mass %
additional elements and the balance aluminium.
Note 2 to entry: See also 7.4.6.
3.8
hot-dip aluminium coating
A
application of an aluminium coating by immersing the prepared strip in a molten bath of pure aluminium
Note 1 to entry: The iron content in the bath is less than 5 mass %.
Note 2 to entry: see also 7.4.7.
3.9
coating mass
total mass of coating given for both surfaces
Note 1 to entry: In combination with the symbol for the coating type (Z, ZF, ZA, ZM, AS,A), the nominal coating mass
is used as coating designation.
Note 2 to entry: The coating mass is expressed in grams per square metre.
Note 3 to entry: See 7.9.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
3.10
bake-hardening steel
B
steel exhibiting an increase in proof strength following heating in the region of 170°C for 20 min
Note 1 to entry: These steels have a good suitability for cold forming and present a high resistance to plastic
straining (which is increased on finished parts during heat treatment) and a good dent resistance.
3.11
complex-phase steel
C
steel with a multiphase microstructure containing mainly bainite, ferrite, whereas martensite, tempered
martensite, retained austenite and pearlite may be present as additional phases
Note 1 to entry: The fine grained microstructure can be generated by retarded recrystallization or precipitation of
micro-alloying elements.
3.12
complex-phase steel with improved formability
CH
steel consisting mainly of martensite, bainite and retained austenite
Note 1 to entry: Depending on strength class, small amounts of ferrite can also be present.
Note 2 to entry: At a given high tensile strength, complex phase steels with improved formability show a high yield
ratio (Re/Rm).
3.13
dual-phase steel
X
steel consisting of mainly ferrite and martensite and possible bainite as a complementary phase
Note 1 to entry: According to their high tensile strength levels, dual phase steels show a low yield strength ratio
and a high work hardening rate.
3.14
dual-phase steel with improved formability
XH
steel consisting mainly of ferrite and martensite and small amounts of bainite and retained austenite
Note 1 to entry: According to their high tensile strength levels, dual phase steels with improved formability show
higher uniform elongation.
3.15
ferritic-bainitic steel
F
steel with a matrix of ferrite or strengthened ferrite containing bainite or strengthened bainite
Note 1 to entry: The strengthening of the matrix is caused by a high density of dislocations, by grain refinement
and precipitation of micro-alloying elements.
Symbol used in the steel name (see Tables 3, 4 and 5).
oSIST prEN 10346:2025
prEN 10346:2025 (E)
3.16
high strength interstitial free steel
Y
steel whose composition is controlled to achieve improved plastic strain ratio r and strain hardening
exponent n values
Note 1 to entry: These steels have both, a high mechanical strength and an excellent suitability for cold forming,
due to their solid solution hardening and interstitial free microstructure.
3.17
low alloy steel
micro-alloyed steel
LA
steel containing one or more of alloying elements Nb, Ti and V to achieve required proof strength levels
Note 1 to entry: Combined precipitation and grain refinement hardening modes allow reaching a high mechanical
resistance while reducing the content of alloying elements.
Note 2 to entry: Alternatively, carbon-manganese alloying concepts in combination with grain refinement can be
used.
3.18
low carbon steel
steel with low carbon content characterized by low yield strength and high ductility
3.19
multi-phase steels with high global formability
AH
steel containing a combination of tempered martensite, bainite and retained austenite
Note 1 to entry: Ferrite and martensite can be present.
3.20
steel for construction
steel with minimum strength levels and no special demand for suitability for cold forming
3.21
transformation induced plasticity steel
T
steel with a ferritic matrix containing retained austenite capable of transformation into martensite during
the forming process (TRIP effect)
Note 1 to entry: Because of high work-hardening rate the steel reaches high uniform elongation values and high
tensile strength levels.
4 Classification and designation
4.1 Classification
4.1.1 General
The steels covered by this document are either alloy quality steels or non-alloy quality steels in
accordance with EN 10020. All steels in Tables 1, 3, 4, 5 and steel grade S650GDR in Table 2 are alloy
quality steels. All steels in Table 2 with the exception of S650GDR are non-alloy quality steels.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
4.1.2 Low carbon steels for cold forming
The steel grades are classified in accordance with their increasing suitability for cold forming as follows
(see Table 7):
— DX51D: bending and profiling quality;
— DX52D: drawing quality;
— DX53D: deep drawing quality;
— DX54D: special deep drawing quality;
— DX55D: special deep drawing quality (only +AS);
— DX56D: extra deep drawing quality;
— DX57D: super deep drawing quality;
— DX58D: extra super deep drawing quality.
Only steel grades DX51D, DX52D and DX53D can be ordered as hot rolled products.
4.1.3 Steels for construction
The steel grades are classified in accordance with their increasing minimum proof strength Rp (see
0,2
Table 8).
4.1.4 Steels with high proof strength for cold forming
The steel grades are classified in accordance with their increasing minimum proof strength Rp (see
0,2
Table 9).
Only low alloy/micro-alloyed steel grades can be ordered as hot rolled products.
4.1.5 Multiphase steels for cold forming
The steel grades are classified in accordance with their increasing minimum tensile strength Rm (see
Tables 10 and 11). See Annex E for the steel names and steel numbers of advanced high strength steels
(AHSS).
4.2 Designation
4.2.1 Steel names
The steel names shall be in accordance with EN 10027-1.
4.2.2 Steel numbers
The steel numbers shall be in accordance with EN 10027-2.
5 Information to be supplied by the purchaser
5.1 Mandatory information
The following information shall be supplied by the purchaser at the time of enquiry and order:
a) quantity to be delivered;
b) type of product (strip, sheet, cut length);
oSIST prEN 10346:2025
prEN 10346:2025 (E)
c) number of the dimensional standard in accordance with EN 10143;
d) nominal dimensions and the tolerances on dimensions and shape and, if applicable, letters denoting
relevant special tolerances;
e) term “steel”;
f) number of this document, i.e. EN 10346;
g) steel name or steel number and symbol for the type of hot-dip coating as given in Tables 1 to 5;
h) number designating the nominal mass of coating (e.g. 275 = 275 g/m including both surfaces, see
Table 12);
i) letter denoting the coating finish (N or M, see 7.4.2 and Table 13);
j) letter denoting the surface quality (A, B or C, see 7.5 and Tables 13 to 15);
k) letter denoting the surface treatment (C, O, CO, P, PO or S, see 7.6);
l) if relevant (see 8.5.1), selection of the test piece (proportional (A ) or non-proportional (A )
prop 80
specimen) for determination of the mechanical properties.
EXAMPLE 1 sheet, delivered with dimensional tolerances in accordance with EN 10143 with nominal
thickness of 0,80 mm, ordered with special thickness tolerances (S), nominal width 1 200 mm, ordered with special
width tolerances (S), nominal length 2 500 mm, ordered with special flatness tolerances (FS), made of steel
DX53D+Z (1.0951+Z) in accordance with EN 10346, coating mass 100 g/m (100), minimized spangle (M), surface
quality (B), surface treatment oiled (O):
1 sheet EN 10143 — 0,80Sx1200Sx2500FS — steel EN 10346 — DX53D+Z100–M–B–O
or:
1 sheet EN 10143 — 0,80Sx1200Sx2500FS — steel EN 10346 — 1.0951+Z100 –M–B–O.
5.2 Options
A number of options are specified in this document and listed below. lf the purchaser does not indicate a
wish to implement any of these options, the products shall be supplied in accordance with the basis
specification of this document (see 5.1).
1) specification of product thicknesses deviating from those generally covered in the scope (i.e.
t < 0,20 mm) (see Scope);
2) verification of the product analysis (see 7.1);
3) date of supply for products free from stretcher strains when cold forming (see 7.2.1.3);
4) products supplied suitable for the manufacture of a specific part (see 7.2.2.2 and 7.2.4.2);
5) supply of steel grade S550GDR with specified minimum ratio Rm/Re ≥ 1,10 and A ≥ 15 % for
prop
dimensioning in accordance with EN 1993-1-1 (see 7.2.3 – Table 8), where Re is either Rp or Re in
02 H
dependence of yield point phenomenon (footnote b, Table 8).
In case of organic coated steel, this option 5 is upon agreement of the manufacturer.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
6) Supply of steel grade S550GDR or S650GDR with specified minimum ratio Rm/Re ≥ 1,05 for
dimensioning in accordance with EN 1993-1-1 (see 7.2.3 – Table 8), where Re is either Rp or Re in
02 H
dependence of yield point phenomenon (footnote b, Table 8).
In case of organic coated steel, this option 6 is upon agreement of the manufacturer.
7) coating masses different from those of Table 12 and/or special requirements for different coating
masses on each surface (see 7.3.2);
8) special coatings and/or surface qualities (see Tables 13 and 15, footnote a);
9) hot-dip zinc coated products with pronounced spangle (see 7.4.2.1);
10) special requirements for a maximum Al-Fe-Si alloy layer mass occurring during hot-dip aluminium-
silicon coating (see 7.4.7);
11) hot-dip coated products with surface quality A without skin passing (see 7.5.2.1);
12) requirement for special applications on bright appearance for aluminium-silicon coated products
(type B surface, see NOTE to 7.5.2.2);
13) range and verification of surface roughness (see 7.5.3);
14) selection of the protective oil (see 7.6.1);
15) type of S coating (see 7.6.6);
16) products free from coil breaks (see 7.7.1);
17) type of inspection and, if applicable, inspection document to be delivered (see 8.1);
18) notification of which surface has been inspected (see 8.5.4.2);
19) marking desired by branding of the products (see 9.2);
20) requirement for packing (see Clause 10);
21) according to EN 1090-4
i) determination of the ratio bend radius to thickness, if relevant;
ii) display of the result of the adhesion test in the inspection document (see 7.10).
6 Manufacturing and processing
6.1 Manufacturing
Unless there are restrictions by the selected steel grade, the processes used in steelmaking and the
manufacture of the products shall be left to the discretion of the manufacturer.
6.2 Processing
6.2.1 Ageing
Due to ageing, a reduction in formability can take place for all the products supplied according to this
document. Coil breaks or fluting can occur additionally during processing. The risk of coil breaks
increases, especially for thicknesses > 0,9 mm, with the duration of storage.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Therefore the user should process the products after their receipt as quick as possible (see 7.2.1.3).
6.2.2 Coating appearance
The coating surface can vary and change to a dark appearance by oxidation.
Due to ageing of the coating a certain cracking of the surface can appear during processing which can
consequently reduce abrasion resistance.
The user should take these characteristics into account.
6.2.3 Surface protection
Regarding surface protection during transport and storage the following should be taken into
consideration:
— Only a temporary corrosion resistance during transportation or storage is provided by any surface
protection applied. Colour changes can occur.
— In particular, protection by oiling is dependent on storage time. The primarily uniform oil film
becomes more and more unequal, and bare spots can develop. Different oils can show different
behaviour.
7 Requirements
7.1 Chemical composition
The chemical composition according to the cast analysis shall be as specified in Tables 1 to 5.
If a product analysis is agreed at the time of enquiry and order, the permitted deviations from the cast
analysis given in Tables 1 to 5 shall meet the requirements in Table 6.
Table 1 — Chemical composition (cast analysis) of low carbon steels for cold forming
Chemical composition
Designation % by mass
max.
Steel grade
Symbols for the types of
a
C Si Mn P S Ti
Steel Steel
available coatings
name number
DX51D 1.0917 +Z,+ZF,+ZA,+ZM, +AS 0,18 1,20 0,12
DX52D 1.0918 +Z,+ZF,+ZA,+ZM, +AS
DX53D 1.0951 +Z,+ZF,+ZA,+ZM, +AS
DX54D 1.0952 +Z,+ZF,+ZA,+ZM, +AS
DX55D 1.0962 +AS 0,12 0,50 0,60 0,10 0,045 0,30
DX56D 1.0963 +Z,+ZF,+ZA,+ZM, +AS
DX57D 1.0853 +Z,+ZF,+ZA,+ZM,+AS
DX58D 1.9946 +Z
a
By agreement at the time of enquiry and order, the content of Ti for the steel grades mentioned in
this Table may be lowered to < 0,05 % which means that the steel grade is non alloyed.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Table 2 — Chemical composition (cast analysis) of steels for construction
Chemical composition
Designation % by mass
max.
Steel grade
Symbols for the types of
C Si Mn P S
Steel
available coatings
Steel name
number
S220GD 1.0241 +Z,+ZF,+ZA,+ZM, +A
S250GD 1.0242 +Z,+ZF,+ZA,+ZM, +AS, +A
S280GD 1.0244 +Z,+ZF,+ZA,+ZM, +AS, +A
S320GD 1.0250 +Z,+ZF,+ZA,+ZM, +AS, +A
S350GD 1.0529 +Z,+ZF,+ZA,+ZM, +AS, +A
S390GD 1.0238 +Z,+ZF,+ZA,+ZM 0,20 0,60 1,70 0,10 0,045
S420GD 1.0239 +Z,+ZF,+ZA,+ZM
S450GD 1.0233 +Z,+ZF,+ZA,+ZM
S500GD 1.9527 +Z,+ZF,+ZA,+ZM
S550GD 1.0531 +Z,+ZF,+ZA,+ZM
Steels for construction with specified minimum ductility (R)
a
S550GDR 1.9541 +Z,+ZA,+ZM 0,20 0,60 1,70 0,10 0,045
a
S650GDR 1.9542 +Z, +ZA,+ZM 0,2 0,6 2,00 0,10 0,045
By agreement at the time of enquiry and order, if other chemical elements are added, they shall be
mentioned on the inspection document which may need a change of classification.
a
R means steel grade with specified minimum ductility, because these steels show a high total elongation in
relation to high strengths.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Table 3 — Chemical composition (cast analysis) of steels
with high proof strength for cold forming
Chemical composition
Steel grade
% by mass
+Z,+ZF,+ZA, +ZM, +AS C Si Mn P S Al Nb Ti
total
Steel name Steel number max. max. max. max. max. max. max.
HX160YD 1.0910 0,01 0,30 0,60 0,060 0,025 ≥ 0,010 0,09 0,12
HX180YD 1.0921 0,01 0,30 0,70 0,060 0,025 ≥ 0,010 0,09 0,12
HX180BD 1.0914 0,06 0,50 0,70 0,060 0,025 ≥ 0,015 0,09 0,12
HX220YD 1.0923 0,01 0,30 0,90 0,080 0,025 ≥ 0,010 0,09 0,12
HX220BD 1.0919 0,08 0,50 0,70 0,085 0,025 ≥ 0,015 0,09 0,12
HX260YD 1.0926 0,01 0,30 1,60 0,10 0,025 ≥ 0,010 0,09 0,12
HX260BD 1.0924 0,10 0,50 1,00 0,10 0,030 ≥ 0,010 0,09 0,12
HX260LAD 1.0929 0,11 0,50 1,00 0,030 0,025 ≥ 0,015 0,09 0,15
HX300YD 1.0927 0,015 0,30 1,60 0,10 0,025 ≥ 0,010 0,09 0,12
HX300BD 1.0930 0,11 0,50 0,80 0,12 0,025 ≥ 0,010 0,09 0,12
HX300LAD 1.0932 0,12 0,50 1,40 0,030 0,025 ≥ 0,015 0,09 0,15
HX340BD 1.0945 0,11 0,50 0,80 0,12 0,025 ≥ 0,010 0,09 0,12
HX340LAD 1.0933 0,12 0,50 1,4 0,030 0,025 ≥ 0,015 0,10 0,15
HX380LAD 1.0934 0,12 0,50 1,5 0,030 0,025 ≥ 0,015 0,10 0,15
HX420LAD 1.0935 0,12 0,50 1,6 0,030 0,025 ≥ 0,015 0,10 0,15
HX460LAD 1.0990 0,15 0,50 1,7 0,030 0,025 ≥ 0,015 0,10 0,15
HX500LAD 1.0991 0,15 0,50 1,7 0,030 0,025 ≥ 0,015 0,10 0,15
HX600LAD 1.9950 0,15 0,50 2,0 0,030 0,025 ≥ 0,015 0,10 0,15
HX700LAD 1.9951 0,15 0,50 2,0 0,030 0,025 ≥ 0,015 0,10 0,17
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Table 4 — Chemical composition (cast analysis) of multiphase steels
for cold forming (cold rolled products)
Chemical composition
Steel grade % by mass
+Z,+ZF,+ZM
Cr + Nb +
C Si Mn P S Al B
total
Mo Ti
Steel name Steel number max. max. max. max. max. max. max. max.
Dual-phase steels (X)
0,015 to
HCT450X 1.0937 0,14 0,75 2,00 0,080 0,015
1,00 0,15 0,005
1,0
0,015 to
HCT490X 1.0995 0,14 0,50 1,80 0,050 0,010 1,00 0,15 0,005
1,0
0,015 to
HCT590X 1.0996 0,15 0,80 2,50 0,050 0,010 1,40 0,15 0,005
1,5
0,015 to
HCT780X 1.0943 0,18 0,80 2,50 0,050 0,010 1,40 0,15 0,005
2,0
0,015 to
a
HCT780XG 1.9926 0,18 0,80 2,50 0,05 0,01 1,4 0,15 0,005
1,0
0,015 to
HCT980X 1.0944 0,20 1,00 2,90 0,050 0,010 1,40 0,15 0,005
2,0
0,015 to
a
HCT980XG 1.0997 0,23 1,00 2,90 0,050 0,010 1,40 0,15 0,005
2,0
0,015 to
HCT1180X 1.9929 0,25 1,00 2,90 0,050 0,010 1,40 0,15 0,005
1,0
0,015 to
a
HCT1180XG 1.9930 0,20 1,00 2,90 0,050 0,010 1,40 0,15 0,005
1,0
Dual-phase steels with improved formability (XH)
0,015 to
HCT590XH 1.9931 0,15 0,80 2,50 0,050 0,010 1,40 0,15 0,005
1,0
0,015 to
HCT780XH 1.9932 0,18 0,80 2,50 0,050 0,010 1,40 0,15 0,005
1,0
0,015 to
HCT980XH 1.9933 0,23 1,20 2,90 0,050 0,010 1,40 0,15 0,005
1,0
0,015 to
HCT1180XH 1.9934 0,25 1,50 2,90 0,050 0,010 1,40 0,15 0,005
1,0
Transformation induced plasticity steels (T)
0,015 to
HCT690T 1.0947 0,24 2,00 2,20 0,050 0,010 0,60 0,20 0,005
2,0
0,015 to
HCT780T 1.0948 0,25 2,20 2,50 0,050 0,010 0,60 0,20 0,005
2,0
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Chemical composition
Steel grade % by mass
+Z,+ZF,+ZM
Cr + Nb +
C Si Mn P S Al B
total
Mo Ti
Steel name Steel number max. max. max. max. max. max. max. max.
Complex-phase steels (C)
0,015 to
HCT600C 1.0953 0,18 0,80 2,20 0,080 0,015 1,00 0,15 0,005
2,0
0,015 to
HCT780C 1.0954 0,18 1,00 2,50 0,050 0,010 1,00 0,15 0,005
1,0
0,015 to
HCT980C 1.0955 0,23 1,00 2,70 0,050 0,010 1,00 0,15 0,005
1,0
0,015 to
HCT1180C 1.9928 0,23 1,00 2,90 0,050 0,010 1,00 0,15 0,005
1,0
Complex-phase steels with improved formability (CH)
0,015 to
HCT980CH 1.9935 0,20 1,20 3,00 0,050 0,015 1,00 0,15 0,005
1,0
0,015 to
HCT1180CH 1.9936 0,23 1,20 3,00 0,050 0,010 1,00 0,15 0,005
1,0
0,015 to
HCT1370CH 1.9937 0,26 1,20 3,00 0,050 0,010 1,00 0,15 0,005
1,0
Multi-phase steels with high global formability (AH)
0,015 to
HCT980AH 1.9938 0,26 2,20 2,50 0,050 0,010 1,40 0,15 0,005
2,0
0,015 to
HCT1180AH 1.9939 0,26 2,20 3,00 0,050 0,010 1,40 0,15 0,005
2,0
a
XG means dual-phase steel with increased yield strength.
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Table 5 — Chemical composition (cast analysis) of multiphase steels
for cold forming (hot rolled products)
Chemical composition
Steel grade % by mass
+Z,+ZF, +ZM
Cr + Nb +
C Si Mn P S Al B
total
Mo Ti
Steel
Steel name max. max max. max. max. max. max. max.
number
Ferritic-bainitic steels (F)
0,015
HDT450F 1.0961 0,18 0,50 2,00 0,050 0,010 1,00 0,15 0,005
to 2,0
0,015
HDT580F 1.0994 0,18 0,50 2,00 0,050 0,010 1,00 0,15 0,01
to 2,0
Dual-phase steel (X)
0,015
HDT580X 1.0936 0,14 1,0 2,20 0,085 0,015 1,40 0,15 0,005
to 1,0
Complex-phase steels (C)
0,015
HDT760C 1.0998 0,18 1,00 2,20 0,050 0,010
1,00 0,25 0,005
to 1,2
0,015
HDT950C 1.0958 0,23 1,00 2,70 0,080 0,015 1,20 0,25 0,005
to 1,20
oSIST prEN 10346:2025
prEN 10346:2025 (E)
Table 6 — Permissible deviations of th
...