

kSIST FprEN 18213-2:2026
(Main)District heating and district cooling pipes - Bonded single and twin pipe systems for directly buried hot and cold water networks - Part 2: Qualification testing of PE-Welder
- Abstract
This document specifies the methods of examining the knowledge and skill set of the PE-welder required to carry out on-site weldable joint casing connections on thermally insulated rigid single and twin pipe systems for directly buried hot and cold water networks according to EN 13941-1 [7] and EN 13941-2 [8] also as for flexible pipe systems according to EN 15632-1 [10], EN 15632-2 [11], EN 15632-3 [12], EN 15632-4 [13], EN 17414-1 [17], EN 17414-2 [18], EN 17414-3 [19], EN 17878-1 [23], EN 17878-2 [24], EN 17878-3 [25] and CEN/TS 17889 [26].
The application of these specifications ensures that the examination is carried out according to a standardised examining procedure.
This document applies to the following processes:
- preparatory works for joint casing assembly;
- assembling and testing the elements for surveillance systems;
- assembling weldable joint casing system;
- executing hot gas welding and hot gas extrusion welding
- verifying joint tightness (leak-tightness testing);
- thermally insulating the joint casing (PUR foaming or half-shell);
- sealing fill & vent openings (weldable plugs);
- assessing overall installation quality of the completed welded joint casing assembly and on-site welded component (non-destructive);
Requirements for test institutes and supervisors are also specified.
NOTE Due to differences of the specific application methods and equipment from joint casing system suppliers, it might be advisable for the PE-welder to be certified for the particular weldable joint casing system.
- Status
- Not Published
- Public Enquiry End Date
- 24-Dec-2025
- Technical Committee
- I13 - Imaginarni 13
- Current Stage
- 5020 - Formal vote (FV) (Adopted Project)
- Start Date
- 20-Aug-2026
- Due Date
- 08-Oct-2026
- Completion Date
- 20-Aug-2026

kSIST FprEN 18213-2:2026 is a CEN draft European Standard for district heating and district cooling pipe systems. It specifies how the knowledge and practical skill of a PE-welder are examined for on-site welded joint casing connections on directly buried hot and cold water networks, including joint casing assembly, hot gas welding, hot gas extrusion welding, leak-tightness testing, insulation and plug sealing. It is written for test institutes, supervisors, PE-welders, training bodies and certification organisations.
What does kSIST FprEN 18213-2:2026 specify?
kSIST FprEN 18213-2:2026 sets out a standardised examination procedure for PE-welders who work on thermally insulated single and twin pipe systems for directly buried hot and cold water networks. The document is aimed at proving competence for the work that protects the joint area, so that installation quality can be checked in a consistent way.
The scope covers on-site joint casing connections for rigid systems according to EN 13941-1 and EN 13941-2, and it also names related flexible pipe system standards in the same field. The document is organised into Clauses 1 to 13 and Annexes A to E.
| Annex | What it covers |
|---|---|
| Annex A | Qualification of PE-Welders, including training content and subject areas |
| Annex B | Checklist for welded joint casing systems, hot gas welding and hot gas extrusion welding |
| Annex C | Further test examples for hot gas extrusion welding |
| Annex D | Template PE-Welder qualification test certificate |
| Annex E | Template PE-Welder qualification test identity card |
What are the key requirements of kSIST FprEN 18213-2:2026?
Examination bodies and access to the test
Clause 4 requires the examination to be carried out by a recognised Test Institute and supervised by a qualified Supervisor. In practice, this means the exam body must have suitable premises, test equipment and documented experience in joint casing installation, because the result is meant to be accepted as a formal qualification.
The Test Institute recognition process is tied to Euroheat & Power (EHP), and the recognition period is 5 years. Clause 5 limits admission to candidates whose training or work history indicates that they are likely to pass, and it includes training in handling of isocyanate. Annex A explains the recommended training and the technical topics that should support that entry stage.
Theoretical test
Clause 6.2 requires a supervised theoretical test with 20 multiple-choice questions completed in no more than one hour and without teaching aids. The questions cover personal protective equipment (PPE), trench preparation, storage and handling of chemicals, tools, site conditions, welding areas, surveillance systems, leak-tightness testing, PUR-foam, sealing openings and health and safety.
In practice, this test checks whether the candidate understands the job before touching the pipe system. A candidate who cannot answer the theory questions is unlikely to work safely or follow the installation sequence correctly on site.
Practical test
Clause 6.3 requires a practical test under supervision on an approved weldable joint casing system or a defined test piece. The candidate is responsible for personal protective and suitable installation equipment, and the test centre must have equipment that is sound, functional and calibrated when it is used.
The practical test covers the full workflow that matters on site: preparation, assembling measuring elements, preparing welding areas, handling the joint casing system, hot gas welding or hot gas extrusion welding where relevant, leak-tightness testing, PUR-foam work, closing fill and vent openings, visual inspection and documentation. The test is limited to 120 minutes per test piece, so the candidate has to work in a controlled and organised way.
Clause 6.3.3 and 6.3.4 describe the above-ground test piece arrangements that simulate site conditions. For hot gas welding and hot gas extrusion welding, the document uses a T-piece, and Annex C gives additional T-piece examples for the extrusion welding part.
Checking, evaluation and acceptance
Clauses 8 and 9 describe how the Supervisor checks identity, materials, equipment and the assembled test piece. If the candidate runs into difficulties that are not their fault, the test piece can be replaced with prior approval, and errors may only be repaired with permission.
Clause 9 uses a clear pass or fail outcome, recorded as conform or non-conform. The evaluation includes measuring elements, visual inspection of the welded joint casing, visual inspection of hot gas welding and hot gas extrusion welding, preparation of the test piece, bending tests on specimens, and a mechanical test for welded PE plugs. Annex B is the checklist used for that assessment.
Result, qualification and validity
Clause 10 says the qualification is passed only if both the theoretical and practical tests are passed. The theoretical test requires at least 80% correct answers, while the practical test must satisfy the requirements for each relevant section in Clause 9.
The qualification certificate and identity card are defined so that employers and site supervisors can verify competence. Clause 12 gives the qualification a validity period of 3 years, with conditions on continuous work, no interruption longer than 6 months, and annual employer confirmation of continuing competence. Clause 13 allows renewal before expiry, with timing rules that affect when the renewed validity starts.
What terms does kSIST FprEN 18213-2:2026 define?
- PE-welder - the person whose knowledge and practical skill are examined for on-site joint casing work and related PE welding tasks.
- Test Institute - a recognised centre that examines PE-welders and may also train them.
- Supervisor - the qualified person who supervises, rates and validates the examination.
- Weldable joint casing system - the PE casing system assembled and welded around the joint area to protect it and keep it sealed.
- Surveillance system - the monitoring system fitted into the joint casing, including measuring wires and electrical checks.
- PUR-foam - the polyurethane foam used to thermally insulate the joint casing cavity.
- Hot gas welding - a PE welding process used in the joint casing and T-piece tests.
- Hot gas extrusion welding - a PE welding process with its own practical test examples and specimen checks.
Who uses kSIST FprEN 18213-2:2026?
kSIST FprEN 18213-2:2026 is used by test institutes that examine PE-welders, and by supervisors who run and mark the examination. It also matters to PE-welders, installers, manufacturers, suppliers and employers who need a documented qualification for joint casing work on district heating and district cooling networks.
Certification bodies and training organisations use it to structure recognition, training and evidence of competence. Quality managers and buyers can use it to check whether a worker, contractor or training programme matches the expected qualification process for site installation work.
Which standards are used with kSIST FprEN 18213-2:2026?
- EN 253 - provides the factory-made pipe assembly basis used in the practical test set-up.
- EN 448 - supports the fitting assembly and the visual requirements for processed welding.
- EN 489-1 - is the main reference for joint casing assemblies and thermal insulation, and it is the basis for the practical qualification scope.
- EN 14419 - covers surveillance systems and their installation checks.
- EN 17248:2019 - provides the terms and definitions used by the document.
- EN 13941-1:2019 and EN 13941-2:2019 - define the design and installation framework for the network types named in the scope.
- EN 15632-1 to EN 15632-4, EN 17414-1 to EN 17414-3, EN 17878-1 to EN 17878-3 and CEN/TS 17889 - are named in the scope as related standards for flexible pipe systems in the same application area.
- prEN 18213-1 - is the companion part for fitter qualification testing and is also referenced for combined qualification arrangements.
What does the kSIST FprEN 18213-2:2026 document contain?
The document contains a full qualification framework, not just a short test description. It includes the training subjects in Annex A, a detailed examination checklist in Annex B, and additional hot gas extrusion welding examples in Annex C.
It also includes figures for the test piece set-ups and tables for specimen positions, preparation criteria, plug assessment and the practical qualification scope. For administration, the document provides templates for a certificate and an identity card in Annexes D and E, which are used to record and present the PE-welder qualification on site.
Get Certified
Connect with accredited certification bodies for this standard

Institut za varilstvo d.o.o. (Welding Institute)
Slovenia's leading welding institute since 1952. ISO 3834, EN 1090, pressure equipment certification, NDT personnel, welder qualification. Only IIW Au
Sponsored listings
Frequently Asked Questions
kSIST FprEN 18213-2:2026 is a draft published by the Slovenian Institute for Standardization (SIST). Its full title is "District heating and district cooling pipes - Bonded single and twin pipe systems for directly buried hot and cold water networks - Part 2: Qualification testing of PE-Welder". This standard covers: This document specifies the methods of examining the knowledge and skill set of the PE-welder required to carry out on-site weldable joint casing connections on thermally insulated rigid single and twin pipe systems for directly buried hot and cold water networks according to EN 13941-1 [7] and EN 13941-2 [8] also as for flexible pipe systems according to EN 15632-1 [10], EN 15632-2 [11], EN 15632-3 [12], EN 15632-4 [13], EN 17414-1 [17], EN 17414-2 [18], EN 17414-3 [19], EN 17878-1 [23], EN 17878-2 [24], EN 17878-3 [25] and CEN/TS 17889 [26]. The application of these specifications ensures that the examination is carried out according to a standardised examining procedure. This document applies to the following processes: - preparatory works for joint casing assembly; - assembling and testing the elements for surveillance systems; - assembling weldable joint casing system; - executing hot gas welding and hot gas extrusion welding - verifying joint tightness (leak-tightness testing); - thermally insulating the joint casing (PUR foaming or half-shell); - sealing fill & vent openings (weldable plugs); - assessing overall installation quality of the completed welded joint casing assembly and on-site welded component (non-destructive); Requirements for test institutes and supervisors are also specified. NOTE Due to differences of the specific application methods and equipment from joint casing system suppliers, it might be advisable for the PE-welder to be certified for the particular weldable joint casing system.
This document specifies the methods of examining the knowledge and skill set of the PE-welder required to carry out on-site weldable joint casing connections on thermally insulated rigid single and twin pipe systems for directly buried hot and cold water networks according to EN 13941-1 [7] and EN 13941-2 [8] also as for flexible pipe systems according to EN 15632-1 [10], EN 15632-2 [11], EN 15632-3 [12], EN 15632-4 [13], EN 17414-1 [17], EN 17414-2 [18], EN 17414-3 [19], EN 17878-1 [23], EN 17878-2 [24], EN 17878-3 [25] and CEN/TS 17889 [26]. The application of these specifications ensures that the examination is carried out according to a standardised examining procedure. This document applies to the following processes: - preparatory works for joint casing assembly; - assembling and testing the elements for surveillance systems; - assembling weldable joint casing system; - executing hot gas welding and hot gas extrusion welding - verifying joint tightness (leak-tightness testing); - thermally insulating the joint casing (PUR foaming or half-shell); - sealing fill & vent openings (weldable plugs); - assessing overall installation quality of the completed welded joint casing assembly and on-site welded component (non-destructive); Requirements for test institutes and supervisors are also specified. NOTE Due to differences of the specific application methods and equipment from joint casing system suppliers, it might be advisable for the PE-welder to be certified for the particular weldable joint casing system.
kSIST FprEN 18213-2:2026 is classified under the following ICS (International Classification for Standards) categories: 23.040.07 - Pipeline and its parts for district heat; 23.040.99 - Other pipeline components. The ICS classification helps identify the subject area and facilitates finding related standards.
kSIST FprEN 18213-2:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
oSIST prEN 18213-2:2025
01-december-2025
Cevi za daljinsko ogrevanje in daljinsko hlajenje - Sistemi s spojenimi eno- in
dvocevnimi sistemi za neposredno vkopana omrežja za toplo in hladno vodo - 2.
del: Preskus usposobljenosti PE-varilca
District heating and district cooling pipes - Bonded single and twin pipe systems for
directly buried hot and cold water networks - Part 2: Qualification testing of PE-Welder
Fernwärme- und Fernkälterohre - Ein- und Doppelrohr-Verbundsysteme für direkt
erdverlegte Fernwärme- und Fernkältenetze - Teil 2: Prüfung von PE-Schweißern
Tuyaux de chauffage et de refroidissement urbains - Systèmes bloqués de monotubes et
bitubes pour les réseaux d'eau chaude et froide enterrés directement - Partie 2 :
Épreuve de qualification de soudeur de PE
Ta slovenski standard je istoveten z: prEN 18213-2
ICS:
23.040.07 Cevovodi za daljinsko Pipeline and its parts for
ogrevanje in njihovi deli district heat
23.040.99 Drugi sestavni deli za Other pipeline components
cevovode
oSIST prEN 18213-2:2025 en,fr,de
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
oSIST prEN 18213-2:2025
oSIST prEN 18213-2:2025
DRAFT
EUROPEAN STANDARD
prEN 18213-2
NORME EUROPÉENNE
EUROPÄISCHE NORM
October 2025
ICS 23.040.07; 23.040.99
English Version
District heating and district cooling pipes - Bonded single
and twin pipe systems for directly buried hot and cold
water networks - Part 2: Qualification testing of PE-Welder
Tuyaux de chauffage et de refroidissement urbains - Fernwärme- und Fernkälterohre - Ein- und
Systèmes bloqués de monotubes et bitubes pour les Doppelrohr-Verbundsysteme für direkt erdverlegte
réseaux d'eau chaude et froide enterrés directement - Fernwärme- und Fernkältenetze - Teil 2: Prüfung von
Partie 2 : Épreuve de qualification de soudeur de PE PE-Schweißern
This draft European Standard is submitted to CEN members for enquiry. It has been drawn up by the Technical Committee
CEN/TC 107.
If this draft becomes a European Standard, CEN members are bound to comply with the CEN/CENELEC Internal Regulations
which stipulate the conditions for giving this European Standard the status of a national standard without any alteration.
This draft European Standard was established by CEN in three official versions (English, French, German). A version in any other
language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC
Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
Recipients of this draft are invited to submit, with their comments, notification of any relevant patent rights of which they are
aware and to provide supporting documentation.
Warning : This document is not a European Standard. It is distributed for review and comments. It is subject to change without
notice and shall not be referred to as a European Standard.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2025 CEN All rights of exploitation in any form and by any means reserved Ref. No. prEN 18213-2:2025 E
worldwide for CEN national Members.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
Page
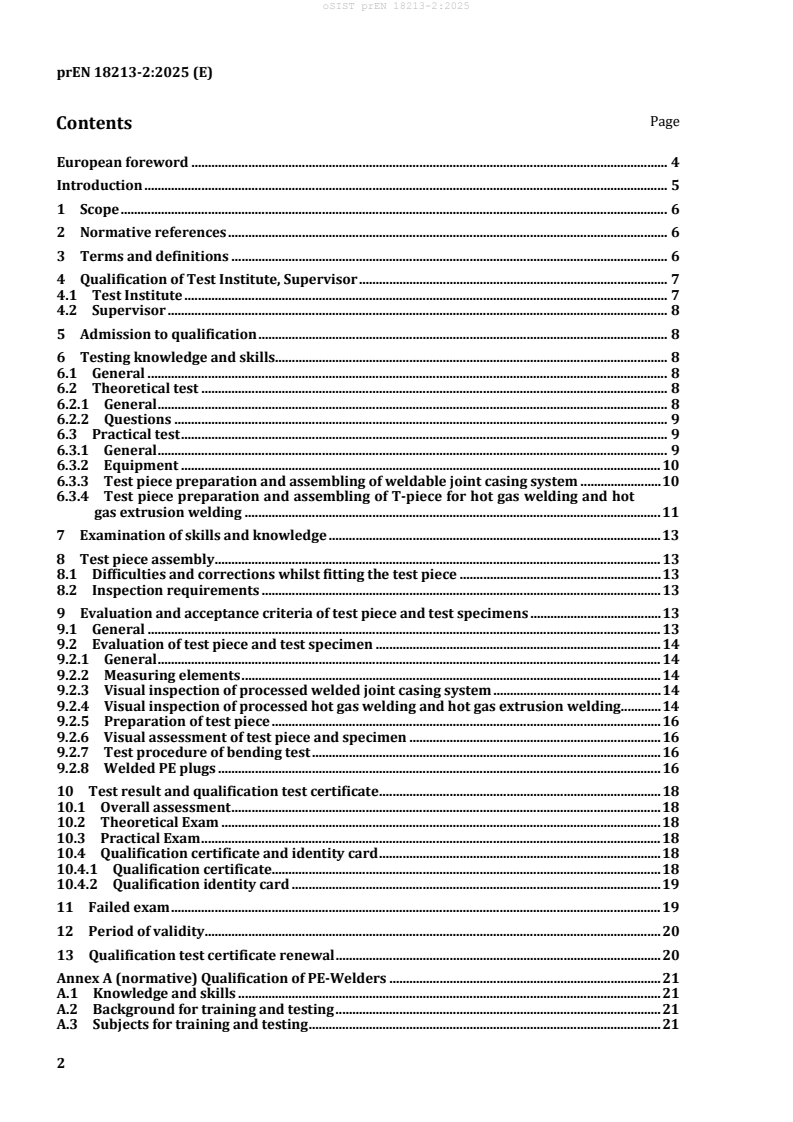
Contents
European foreword . 4
Introduction . 5
1 Scope . 6
2 Normative references . 6
3 Terms and definitions . 6
4 Qualification of Test Institute, Supervisor . 7
4.1 Test Institute . 7
4.2 Supervisor . 8
5 Admission to qualification . 8
6 Testing knowledge and skills. 8
6.1 General . 8
6.2 Theoretical test . 8
6.2.1 General . 8
6.2.2 Questions . 9
6.3 Practical test . 9
6.3.1 General . 9
6.3.2 Equipment . 10
6.3.3 Test piece preparation and assembling of weldable joint casing system . 10
6.3.4 Test piece preparation and assembling of T-piece for hot gas welding and hot
gas extrusion welding . 11
7 Examination of skills and knowledge . 13
8 Test piece assembly . 13
8.1 Difficulties and corrections whilst fitting the test piece . 13
8.2 Inspection requirements . 13
9 Evaluation and acceptance criteria of test piece and test specimens . 13
9.1 General . 13
9.2 Evaluation of test piece and test specimen . 14
9.2.1 General . 14
9.2.2 Measuring elements . 14
9.2.3 Visual inspection of processed welded joint casing system . 14
9.2.4 Visual inspection of processed hot gas welding and hot gas extrusion welding . 14
9.2.5 Preparation of test piece . 16
9.2.6 Visual assessment of test piece and specimen . 16
9.2.7 Test procedure of bending test . 16
9.2.8 Welded PE plugs . 16
10 Test result and qualification test certificate . 18
10.1 Overall assessment . 18
10.2 Theoretical Exam . 18
10.3 Practical Exam . 18
10.4 Qualification certificate and identity card . 18
10.4.1 Qualification certificate. 18
10.4.2 Qualification identity card . 19
11 Failed exam . 19
12 Period of validity. 20
13 Qualification test certificate renewal . 20
Annex A (normative) Qualification of PE-Welders . 21
A.1 Knowledge and skills . 21
A.2 Background for training and testing . 21
A.3 Subjects for training and testing . 21
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
A.3.1 General . 21
A.3.2 Polyethylene (PE) casing . 22
A.3.3 Surveillance systems . 22
A.3.4 PUR-foam system . 22
A.3.5 Joint casing systems . 23
A.3.6 Joint installation . 25
Annex B (normative) Checklist of welded joint casing systems as well as hot gas and hot
gas extrusion welding . 29
Annex C (informative) Further test examples for hot gas extrusion welding . 32
C.1 General . 32
C.2 Weld on main pipe only . 32
C.3 Weld on main pipe and branch . 33
C.4 Weld on saddle piece . 33
C.5 Weld at branch . 34
Annex D (informative) Template PE-Welder's qualification test certificate . 35
Annex E (informative) Template PE-Welder's qualification test identity card. 36
E.1 Front of the identity card (Example) . 36
E.2 Back of the identity card (Example) . 36
Bibliography . 39
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
European foreword
This document (prEN 18213-2:2025) by Technical Committee CEN/TC 107 “District heating and cooling
systems”, the secretariat of which is held by DS.
This document is currently submitted to the CEN Enquiry.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
Introduction
The installation quality of the joint casing application and of measuring elements for surveillance
systems also as welding of PE-casings is crucial for the service life and efficiency of district heating and
cooling networks, built with factory-made thermally insulated pipe, fitting and valve assemblies.
Damage caused by improper application leads to moisture ingress into the thermal insulation and to
corrosion of the steel service pipe.
This document deals with the installation of weldable joint casing systems according to EN 489-1[1] as
well as with hot gas welding and hot gas extrusion welding.
The PE-welder's ability to follow verbal or written instructions and to evidence his skills are important
factors in ensuring the integrity of the joint casing connection.
This document serves as the basis for the general recognition by test and certification bodies of the PE-
welder's competency and qualification.
PE-welders can also take an examination according to prEN 18213-1[2] to demonstrate their ability to
install sealable joint casing systems.
This document is an integral part of the standards for bonded pipe systems for district heating and
cooling.
EN 13941-
Other standards from CEN/TC 107 covering this subject: EN 253[3], EN 448[4], EN 489-1[1],
1[5], EN 13941-2[6], EN 14419[7], EN 15698-1[8], EN 15698-2[9], EN 17248[10], EN 17415-1[11], EN
17415-2[12], EN 17415-3[13], EN 17878-1[14], EN 17878-2[15], EN 17878-3[16] and prEN 18213-1[2]
are listed in the bibliography.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
1 Scope
This document specifies the methods of examining the knowledge and skill set of the PE-welder
required to carry out on-site joint casing connections on thermally insulated single and twin pipe
systems for directly buried hot and cold water networks according to EN 13941-1:2019[17] and EN
13941-2:2019[18].
The application of these specified methods specifications ensures that the examination is carried out
according to a standardised examining procedure.
This document applies to the following processes:
— preparatory works for joint casing assembly;
— assembling and testing the elements for surveillance systems;
NOTE For special surveillance systems it can be important to have additional training.
— preparatory works for joint casing system installation;
— assembling weldable joint casing system;
— executing hot gas welding and hot gas extrusion welding
— verifying joint tightness (leakage testing);
— thermally insulating the joint casing (PUR foaming or half-shell);
— sealing fill & vent openings (weldable plugs);
— assessing overall installation quality of the completed joint connection (non-destructive).
2 Normative references
The following documents are referred to in the text in such a way that some or all of their content
constitutes requirements of this document. For dated references, only the edition cited applies. For
undated references, the latest edition of the referenced document (including any amendments) applies.
EN 253, District heating pipes - Bonded single pipe systems for directly buried hot water networks - Factory
made pipe assembly of steel service pipe, polyurethane thermal insulation and a casing of polyethylene
EN 448, District heating pipes - Bonded single pipe systems for directly buried hot water networks - Factory
made fitting assemblies of steel service pipes, polyurethane thermal insulation and a casing of polyethylene
EN 489-1, District heating pipes - Bonded single and twin pipe systems for buried hot water networks -
Part 1: Joint casing assemblies and thermal insulation for hot water networks in accordance with EN
13941-1
EN 14419, District heating pipes - Bonded single and twin pipe systems for buried hot water networks -
Surveillance systems
EN 17248:2019, District heating and district cooling pipe systems - Terms and definitions
3 Terms and definitions
For the purposes of this document, the terms and definitions given in EN 17248:2019 apply.
ISO and IEC maintain terminological databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at http://www.iso.org/obp
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
— IEC Electropedia: available at http://www.electropedia.org/
4 Qualification of Test Institute, Supervisor
4.1 Test Institute
The test institute is a recognized centre for the examination of PE-welders.
NOTE The training of PE-welders can also take place at the test institute.
Test institutes can be companies that:
— manufacture factory made district heating and district cooling pipe, fitting and valve assemblies ,
— distribute factory made district heating and district cooling pipe, fitting and valve assemblies,
— carry out joint installation work on factory made bonded and flexible pipe systems for district
heating and district cooling,
who have demonstrated extensive theoretical and practical experience in joint casing installation over
a minimum period of 5 years.
or:
— institutions whose business activities include the education and examination of specialist staff,
however with additional personnel requirements, in case extensive theoretical and practical
expertise over a minimum period of 5 years cannot be demonstrated.
Factual requirements for the test institute are suitable equipment engineering, testing technology and
premises for knowledge and practical skills tests.
The application for recognition as testing institute shall be submitted in writing to the Euroheat & Power
association (EHP), followed by an examination of the required specialist knowledge of the supervisors
as well as by an inspection of the required spatial and factual infrastructure. A group of experts decides
on the award or refusal of the certificate of recognition or raises deficiencies for rectification.
The rules of procedure for the entire recognition process should be adhered to
— process of the recognition procedure
— duration of validity
— recognition of additional supervisors
— issuance, expiry or withdrawal of recognition
— monitoring
— review
— extension of the period of validity
— change of recognition
— complaints procedure
The recognition is valid for a period of 5 years. In order to maintain its recognition, the test institute
shall ensure the necessary premises, technical equipment, further training and the availability of a
recognized supervisor.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
4.2 Supervisor
The qualification of a supervisor shall be:
— an engineer, bachelor, master, technician or state-recognized master craftsman respectively
master chamber of industry and commerce in a relevant technical profession;
— proving extensive theoretical and practical experience over a minimum period of 5 years in joint
casing installation as well as in the assessment of joint casing quality characteristics, in particular
in the joint casing installation processes to be tested;
— having served at least 3 observations/internships during PE-welder examinations;
— knowledgeable and experienced in PE-welding processes.
Instead of the 5 years of practical experience, the necessary skills can be demonstrated through the
following evidence:
— a valid test certificate according to this document, and
, and
— a valid test certificate according to prEN 18213-1[2]
— at least 10 days observation/internship on joint casing installation construction sites.
5 Admission to qualification
Only applicants whose training and/or previous activities show that they are likely to pass the planned
test may be admitted as a candidate.
As a rule, this is the case if one of the following is met:
— completed apprenticeship as plastics fabricator;
— at least one year experience as joint casing installation assistant, confirmed by employer’s
declaration;
— completion of both a theoretical and practical training course in preparation for the PE-welder´s
qualification test.
The applicant shall be trained in handling of isocyanate.
NOTE Further information can be found in the European REACH regulation.
The content of the training course is defined in Annex A.
6 Testing knowledge and skills
6.1 General
The candidate shall demonstrate in qualification tests his theoretical knowledge according to 6.2 and
practical skills according to 6.3.
6.2 Theoretical test
6.2.1 General
The candidate’s knowledge of the practical rules for skillful and safe working shall be evaluated in a
theoretical test.
This part of the qualification test is carried out under the supervision of the supervisor.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
The candidate shall answer 20 multiple-choice questions. Filling in the questionnaire shall not exceed
one hour and be continuous without access to teaching aids.
The questions shall cover the subjects in 6.2.2.
6.2.2 Questions
The questions shall be related to the following subjects, as appropriate:
— personal protective equipment (PPE) (observe the national requirements)
— preparation of pipe trench
— storage, transport and handling of chemicals and flammable/corrosive substances
— proper installation equipment and tools
— surrounding conditions for joint casing installation
— working and ambient conditions
— systems and products to be used
— preparatory works for joint casing installation
— assembly and test of surveillance systems
— preparation of welding areas
— installation of weldable joint casing systems
— execution of hot gas welding and hot gas extrusion welding (if a qualification is intended for)
— tightness testing of the joint casing prior to thermal insulation
— production of PUR foam sample
— thermal insulation of joint casing cavity
— sealing foam and vent openings
— self-assessment possibilities of welded joint casing assembly
— awareness of health and safety requirements.
6.3 Practical test
6.3.1 General
The practical test shall be carried out under the supervision of the supervisor on a weldable joint casing
system approved in accordance with EN 489-1 and / or on a test piece according to 6.3.4.
Assembling the test piece is to be carried out following the installation instructions.
Prior to the practical test, the supervisor shall inform the candidates about the procedure of examining
and rating the individual installation steps. During the practical test, the supervisor shall not provide
any advice.
All materials and documents necessary for the practical test shall be available to the candidate.
The PE-welder himself is responsible for the personal protective and suitable installation equipment.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
The PE-welder himself can decide whether to use his own tools and equipment (or those of his
employer) or those of the test centre. Unless the PE-welder uses the tools and equipment of the test
centre, separate proof shall be provided about its flawless condition, functionality and calibration.
Depending on the qualification aimed for, the PE welder shall produce a separate test piece for joint
casing systems 4.1 and 5.1 in accordance with EN 489-1 as well as for the hot gas welding and hot gas
extrusion welding processes according to 6.3.4.
The practical test shall be conducted within 120 minutes per test piece.
Subject areas of the practical test are:
— preparatory works for weldable joint casing assembly or T-piece according to 6.3.4;
— assembly of measuring elements and test of surveillance system;
— preparation of welding areas;
— handling of joint casing system;
— execution of hot gas welding and hot gas extrusion welding (if qualification is intended for);
— tightness test of joint casing, if applicable;
— handling of PUR foam
— closing of foam and vent openings, if applicable;
— visual inspection of assembled joint casing system / T-piece;
— documentation of joint casing system / T-piece installation.
6.3.2 Equipment
The equipment to be used in the practical test shall be in flawless condition, functional and calibrated.
Equipment can be the one of the candidate or of the test institute.
6.3.3 Test piece preparation and assembling of weldable joint casing system
The test piece shall be positioned above ground level similarly to the situation on site. The height of the
supports to be attached to the free ends of the steel service pipe shall be between 200 and 400 mm from
the floor to the bottom edge of the steel service pipe, see Figure 1.
The test piece shall be properly prepared for assembling of the joint casing system by the candidate.
Key
A Non-rotating pipe fixings
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
B Factory made pipe assembly according to EN 253
C Weldable joint casing system according to EN 489-1
D Distance between floor and bottom edge of the service pipe (200 mm to 400 mm)
E Floor
Figure 1 — Set-up of the test piece for the preparation and assembly of the joint casing system
6.3.4 Test piece preparation and assembling of T-piece for hot gas welding and hot gas
extrusion welding
A T-piece is used as the test piece. It shall be positioned above ground level similarly to the situation on
site. The height of the supports to be attached to the free ends of the steel service pipe shall be between
200 and 400 mm from the floor to the bottom edge of the steel service pipe, see Figure 2.
Further possible examples for hot gas welding and hot gas extrusion welding are shown in Annex C. If a
test piece other than shown in Figure 2 is used in the practical test, it shall be mentioned in the
Certificate.
The test piece shall be properly prepared for assembling of the casing construction by the applicant.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
Key
1 Pipe assembly according to EN 253[19] with diameter casing (DC) 160 mm
2 Main pipe casing with cut-out [window] for branch-off pipe
3 Pipe assembly according to EN 253[19] with diameter casing (DC) 110 mm
4 Branch pipe casing
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
5 Circumferential weld seams by root pass using the hot gas welding process with or without filler material
and by cover pass using the hot gas extrusion welding process
6 Longitudinal seams as V-seam by root pass using the hot gas welding process with or without filler
material and by cover pass using the hot gas extrusion welding process
7 Ground level
8 Non-rotating pipe fixings
Figure 2 — Arrangement and dimensions of the test piece (Dimensional data [mm] as circa
dimensions)
7 Examination of skills and knowledge
The exam shall be supervised, rated and validated by the supervisor.
8 Test piece assembly
8.1 Difficulties and corrections whilst fitting the test piece
In the event of difficulties during the practical test for which the candidate is not responsible, the test
piece on which assembling has been started may be replaced provided the supervisor’s prior consent.
Errors made or occurring during the assembling may be repaired only after permission has been given
by the supervisor.
8.2 Inspection requirements
Before assembling, the supervisor shall check the identity of the candidate as well as the suitability of
the materials and equipment. The test piece shall be identified with the number or mark of the
supervisor and of the candidate.
The supervisor shall
— supervise the preparation and the assembling of the test piece.
— terminate the qualification test if the assembling is not in compliance with the manufacturer’s
instructions or the candidate does not have the skills required to obtain a satisfactory result.
— visually check the test piece after completion by the candidate.
9 Evaluation and acceptance criteria of test piece and test specimens
9.1 General
The supervisor inspects the installation documentation and evaluates the test specimen made by the
candidate.
The test has to be evaluated as follows:
— “c”: conform;
— “nc”: non-conform.
Storage or disposal of the test piece or test specimens shall be as instructed by the supervisor.
oSIST prEN 18213-2:2025
prEN 18213-2:2025 (E)
9.2 Evaluation of test piece and test specimen
9.2.1 General
Assembling of the test piece shall comply with the
— installation instructions of the joint casing system used in the practical test
— execution conditions of hot gas welding and hot gas extrusion welding.
The supervisor shall visually evaluate the correct application by accompanying the assembly of the test
piece by the candidate.
After completion of the test piece, visual inspection and destructive tests shall be performed under
supervision.
The evaluation shall be recorded in accordance with Annex B.
Mechanical-technological tests in general shall be carried out after cooling down to 20 +/-10°C.
Test piece or test specimens are stored or disposed of in accordance with the supervisor’s instructions.
9.2.2 Measuring elements
The following requirements shall be met when installing the monitoring system according to EN 14419:
— Applying the spacers
— Connecting the measuring wires
— Checking for electrical continuity
— Testing for electrical circuit
— Measuring the electrical insulation resistance
— Evaluate the measured values of electrical circuit and electrical insulation resistance
9.2.3 Visual inspection of processed welded joint casing system
— Joint casing is centred over the joint, evenly installed without overheating and firmly resting
against the casing (no upstanding edges)
— There shall be visible marks in the welded zones where pressure bands have been p
...