

SIST EN 1370:2026
(Main)Founding - Examination of surface condition
- Abstract
This document specifies methods for the examination of surface condition (roughness and surface discontinuities) of castings on surfaces that remain as-cast.
This document is applicable to all cast metals and all casting processes except die casting.
This document is not applicable to machined surfaces.
- Status
- Published
- Public Enquiry End Date
- 09-Oct-2025
- Publication Date
- 09-Sep-2026
- Technical Committee
- IFEK - Ferrous metals
- Current Stage
- 6060 - National Implementation/Publication (Adopted Project)
- Start Date
- 04-Sep-2026
- Due Date
- 09-Nov-2026
- Completion Date
- 10-Sep-2026
SIST EN 1370:2026 specifies methods for examining the surface condition of castings, focusing on roughness and surface discontinuities on surfaces that remain as-cast. It is the Slovenian adoption of EN 1370:2026 from CEN and is used when buyers and foundries need a common way to judge casting surfaces in practice.
What does SIST EN 1370:2026 specify?
SIST EN 1370:2026 covers how to examine as-cast surfaces on cast metals, and it applies to all casting processes except die casting. It does not apply to machined surfaces, so its methods are aimed at the condition of the casting surface itself, not later machining marks.
The document is organized into:
- Clause 1 - Scope
- Clause 2 - Normative references
- Clause 3 - Terms and definitions
- Clause 4 - Comparators
- Clause 5 - Requirements
- Clause 6 - Documentation
- Annex A - Significant technical changes from the previous edition
Clause 4 and Clause 5 are central because they describe the comparator-based and instrument-based ways to assess roughness and the visual methods for checking surface discontinuities.
What are the key requirements of SIST EN 1370:2026?
SIST EN 1370:2026 makes surface-condition checking something that must be agreed in advance between the parties. In practice, the order or drawing needs to state the required severity level, any unacceptable discontinuities, the areas to be examined, how many castings are checked, and the manufacturing stage for the inspection.
Agreement before inspection
Clause 5.1 requires that different surfaces on the same casting may have different severity levels, and this must be shown clearly on the drawing. The examination is to be carried out by trained personnel with satisfactory visual acuity, which matters because the method depends on human visual judgment.
Roughness by comparators or instruments
Clause 5.2 limits the roughness methods to casting surfaces and to the sample rate agreed for the order. Visual tactile comparators are used without optical aids and must be held next to the casting under sufficient lighting; the result is acceptable when the casting surface is as rough as, or smoother than, the comparator.
Clause 5.2.3 also allows contact stylus instruments or non-contact optical instruments, but only when agreed at the time of ordering. If that route is chosen, the method, areas, scan size, measured profile parameters, and acceptable minimum or maximum values all have to be set out up front.
Surface discontinuities
Clause 5.3 requires the surface to be clean before inspection, so rust, sand, scale, mould residues, oil, grease, and similar contamination do not mask defects. The discontinuity assessment uses the dimensions H and L, and step-like borders or edges that are not parting lines are treated as discontinuities.
Clause 5.3.2 classifies discontinuities by size into severity levels VD1 to VD8. The practical point is that very small height or depth is ignored below the lower limit, while larger castings can justify larger permitted discontinuities if that is agreed.
Comparator-based classification for steel and iron castings
Clause 5.3.3 uses visual tactile comparators for steel and iron castings and asks for each discontinuity category to be judged against the relevant severity level. It covers inclusions, gas porosities, laps and cold shuts, scabs, inserts, and welds, and the result is satisfactory only if the area is equal to or better than the stated comparator.
Clause 5.3.3 also links surface roughness to what discontinuities can normally be detected. In practice, a rougher surface can hide smaller defects, so the roughness level affects the inspection limit.
Documentation
Clause 6 requires a record and report when this is agreed at ordering. The record identifies the casting, the examiner, the comparator or instrument used, the category and level for each area, and the results.
What terms does SIST EN 1370:2026 define?
SIST EN 1370:2026 uses several key terms and abbreviations in its inspection method.
- Comparator - a positive replica of an actual casting surface used as the reference for visual comparison.
- Visual tactile comparator - a comparator used by direct side-by-side viewing without optical aids.
- Ra - the arithmetic mean roughness parameter used as guidance for surface roughness.
- VD - the severity series for surface discontinuities based on dimensions, standing for Visual examination of discontinuities Dimensions.
- VC - the severity series for visual comparator assessment of discontinuities, standing for Visual examination of discontinuities by Comparators.
- H - the largest depth or height of a discontinuity measured perpendicular to the surface.
- L - the largest length of a discontinuity.
Who uses SIST EN 1370:2026?
SIST EN 1370:2026 is used by foundries, inspection personnel, quality managers, and customers who specify or accept castings. It is relevant when the surface condition of as-cast parts has to be checked during purchasing, production, or acceptance.
It is especially useful when the parties need a shared way to:
- agree the required surface quality on drawings or orders
- compare castings with BNIF or SCRATA comparators
- check roughness and visible surface discontinuities
- record the outcome of inspection for traceability
What changed in SIST EN 1370:2026 from the previous edition?
SIST EN 1370:2026 supersedes EN 1370:2011. Annex A summarizes the significant technical changes.
The changes stated in the document are:
- Clause 2 was added for normative references to match CEN drafting rules
- Clause 3 was added for terms and definitions to match CEN drafting rules
- Table 4 was corrected for the severity levels VC2, VC3, and VC4 for laps and cold shuts, and inserts
- the introduction updates the supplier information for BNIF 359
Which standards are used with SIST EN 1370:2026?
SIST EN 1370:2026 has no normative references, but it cites related documents that support its use.
- EN 1559-3 - gives guidance on specifying acceptance criteria for iron castings.
- EN 13018 - gives general principles for visual testing.
- BNIF 359 - provides comparator specimens used for surface-condition assessment of castings.
- SCRATA surface comparators for the definition of surface quality of steel and iron castings - provide comparator sets for steel and iron castings.
- SCRATA surface comparators for the definition of surface texture of precision steel castings - provide the precision-steel comparator set used for finer surface assessment.
What does the SIST EN 1370:2026 document contain?
SIST EN 1370:2026 contains the comparator tables and visual classification methods used to judge casting surfaces. Tables 1 and 2 compare roughness categories for BNIF and SCRATA comparator sets, while Table 3 classifies discontinuities by size and Table 4 classifies common discontinuity types for steel and iron castings.
It also includes Figure 1 for the H and L dimensions of discontinuities and Figure 2 for step irregularities. Table 5 links surface roughness to the smallest discontinuities that can normally be detected, which is important when choosing an inspection method and setting an acceptance limit.
Annex A lists the main technical changes from EN 1370:2011, and the bibliography identifies the comparator documents and related standards used in the text.
Relations
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Referred By
SIST EN 1371-2:2000 - Founding - Liquid penetrant inspection - Part 2: Investment castings - Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Sep-2026
- Effective Date
- 02-Feb-2023
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.

BSMI (Bureau of Standards, Metrology and Inspection)
Taiwan's standards and inspection authority.
Inštitut za kovinske materiale in tehnologije
Institute of Metals and Technology. Materials testing, metallurgical analysis, NDT.
Sponsored listings
Frequently Asked Questions
SIST EN 1370:2026 is a standard published by the Slovenian Institute for Standardization (SIST). Its full title is "Founding - Examination of surface condition". This standard covers: This document specifies methods for the examination of surface condition (roughness and surface discontinuities) of castings on surfaces that remain as-cast. This document is applicable to all cast metals and all casting processes except die casting. This document is not applicable to machined surfaces.
This document specifies methods for the examination of surface condition (roughness and surface discontinuities) of castings on surfaces that remain as-cast. This document is applicable to all cast metals and all casting processes except die casting. This document is not applicable to machined surfaces.
SIST EN 1370:2026 is classified under the following ICS (International Classification for Standards) categories: 17.040.20 - Properties of surfaces; 77.180 - Equipment for the metallurgical industry. The ICS classification helps identify the subject area and facilitates finding related standards.
SIST EN 1370:2026 has the following relationships with other standards: It is inter standard links to SIST EN 1371-2:2015, SIST EN 1559-2:2000, SIST EN 15776:2011, SIST EN 15551:2017, SIST EN 15689:2012, SIST EN 1559-5:2017, SIST EN 1559-3:2011, SIST EN 1371-2:2000, SIST EN 12680-2:2026, SIST EN 15551:2009+A1:2010, SIST EN 1559-2:2014, SIST EN 1370:2012. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
SIST EN 1370:2026 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
SLOVENSKI STANDARD
01-oktober-2026
Livarstvo - Preiskave hrapavosti površine
Founding - Examination of surface condition
Gießereiwesen - Bewertung des Oberflächenzustandes
Fonderie - Contrôle de l'état de surface
Ta slovenski standard je istoveten z: EN 1370:2026
ICS:
17.040.20 Lastnosti površin Properties of surfaces
77.180 Oprema za metalurško Equipment for the
industrijo metallurgical industry
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.
EN 1370
EUROPEAN STANDARD
NORME EUROPÉENNE
August 2026
EUROPÄISCHE NORM
ICS 17.040.20; 77.180 Supersedes EN 1370:2011
English Version
Founding - Examination of surface condition
Fonderie - Contrôle de l'état de surface Gießereiwesen - Bewertung des Oberflächenzustandes
This European Standard was approved by CEN on 19 July 2026.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this
European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references
concerning such national standards may be obtained on application to the CEN-CENELEC Management Centre or to any CEN
member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by
translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC Management
Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia,
Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway,
Poland, Portugal, Republic of North Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and
United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION
EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre: Rue de la Science 23, B-1040 Brussels
© 2026 CEN All rights of exploitation in any form and by any means reserved Ref. No. EN 1370:2026 E
worldwide for CEN national Members.
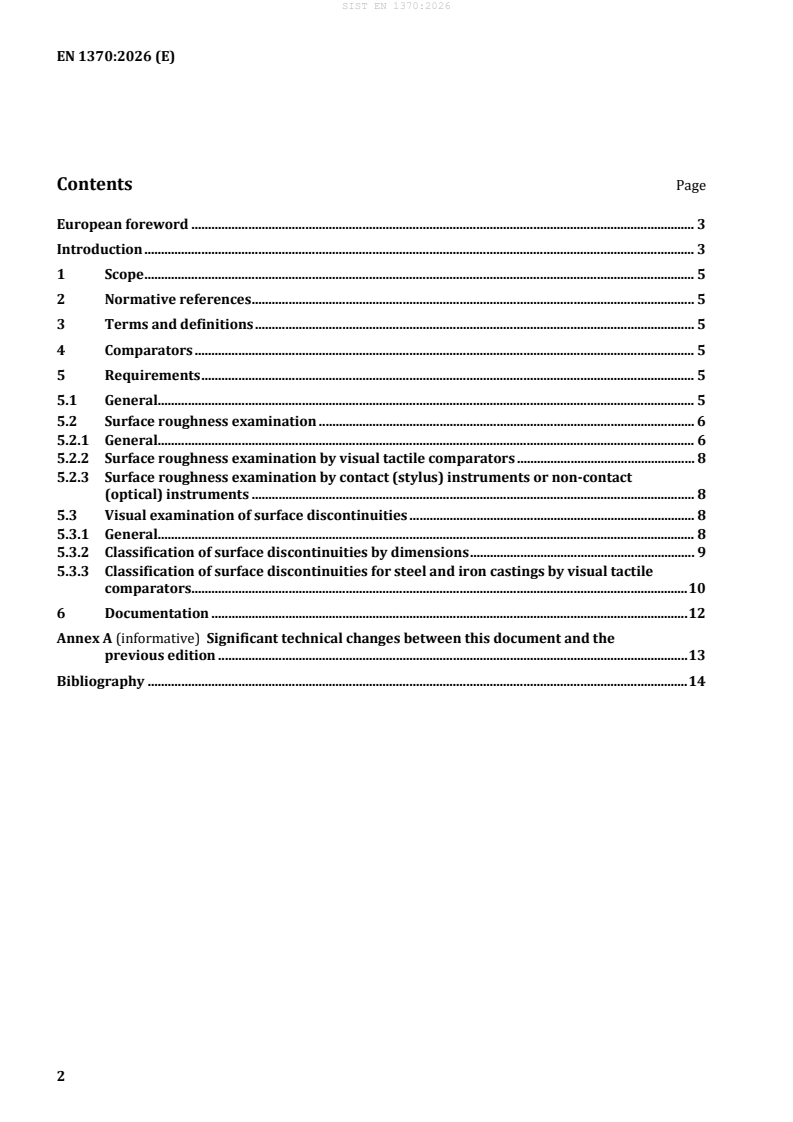
Contents Page
European foreword . 3
Introduction . 3
1 Scope . 5
2 Normative references . 5
3 Terms and definitions . 5
4 Comparators . 5
5 Requirements . 5
5.1 General. 5
5.2 Surface roughness examination . 6
5.2.1 General. 6
5.2.2 Surface roughness examination by visual tactile comparators . 8
5.2.3 Surface roughness examination by contact (stylus) instruments or non-contact
(optical) instruments . 8
5.3 Visual examination of surface discontinuities . 8
5.3.1 General. 8
5.3.2 Classification of surface discontinuities by dimensions . 9
5.3.3 Classification of surface discontinuities for steel and iron castings by visual tactile
comparators. 10
6 Documentation . 12
Annex A (informative) Significant technical changes between this document and the
previous edition . 13
Bibliography . 14
European foreword
This document (EN 1370:2026) has been prepared by Technical Committee CEN/TC 190 “Foundry
technology”, the secretariat of which is held by DIN.
This European Standard shall be given the status of a national standard, either by publication of an
identical text or by endorsement, at the latest by February 2027 and conflicting national standards shall
be withdrawn at the latest by February 2027.
Attention is drawn to the possibility that some of the elements of this document may be the subject of
patent rights. CEN shall not be held responsible for identifying any or all such patent rights.
This document supersedes EN 1370:2011.
Annex A, Table A.1 provides details of significant technical changes between this document and the
previous edition.
Any feedback and questions on this document should be directed to the users’ national standards body.
A complete listing of these bodies can be found on the CEN website.
According to the CEN-CENELEC Internal Regulations, the national standards organizations of the
following countries are bound to implement this European Standard: Austria, Belgium, Bulgaria, Croatia,
Cyprus, Czech Republic, Denmark, Estonia, Finland, France, Germany, Greece, Hungary, Iceland, Ireland,
Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Republic of North
Macedonia, Romania, Serbia, Slovakia, Slovenia, Spain, Sweden, Switzerland, Türkiye and the United
Kingdom.
Introduction
The surface roughness of a casting is influenced by the manufacturing process (moulding, grinding,
finishing, etc.), the moulding materials used (sand, coating, etc.), the production equipment available and
the alloy cast.
Depending on the applications of the casting, the surface requirements are related to mechanical
loadings, appearance, surface treatment, etc.
Since cast surfaces do not exhibit the same cyclic character as machined surfaces, it is difficult to evaluate
their roughness using conventional mechanical, optical, or pneumatic devices. Other optical/electronic
means are now available for measuring surface roughness of cast surfaces. For the ease of use, visual
tactile comparators are preferred.
Moreover, in order to take into account the irregularities on as-cast surfaces, ground surfaces or other
means of finishing of castings, comparators should have relatively large dimensions in order to make
them more reliable and their results repeatable and consistent.
Two sets of comparators are in widespread use:
— “BNIF 359 Recommandation technique du Bureau de Normalisation des Industries de la Fonderie.
Caractérisation d'états de surface des pièces moulées — Utilisation des échantillons types
de 110 × 160 mm”, available from CETIM, KMØ - 30 rue François Spoerry, 68100 Mulhouse,
France [1];
— “SCRATA comparators for the definition of surface quality of steel and iron castings”, ASTM A 802
Shorter Set, available from Castings Technology International, Advanced Manufacturing Park, Brunel
Way, Rotherham, S60 5WG, South Yorkshire, United Kingdom [2].
A third set of comparators, for precision steel castings, is also available:
— “SCRATA surface comparators for the definition of surface texture of precision steel castings”,
precision set, available from Castings Technology International, Advanced Manufacturing Park,
Brunel Way, Rotherham, S60 5WG, South Yorkshire, United Kingdom [3].
This document also specifies 8 levels of surface imperfections based on maximum dimensions to be
detected by visual examination.
The SCRATA comparators shorter set [2], can also be used for the classification of surface discontinuities
on steel and iron castings.
BNIF N°359 comparators can be used for all cast metals.
100 mm × 150 mm for SCRATA comparators; 110 mm × 160 mm for BNIF comparators.
1 Scope
This document specifies methods for the examination of surface condition (roughness and surface
discontinuities) of castings on surfaces that remain as-cast.
This document is applicable to all cast metals and all casting processes except die casting.
This document is not applicable to machined surfaces.
2 Normative references
There are no normative references in this document.
3 Terms and definitions
No terms and definitions are listed in this document.
ISO and IEC maintain terminology databases for use in standardization at the following addresses:
— ISO Online browsing platform: available at https://www.iso.org/obp/
— IEC Electropedia: available at https://www.electropedia.org/
4 Comparators
The comparators are essentially positive replicas of actual casting surfaces: as-cast or after further
fettling treatment such as shot blasted or ground.
Full size photographs of the comparators can be used to assist in making a rapid evaluation of the overall
roughness of the comparators. These can give preliminary information for the appropriate selection of a
moulding or finishing process.
It is emphasized however that the comparators, and not the photographs, shall be used to form the basis
of an agreement at the time of ordering.
An overview and a comparison of the different categories and levels of the three sets of comparators are
given in Tables 1, 2 and 4.
5 Requirements
5.1 General
When examination of surface conditions is required, the following shall be as agreed at the time of
ordering:
— category and s
...