


EN 10228-4:2016
(Main)Non-destructive testing of steel forgings - Part 4: Ultrasonic testing of austenitic and austenitic-ferritic stainless steel forgings
General Information
- Abstract
This European Standard describes techniques for the manual, pulse-echo, ultrasonic testing of forgings manufactured from austenitic and austenitic-ferritic stainless steels. Mechanized scanning techniques, such as immersion testing, may be used but should be agreed between the purchaser and supplier (see Clause 4).
This part of EN 10228 applies to four types of forgings, classified according to their shape and method of production. Types 1, 2 and 3 are essentially simple shapes. Type 4 covers complex shapes.
This part of EN 10228 does not apply to:
- closed die forgings;
- turbine rotor and generator forgings.
Ultrasonic testing of ferritic and martensitic steel forgings is the subject of Part 3 of this European Standard.
- Status
- Published
- Publication Date
- 31-May-2016
- Withdrawal Date
- 30-Dec-2016
- Technical Committee
- ECISS/TC 111 - Steel castings and forgings
- Drafting Committee
- ECISS/TC 111 - Steel castings and forgings
- Current Stage
- 9093 - Decision to confirm - Review Enquiry
- Start Date
- 30-Mar-2023
- Completion Date
- 17-Sep-2026
- Directive
- Not Harmonized97/23/EC - Pressure equipment

Overview
EN 10228-4:2016 is the CEN European Standard for non‑destructive testing (NDT) of steel forgings using manual pulse‑echo ultrasonic testing specifically for austenitic and austenitic‑ferritic stainless steel forgings. It defines techniques, equipment, calibration, scanning and reporting requirements to provide consistent detection, classification and recording of discontinuities in forged stainless steel components. Mechanized scanning (for example immersion testing) may be used only by agreement between purchaser and supplier.
Key topics and technical requirements
- Scope and exclusions: Applies to forgings classified as Types 1–4 (Types 1–3 = simple shapes, Type 4 = complex). Does not apply to closed‑die forgings or turbine rotor/generator forgings.
- Test method: Manual pulse‑echo ultrasonic testing; mechanized techniques permitted if agreed. Instrument must provide A‑scan presentation and meet EN 12668‑1.
- Probes: Initial detection probes should meet EN 12668‑2. Nominal frequencies: 0.5–6 MHz. Normal‑beam effective diameters 10–40 mm; angle‑beam probe angles 35°–70° with effective areas 20–625 mm². Dual‑element probes are required for near‑surface testing.
- Calibration & reference blocks: Reference and calibration blocks per EN ISO 2400; DAC (distance‑amplitude curve) and DGS techniques are referenced for sensitivity and sizing (with limits on reference‑block use for DGS). Surface condition of reference blocks should match the test piece.
- Personnel & procedure: Operators must be qualified per EN ISO 9712. Testing is performed against a written test procedure specifying stage of manufacture, scanning plan, couplant, equipment, calibration, recording levels, sizing and acceptance criteria.
- Scanning & acceptance: Options include grid scanning or 100% scanning; scanning coverage, sensitivity setting, recording/acceptance criteria and sizing methods are defined (see EN 10228‑4 tables for recording/acceptance levels).
Applications and users
Who uses EN 10228-4:2016:
- NDT engineers and inspection personnel performing ultrasonic testing on stainless steel forgings
- Forging manufacturers and suppliers specifying inspection requirements
- Purchasers, OEMs and quality/acceptance inspectors who require standardized ultrasonic inspection procedures
- Inspection bodies and certification organizations
Practical benefits:
- Standardizes ultrasonic testing practice for austenitic stainless forgings
- Improves defect detection consistency across suppliers and purchasers
- Defines equipment, calibration and competency requirements to support reliable acceptance decisions
Related standards
- EN 12668‑1/2/3 (ultrasonic instrument/probe/equipment characterization)
- EN ISO 2400 (calibration block)
- EN ISO 16811, EN ISO 16827 (sensitivity, range and sizing)
- EN ISO 9712 (NDT personnel qualification)
- EN 10228 parts 1–3 (magnetic particle, penetrant, and ferritic/martensitic ultrasonic testing)
Keywords: EN 10228-4:2016, ultrasonic testing, austenitic stainless steel forgings, non‑destructive testing, NDT, pulse‑echo, DAC, DGS, EN ISO 9712.
Relations
- Effective Date
- 08-Jun-2016
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.

Inštitut za kovinske materiale in tehnologije
Institute of Metals and Technology. Materials testing, metallurgical analysis, NDT.
Sponsored listings
Frequently Asked Questions
EN 10228-4:2016 is a standard published by the European Committee for Standardization (CEN). Its full title is "Non-destructive testing of steel forgings - Part 4: Ultrasonic testing of austenitic and austenitic-ferritic stainless steel forgings". This standard covers: This European Standard describes techniques for the manual, pulse-echo, ultrasonic testing of forgings manufactured from austenitic and austenitic-ferritic stainless steels. Mechanized scanning techniques, such as immersion testing, may be used but should be agreed between the purchaser and supplier (see Clause 4). This part of EN 10228 applies to four types of forgings, classified according to their shape and method of production. Types 1, 2 and 3 are essentially simple shapes. Type 4 covers complex shapes. This part of EN 10228 does not apply to: - closed die forgings; - turbine rotor and generator forgings. Ultrasonic testing of ferritic and martensitic steel forgings is the subject of Part 3 of this European Standard.
This European Standard describes techniques for the manual, pulse-echo, ultrasonic testing of forgings manufactured from austenitic and austenitic-ferritic stainless steels. Mechanized scanning techniques, such as immersion testing, may be used but should be agreed between the purchaser and supplier (see Clause 4). This part of EN 10228 applies to four types of forgings, classified according to their shape and method of production. Types 1, 2 and 3 are essentially simple shapes. Type 4 covers complex shapes. This part of EN 10228 does not apply to: - closed die forgings; - turbine rotor and generator forgings. Ultrasonic testing of ferritic and martensitic steel forgings is the subject of Part 3 of this European Standard.
EN 10228-4:2016 is classified under the following ICS (International Classification for Standards) categories: 77.020 - Production of metals; 77.040.20 - Non-destructive testing of metals; 77.140.85 - Iron and steel forgings. The ICS classification helps identify the subject area and facilitates finding related standards.
EN 10228-4:2016 has the following relationships with other standards: It is inter standard links to EN 10228-4:1999, EN ISO 16811:2025, EN ISO 22232-3:2020, EN ISO 5577:2025, EN ISO 22232-1:2020, EN ISO 9712:2022, EN ISO 2400:2025, EN ISO 16827:2025, EN ISO 22232-2:2020, EN 1330-1:2014, EN 10250-1:2022, EN 14141:2003, EN 10253-4:2025, EN 10222-1:2017, EN 10222-1:1998. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
EN 10228-4:2016 is associated with the following European legislation: EU Directives/Regulations: 97/23/EC. When a standard is cited in the Official Journal of the European Union, products manufactured in conformity with it benefit from a presumption of conformity with the essential requirements of the corresponding EU directive or regulation.
EN 10228-4:2016 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.Zerstörungsfreie Prüfung von Schmiedestücken aus Stahl - Teil 4: Ultraschallprüfung von Schmiedestücken aus austenitischem und austenitisch-ferritischem nichtrostendem StahlEssais non destructifs des pièces forgées en acier - Partie 4 : Contrôle par ultrasons des pièces forgées en aciers inoxydables austénitiques et austéno-ferritiquesNon-destructive testing of steel forgings - Part 4: Ultrasonic testing of austenitic and austenitic-ferritic stainless steel forgings77.140.85Železni in jekleni kovani izdelkiIron and steel forgings77.040.20Neporušitveno preskušanje kovinNon-destructive testing of metalsICS:Ta slovenski standard je istoveten z:EN 10228-4:2016SIST EN 10228-4:2016en,fr,de01-september-2016SIST EN 10228-4:2016SLOVENSKI
STANDARDSIST EN 10228-4:20001DGRPHãþD
EUROPEAN STANDARD NORME EUROPÉENNE EUROPÄISCHE NORM
EN 10228-4
June
t r s x ICS
y yä r v rä t râ
y yä s v rä z w Supersedes EN
s r t t zæ vã s { { {English Version
Nonædestructive testing of steel forgings æ Part
vã Ultrasonic testing of austenitic and austeniticæferritic stainless steel forgings Essais non destructifs des pièces forgées en acier æ Partie
vã Contrôle par ultrasons des pièces forgées en aciers inoxydables austénitiques et austénoæferritiques Zerstörungsfreie Prüfung von Schmiedestücken aus Stahl æ Teil
vã Ultraschallprüfung von Schmiedestücken aus austenitischem und austenitischæferritischem nichtrostendem Stahl This European Standard was approved by CEN on
u October
t r s wä
egulations which stipulate the conditions for giving this European Standard the status of a national standard without any alterationä Upætoædate lists and bibliographical references concerning such national standards may be obtained on application to the CENæCENELEC Management Centre or to any CEN memberä
translation under the responsibility of a CEN member into its own language and notified to the CENæCENELEC Management Centre has the same status as the official versionsä
CEN members are the national standards bodies of Austriaá Belgiumá Bulgariaá Croatiaá Cyprusá Czech Republicá Denmarká Estoniaá Finlandá Former Yugoslav Republic of Macedoniaá Franceá Germanyá Greeceá Hungaryá Icelandá Irelandá Italyá Latviaá Lithuaniaá Luxembourgá Maltaá Netherlandsá Norwayá Polandá Portugalá Romaniaá Slovakiaá Sloveniaá Spainá Swedená Switzerlandá Turkey andUnited Kingdomä
EUROPEAN COMMITTEE FOR STANDARDIZATION COMITÉ EUROPÉEN DE NORMALISATION EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre:
Avenue Marnix 17,
B-1000 Brussels
t r s x CEN All rights of exploitation in any form and by any means reserved worldwide for CEN national Membersä Refä Noä EN
s r t t zæ vã t r s x ESIST EN 10228-4:2016
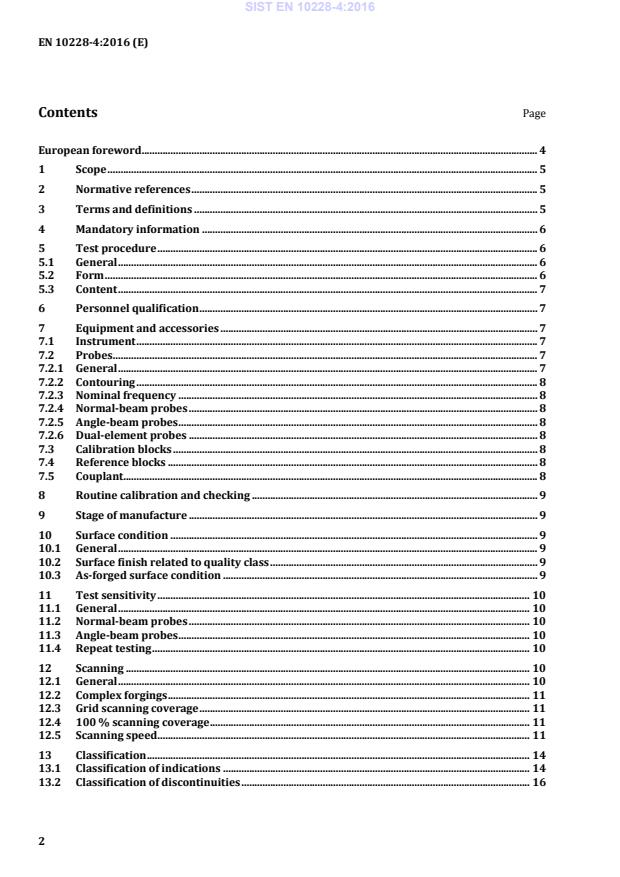
European foreword . 4 1 Scope . 5 2 Normative references . 5 3 Terms and definitions . 5 4 Mandatory information . 6 5 Test procedure . 6 5.1 General . 6 5.2 Form . 6 5.3 Content . 7 6 Personnel qualification . 7 7 Equipment and accessories . 7 7.1 Instrument . 7 7.2 Probes. 7 7.2.1 General . 7 7.2.2 Contouring . 8 7.2.3 Nominal frequency . 8 7.2.4 Normal-beam probes . 8 7.2.5 Angle-beam probes . 8 7.2.6 Dual-element probes . 8 7.3 Calibration blocks . 8 7.4 Reference blocks . 8 7.5 Couplant. 8 8 Routine calibration and checking . 9 9 Stage of manufacture . 9 10 Surface condition . 9 10.1 General . 9 10.2 Surface finish related to quality class . 9 10.3 As-forged surface condition . 9 11 Test sensitivity . 10 11.1 General . 10 11.2 Normal-beam probes . 10 11.3 Angle-beam probes . 10 11.4 Repeat testing . 10 12 Scanning . 10 12.1 General . 10 12.2 Complex forgings . 11 12.3 Grid scanning coverage . 11 12.4 100 % scanning coverage . 11 12.5 Scanning speed . 11 13 Classification . 14 13.1 Classification of indications . 14 13.2 Classification of discontinuities . 16 SIST EN 10228-4:2016
Maximum testable depth for corresponding beam path range for circumferential angle-beam scans . 22 Annex B (informative)
Amplitude of indication in dB relative to % DAC . 24 Annex C (informative)
Significant technical changes to the version EN 10228-4:1999 . 25
...